IN
₹
Apparel & Fashion
Description
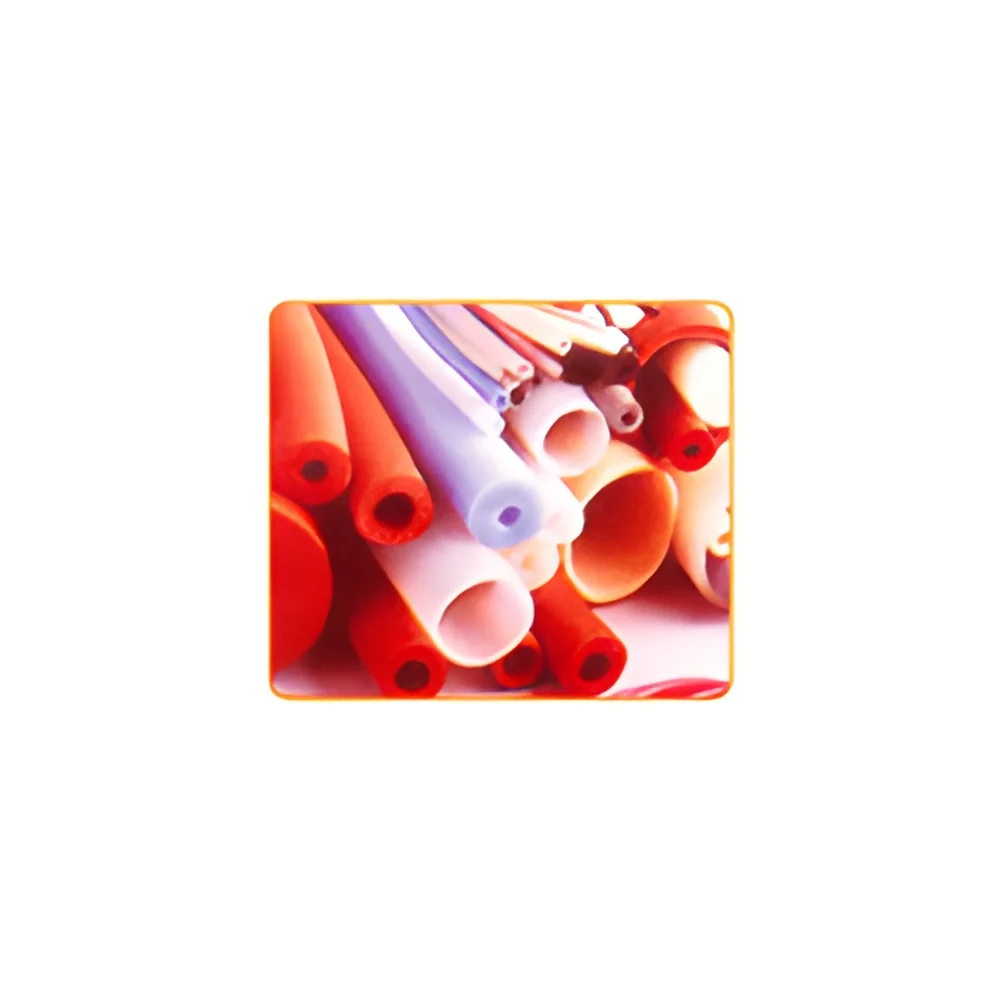
Premium food-grade silicon tubes provide reliable fluid transfer solutions for industrial applications requiring strict hygiene standards and temperature resistance. Manufactured from high-quality materials, these tubes maintain excellent performance across extreme temperature ranges while ensuring non-toxic safety for direct product contact. Their durable construction withstands demanding operational conditions, offering consistent reliability for processing systems that handle food, beverages, and pharmaceutical products. The tubes comply with international safety standards, providing assurance for operations where product purity and consumer safety are paramount.

These silicon tubes serve essential functions across multiple industrial sectors with rigorous hygiene requirements. Food processing facilities utilize them for transferring ingredients, semi-processed materials, and finished products through various production stages. Dairy operations depend on them for handling milk, cre...
Premium food-grade silicon tubes provide reliable fluid transfer solutions for industrial applications requiring strict hygiene standards and temperature resistance. Manufactured from high-quality materials, these tubes maintain excellent performance across extreme temperature ranges while ensuring non-toxic safety for direct product contact. Their durable construction withstands demanding operational conditions, offering consistent reliability for processing systems that handle food, beverages, and pharmaceutical products. The tubes comply with international safety standards, providing assurance for operations where product purity and consumer safety are paramount.

These silicon tubes serve essential functions across multiple industrial sectors with rigorous hygiene requirements. Food processing facilities utilize them for transferring ingredients, semi-processed materials, and finished products through various production stages. Dairy operations depend on them for handling milk, cream, and cultured products while enduring frequent cleaning and sanitation cycles. Breweries implement them in high-temperature brewing and transfer processes, while pharmaceutical manufacturers rely on them for sterile fluid handling in controlled environments. Agricultural applications benefit from their chemical resistance in distribution systems, demonstrating their versatility across diverse industrial settings.

The operational value of these silicon tubes lies in their proven reliability and durability, which directly contributes to reduced maintenance requirements and operational downtime. Their heat resistance and non-toxic properties ensure consistent product quality and compliance with food safety regulations, protecting both product integrity and brand reputation. The tubes are engineered to withstand harsh industrial environments, providing extended service life and excellent return on investment. Their compliance with international standards gives procurement professionals confidence in product safety and performance, making them a trusted choice for industrial fluid transfer applications.

Key Features:
- High heat resistance maintains performance across extreme temperature ranges
- Non-toxic food-grade material ensures safe product contact
- Durable construction resistant to wear, tear, and chemical exposure
- Maintains flexibility and integrity through thermal cycles
- Compliant with international food safety and quality standards

Benefits:
- Reliable performance reduces operational downtime and maintenance costs
- Safe for direct food contact protects product quality and consumer safety
- Long service life provides excellent return on investment
- Withstands harsh industrial environments and cleaning processes
- Compliance with standards ensures regulatory requirements are met
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
These food-grade silicon tubes deliver exceptional performance in demanding industrial environments where product safety and operational reliability are critical. Their high heat resistance maintains structural integrity during thermal processing, while the non-toxic composition ensures safe contact with consumable products. The tubes withstand frequent cleaning cycles and maintain flexibility across varying temperatures, making them ideal for hygienic processing systems that handle liquids, semi-liquids, and gases without contamination risk.
Multiple industries depend on these silicon tubes for consistent, safe fluid transfer operations. Food processing plants utilize them for ingredient transfer and product movement, while dairy operations rely on them for milk and yogurt processing. Breweries implement them in high-temperature brewing systems, and pharmaceutical manufacturers use them for sterile solution handling. Agricultural applications benefit from their chemical resistance in spray systems, ensuring reliable performance across diverse operational requirements.
- Transferring milk and dairy products through processing and packaging lines
- Moving beer and wort in brewing systems requiring high-temperature sanitation
- Handling pharmaceutical liquids and sterile solutions in manufacturing processes
- Distributing agricultural chemicals and fertilizers in spray application systems
- Operating pneumatic controls and fluid transfer in food processing automation
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Anil Rubber Products, Maharashtra
 Maharashtra, India
Automotive & Transport•Manufacturer•Distributor / Wholesaler
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Main Markets
Domestic
Food Grade Silicon Tubes High Heat Resistance Non Toxic
Food grade silicon tubes offer high heat resistance and non-toxic safety for food processing, dairy, brewing, and pharmaceutical applications. Durable and reliable for industrial fluid transfer systems.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Anil Rubber Products
 Maharashtra, India
Automotive & TransportManufacturer