IN
₹
Apparel & Fashion
Description
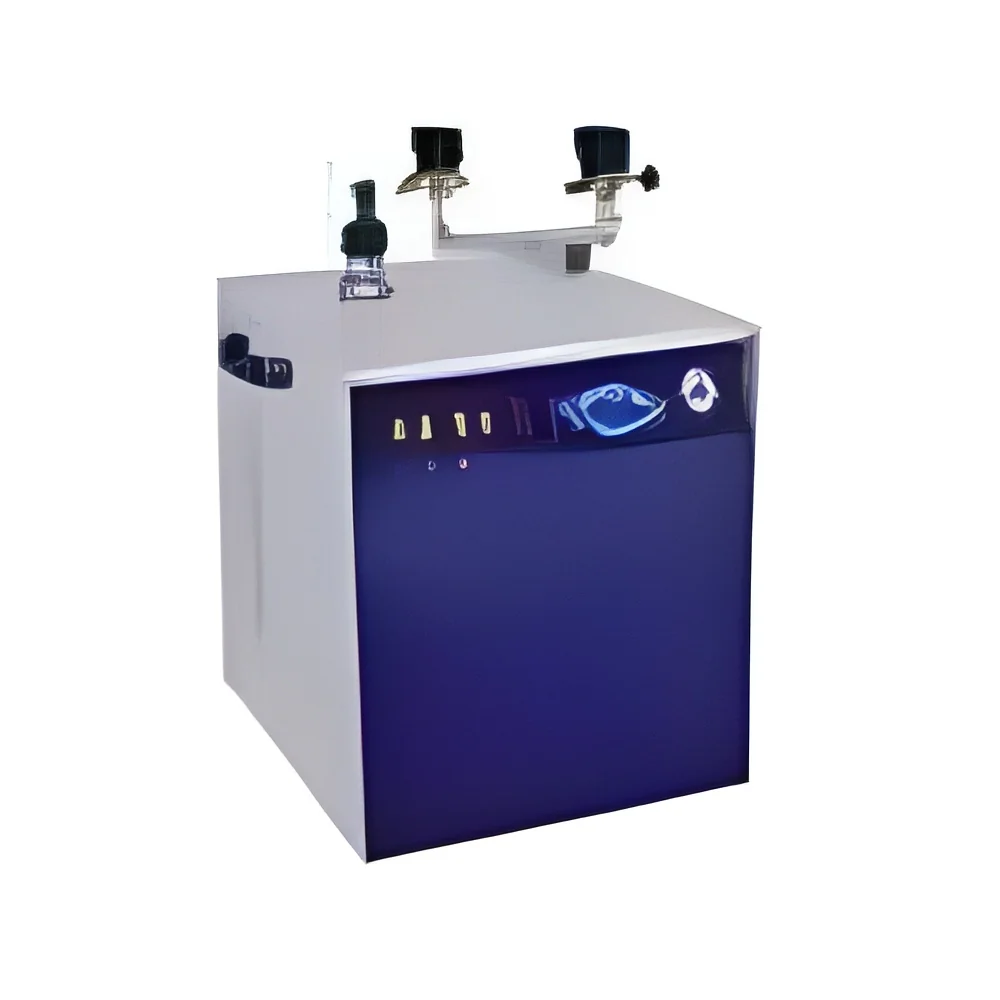
Industrial semi-automatic steam boilers represent the optimal solution for businesses requiring consistent steam generation with operational flexibility. These units bridge the gap between manual systems and fully automated boilers, offering precise control while maintaining cost efficiency. Engineered with robust materials and advanced control systems, they ensure reliable performance across diverse industrial environments. The design focuses on operational simplicity combined with industrial-grade durability, making them suitable for continuous processing applications where steam quality and availability are critical to production outcomes.

These boilers serve essential functions across multiple industrial sectors, demonstrating remarkable versatility in application. In food processing facilities, they provide steam for cooking, sterilization, and sanitation processes while meeting strict hygiene standards. Textile manufacturers utilize them for dyeing, finishing, and fabric treatme...
Industrial semi-automatic steam boilers represent the optimal solution for businesses requiring consistent steam generation with operational flexibility. These units bridge the gap between manual systems and fully automated boilers, offering precise control while maintaining cost efficiency. Engineered with robust materials and advanced control systems, they ensure reliable performance across diverse industrial environments. The design focuses on operational simplicity combined with industrial-grade durability, making them suitable for continuous processing applications where steam quality and availability are critical to production outcomes.

These boilers serve essential functions across multiple industrial sectors, demonstrating remarkable versatility in application. In food processing facilities, they provide steam for cooking, sterilization, and sanitation processes while meeting strict hygiene standards. Textile manufacturers utilize them for dyeing, finishing, and fabric treatment operations where consistent temperature control is paramount. Pharmaceutical companies depend on these units for equipment sterilization and maintaining controlled environments. Chemical processing plants leverage their precise steam delivery for various reactions and heating applications, while commercial facilities use them for space heating and humidity control in large-scale operations.

The business value of these semi-automatic steam boilers extends beyond initial investment through significant operational advantages. They deliver improved energy efficiency and reduced operational costs compared to manual systems, while requiring less capital investment than fully automated alternatives. Their robust construction ensures long-term reliability with minimal maintenance requirements, providing quick return on investment. The semi-automatic operation reduces labor costs while offering superior control over manual systems, enhancing overall process efficiency. Built to stringent quality standards, these boilers incorporate comprehensive safety features that ensure operational security and consistent performance, supporting business continuity and production targets.

Key Features:
- Semi-automatic control system for operational efficiency and user control
- Robust construction using industrial-grade materials for long service life
- Compatibility with multiple fuel types including natural gas, oil, and biomass
- Advanced safety systems with pressure gauges and automatic safety valves
- Customizable capacity and specifications to match operational requirements

Benefits:
- Reduced operational costs through improved fuel efficiency and lower labor requirements
- Enhanced process control compared to manual systems for consistent output quality
- Long-term reliability with minimal maintenance needs for continuous operation
- Flexibility in fuel selection to optimize energy costs based on local availability
- Comprehensive safety features ensuring secure operation and regulatory compliance
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Semi-automatic steam boilers provide the perfect balance between manual operation and full automation for medium-scale industrial operations. They deliver consistent steam generation with operational control while maintaining cost-effectiveness. These units are designed for businesses that require reliable steam output without complex automated systems, making them ideal for various processing applications across multiple sectors.
These versatile boilers serve critical functions in food processing, textile manufacturing, pharmaceutical production, and chemical processing industries. Their adaptability allows integration with existing systems while supporting multiple fuel options. The semi-automatic operation reduces labor requirements while maintaining precise control over steam output, temperature, and pressure parameters for diverse industrial needs.
- Sterilizing processing equipment and maintaining sterile environments in pharmaceutical facilities
- Cooking, pasteurization, and equipment cleaning in food and beverage manufacturing plants
- Fabric dyeing, finishing, and textile processing operations in manufacturing units
- Supporting chemical reactions and process heating in industrial chemical production
- Providing steam for humidification and space heating in large commercial operations
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Delhi Steam System Co., New Delhi
 New Delhi, India
Manufacturer•Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Main Markets
Domestic
Industrial Semi Automatic Steam Boilers For Manufacturing And Processing
Industrial semi-automatic steam boilers deliver reliable steam generation for manufacturing and processing operations. These efficient units feature robust construction and precise controls for consistent performance in food, textile, and chemical industries.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Delhi Steam System Co.
 New Delhi, India
Manufacturer