IN
₹
Apparel & Fashion

Description
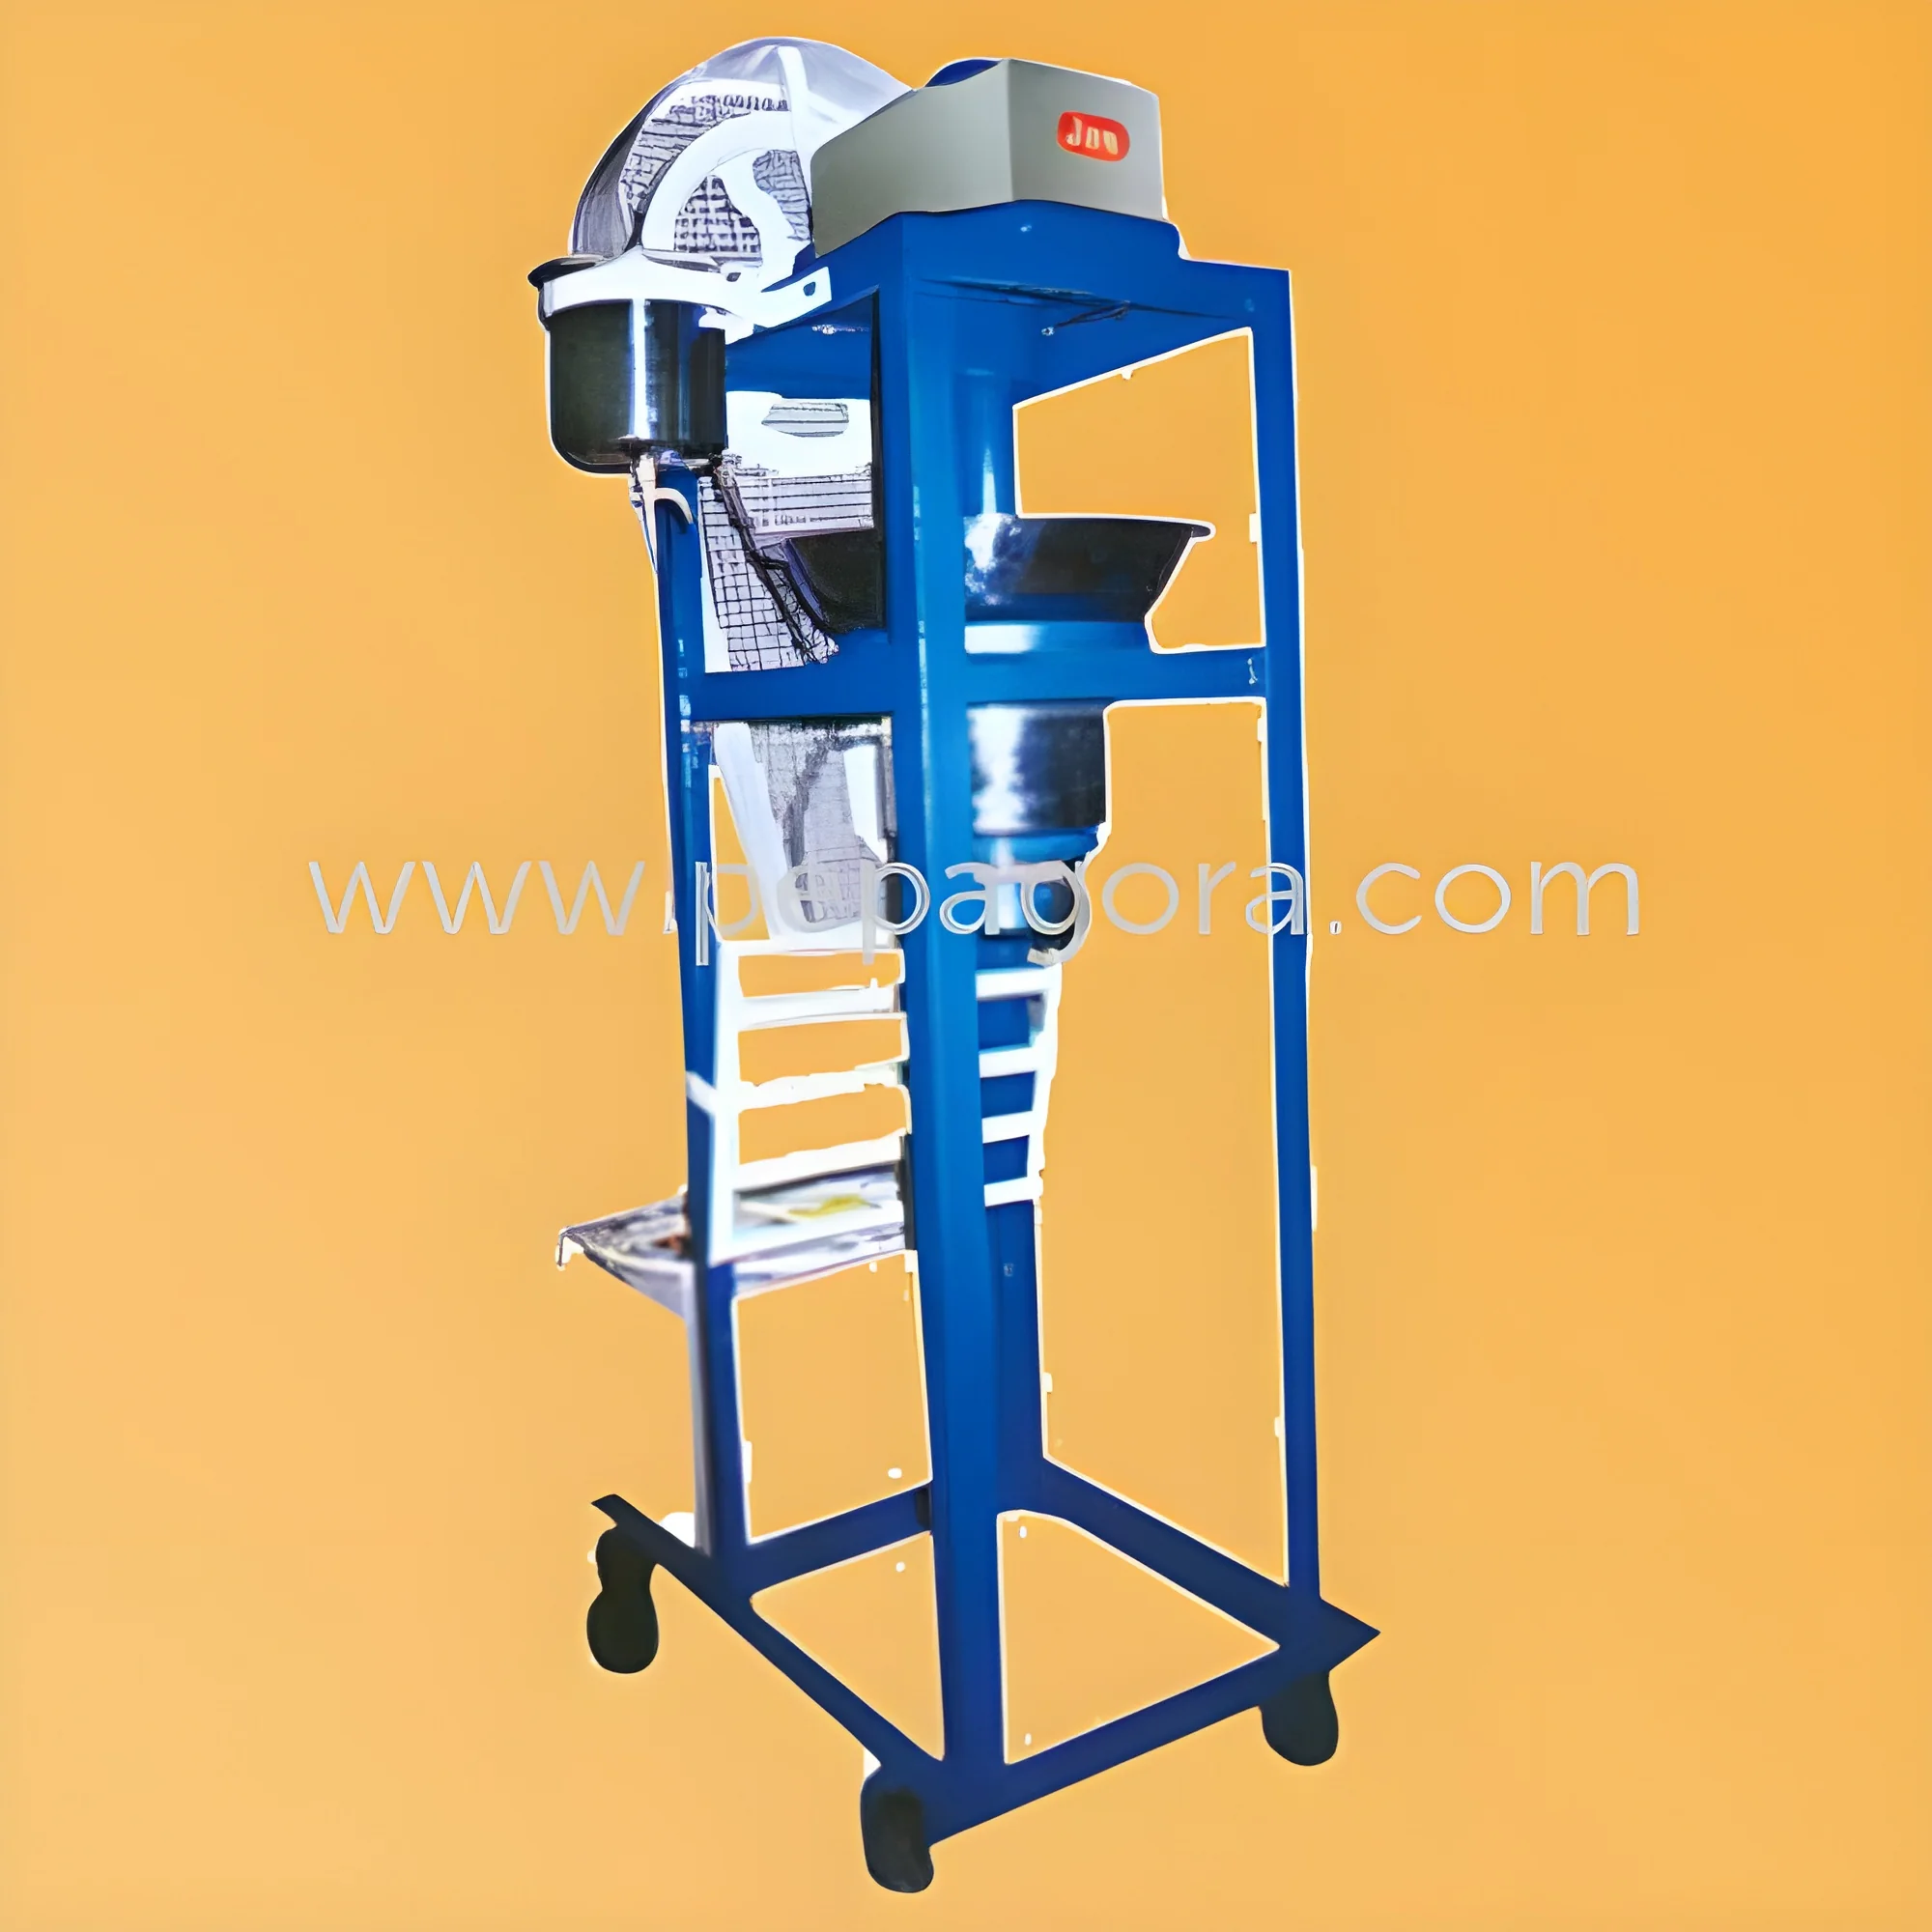
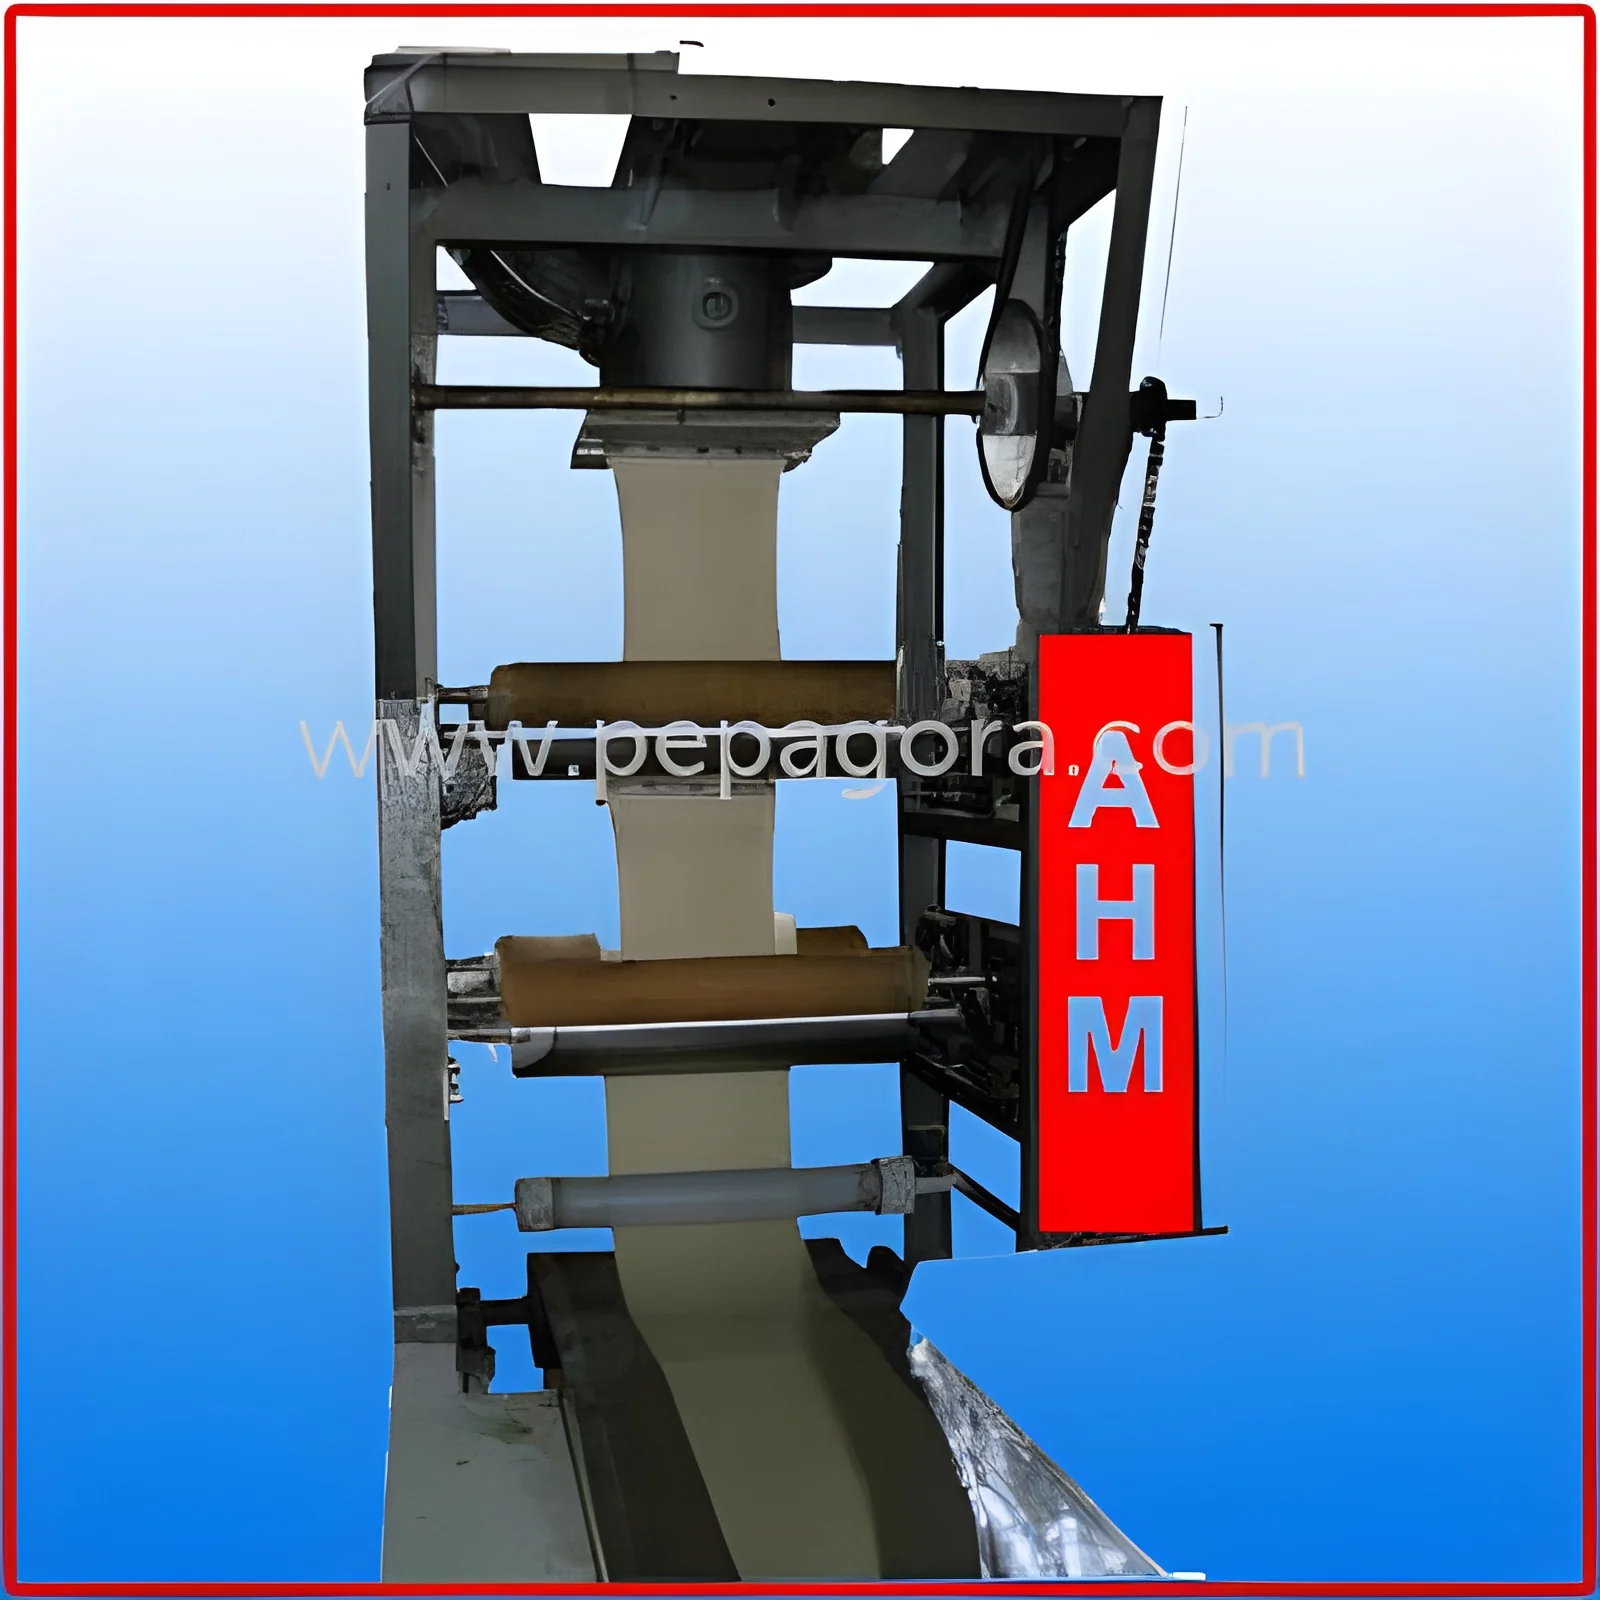
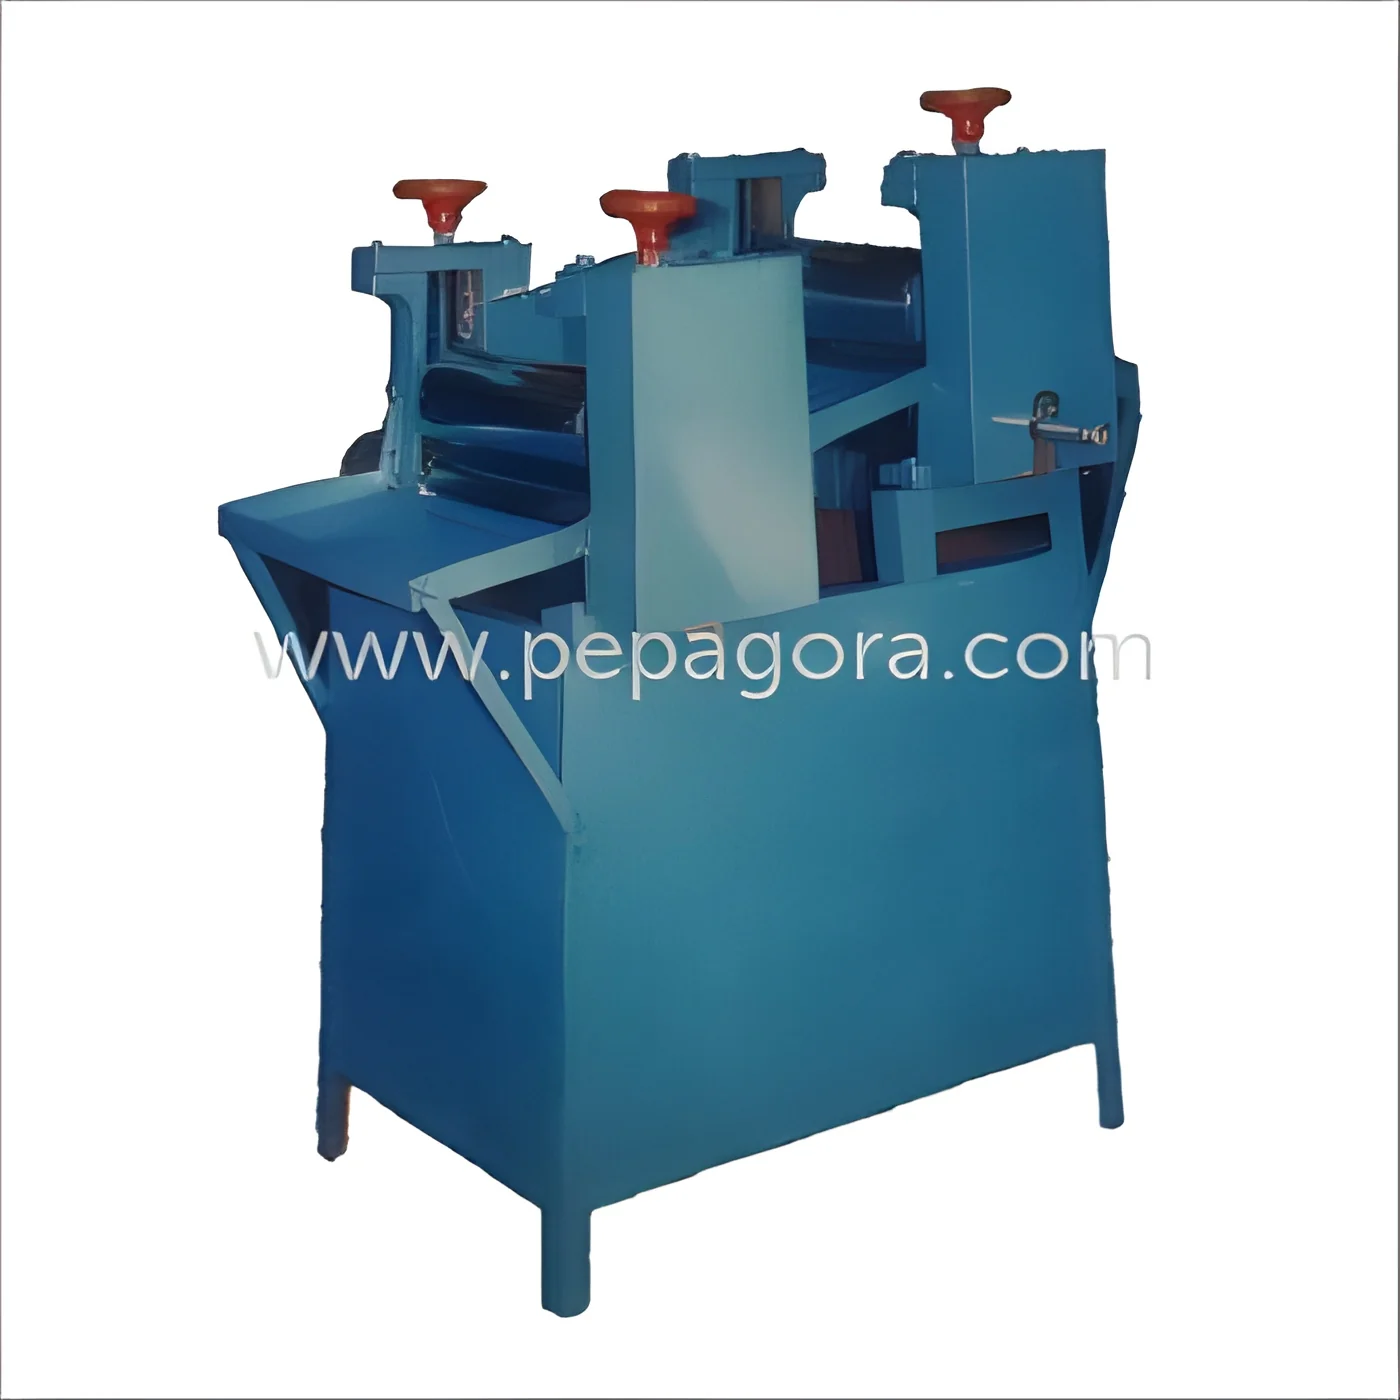
Our industrial stainless steel fire resistant screw conveyor represents premium material handling equipment engineered for demanding applications across multiple sectors. Constructed from high-grade stainless steel, this system provides exceptional resistance to corrosion, abrasion, and high temperatures, making it ideal for harsh industrial environments. The integrated fire-resistant design adds crucial safety protection for operations involving combustible materials, while the hygienic surface ensures compliance with strict cleanliness standards. Featuring a reliable belt conveyor mechanism, this equipment guarantees smooth, consistent movement of various bulk materials from fine powders to semi-solids with precision and reliability.

These screw conveyors serve critical functions across industries where operational safety and material integrity are non-negotiable. In food processing environments, they handle ingredients without contamination risk while meeting stringent hygiene requ...
Our industrial stainless steel fire resistant screw conveyor represents premium material handling equipment engineered for demanding applications across multiple sectors. Constructed from high-grade stainless steel, this system provides exceptional resistance to corrosion, abrasion, and high temperatures, making it ideal for harsh industrial environments. The integrated fire-resistant design adds crucial safety protection for operations involving combustible materials, while the hygienic surface ensures compliance with strict cleanliness standards. Featuring a reliable belt conveyor mechanism, this equipment guarantees smooth, consistent movement of various bulk materials from fine powders to semi-solids with precision and reliability.

These screw conveyors serve critical functions across industries where operational safety and material integrity are non-negotiable. In food processing environments, they handle ingredients without contamination risk while meeting stringent hygiene requirements. Chemical and pharmaceutical manufacturers rely on them for secure transport of sensitive and potentially combustible materials. Agricultural operations utilize these systems for efficient grain and feed handling in storage facilities, while wastewater treatment plants depend on them for sludge conveyance in challenging conditions. Mining and mineral processing operations benefit from the robust construction for transporting abrasive materials in demanding settings.

The business value of these screw conveyors lies in their exceptional reliability and favorable total cost of ownership. Each unit undergoes rigorous quality control and testing to ensure long service life with minimal operational interruptions. The reduced maintenance requirements translate to significant operational savings over the equipment lifespan. Easy cleaning and sanitation capabilities minimize production downtime while ensuring compliance with industry regulations. These conveyors are designed for straightforward integration into existing material handling systems, providing immediate improvements in operational efficiency, workplace safety, and material flow consistency.

Key Features:
- Premium stainless steel construction for maximum durability and corrosion resistance
- Fire-resistant properties provide enhanced safety for combustible materials
- Standard sizes and configurations available to match operational requirements
- Efficient belt conveyor mechanism ensures smooth, consistent material transport
- Designed for straightforward operation with minimal maintenance needs

Benefits:
- Enhanced workplace safety through fire-resistant construction and reliable operation
- Reduced maintenance requirements leading to lower operational costs
- Consistent material handling performance across diverse industrial applications
- Long service life with corrosion-resistant stainless steel construction
- Easy integration into existing material handling systems for immediate productivity gains
Specifications
| Key Attributes | |
|---|---|
| Material | Stainless Steel |
| Material Feature | Fire Resistant |
| Structure | Belt Conveyor |
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Stainless steel screw conveyors deliver dependable bulk material handling across demanding industrial environments where safety and hygiene are critical. Their fire-resistant properties and corrosion-resistant stainless steel construction ensure secure operations in facilities processing combustible materials or requiring strict cleanliness standards. These systems are engineered for consistent movement of powders, granules, and semi-solid materials with minimal maintenance requirements and maximum operational reliability.
Ideal for industries with rigorous safety protocols, these conveyors support continuous production without contamination risks or fire hazards. The robust design handles abrasive materials and high-temperature applications while maintaining peak efficiency. Standard sizes and configurations allow straightforward integration into existing layouts, providing reliable performance in challenging operational conditions day after day with consistent material flow and reduced downtime.
- Food processing facilities for safe transport of flour, sugar, and grain ingredients
- Chemical manufacturing plants moving combustible powders and compounds
- Pharmaceutical production lines handling sensitive granules and raw materials
- Agricultural operations for efficient grain storage and feed handling
- Wastewater treatment plants conveying sludge and solid waste materials
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Shipping & Logistics
| Port of Dispatch | Madurai |
Company Profile

ADHITHYA HITECH MACHINES, Tamil Nadu
 Tamil Nadu, India
Food & Agriculture•Manufacturer•Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Main Markets
Eastern Asia
South Asia
Southeast Asia
Industrial Stainless Steel Fire Resistant Screw Conveyor
Industrial stainless steel fire resistant screw conveyor provides reliable material handling for food, chemical, and pharmaceutical industries. Features durable construction and smooth transport of powders and granules with efficient, low-maintenance operations.
Min. Order Quantity: 1 piece
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
ADHITHYA HITECH MACHINES
 Tamil Nadu, India
Food & AgricultureManufacturer