IN
₹
Apparel & Fashion

Description
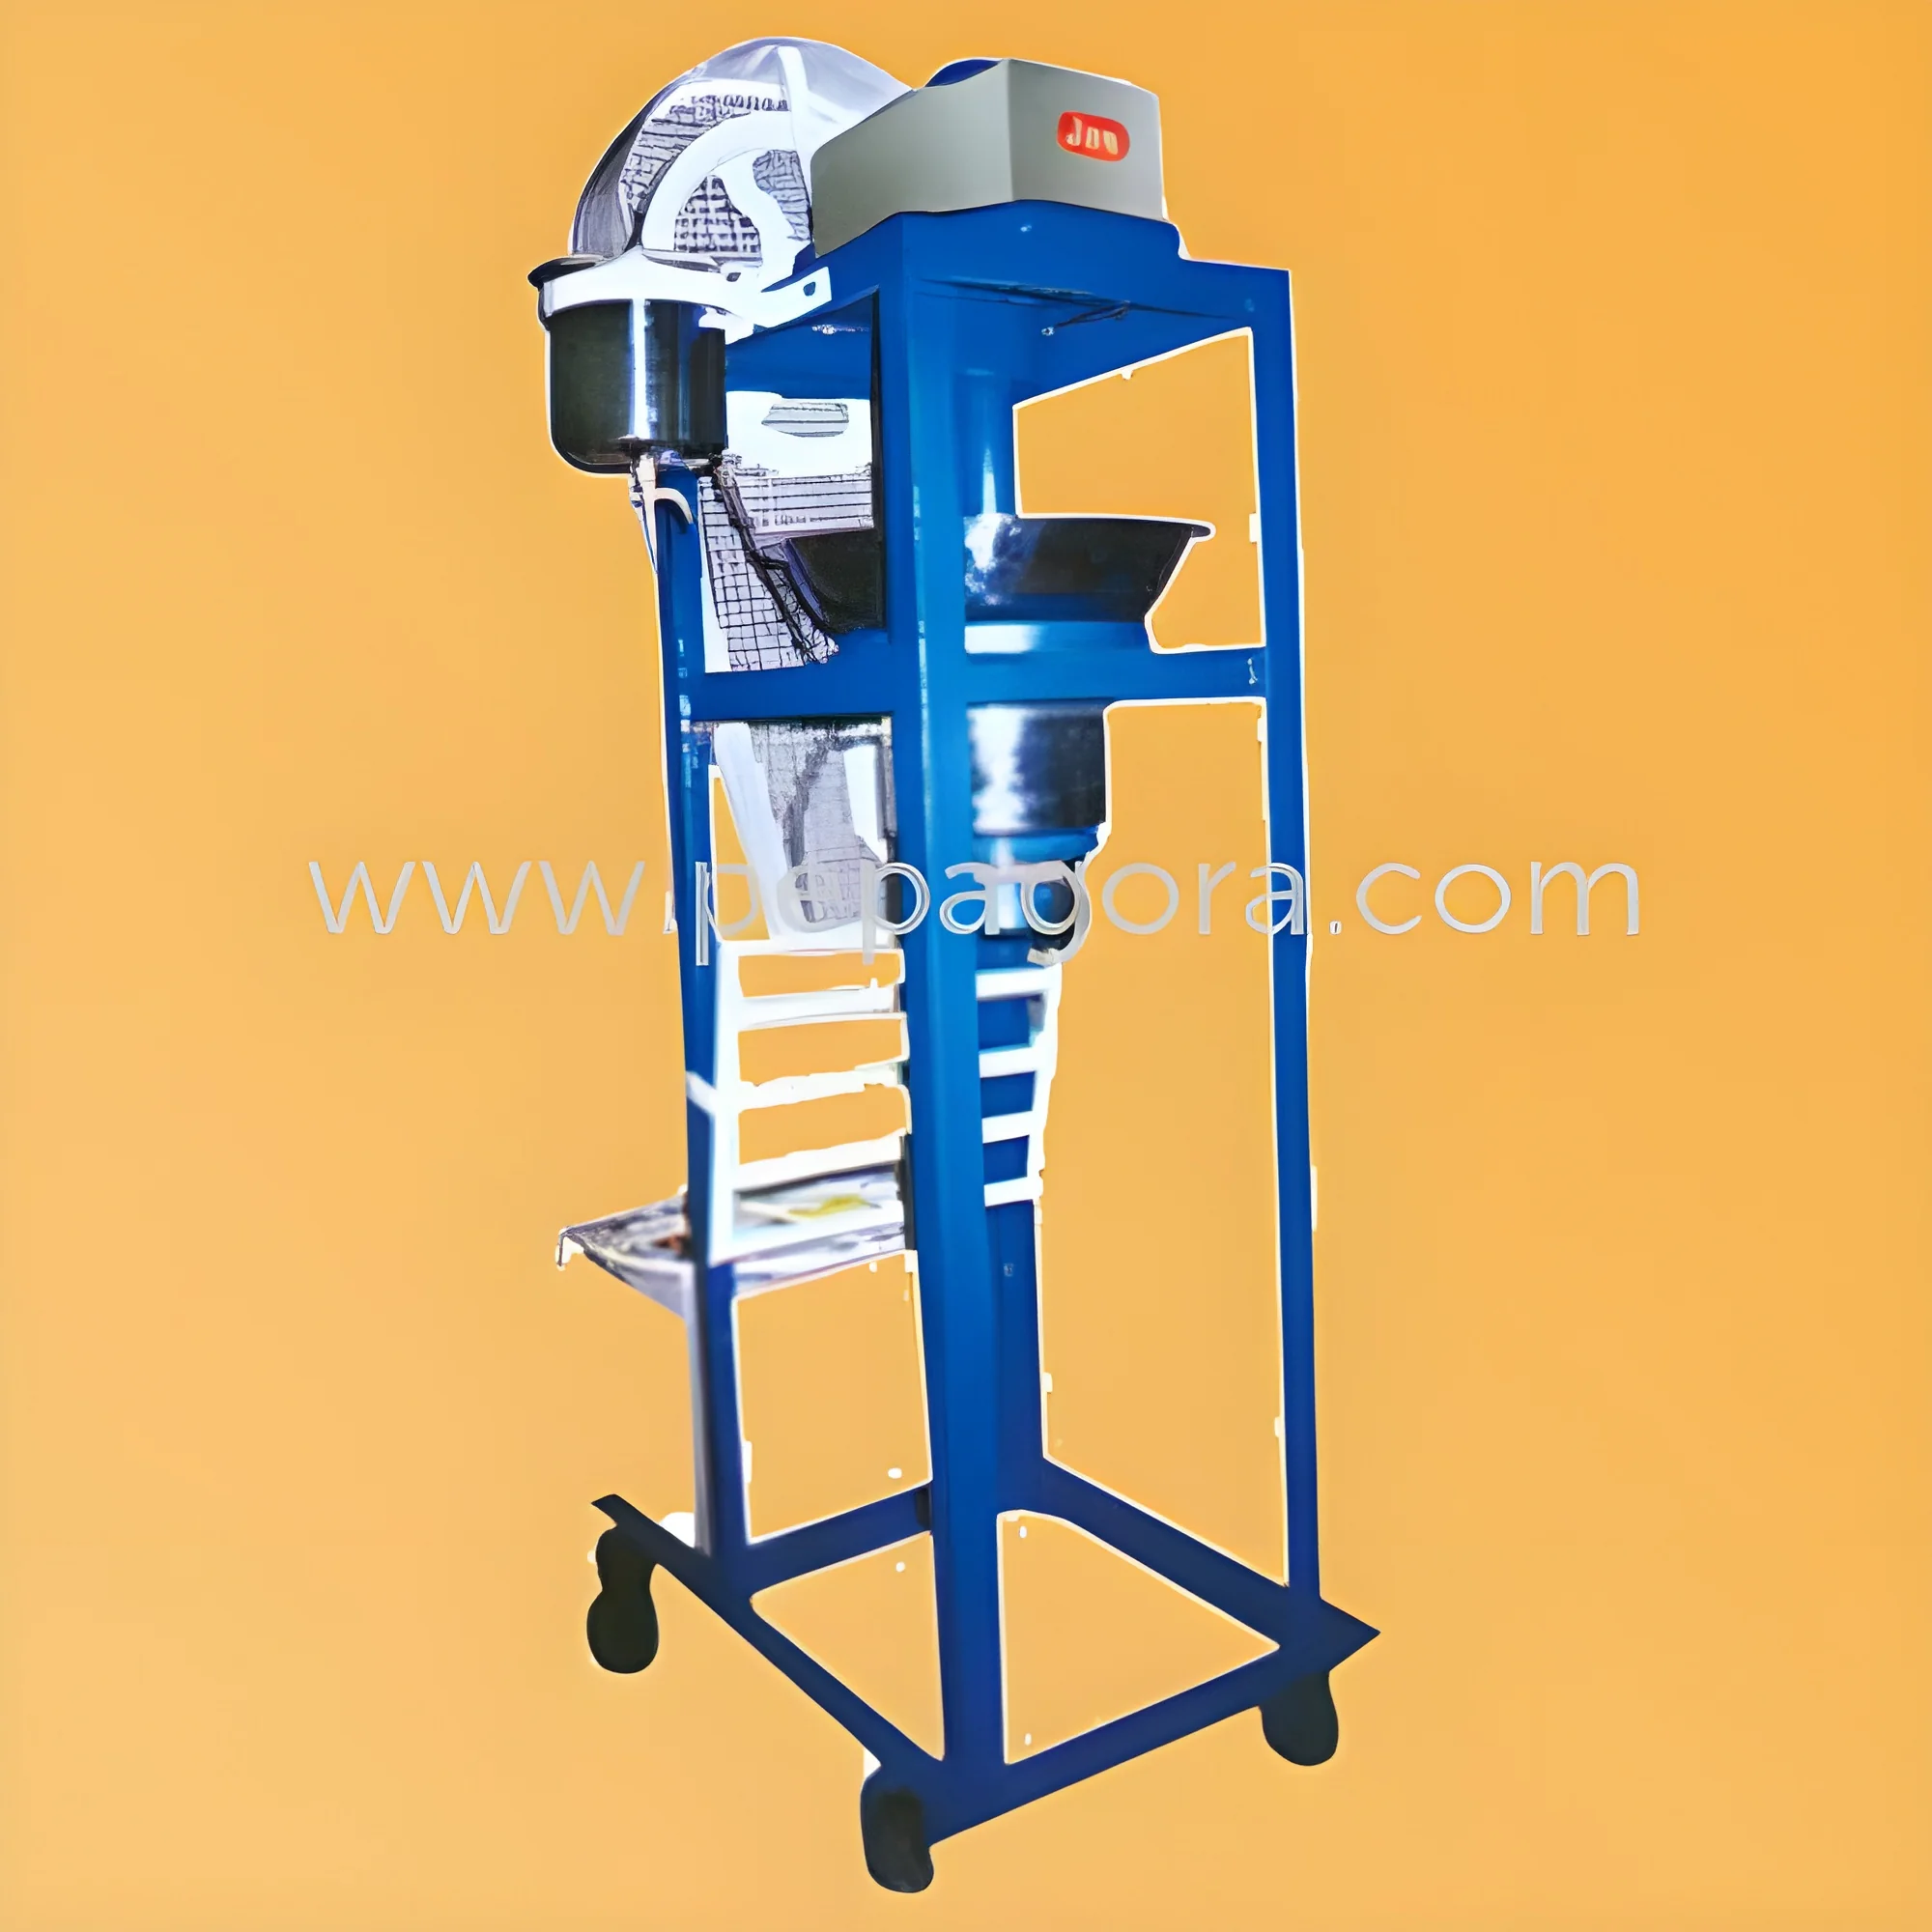
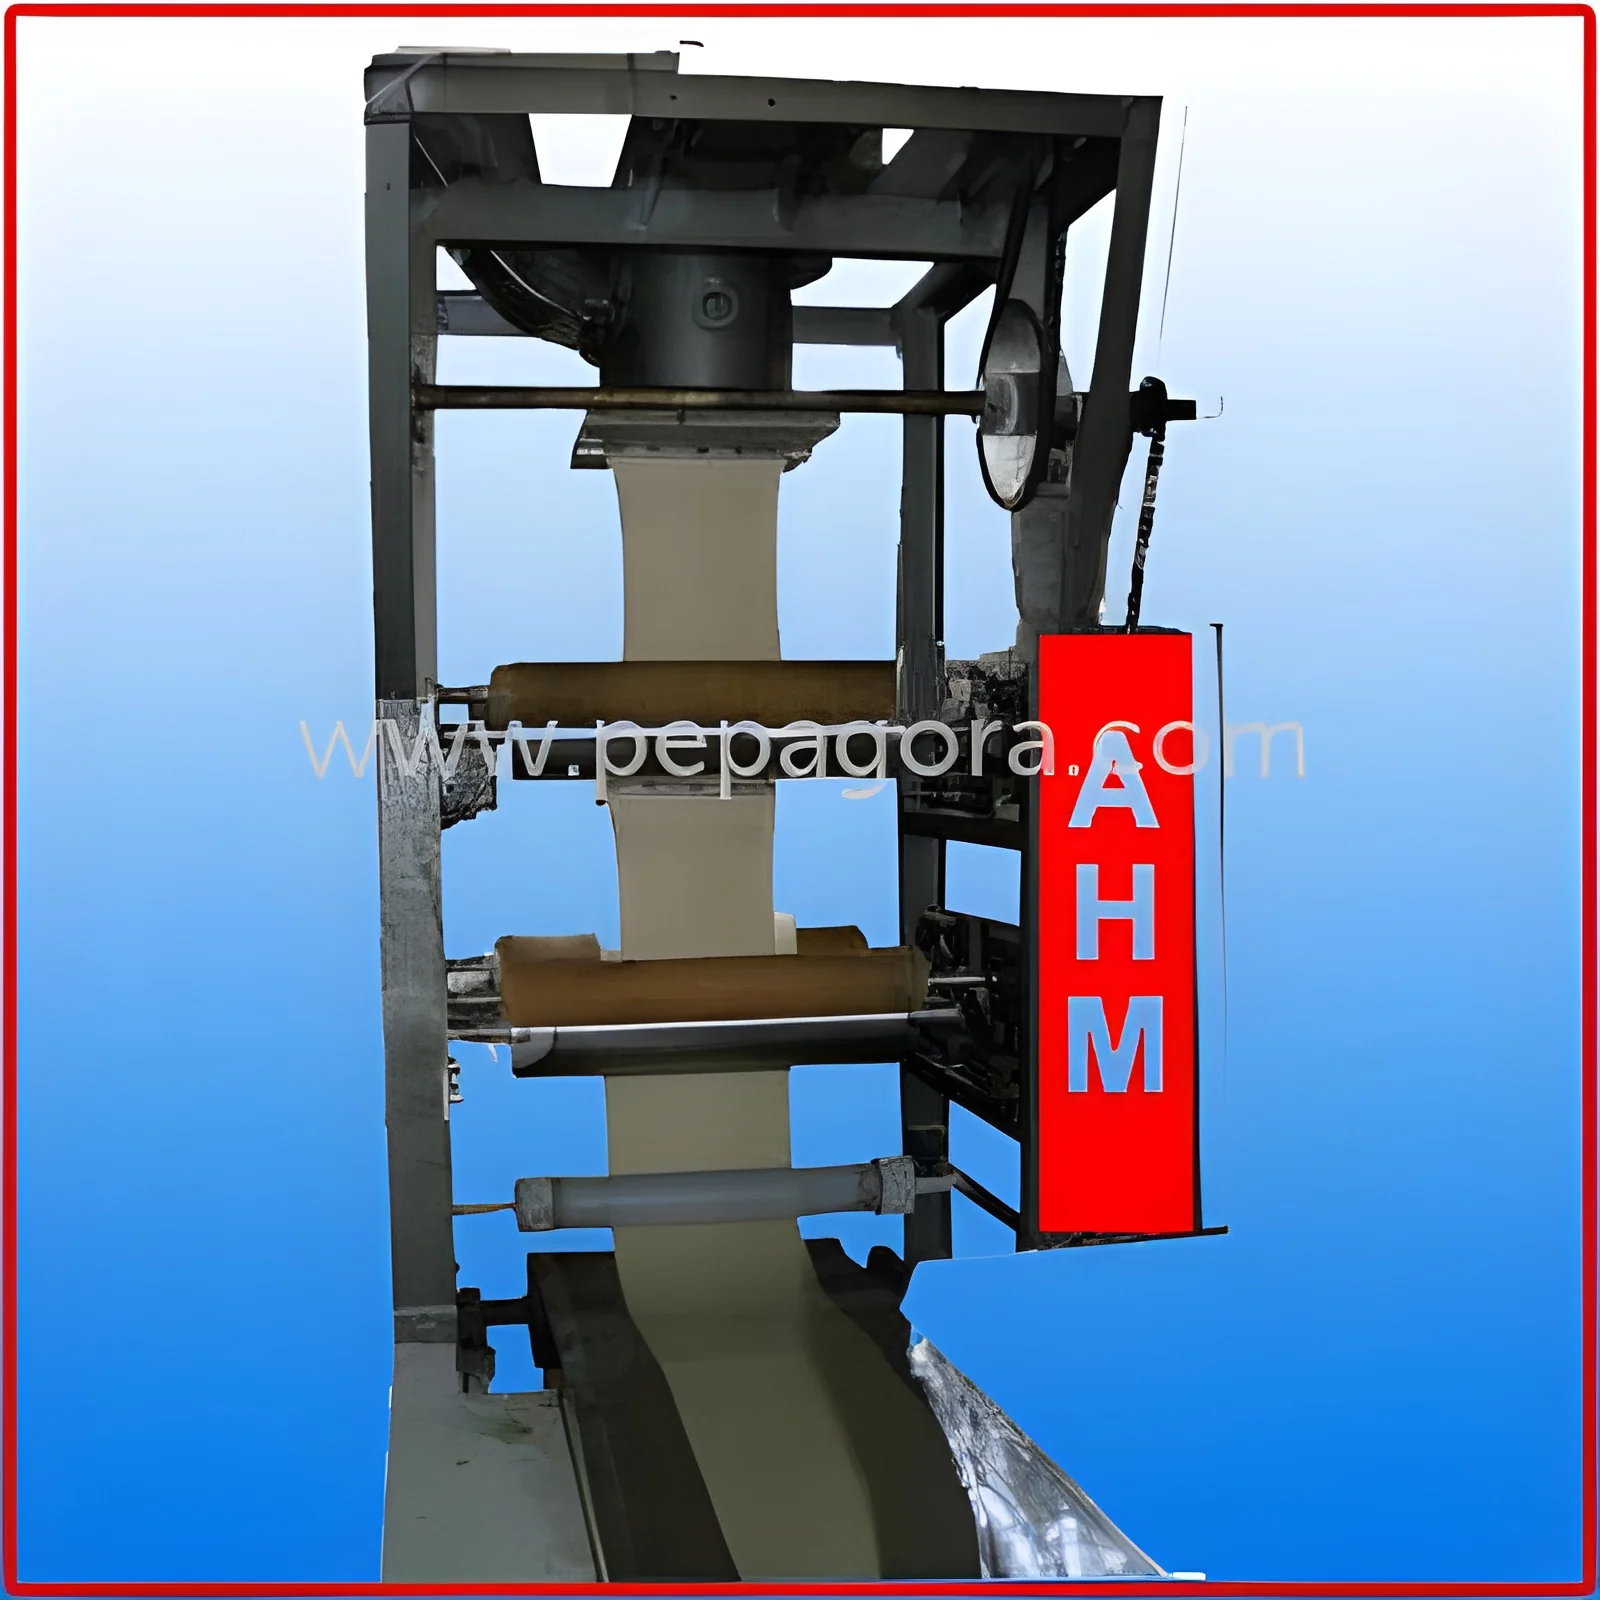
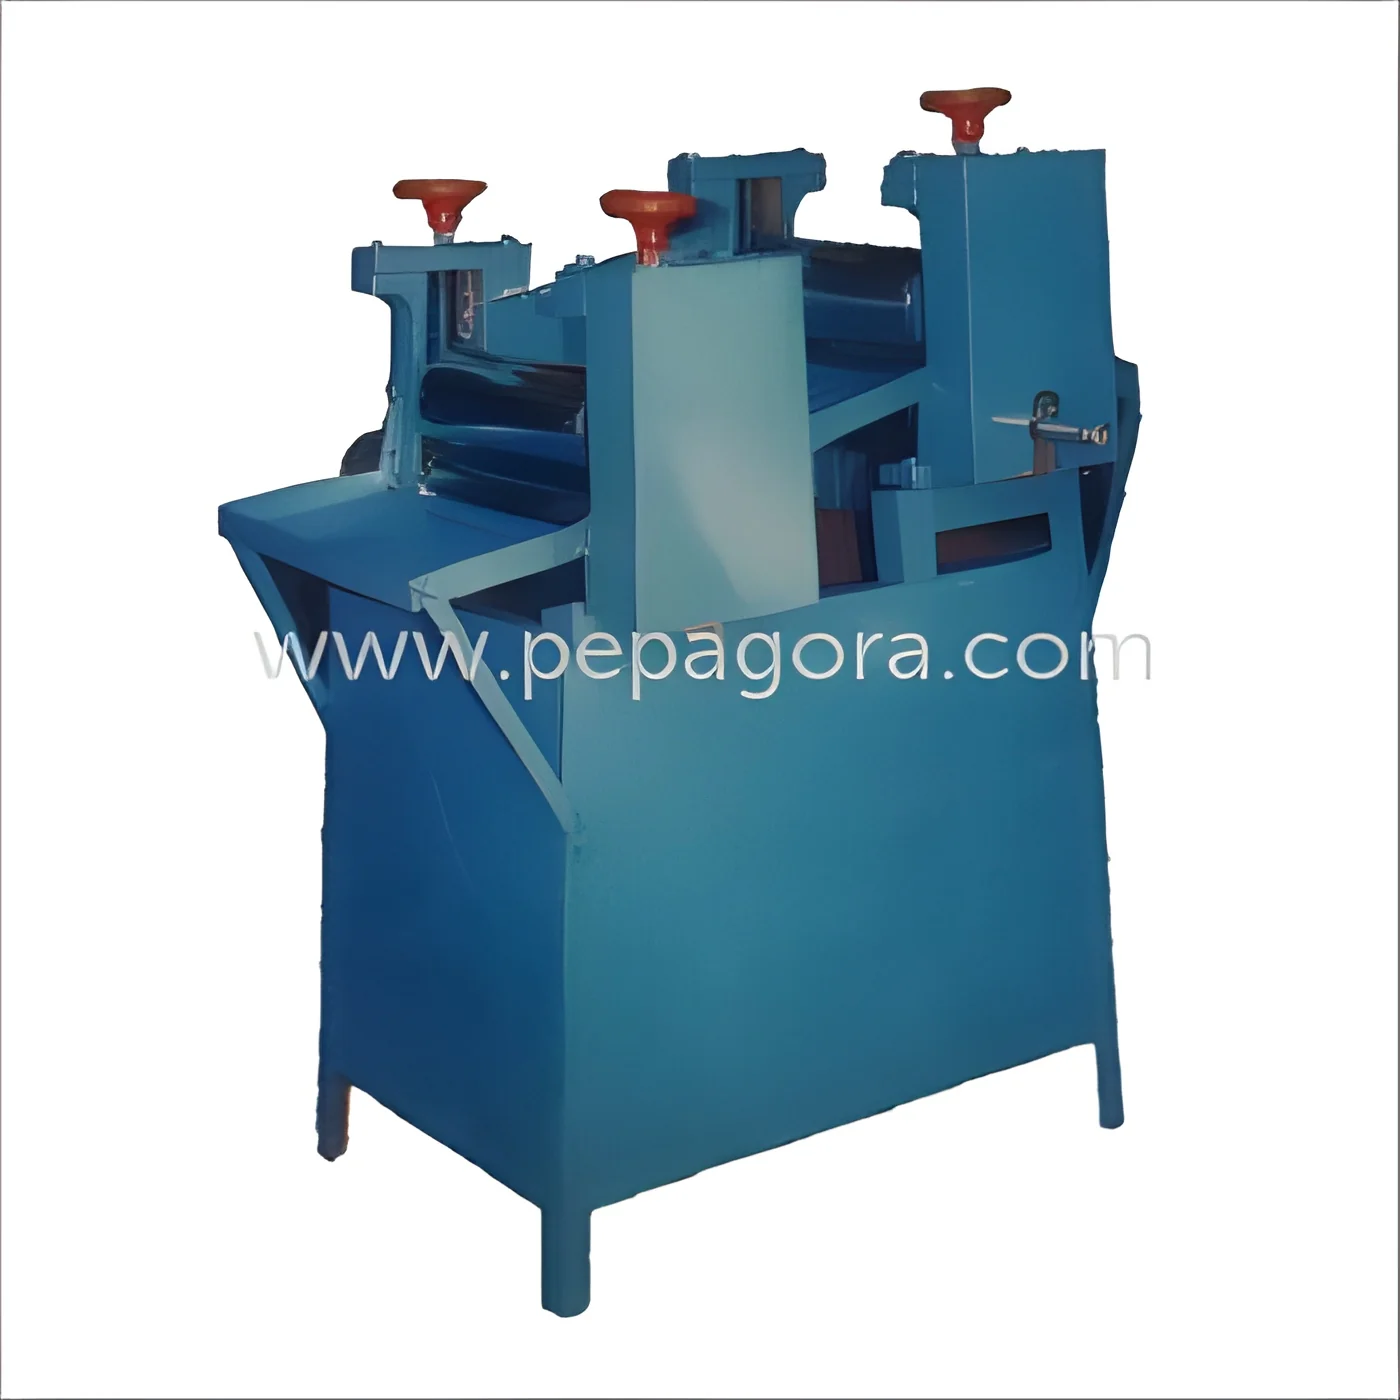
Our industrial brass screw conveyor represents a robust and reliable solution for material handling challenges across various sectors. It features a core construction of fire-resistant stainless steel, ensuring enhanced safety in environments where heat or spark resistance is crucial. The integration of brass components adds to its durability and corrosion resistance, making it suitable for handling a diverse range of materials from food-grade products to industrial chemicals. This conveyor is designed for efficiency and low maintenance, providing a consistent and reliable method to move granular, powdered, and semi-solid materials horizontally or on an incline. Its sturdy build and thoughtful engineering focus on delivering uninterrupted operation, reducing the risk of downtime and ensuring a smooth flow within your production or processing line.

This conveyor serves as a vital asset in industries where precise and sanitary material transfer is non-negotiable. In the food and beverag...
Our industrial brass screw conveyor represents a robust and reliable solution for material handling challenges across various sectors. It features a core construction of fire-resistant stainless steel, ensuring enhanced safety in environments where heat or spark resistance is crucial. The integration of brass components adds to its durability and corrosion resistance, making it suitable for handling a diverse range of materials from food-grade products to industrial chemicals. This conveyor is designed for efficiency and low maintenance, providing a consistent and reliable method to move granular, powdered, and semi-solid materials horizontally or on an incline. Its sturdy build and thoughtful engineering focus on delivering uninterrupted operation, reducing the risk of downtime and ensuring a smooth flow within your production or processing line.

This conveyor serves as a vital asset in industries where precise and sanitary material transfer is non-negotiable. In the food and beverage sector, it is used for hygienic transportation of ingredients, ensuring compliance with strict safety standards. Chemical and pharmaceutical manufacturers rely on its corrosion-resistant and fire-resistant properties to handle sensitive powders and compounds safely. Within agriculture, it facilitates the efficient movement of grains and animal feed. Furthermore, its durable construction makes it applicable in general manufacturing and material recovery facilities for handling abrasive or recycled materials, proving its versatility and strength in demanding operational settings.

The inherent business value of this screw conveyor lies in its combination of reliability, safety, and operational cost-efficiency. By investing in this equipment, you secure a durable asset that minimizes unplanned maintenance and reduces long-term operational expenses. The fire-resistant and corrosion-resistant design directly translates to enhanced workplace safety and prolonged equipment life, even in challenging environments. This reliability ensures consistent productivity, safeguards your material quality, and provides a solid return on investment through reduced downtime and lower total cost of ownership, making it a prudent choice for serious operational upgrades.

Key Features:
- Constructed with fire-resistant stainless steel for improved operational safety.
- Incorporates durable brass components for enhanced corrosion resistance.
- Engineered as a belt conveyor structure for efficient material transport.
- Designed for handling granular, powdered, and semi-solid materials reliably.
- Built with a focus on durability and low-maintenance operation for continuous use.

Benefits:
- Enhances workplace safety with fire-resistant construction suitable for various industrial settings.
- Provides long-term reliability and reduces replacement costs through corrosion-resistant materials.
- Ensures efficient and consistent material flow, supporting uninterrupted production processes.
- Lowers operational expenses by minimizing maintenance requirements and potential downtime.
- Offers a versatile and durable solution suitable for food, chemical, agricultural, and manufacturing applications.
Specifications
| Key Attributes | |
|---|---|
| Material | Stainless Steel |
| Material Feature | Fire Resistant |
| Structure | Belt Conveyor |
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
This brass screw conveyor is engineered for the precise and reliable handling of granular, powdered, and semi-solid materials across continuous industrial operations. Its robust stainless steel construction, combined with fire-resistant properties, ensures safe and consistent performance in environments where hygiene, corrosion resistance, and operational safety are critical priorities. The conveyor's design minimizes material spillage and contamination risks, making it a dependable component for production lines that demand uninterrupted material flow and strict adherence to quality standards. It is built to withstand the rigors of demanding applications, offering a reliable solution for transferring a wide range of materials from food ingredients to industrial compounds with efficiency and integrity.
Real-world applications:
- Food processing facilities for transferring ingredients like flour, sugar, and spices between processing stages.
- Chemical manufacturing plants for moving powdered reagents, compounds, and granular catalysts safely.
- Agricultural operations and grain handling facilities for transporting feed, seeds, and harvested crops.
- Pharmaceutical production lines requiring contamination-free movement of powdered raw materials and blends.
- Industrial manufacturing plants for handling abrasive materials, plastic pellets, or recycled materials in production or sorting processes.
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Shipping & Logistics
| Port of Dispatch | Madurai |
Company Profile

ADHITHYA HITECH MACHINES, Tamil Nadu
 Tamil Nadu, India
Food & Agriculture•Manufacturer•Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Main Markets
Eastern Asia
South Asia
Southeast Asia
Industrial Brass Screw Conveyor Fire Resistant Stainless Steel
Industrial brass screw conveyor with fire-resistant stainless steel construction for reliable material handling in food, chemical, and manufacturing industries. Durable, low-maintenance design ensures efficient operation for demanding applications.
Min. Order Quantity: 1 piece
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
ADHITHYA HITECH MACHINES
 Tamil Nadu, India
Food & AgricultureManufacturer