IN
₹
Apparel & Fashion
Description
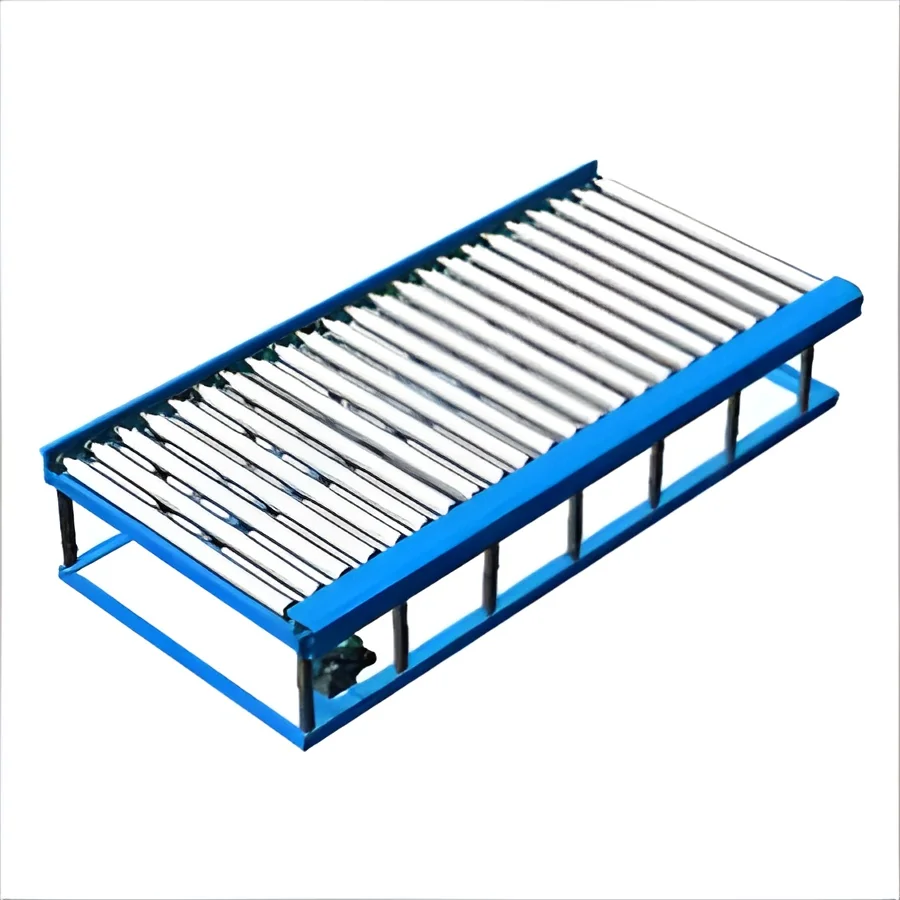
Our industrial roller conveyors represent superior material handling solutions engineered for businesses requiring reliable transportation systems. Manufactured using premium-grade materials from trusted suppliers, these conveyors deliver outstanding performance in demanding industrial settings. The robust construction ensures long service life while maintaining smooth operation for boxes, cartons, and pallets of various dimensions and weights. Each unit is precision-engineered to provide seamless integration into existing operations, offering customizable configurations to meet specific operational requirements and spatial constraints.

These roller conveyors serve essential functions across multiple industrial sectors including manufacturing, warehousing, logistics, and distribution operations. In automotive manufacturing facilities, they facilitate the movement of components along assembly lines with precision timing. Distribution centers utilize them for efficient order processing ...
Our industrial roller conveyors represent superior material handling solutions engineered for businesses requiring reliable transportation systems. Manufactured using premium-grade materials from trusted suppliers, these conveyors deliver outstanding performance in demanding industrial settings. The robust construction ensures long service life while maintaining smooth operation for boxes, cartons, and pallets of various dimensions and weights. Each unit is precision-engineered to provide seamless integration into existing operations, offering customizable configurations to meet specific operational requirements and spatial constraints.

These roller conveyors serve essential functions across multiple industrial sectors including manufacturing, warehousing, logistics, and distribution operations. In automotive manufacturing facilities, they facilitate the movement of components along assembly lines with precision timing. Distribution centers utilize them for efficient order processing and packaging operations with high throughput requirements. Food processing plants benefit from their durable construction for handling packaged goods safely, while logistics hubs employ them for parcel sorting systems that require reliability and consistent performance under continuous use conditions.

The operational value of our roller conveyors extends beyond basic material transportation—they represent a strategic investment in workflow optimization. By minimizing manual handling requirements, they significantly reduce labor costs and decrease workplace injury risks. Their dependable performance ensures consistent material flow, reducing bottlenecks and enhancing overall productivity. The low-maintenance design translates to reduced operational downtime and lower long-term costs. Businesses can expect rapid return on investment through improved efficiency, reduced product damage, and enhanced workflow optimization, making them essential components for competitive industrial operations.

Key Features:
- Constructed with high-grade materials for exceptional durability and longevity
- Customizable dimensions including length, width, and roller spacing configurations
- Robust roller design capable of handling various load capacities and sizes
- Smooth and quiet operation ensuring minimal workplace disruption
- Easy integration with existing conveyor systems and material handling equipment

Benefits:
- Enhanced material handling efficiency with reliable performance
- Reduced manual labor requirements and associated costs
- Minimal maintenance needs for lower operational expenses
- Improved workplace safety with reduced injury risks
- Flexible configurations to match specific operational requirements
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Industrial roller conveyors streamline material movement across diverse operational environments. They efficiently transport boxes, cartons, and pallets in warehouse and distribution settings with reliable performance. The straightforward design ensures smooth operation with minimal maintenance needs, making them perfect for high-volume facilities that require consistent throughput and operational reliability throughout extended work cycles.
These conveyor systems excel in manufacturing plants where they integrate seamlessly with production processes. They handle substantial loads and continuous operation while reducing manual labor and improving workflow efficiency. The adaptability of roller conveyors allows for customization to specific layout requirements and load capacities, ensuring optimal performance across various industrial applications and operational demands.
- Warehouse order picking and packing operations for distribution centers
- Loading and unloading zones in logistics facilities and freight terminals
- Assembly line integration in automotive and electronics manufacturing
- Food processing facilities for safe transport of packaged goods
- Parcel sorting centers and postal distribution operations
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Abhijeet Enterprise, Maharashtra
 Maharashtra, India
Industrial Equipment & Machinery•Manufacturer
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Industrial Roller Conveyors For Efficient Material Handling
Industrial roller conveyors provide efficient material handling for warehouses and manufacturing plants. Built with durable materials for reliable performance in demanding environments. Customizable solutions available for seamless integration.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Abhijeet Enterprise
 Maharashtra, India
Industrial Equipment & MachineryManufacturer