
 IN
₹
Apparel & Fashion
Description
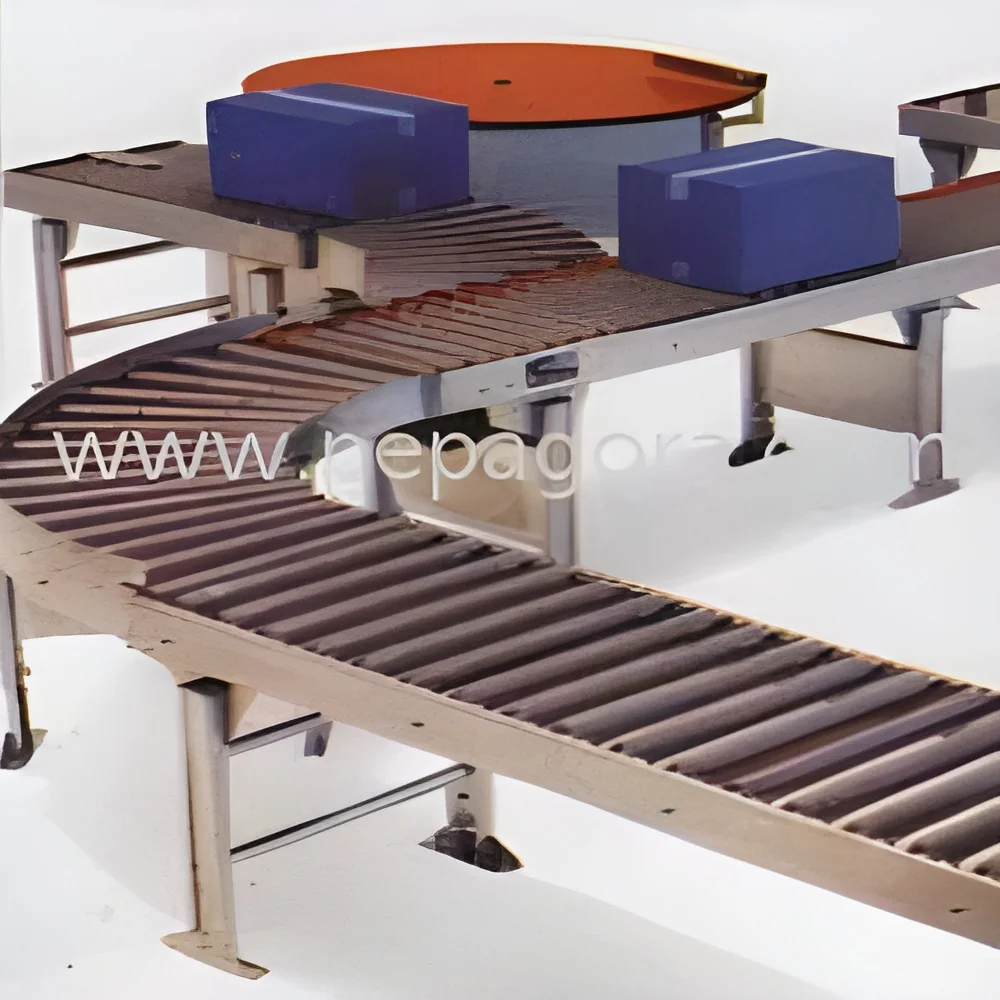
Our heavy-duty roller conveyor systems represent the foundation of efficient industrial material handling, engineered to transport products reliably through various operational processes. These robust systems feature multiple rollers mounted between durable side frames, creating a continuous surface that supports and moves items of different sizes and weights. Available in both gravity-fed and powered configurations, our conveyors accommodate diverse operational requirements while ensuring minimal maintenance needs. The integration of quality bearings reduces mechanical resistance and guarantees long-term performance, making these systems a strategic investment for operations seeking to optimize their material flow efficiency and reliability.

These conveyor systems serve critical functions across multiple industrial sectors including manufacturing, warehousing, logistics, packaging, and distribution operations. In manufacturing environments, they facilitate the movement of raw materia...
Our heavy-duty roller conveyor systems represent the foundation of efficient industrial material handling, engineered to transport products reliably through various operational processes. These robust systems feature multiple rollers mounted between durable side frames, creating a continuous surface that supports and moves items of different sizes and weights. Available in both gravity-fed and powered configurations, our conveyors accommodate diverse operational requirements while ensuring minimal maintenance needs. The integration of quality bearings reduces mechanical resistance and guarantees long-term performance, making these systems a strategic investment for operations seeking to optimize their material flow efficiency and reliability.

These conveyor systems serve critical functions across multiple industrial sectors including manufacturing, warehousing, logistics, packaging, and distribution operations. In manufacturing environments, they facilitate the movement of raw materials and components between production stages with precision timing. Warehouses utilize them for order picking and inventory management processes, while logistics companies depend on them for package sorting and transportation efficiency. The systems prove equally valuable in automotive assembly plants, e-commerce fulfillment centers, and retail distribution facilities where consistent material handling directly impacts operational success and customer satisfaction through timely order processing.

Operations selecting our roller conveyors gain substantial value through enhanced operational efficiency, reduced labor expenses, and improved workplace safety standards. Our systems are engineered for reliability and durability, ensuring consistent performance even in the most demanding industrial environments. The robust construction minimizes downtime and maintenance costs while delivering proven return on investment through increased throughput capacity and reduced product damage. These conveyors provide tangible operational advantages that contribute directly to improved bottom-line results and long-term business sustainability in competitive markets.

Key Features:
- Heavy-duty rollers mounted between reinforced side frames for maximum durability
- Available in both gravity and powered configurations to suit specific operational needs
- Customizable lengths, widths, and roller spacing to handle various product types
- Quality bearings incorporated to minimize mechanical losses and ensure smooth operation
- Modular design allowing for easy expansion and reconfiguration as needs change

Benefits:
- Enhanced operational efficiency through streamlined material flow
- Reduced labor costs by minimizing manual handling requirements
- Improved workplace safety with automated product transportation
- Minimal product damage during transit ensuring quality preservation
- Scalable solutions that grow with your business operations
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Our heavy-duty roller conveyor systems deliver robust material handling solutions for demanding industrial environments where reliable product transportation is essential. These systems efficiently move goods between workstations, storage areas, and loading docks while minimizing manual handling. The durable construction ensures consistent performance even under continuous operation, making them ideal for high-volume facilities that require dependable material flow throughout their daily operations.
These conveyor systems handle everything from standard packages to heavy industrial components with equal efficiency. The versatility allows seamless integration with existing material handling equipment, creating comprehensive logistics solutions that optimize workflow. Businesses achieve significant operational improvements including reduced labor requirements, minimized product damage, and enhanced throughput capacity. The modular design accommodates future expansion and reconfiguration as operational needs evolve over time.
- Warehouse order fulfillment systems moving packages to shipping areas
- Manufacturing assembly lines transporting components between workstations
- Distribution centers sorting and routing packages efficiently
- Loading docks transferring goods between trucks and storage facilities
- Packaging facilities moving finished products to palletizing stations
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Canara Engineers Pvt Ltd, Maharashtra
 Maharashtra, India
Industrial Equipment & Machinery•Manufacturer•Distributor / Wholesaler
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Warehouse Roller Conveyors Heavy Duty Material Handling Systems
Heavy duty warehouse roller conveyors provide reliable material handling for distribution centers and manufacturing facilities with customizable rollers and sturdy frames for efficient product movement.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Canara Engineers Pvt Ltd
 Maharashtra, India
Industrial Equipment & MachineryManufacturer


