IN
₹
Apparel & Fashion
Description
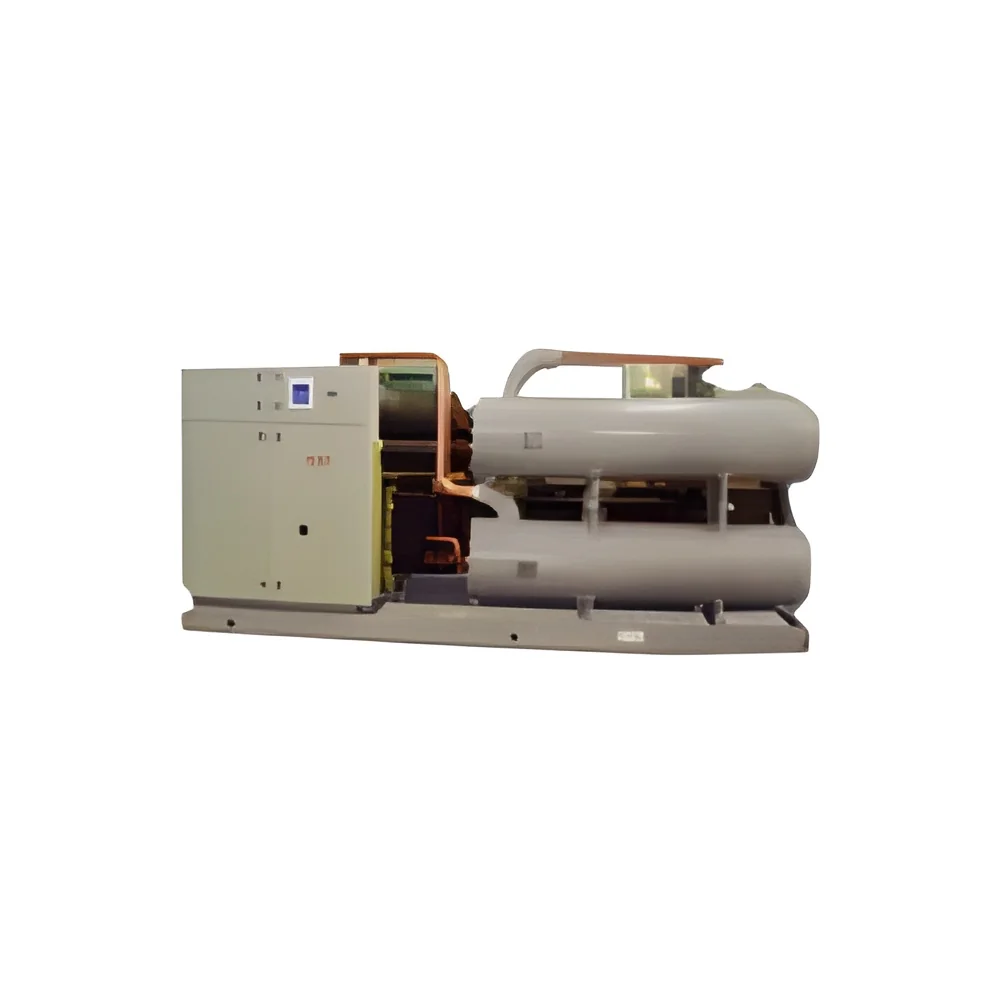
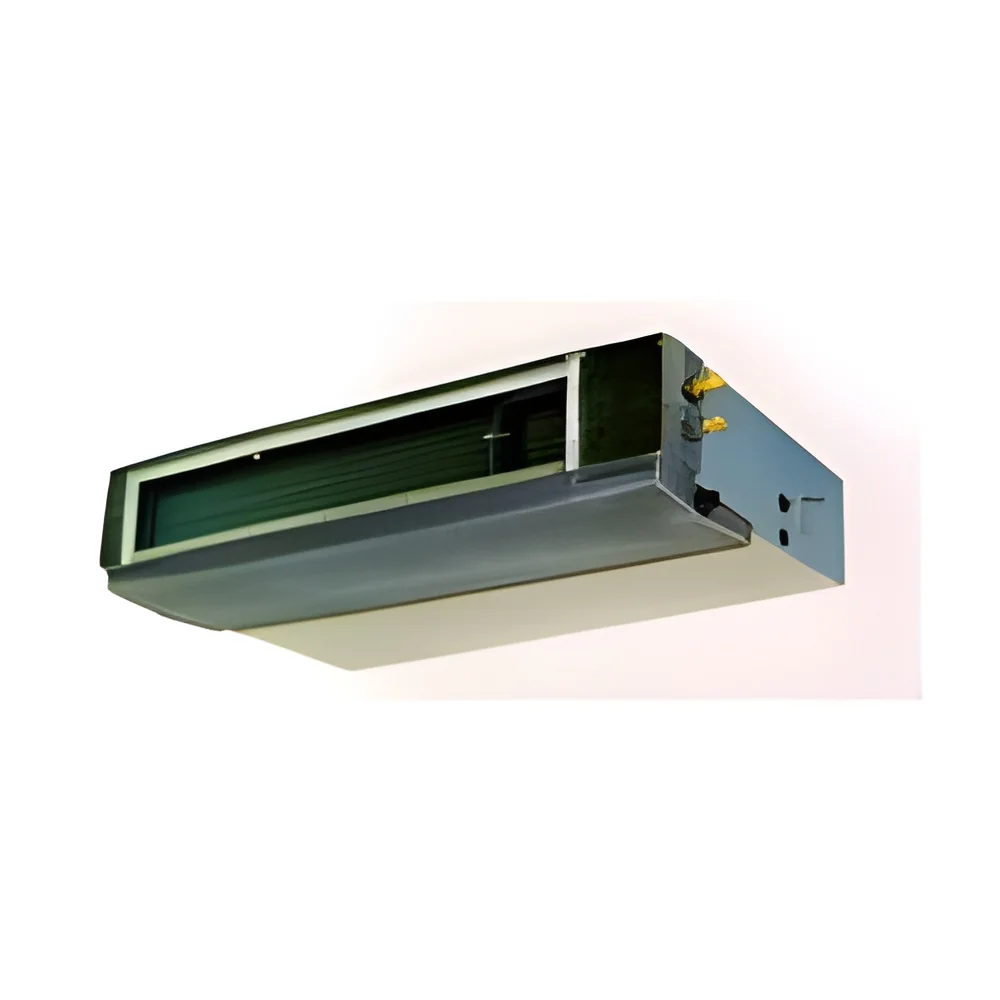
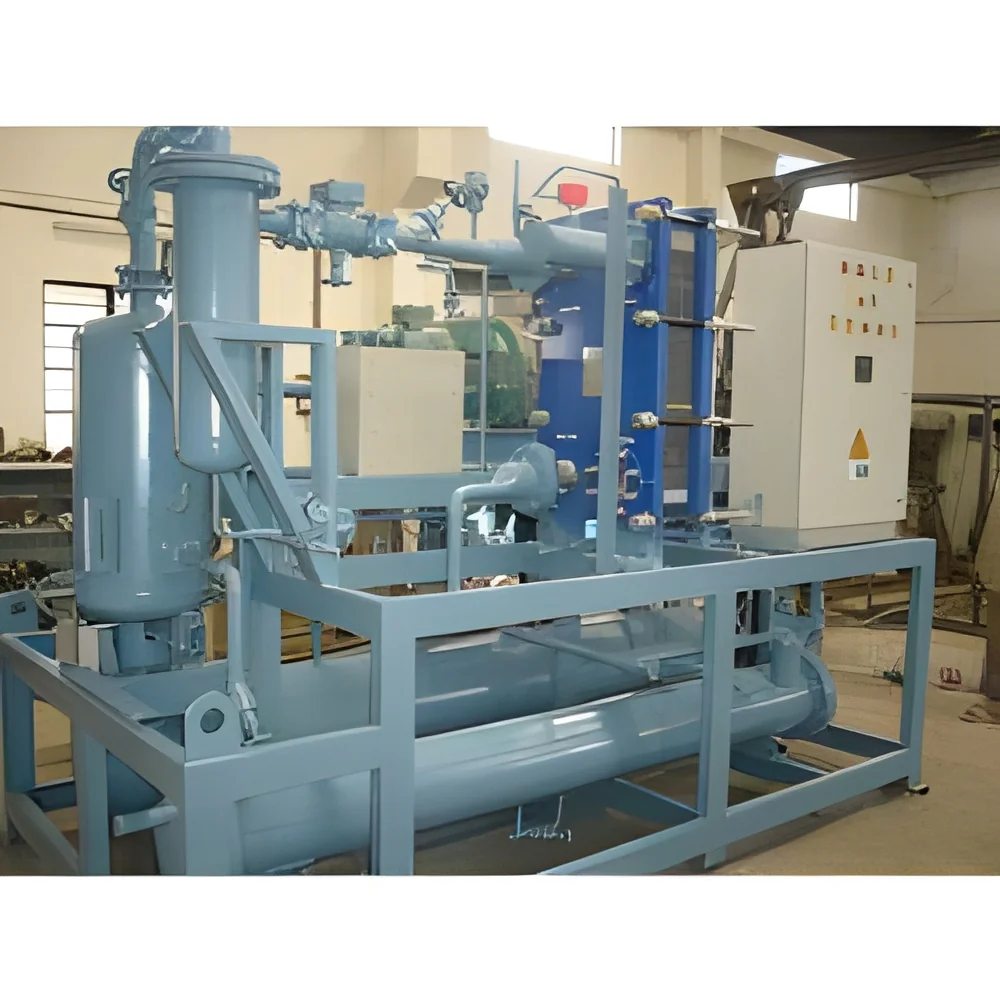
Industrial refrigeration systems represent advanced cooling technology engineered for commercial and industrial applications where temperature reliability is essential. These systems incorporate high-performance compressors, energy-efficient condensers, and precision temperature controls to maintain optimal conditions for sensitive products and manufacturing processes. Built with durable components and designed for continuous operation, they deliver consistent cooling performance even in demanding environments while reducing operational costs through intelligent energy management systems. The robust construction ensures long-term reliability and minimal maintenance requirements, making them ideal for critical cooling applications across multiple industries.

These refrigeration solutions serve vital functions throughout the food processing industry, pharmaceutical manufacturing sector, chemical production facilities, and large-scale cold storage logistics operations. In food processing...
Industrial refrigeration systems represent advanced cooling technology engineered for commercial and industrial applications where temperature reliability is essential. These systems incorporate high-performance compressors, energy-efficient condensers, and precision temperature controls to maintain optimal conditions for sensitive products and manufacturing processes. Built with durable components and designed for continuous operation, they deliver consistent cooling performance even in demanding environments while reducing operational costs through intelligent energy management systems. The robust construction ensures long-term reliability and minimal maintenance requirements, making them ideal for critical cooling applications across multiple industries.

These refrigeration solutions serve vital functions throughout the food processing industry, pharmaceutical manufacturing sector, chemical production facilities, and large-scale cold storage logistics operations. In food processing plants, they ensure proper preservation from initial production stages through final distribution, maintaining product quality and safety. Pharmaceutical manufacturers rely on these systems for temperature-sensitive storage that complies with strict regulatory standards and quality control requirements. Manufacturing facilities utilize them for process cooling needs while logistics companies depend on their consistent performance for maintaining cold chain integrity during storage and transportation operations.

The operational value of these refrigeration systems lies in their proven reliability, reduced maintenance requirements, and long-term efficiency. Engineered to minimize downtime through robust construction and accessible service components, they ensure continuous operation that protects valuable inventory and manufacturing processes. The systems are designed with operational flexibility to match specific capacity requirements and workflow demands, resulting in improved productivity and reduced total cost of ownership. Their energy-efficient performance translates to significant operational savings while maintaining the precise temperature control necessary for sensitive applications.

Key Features:
- High-performance compressor technology for reliable cooling operation
- Precision temperature control systems with digital monitoring capabilities
- Corrosion-resistant construction materials for extended durability
- Scalable capacity options suitable for various industrial requirements
- Integrated energy management systems for operational efficiency

Benefits:
- Consistent temperature maintenance for product quality preservation
- Reduced energy consumption through efficient cooling technology
- Minimal maintenance requirements with durable component construction
- Reliable performance in demanding industrial environments
- Compliance with industry standards for safety and quality assurance
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Industrial refrigeration systems deliver consistent cooling performance for perishable goods storage and climate-sensitive operations. These robust solutions maintain precise temperature control in demanding environments while ensuring energy efficiency and operational reliability across various industrial settings. They handle high-capacity requirements for food preservation, pharmaceutical storage, and manufacturing processes with uncompromising temperature stability and compliance with industry standards.
These refrigeration units serve critical roles in food processing facilities, pharmaceutical storage warehouses, chemical manufacturing plants, and large-scale cold storage operations. The systems provide reliable cooling for blast freezing, chilled storage, and process cooling applications while integrating seamlessly with existing infrastructure. Their durable construction withstands challenging conditions while maintaining consistent performance for temperature-sensitive products and industrial processes.
- Temperature-controlled storage for perishable foods in distribution centers
- Climate-sensitive storage for pharmaceutical products and vaccines
- Process cooling in food manufacturing and packaging facilities
- Industrial chemical processing requiring precise temperature management
- Large-scale commercial refrigeration for storage warehouses and logistics
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Chill Tech Engineers Private Limited, Tamil Nadu
 Tamil Nadu, India
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Industrial Refrigeration Systems For Food Storage And Pharmaceuticals
Industrial refrigeration systems provide reliable temperature control for food storage and pharmaceutical applications. These premium cooling solutions ensure precise climate management with durable construction and energy-efficient performance.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Chill Tech Engineers Private Limited
 Tamil Nadu, India