IN
₹
Apparel & Fashion
Description
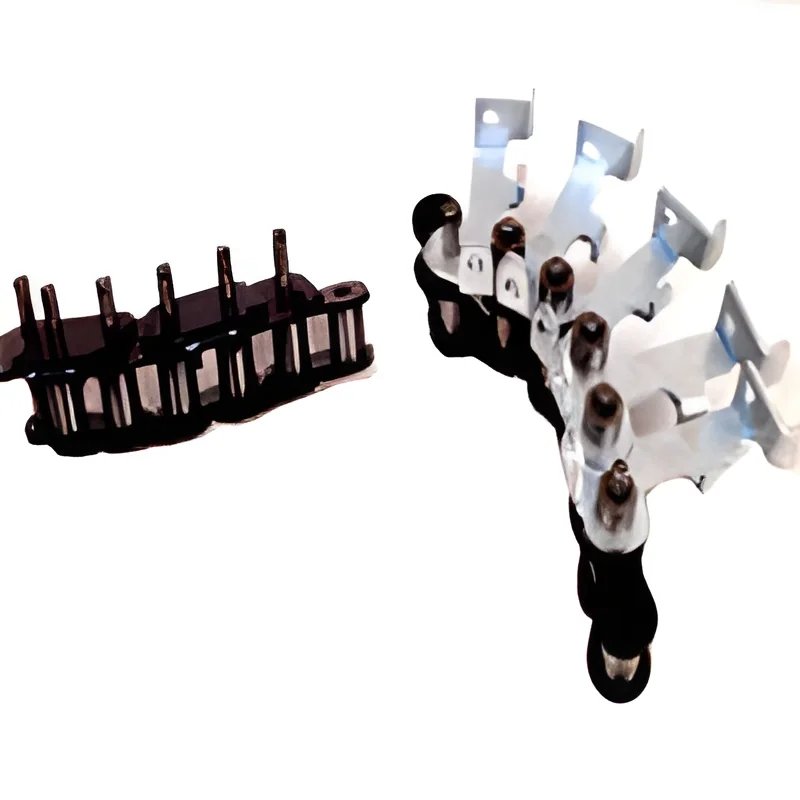
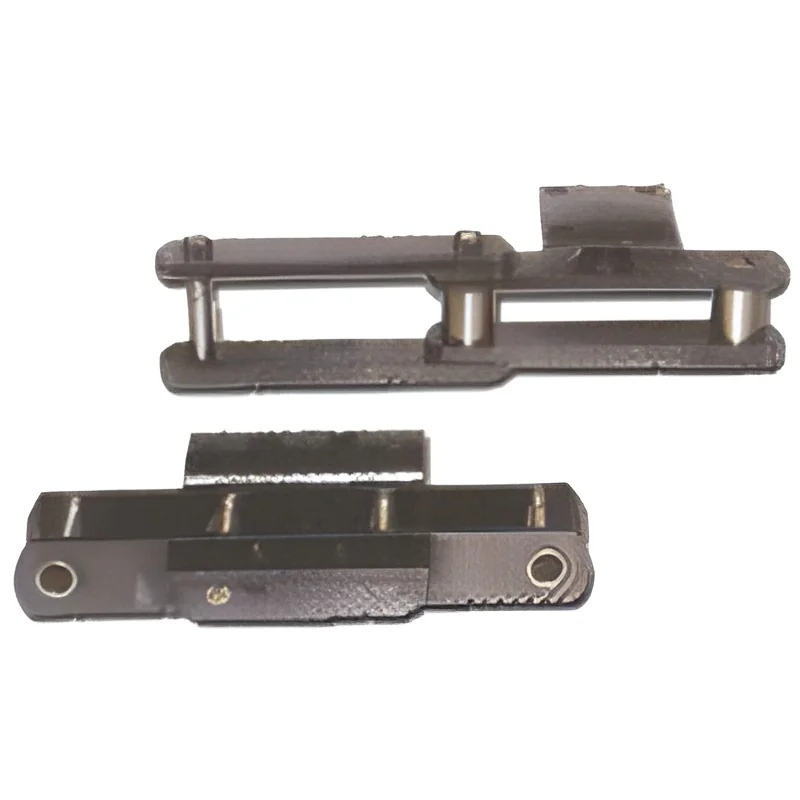
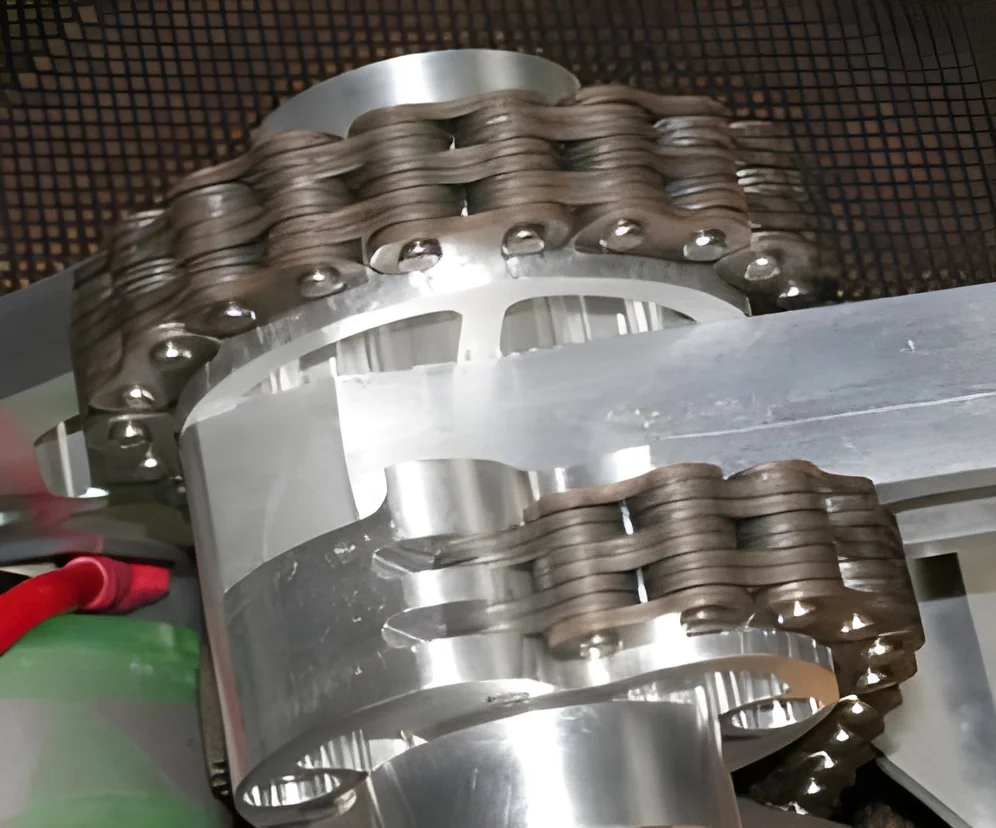
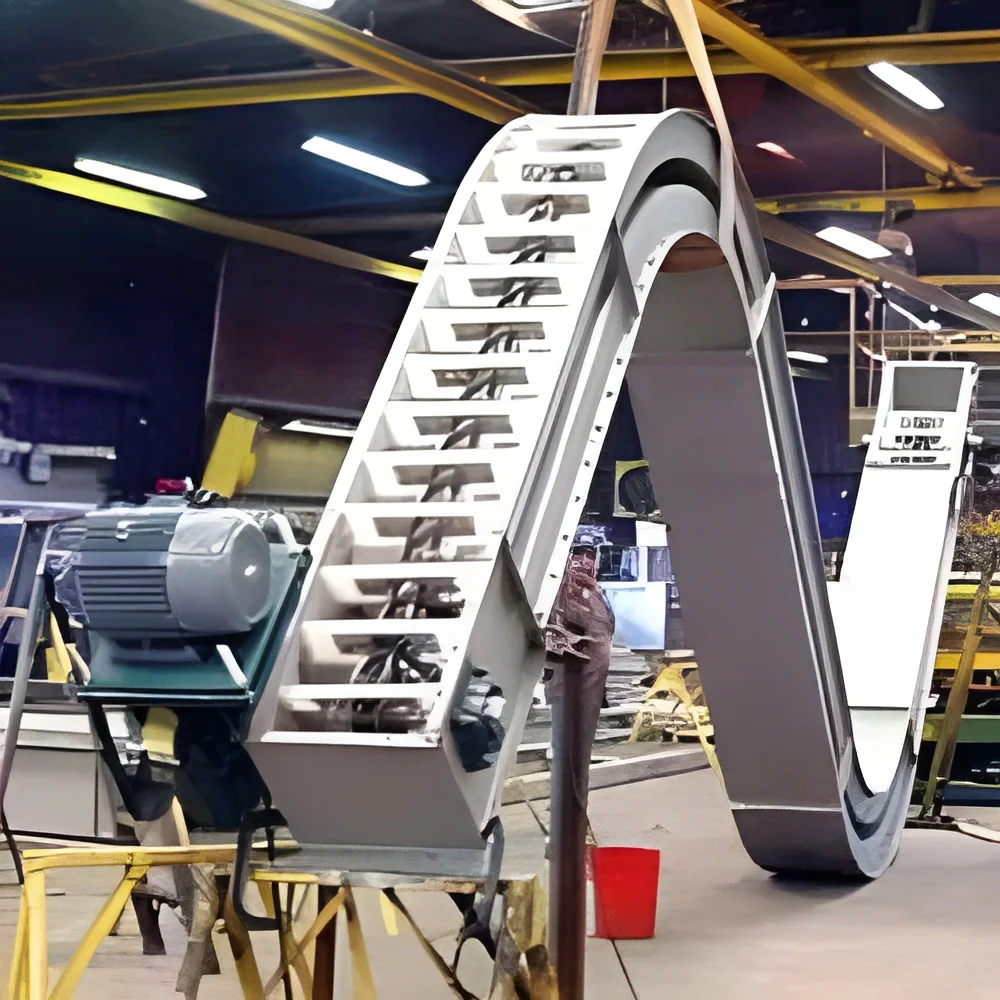
Heavy Duty Redler Conveyor Chains are engineered as premier solutions for efficient and reliable bulk material handling. These specialized chains feature a unique design with attached flights that push materials through enclosed troughs, effectively preventing spillage and contamination while ensuring a smooth, consistent material flow. Built for the most demanding applications, they handle a wide range of materials from fine powders to coarse aggregates with minimal maintenance requirements. Constructed from high-grade steel with options for various surface treatments, they offer superior resistance to wear, corrosion, and abrasion, significantly extending service life even under extreme operating conditions. The modular design facilitates straightforward installation and allows for the easy replacement of individual components, reducing system downtime and maintenance costs while ensuring continuous operation in critical processing lines.

These conveyor chains are indispensable acro...
Heavy Duty Redler Conveyor Chains are engineered as premier solutions for efficient and reliable bulk material handling. These specialized chains feature a unique design with attached flights that push materials through enclosed troughs, effectively preventing spillage and contamination while ensuring a smooth, consistent material flow. Built for the most demanding applications, they handle a wide range of materials from fine powders to coarse aggregates with minimal maintenance requirements. Constructed from high-grade steel with options for various surface treatments, they offer superior resistance to wear, corrosion, and abrasion, significantly extending service life even under extreme operating conditions. The modular design facilitates straightforward installation and allows for the easy replacement of individual components, reducing system downtime and maintenance costs while ensuring continuous operation in critical processing lines.

These conveyor chains are indispensable across multiple sectors where efficient and reliable bulk material transport is a cornerstone of operations. In agricultural processing, they handle grains, seeds, and animal feed with a gentle action that preserves product integrity. The construction and building materials industry relies on them for the consistent handling of cement, sand, and aggregates within batching plants and production facilities. Chemical manufacturing plants utilize their enclosed, dust-minimizing design for the safe transport of various powders and granules. Food processing facilities benefit from their design, which supports hygiene standards and easy cleaning for ingredients such as sugar, flour, and grains. Furthermore, mining operations deploy these heavy-duty chains for transporting ore, coal, and minerals where reliability under substantial, continuous loads is non-negotiable.

The core business value of these Heavy Duty Redler Conveyor Chains lies in their exceptional reliability, operational efficiency, and long-term cost-effectiveness. Their rugged construction drastically reduces the frequency of unexpected breakdowns and extensive maintenance, ensuring a continuous production flow and minimizing costly operational disruptions. The ability to customize key elements allows for perfect integration into existing layouts and precise matching to material characteristics, eliminating the need for expensive system overhauls. Their energy-efficient operation leads to lower power consumption compared to many alternative conveying methods, contributing to reduced operating expenses and a smaller environmental footprint. Ultimately, the extended service life and minimal upkeep requirements translate into a significantly lower total cost of ownership, representing a prudent and valuable investment for operations focused on sustained productivity and superior return on investment.

Key Features:
- Heavy-duty steel construction with optional surface treatments for enhanced durability and corrosion resistance
- Customizable flight designs and chain pitches to match specific material characteristics and flow requirements
- Enclosed trough design effectively prevents material spillage and minimizes environmental contamination
- Modular component design allows for easy part replacement, reducing maintenance downtime
- Engineered for both horizontal and inclined conveying applications within specified angles

Benefits:
- Ensures reliable, continuous operation with minimal unplanned downtime in critical processes
- Reduces long-term operational and maintenance costs through durable construction and design
- Protects material quality with gentle handling and an enclosed, contamination-free system
- Offers flexible integration into existing layouts with customizable configuration options
- Delivers a high return on investment through energy efficiency and extended service life
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Heavy Duty Redler Conveyor Chains are engineered for continuous, high-capacity bulk material handling across demanding industrial environments. Their robust design ensures efficient transportation of granular, powdered, and abrasive materials without slippage or breakdown, making them ideal for production settings where operational uptime is critical. These chains are particularly effective for applications requiring gentle material handling to prevent product degradation or segregation. With customizable flight designs and chain pitches, they adapt to specific material characteristics and spatial constraints, providing versatile solutions for horizontal and inclined conveying paths in confined spaces.
Real-world applications:
- Grain, seed, and feed handling in agricultural processing and storage facilities
- Cement, sand, and raw meal conveying in construction material manufacturing plants
- Chemical and fertilizer production lines for safe powder and granule transfer
- Food processing for dry ingredients like sugar, flour, and grains
- Mining and mineral processing for heavy-duty ore, coal, and aggregate transportation
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Asian Engineering Works, Maharashtra
 Maharashtra, India
Industrial Equipment & Machinery•Manufacturer•Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Heavy Duty Redler Conveyor Chains For Bulk Material Handling
Heavy Duty Redler Conveyor Chains for bulk material handling offer reliable, durable conveying solutions for demanding industries like agriculture, mining, and construction, ensuring smooth, efficient operations.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Asian Engineering Works
 Maharashtra, India
Industrial Equipment & MachineryManufacturer