IN
₹
Apparel & Fashion
Description
The Q2612A toner cartridge represents a significant advancement in water purification technology, designed specifically to upgrade standard candle filters into comprehensive purification systems. This high-performance component effectively removes various impurities and contaminants, ensuring consistently cleaner and safer water output. Engineered for reliability and straightforward operation, it provides businesses with a practical solution to enhance their water treatment capabilities without requiring complete system replacements. The cartridge's compatibility with existing filter setups enables seamless integration, minimizing operational disruptions and reducing implementation costs. With emphasis on quality craftsmanship and durable construction, the Q2612A delivers sustained performance that meets the rigorous demands of diverse commercial and industrial applications, making it an economically sensible choice for organizations prioritizing water purity and operational efficiency...
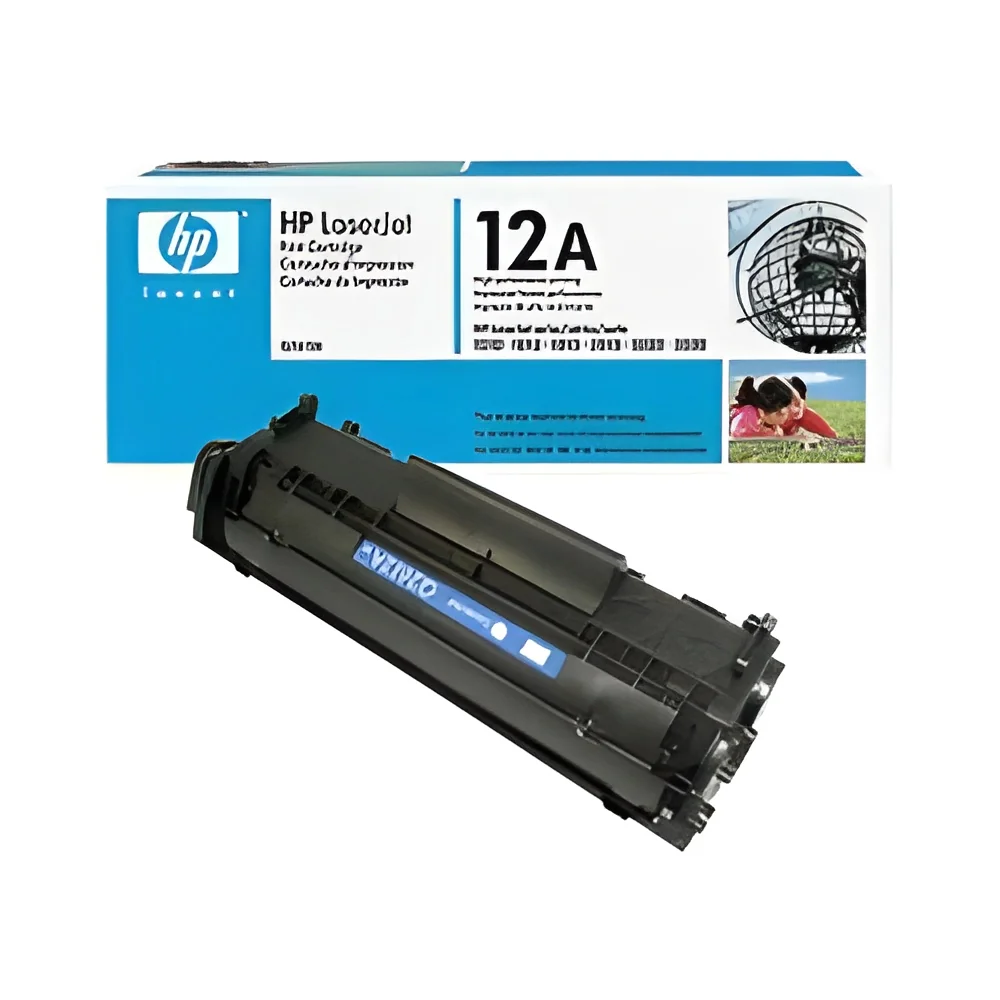
The Q2612A toner cartridge represents a significant advancement in water purification technology, designed specifically to upgrade standard candle filters into comprehensive purification systems. This high-performance component effectively removes various impurities and contaminants, ensuring consistently cleaner and safer water output. Engineered for reliability and straightforward operation, it provides businesses with a practical solution to enhance their water treatment capabilities without requiring complete system replacements. The cartridge's compatibility with existing filter setups enables seamless integration, minimizing operational disruptions and reducing implementation costs. With emphasis on quality craftsmanship and durable construction, the Q2612A delivers sustained performance that meets the rigorous demands of diverse commercial and industrial applications, making it an economically sensible choice for organizations prioritizing water purity and operational efficiency.

Multiple industries depend on the Q2612A toner cartridge where water purity directly impacts operational success and compliance. Manufacturing facilities utilize these cartridges to maintain water quality in critical processes including equipment cooling, product rinsing, and production operations, ensuring both equipment longevity and product consistency. Hospitality establishments such as hotels and restaurants rely on them to provide safe drinking water for guests and staff, enhancing customer experience while meeting health regulations. Healthcare institutions implement these cartridges to achieve sterile water standards necessary for medical procedures and equipment sterilization, supporting patient safety and infection control protocols. The food and beverage sector benefits from their purification capabilities in production processes, safeguarding product integrity and compliance with stringent safety standards. Educational institutions and commercial buildings also deploy these cartridges to ensure clean water availability for daily consumption and operational use.

Organizations select the Q2612A toner cartridge for its demonstrated value proposition, reliability, and adaptability to various operational contexts. It presents a cost-efficient method to upgrade existing water filtration infrastructure, eliminating the need for expensive complete system replacements while substantially improving water quality outcomes. The cartridge's rugged design guarantees extended service life, reducing maintenance frequency and associated operational downtime. Its standardized compatibility allows businesses to implement solutions that precisely match their specific requirements, enhancing operational flexibility and efficiency. With a foundation built on trustworthiness and consistent performance, this product enables organizations to meet regulatory mandates, safeguard their operational processes, and deliver safe water reliably. It serves as a dependable component for businesses committed to maintaining quality standards and sustainable practices in their water management protocols.

Key Features:
- Engineered to transform standard candle water filters into efficient purification systems
- Maintains compatibility with existing filtration setups for straightforward implementation
- Constructed using premium materials for enhanced durability and extended service life
- Effectively eliminates contaminants and impurities to ensure water purity
- Delivers consistent performance across various water treatment scenarios

Benefits:
- Upgrades existing filtration systems without requiring complete replacement
- Reduces implementation costs through easy integration with current setups
- Minimizes maintenance requirements through durable construction and reliable operation
- Ensures water safety and quality compliance across different applications
- Provides dependable performance that supports operational continuity and efficiency
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
The Q2612A toner cartridge transforms standard candle water filters into advanced purification systems by effectively removing contaminants and impurities. Its straightforward integration into existing setups makes it ideal for operations requiring enhanced water quality without system overhauls. The robust construction ensures dependable performance across various water treatment scenarios where purity and safety are paramount.
Manufacturing plants, hospitality venues, healthcare facilities, and food processing units benefit from this cartridge's consistent purification capabilities. It supports compliance with health standards while protecting equipment and ensuring product quality. The versatility allows deployment in both small-scale and large-scale environments, providing cost-effective water safety solutions for diverse operational needs.
- Enhancing drinking water safety in commercial office buildings and public facilities
- Purifying process water for food and beverage manufacturing to maintain quality standards
- Providing sterile water solutions for medical equipment and procedures in healthcare settings
- Treating water used in industrial cooling systems and manufacturing rinse processes
- Ensuring clean water supply for hotel and restaurant operations to meet hospitality requirements
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Avanti Stationers, Maharashtra
 Maharashtra, India
Packaging & Printing•Manufacturer•Distributor / Wholesaler•Retailer
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Water Purification Q2612A Toner Cartridge For Candle Filters
Q2612A toner cartridge upgrades standard candle water filters into efficient purification systems. This high-quality component removes impurities effectively, delivering reliable water purification for industrial and commercial applications with consistent performance.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Avanti Stationers
 Maharashtra, India
Packaging & PrintingManufacturer