IN
₹
Apparel & Fashion
Description
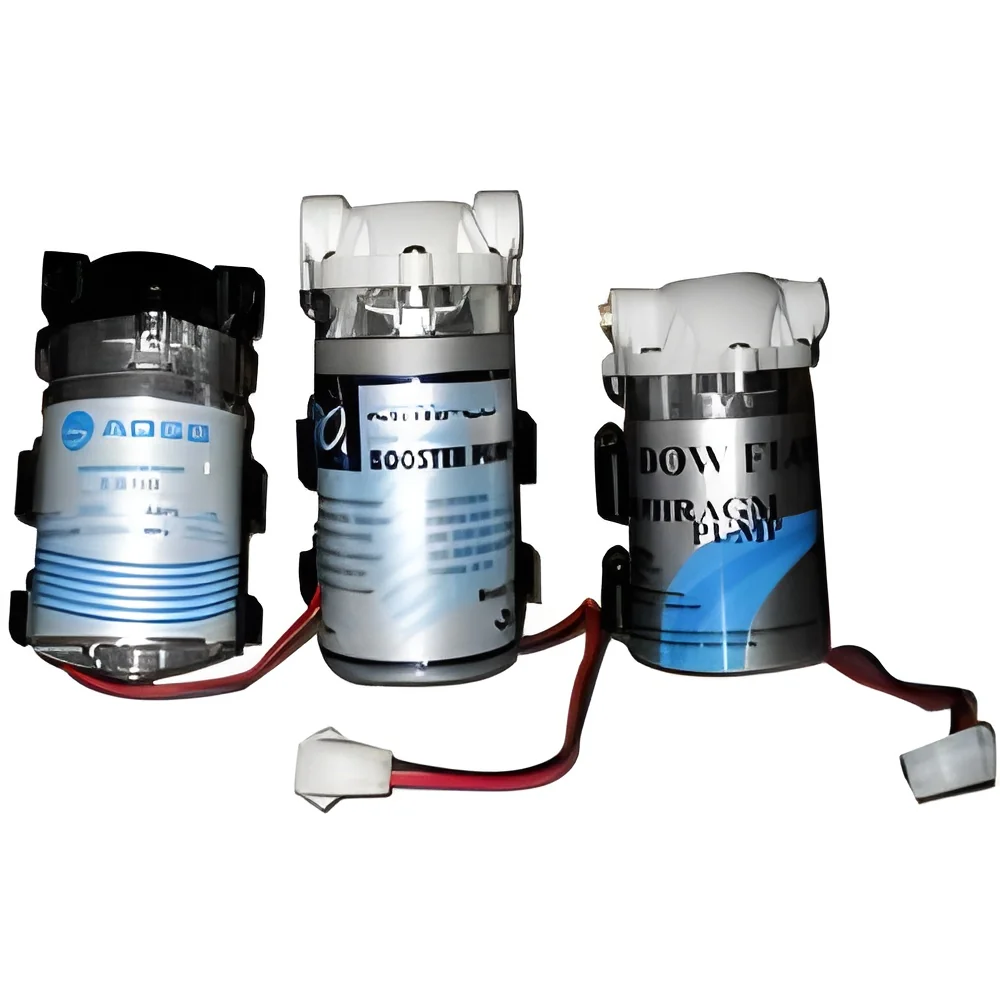
Our comprehensive range of premium pumps represents advanced fluid handling technology designed for both domestic and industrial applications. Engineered with precision and built for longevity, these pumps incorporate sophisticated features that ensure optimal performance, energy efficiency, and operational reliability. Manufactured using superior quality materials and the latest technological innovations, our products provide dependable fluid transfer capabilities that reduce downtime and maintenance costs while maximizing productivity across various pressure requirements and fluid types. Whether for standard applications or specialized needs, these pumps deliver consistent results that businesses can rely on day after day.

These versatile pumps serve diverse industries including water treatment facilities, agricultural operations, manufacturing plants, chemical processing units, and construction projects. Municipal corporations utilize them for water distribution networks and sewage...
Our comprehensive range of premium pumps represents advanced fluid handling technology designed for both domestic and industrial applications. Engineered with precision and built for longevity, these pumps incorporate sophisticated features that ensure optimal performance, energy efficiency, and operational reliability. Manufactured using superior quality materials and the latest technological innovations, our products provide dependable fluid transfer capabilities that reduce downtime and maintenance costs while maximizing productivity across various pressure requirements and fluid types. Whether for standard applications or specialized needs, these pumps deliver consistent results that businesses can rely on day after day.

These versatile pumps serve diverse industries including water treatment facilities, agricultural operations, manufacturing plants, chemical processing units, and construction projects. Municipal corporations utilize them for water distribution networks and sewage management systems, while agricultural businesses depend on them for irrigation and drainage applications. Manufacturing and processing industries employ our pumps for chemical transfer, coolant circulation, and raw material handling. The construction sector relies on them for dewatering operations and concrete pumping, demonstrating their adaptability across multiple industrial environments and operational challenges where dependable fluid movement is essential.

Businesses choose our pumps for their exceptional reliability, consistent performance, and long-term value. The products are engineered to withstand demanding operating conditions while maintaining precise fluid control, enhanced durability, and operational safety. This reliability translates to reduced total cost of ownership through lower energy consumption and minimal maintenance requirements. Each pump is designed with the end-user in mind, providing solutions that meet specific operational needs without compromise, ensuring that your fluid handling systems operate smoothly and efficiently for years to come.

Key Features:
- Advanced engineering technology for superior performance across applications
- Robust construction using high-quality, durable materials
- Designed for both domestic water supply and industrial chemical transfer
- Precision engineering ensures consistent operation under varying pressures
- Energy-efficient design reduces operational costs

Benefits:
- Reliable performance minimizes downtime and maintenance requirements
- Versatile application across multiple industries and fluid types
- Long service life reduces replacement frequency and costs
- Energy-efficient operation lowers electricity consumption
- Consistent fluid handling ensures process stability and quality
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Our high-performance pumps serve critical roles in domestic water supply systems, agricultural irrigation networks, and commercial building services. They ensure efficient fluid transfer in residential complexes, farms, and HVAC installations with consistent reliability and minimal maintenance requirements. These units handle continuous operation across varied pressure conditions, making them ideal for both small-scale and medium-scale fluid management needs across multiple environments and applications.
Industrial sectors depend on our pumps for demanding processes including chemical transfer, wastewater management, fuel handling, and manufacturing operations. Built to handle aggressive fluids, high temperatures, and corrosive environments found in factories and processing plants, their robust construction meets rigorous demands across pharmaceuticals, food processing, construction, and municipal water treatment facilities. These pumps deliver consistent performance where reliability matters most.
- Water supply and pressure boosting in residential and commercial buildings
- Agricultural irrigation and drainage systems for farms and greenhouses
- Chemical transfer and processing in pharmaceutical and manufacturing plants
- Wastewater and sewage management in municipal and industrial treatment facilities
- Fuel transfer and circulation systems in automotive and marine industries
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Bharat Lubricants, New Delhi
 New Delhi, India
Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
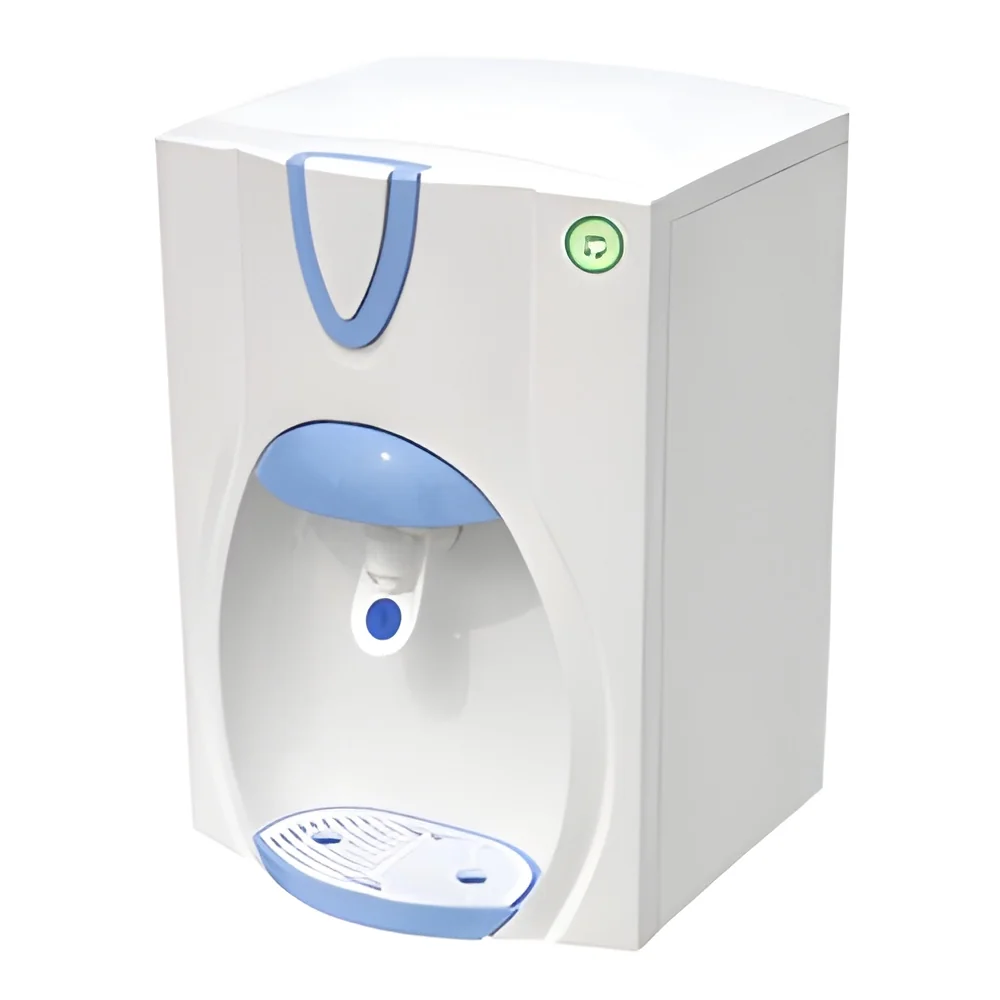
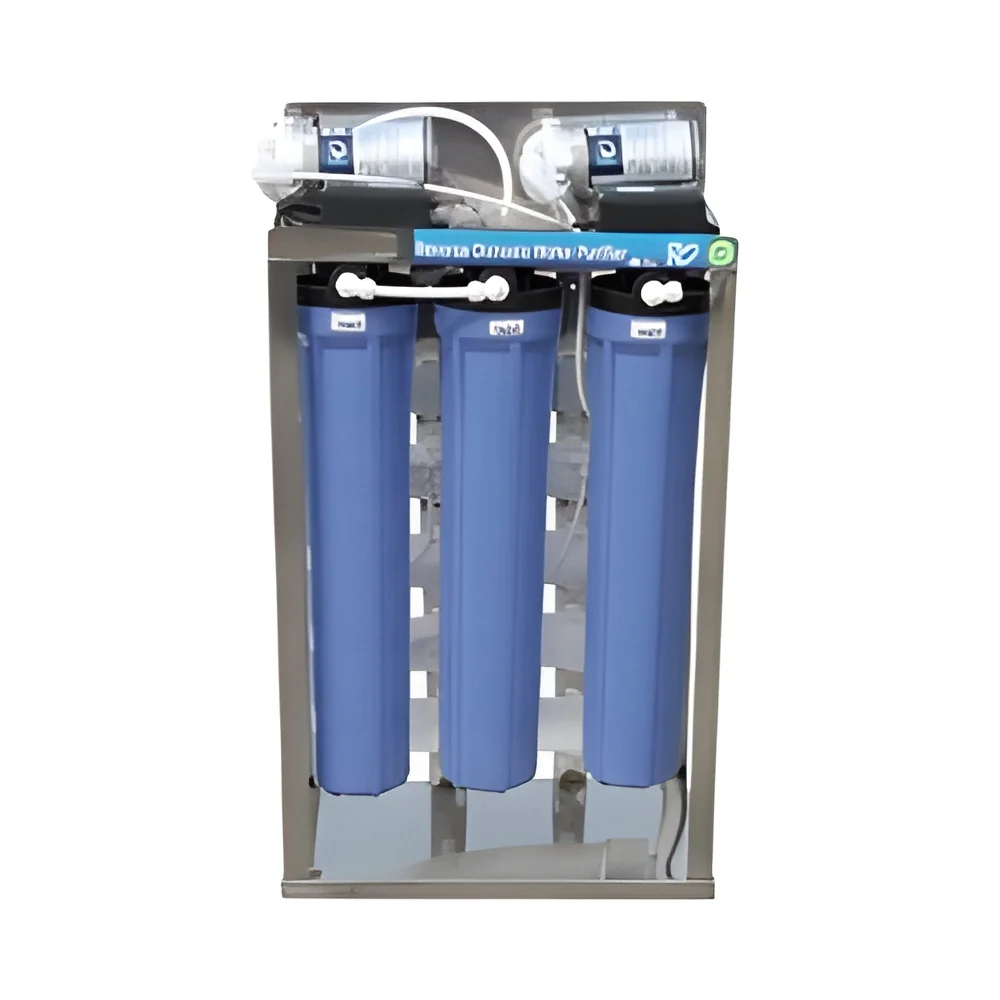
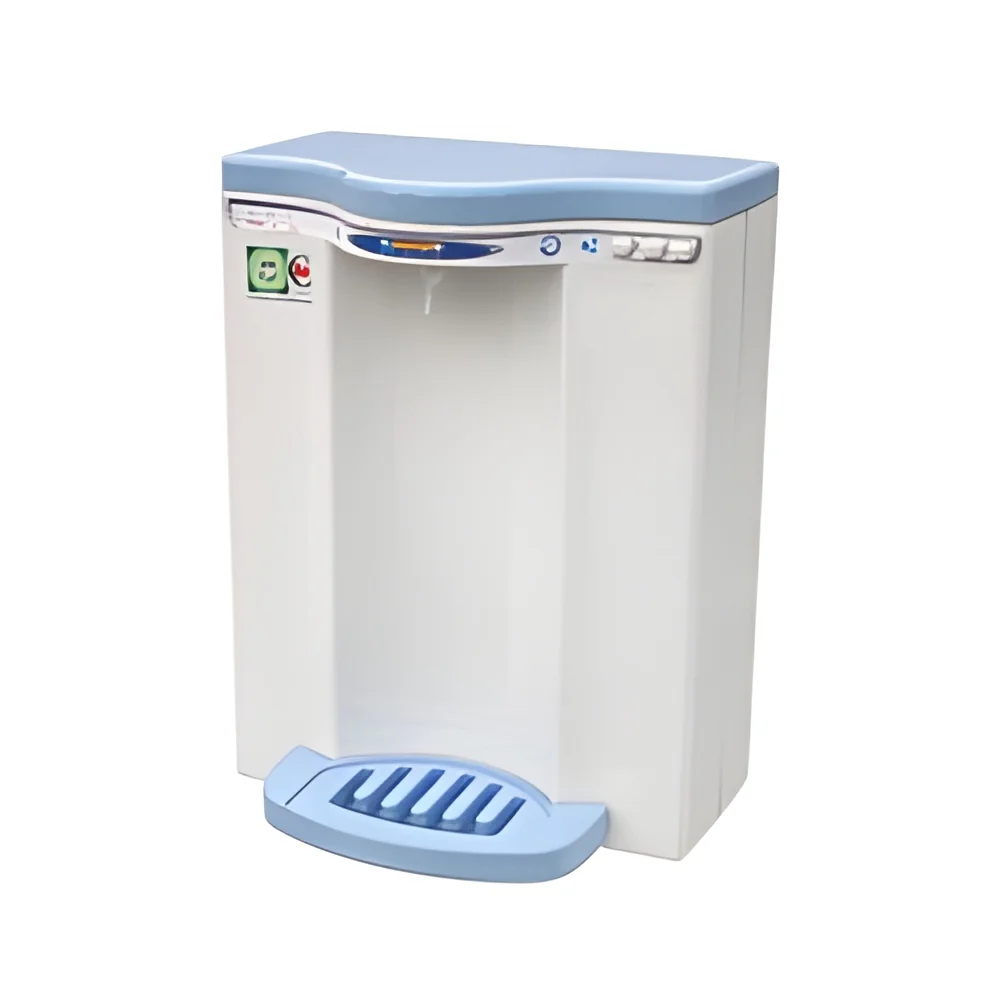
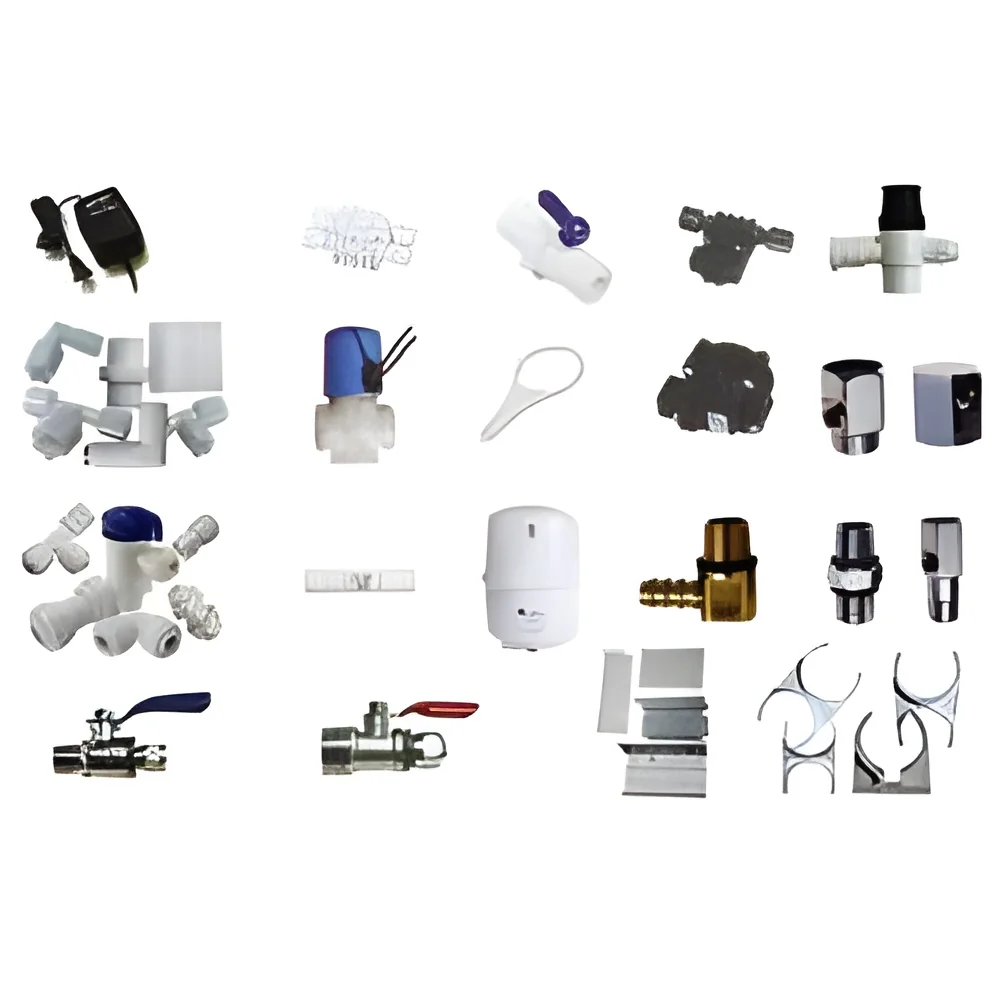
Industrial And Domestic Pumps For Water Supply And Chemical Transfer
Premium industrial and domestic water pumps deliver reliable performance for water supply and chemical transfer applications. Engineered with advanced technology for superior durability and efficiency across residential, agricultural, and industrial sectors.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Bharat Lubricants
 New Delhi, India
Distributor / Wholesaler