IN
₹
Apparel & Fashion
Description
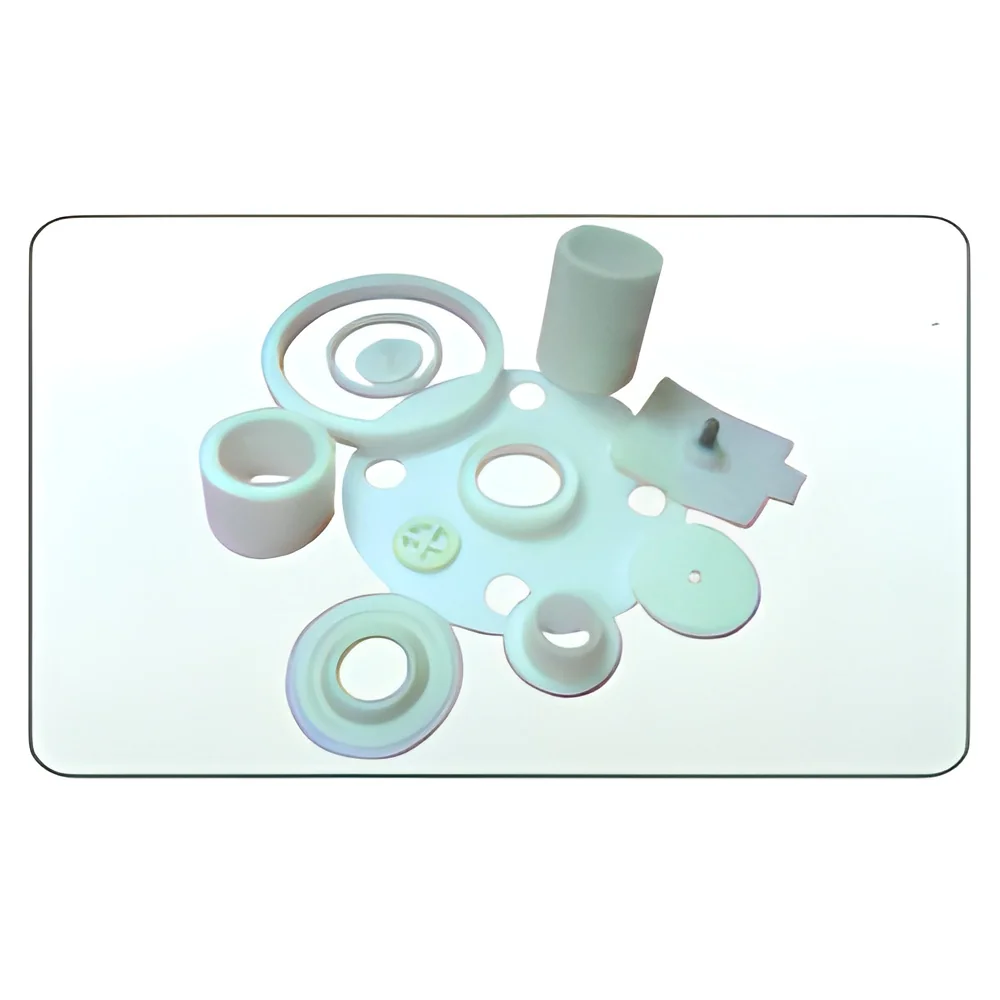
Our industrial PTFE products represent the highest standard in polymer manufacturing, specifically engineered for demanding industrial environments where reliability and performance are critical. These components offer unmatched chemical resistance against acids, solvents, and aggressive media while maintaining excellent mechanical properties and structural integrity across extreme temperature ranges. Manufactured using premium virgin PTFE materials from certified suppliers, each product undergoes rigorous quality control to ensure consistent performance and long-term reliability. The material's inherent non-toxic properties and compliance with international standards make it suitable for applications requiring purity and safety in sensitive processing environments. We provide reliable solutions tailored to specific operational requirements with precise dimensional accuracy and material specifications.

These PTFE components serve essential functions across multiple industries where ma...
Our industrial PTFE products represent the highest standard in polymer manufacturing, specifically engineered for demanding industrial environments where reliability and performance are critical. These components offer unmatched chemical resistance against acids, solvents, and aggressive media while maintaining excellent mechanical properties and structural integrity across extreme temperature ranges. Manufactured using premium virgin PTFE materials from certified suppliers, each product undergoes rigorous quality control to ensure consistent performance and long-term reliability. The material's inherent non-toxic properties and compliance with international standards make it suitable for applications requiring purity and safety in sensitive processing environments. We provide reliable solutions tailored to specific operational requirements with precise dimensional accuracy and material specifications.

These PTFE components serve essential functions across multiple industries where material failure is not an option. In chemical processing, they provide dependable sealing solutions for reactors, pipes, and storage systems handling corrosive substances at extreme temperatures. The automotive sector utilizes PTFE for bearings and bushings that withstand temperature variations and reduce friction in transmission systems. Oil and gas applications depend on PTFE for valve components that resist sour gas environments and high-pressure conditions, while the pharmaceutical industry values its purity for processing equipment requiring strict contamination control. Electrical industries benefit from its excellent dielectric properties in high-voltage applications and semiconductor manufacturing processes.

Businesses choose our PTFE products for their proven reliability and significant long-term cost savings through reduced maintenance cycles and extended equipment lifespan. The material's exceptional durability translates to improved operational efficiency and minimized downtime, directly impacting productivity and operational costs. Our customization capabilities ensure perfect compatibility with existing systems, while our testing protocols guarantee performance meets international standards including ASTM and ISO specifications. We provide comprehensive technical support to help select the appropriate PTFE grade for specific application requirements, ensuring optimal performance and maximum value for your operational needs.

Key Features:
- Superior chemical resistance against acids, solvents, and aggressive media
- Exceptional temperature resistance from -200°C to 260°C
- High tensile strength and excellent mechanical properties
- Non-toxic properties suitable for sensitive applications
- Customizable solutions with precise dimensional accuracy

Benefits:
- Extended equipment lifespan through superior material durability
- Reduced maintenance costs and operational downtime
- Reliable performance in extreme temperature conditions
- Safe operation in sensitive processing environments
- Perfect compatibility with existing industrial systems
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Industrial PTFE products excel in harsh environments where chemical resistance and minimal friction are critical. They maintain structural integrity across extreme temperatures from -200°C to 260°C, outperforming other materials in demanding conditions. Their non-stick properties and electrical insulation capabilities ensure reliable operation across diverse industrial settings and challenging operational requirements.
These components serve essential functions in sealing systems, bearing assemblies, and insulation applications across multiple sectors. Their durability ensures extended service life with minimal maintenance, reducing operational downtime and replacement costs. Industries rely on PTFE for consistent performance under pressure and in corrosive conditions where reliability is essential for continuous operations and safety compliance.
- Chemical processing equipment seals, gaskets, and linings for acid handling systems
- Automotive industry bearings, bushings, and thrust washers in transmission systems
- Oil and gas industry valve seats, seals, and ball valve components for sour gas environments
- Pump parts including impellers, diaphragms, and wear rings for corrosive fluid transfer
- Electrical insulation applications in transformers, connectors, and semiconductor manufacturing
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Anil Rubber Products, Maharashtra
 Maharashtra, India
Automotive & Transport•Manufacturer•Distributor / Wholesaler
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Main Markets
Domestic
Industrial PTFE Products For Chemical Resistance And High Temperature
Industrial PTFE products provide superior chemical resistance and high temperature performance from -200°C to 260°C for chemical processing, automotive, and oil and gas industries with reliable customization options.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Anil Rubber Products
 Maharashtra, India
Automotive & TransportManufacturer