IN
₹
Apparel & Fashion

Description
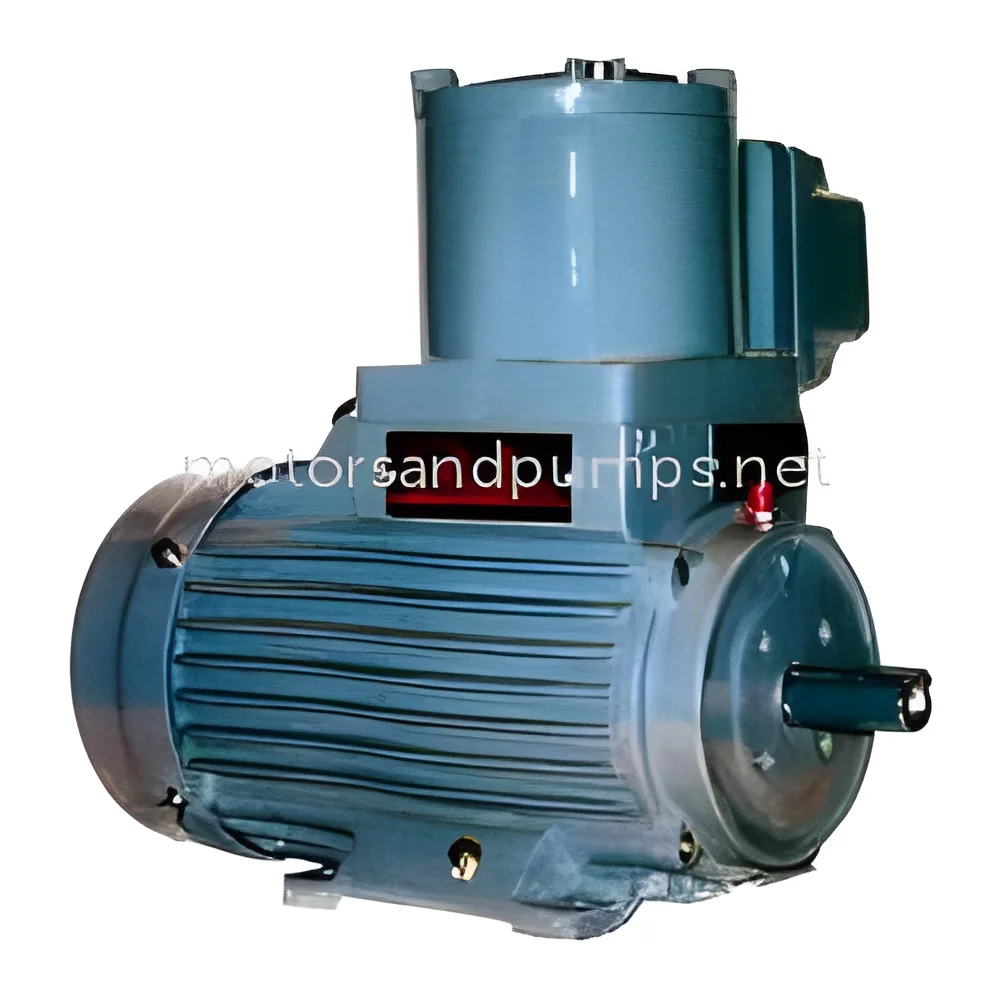
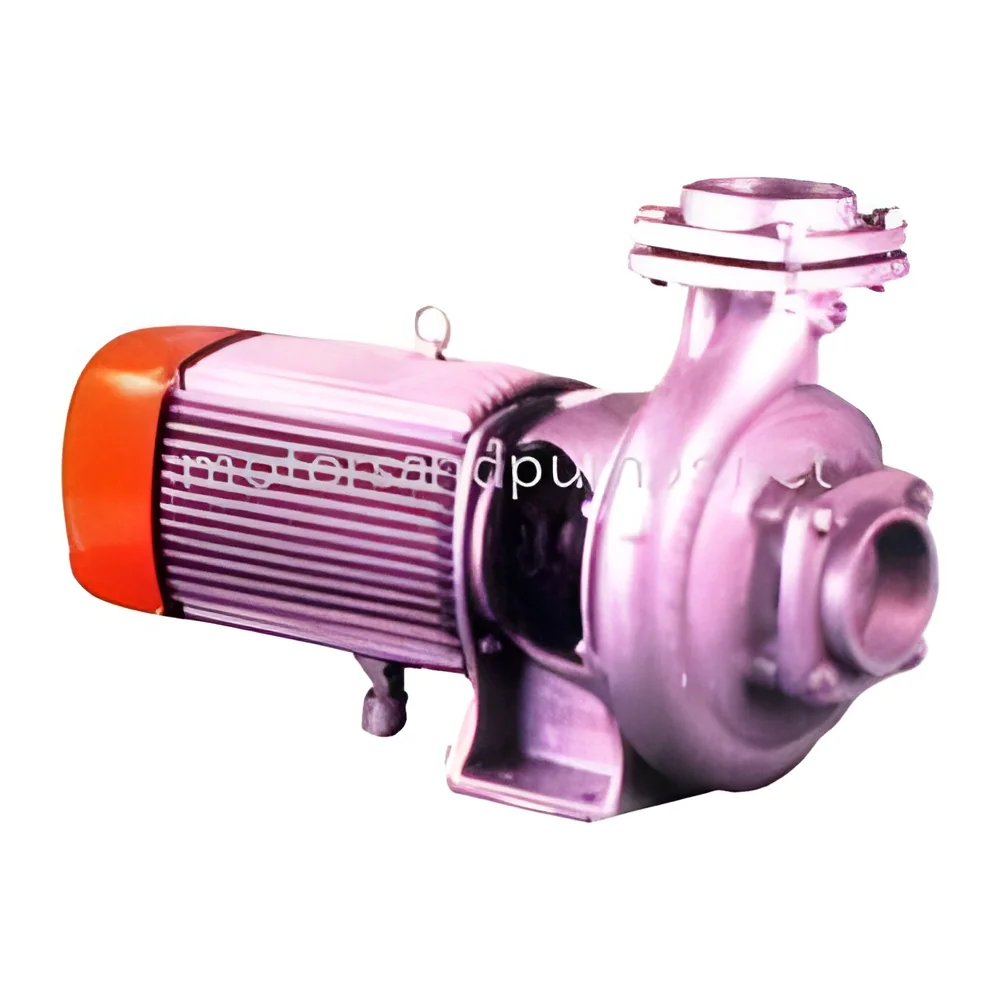
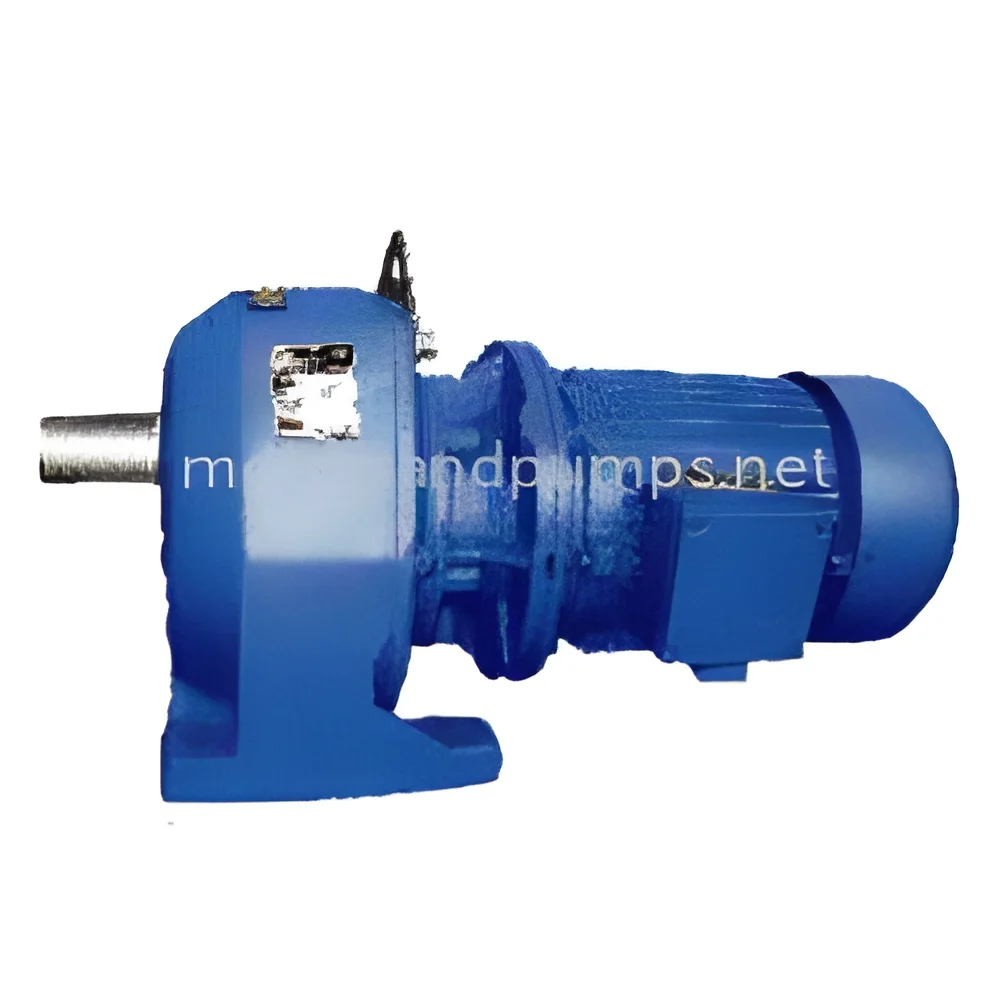
Industrial process pump sets deliver reliable fluid transfer solutions specifically engineered for demanding chemical and water treatment applications. These robust systems feature corrosion-resistant construction materials that withstand aggressive chemicals, high-purity water, and various industrial fluids while maintaining consistent performance. Designed for continuous operation in challenging environments, they provide precise flow control and pressure maintenance essential for industrial processes. The engineering focuses on durability and operational efficiency, with components selected for long service life and minimal maintenance requirements across extended operational cycles.

Multiple industries rely on these process pump sets for critical fluid handling operations. Chemical manufacturing facilities utilize them for transferring acids, solvents, and reactive compounds while ensuring containment integrity and safety. Water treatment plants implement these systems for chemica...
Industrial process pump sets deliver reliable fluid transfer solutions specifically engineered for demanding chemical and water treatment applications. These robust systems feature corrosion-resistant construction materials that withstand aggressive chemicals, high-purity water, and various industrial fluids while maintaining consistent performance. Designed for continuous operation in challenging environments, they provide precise flow control and pressure maintenance essential for industrial processes. The engineering focuses on durability and operational efficiency, with components selected for long service life and minimal maintenance requirements across extended operational cycles.

Multiple industries rely on these process pump sets for critical fluid handling operations. Chemical manufacturing facilities utilize them for transferring acids, solvents, and reactive compounds while ensuring containment integrity and safety. Water treatment plants implement these systems for chemical dosing, filtration processes, and wastewater management where reliable performance is essential. Pharmaceutical manufacturers depend on them for sterile fluid handling and precise metering applications that require contamination control. Industrial processing plants use these pumps for cooling systems, process chemical transfer, and various manufacturing applications where consistent fluid movement supports production efficiency.

Businesses select these process pump sets for their proven reliability and operational advantages. The durable construction reduces downtime through extended service intervals and easy maintenance access, while energy-efficient design contributes to lower operating costs. These systems offer consistent performance that protects production processes and minimizes operational risks in demanding industrial settings. With quality engineering and thorough testing protocols, they provide dependable fluid transfer solutions that support continuous operations and process stability across various industrial applications.

Key Features:
- Corrosion-resistant construction materials suitable for aggressive chemical handling
- Robust mechanical seals designed for extended service life and leak prevention
- Precision-engineered impellers for consistent flow rates and pressure maintenance
- Thermal protection and overload safeguards for enhanced operational security
- Durable motor configurations designed for continuous industrial operation

Benefits:
- Reliable performance in demanding chemical and water treatment applications
- Reduced maintenance requirements through durable construction and quality components
- Consistent fluid transfer supporting process stability and production efficiency
- Energy-efficient operation contributing to lower operational costs
- Long service life minimizing replacement frequency and total cost of ownership
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Industrial process pump sets provide dependable fluid transfer solutions for demanding chemical and water treatment applications. Their robust construction handles aggressive chemicals, high-purity water, and various industrial fluids with consistent performance. These systems maintain precise flow control and pressure specifications even during continuous operation cycles, ensuring process stability and operational reliability across different industrial settings.
Engineered for seamless integration into existing infrastructure, these pump sets offer flexible installation options and compatibility with diverse piping configurations. Industries value their ability to handle temperature variations, viscous materials, and corrosive substances while minimizing maintenance requirements. The reliable performance supports critical processes where fluid transfer precision directly impacts production quality and operational safety in challenging industrial environments.
- Chemical manufacturing plants for safe transfer of acids, solvents, and reactive compounds
- Water treatment facilities for chemical injection, filtration, and dosing operations
- Pharmaceutical production for sterile fluid handling and precise metering applications
- Industrial processing plants for circulating cooling water and heat transfer fluids
- Manufacturing facilities for handling process chemicals and wastewater treatment systems
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Petece Enviro Engineers, Tamil Nadu
 Tamil Nadu, India
Electronics & Electrical•Trading Company•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Main Markets
North America
Northern Europe
Mid East
Southern Europe
Eastern Europe
South Asia
Western Europe
Africa
Domestic
Industrial Process Pump Sets For Chemical Water Treatment
Industrial process pump sets for chemical water treatment applications. Built with corrosion-resistant materials for reliable fluid transfer in demanding industrial environments. Ideal for chemical processing, pharmaceutical manufacturing, and water treatment facilities.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Petece Enviro Engineers
 Tamil Nadu, India
Electronics & ElectricalTrading Company