IN
₹

Description
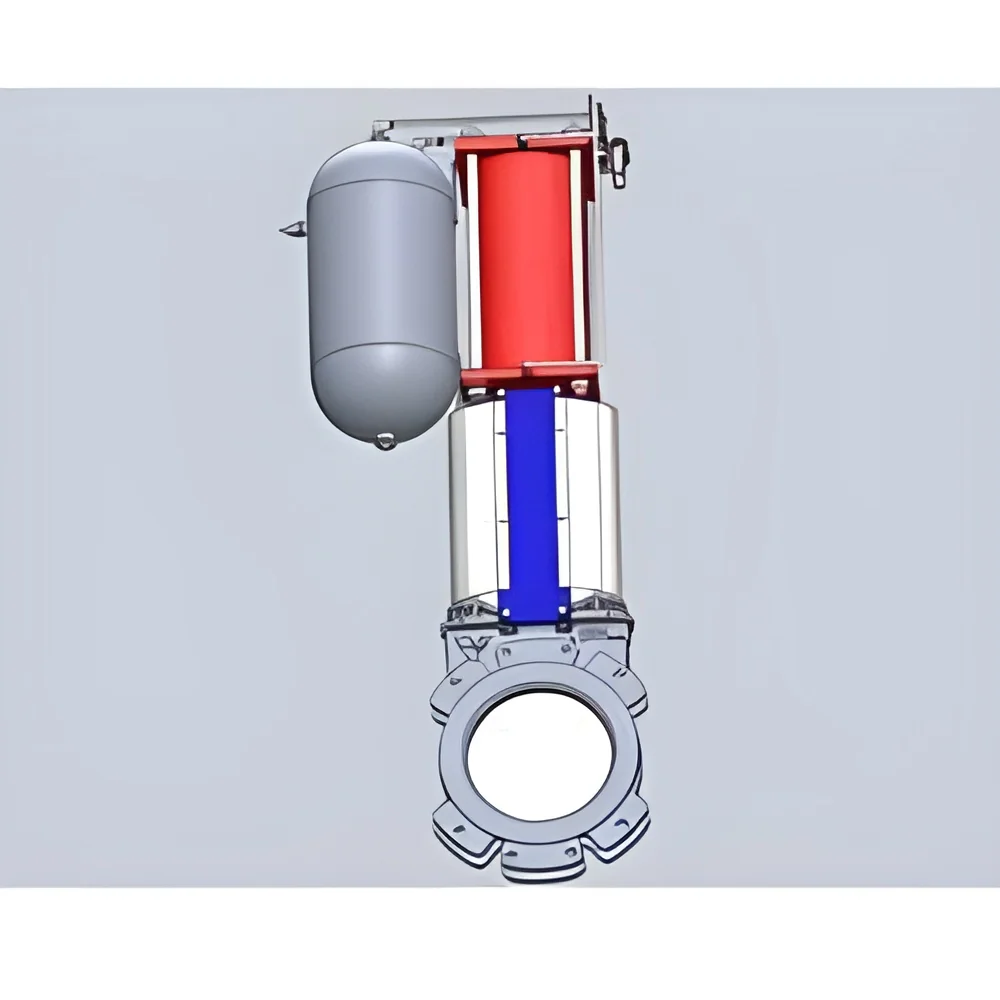
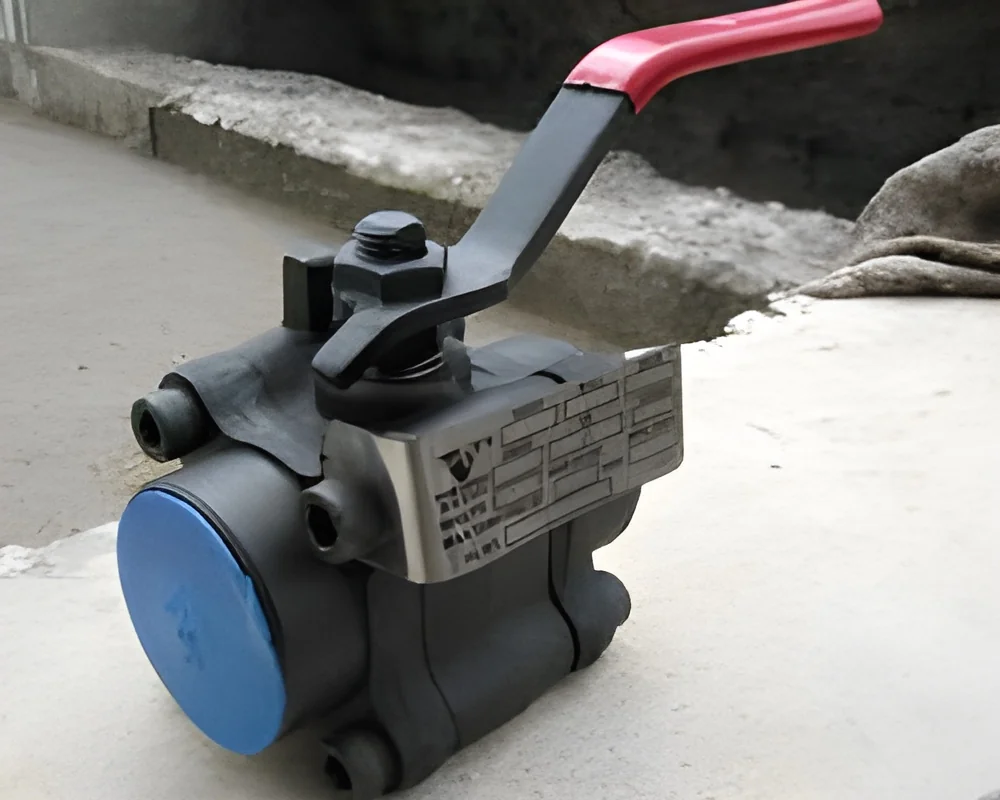
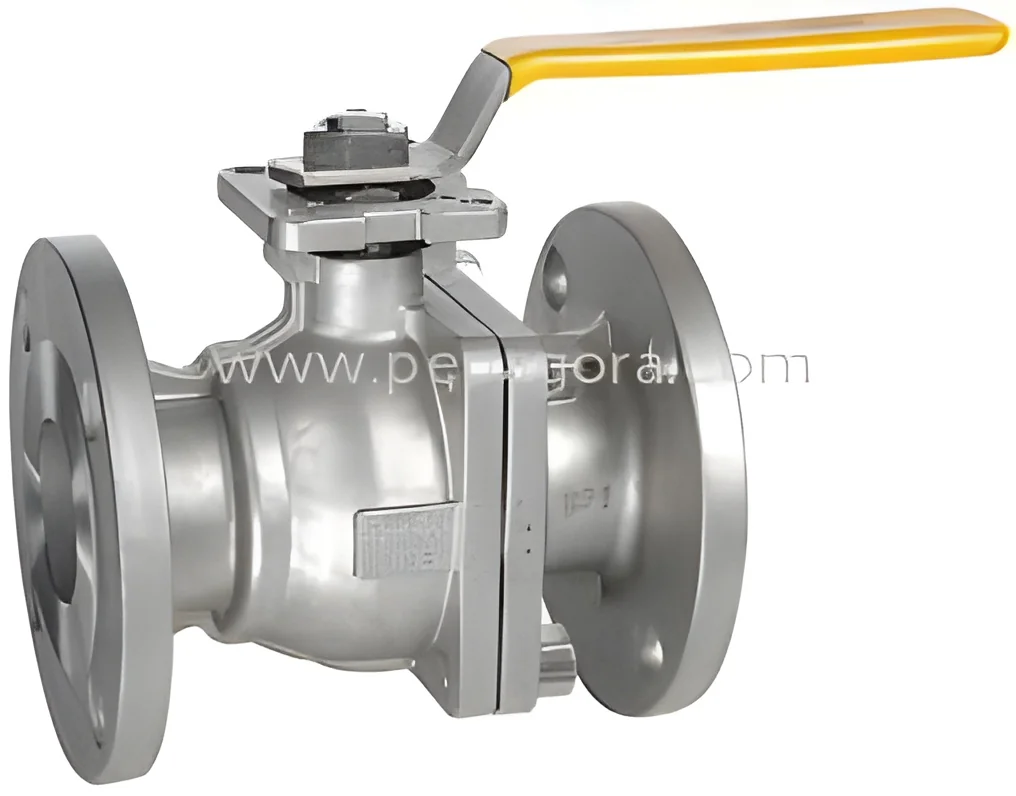
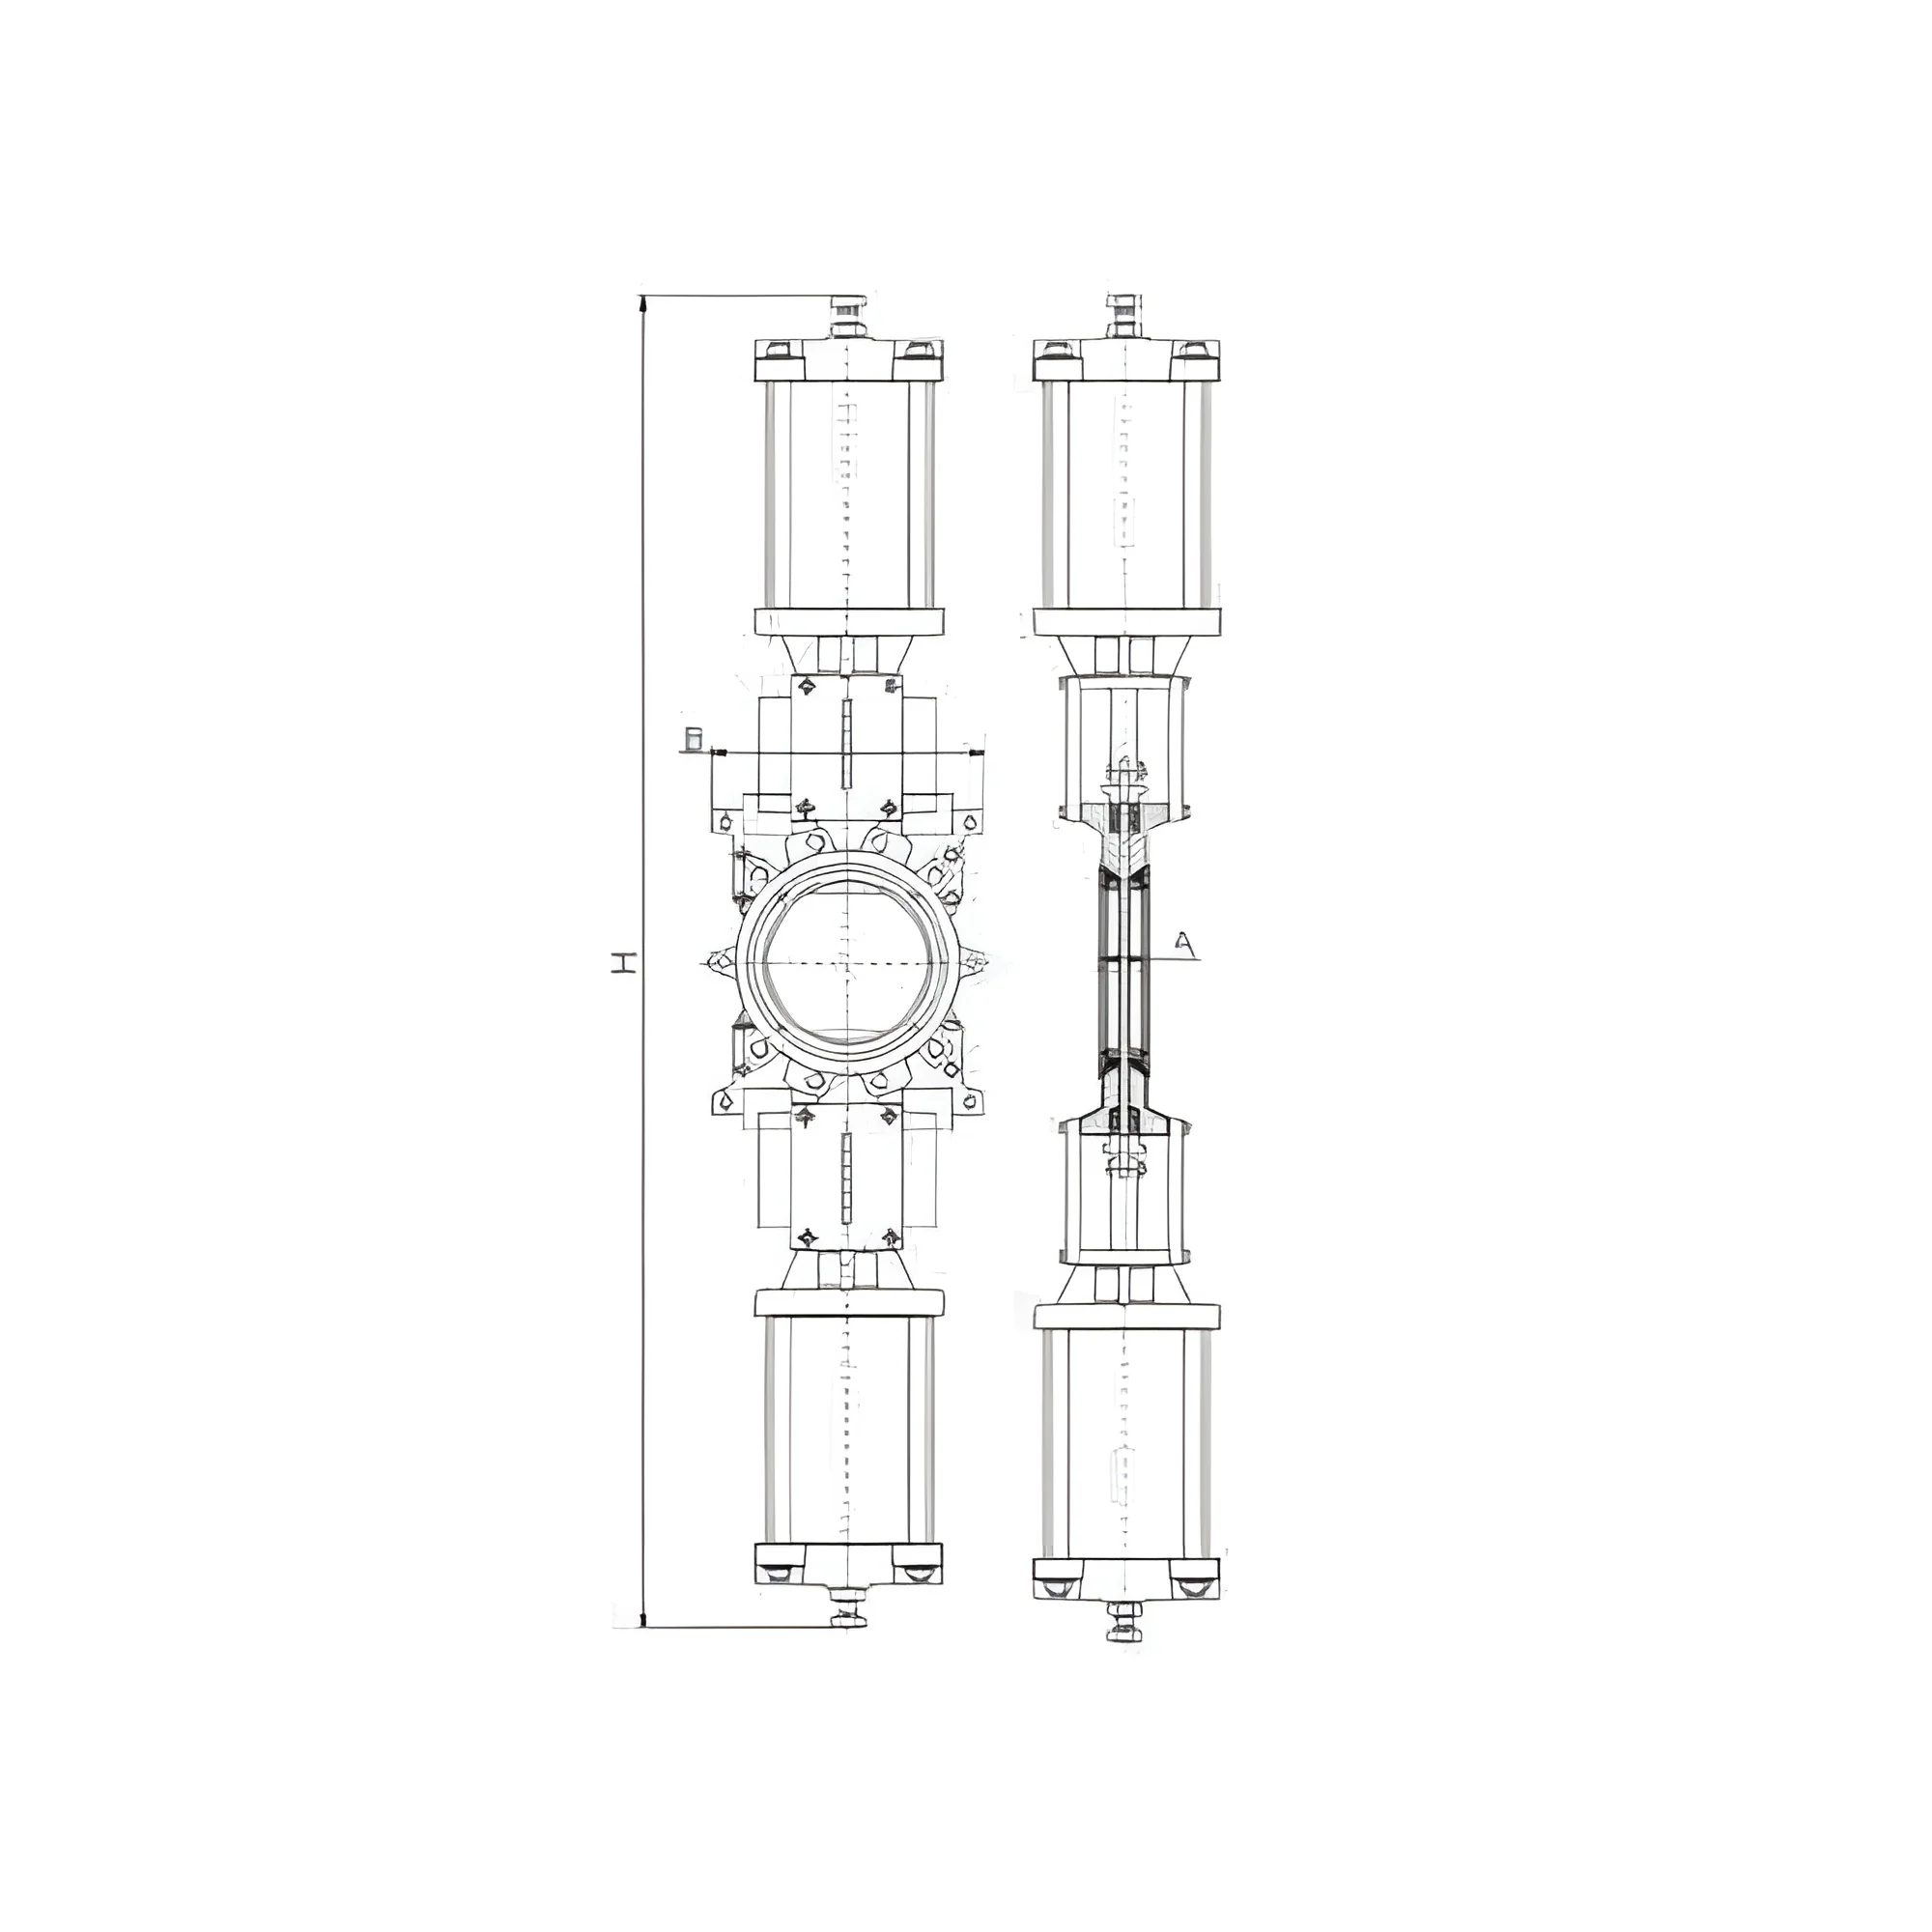
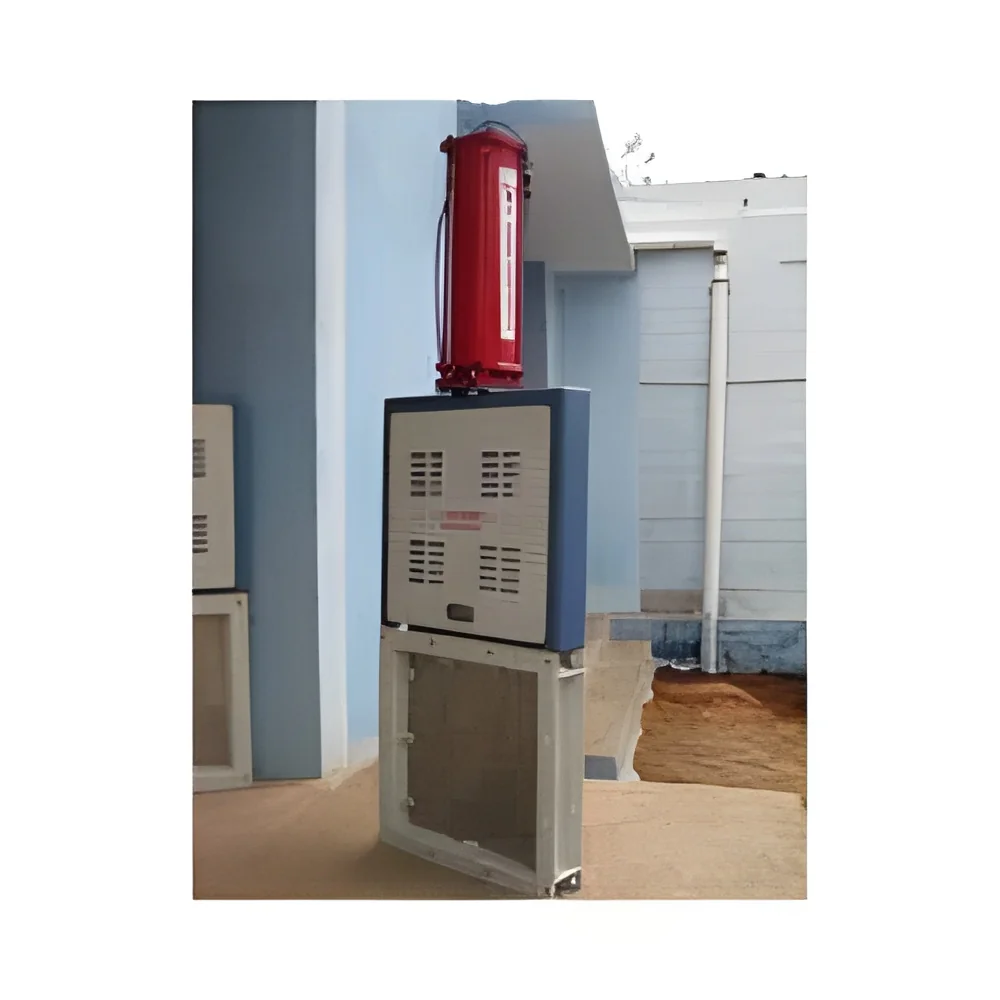
Our industrial pneumatic ball valves are engineered for exceptional durability and precise flow control in demanding operational environments. These high-performance valves feature robust construction with both automatic and manual operation options, providing maximum flexibility for diverse system requirements. Manufactured with quality materials and precision engineering, they deliver long-term reliability and consistent performance across various applications, ensuring your operations run smoothly with minimal downtime and maintenance requirements. The valves are designed to handle pressures from #150 to #1500 and are available in sizes up to 24 inches to accommodate different industrial flow specifications.

These pneumatic ball valves serve critical functions across multiple industries including food processing, chemical manufacturing, water treatment, and agricultural systems. In food processing applications, they maintain strict hygienic standards while controlling various flow ...
Our industrial pneumatic ball valves are engineered for exceptional durability and precise flow control in demanding operational environments. These high-performance valves feature robust construction with both automatic and manual operation options, providing maximum flexibility for diverse system requirements. Manufactured with quality materials and precision engineering, they deliver long-term reliability and consistent performance across various applications, ensuring your operations run smoothly with minimal downtime and maintenance requirements. The valves are designed to handle pressures from #150 to #1500 and are available in sizes up to 24 inches to accommodate different industrial flow specifications.

These pneumatic ball valves serve critical functions across multiple industries including food processing, chemical manufacturing, water treatment, and agricultural systems. In food processing applications, they maintain strict hygienic standards while controlling various flow processes and meeting sanitation requirements. Chemical processing plants rely on their corrosion-resistant properties and ability to handle aggressive media. Water treatment facilities benefit from their reliable shut-off capabilities and durability in continuous operation. Agricultural operations utilize these valves for precise irrigation control and liquid distribution systems, demonstrating their versatility across different industrial sectors.

Businesses choose our pneumatic ball valves for their proven reliability, quality construction, and consistent performance assurance. Each valve undergoes rigorous testing to meet international industry standards, ensuring they perform reliably under pressure and demanding operating conditions. Our commitment to on-time delivery and comprehensive OEM support means you receive products that integrate seamlessly into your existing systems, reducing installation time and maintenance costs while maximizing operational efficiency and productivity. We provide reliable supply chain solutions with consistent quality that industrial buyers can depend on for their critical operations.

Key Features:
- Available in sizes up to 24 inches for various industrial applications
- Pressure ratings from #150 to #1500 to handle different system requirements
- Pneumatic operation for seamless automation integration and remote control
- Robust construction with quality materials for long-term durability and reliability
- Rigorous testing and quality assurance processes ensuring consistent performance

Benefits:
- Precise flow control for improved process efficiency and operational consistency
- Durable construction reduces maintenance requirements and extends service life
- Easy installation and integration with existing automated systems
- Reliable performance under varying pressure conditions from #150 to #1500
- Consistent quality assurance through rigorous testing protocols
Specifications
| Key Attributes | |
|---|---|
| Type | Ball Valves |
| Supply Type | OEM |
| Price | Negotiable |
| Condition | New |
| Standard or Nonstandard | Standard |
| Advantage | Easy to install |
| Delivery | On Time Delivery |
| Automatic Grade | Both Fully Automatic & Manual |
| Power | Pneumatic |
| Design Limit | Upto 24†|
| Pressure | #150 ,#300, #600, #800, #900 and #1500 |
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Pneumatic ball valves deliver exceptional flow control for industrial fluids and gases in automated systems. Their robust construction ensures reliable shut-off and precise regulation in demanding environments, making them essential for process automation across multiple sectors. These valves are specifically engineered for food processing, chemical manufacturing, water treatment, and agricultural applications with pneumatic operation enabling seamless remote control integration.
These industrial valves serve critical functions across food grade processing, chemical handling, water management, and agricultural systems. In food applications, they maintain strict hygienic standards while controlling flow processes. Chemical plants rely on their corrosion-resistant properties and tight sealing capabilities. Water treatment facilities benefit from reliable shut-off performance, while agricultural operations utilize them for precise irrigation control and distribution systems.
- Food processing lines for hygienic flow control and sanitation compliance
- Chemical manufacturing processes requiring precise fluid handling
- Water treatment plants and distribution systems for reliable flow management
- Agricultural irrigation systems and crop spraying equipment for liquid control
- Industrial automation and process control systems across manufacturing facilities
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile

V- Tork Controls, Tamil Nadu
 Tamil Nadu, India
Industrial Equipment & Machinery•Manufacturer•Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Main Markets
Eastern Asia
Industrial Pneumatic Ball Valves OEM Supply 24 Inch #150 #1500 Pressure
Industrial pneumatic ball valves provide precise flow control for food processing, agriculture, and chemical applications. Available in sizes up to 24 inches with pressure ratings from #150 to #1500. Reliable OEM supply with rigorous testing ensures durable performance.
Min. Order Quantity: 1 piece
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
V- Tork Controls
 Tamil Nadu, India
Industrial Equipment & MachineryManufacturer