IN
₹
Apparel & Fashion
Description
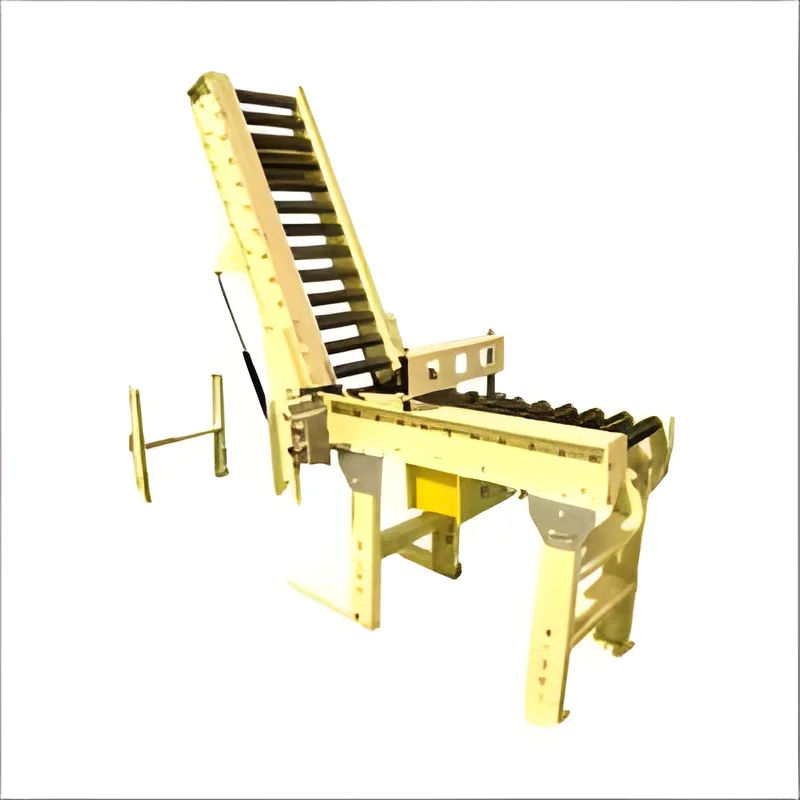
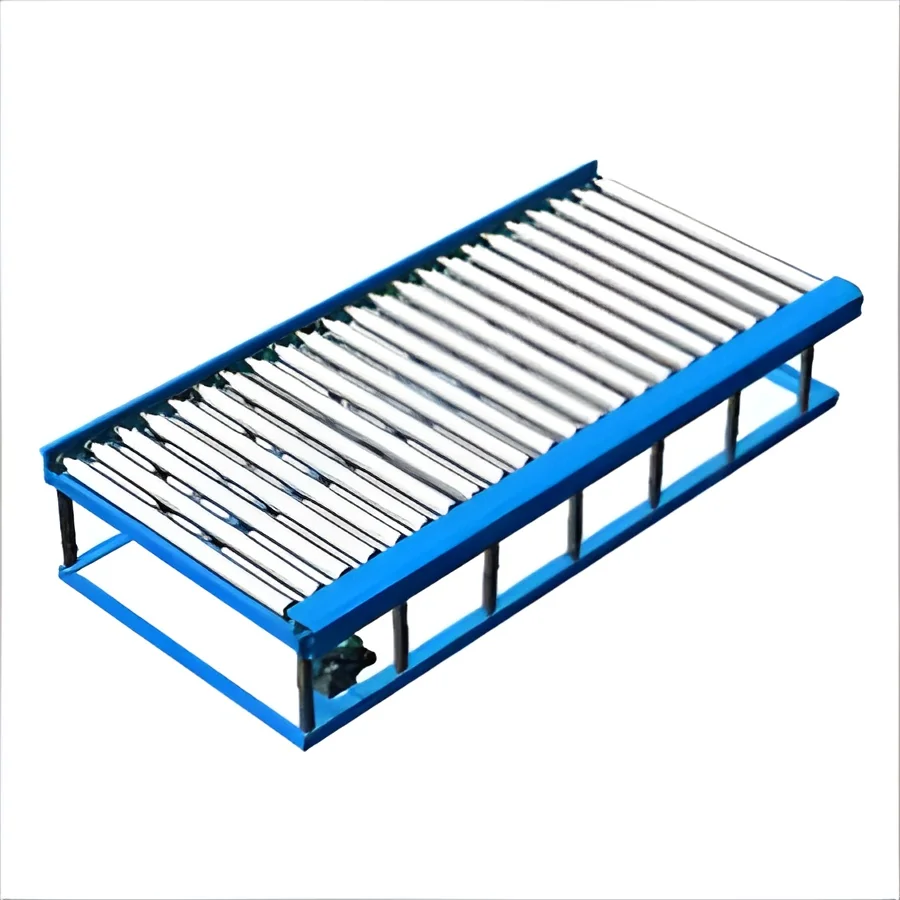
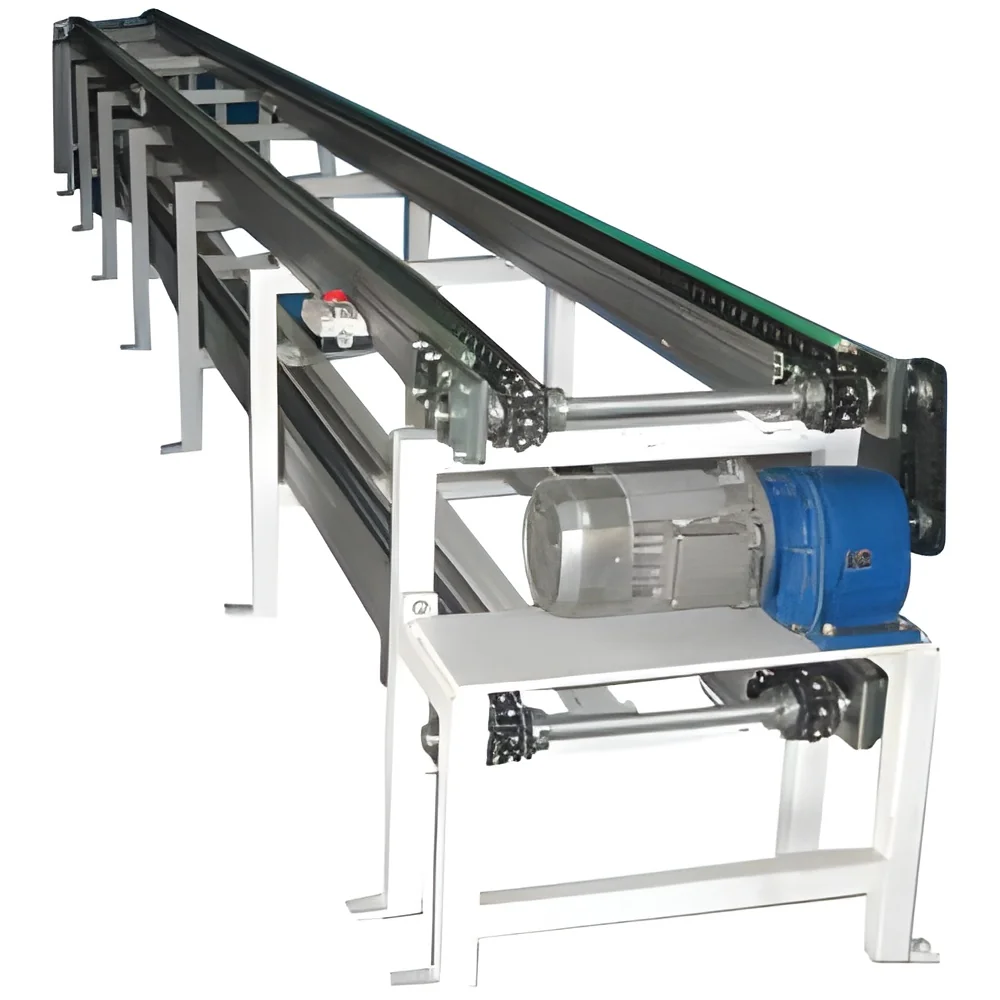
Our heavy duty palletized chain conveyors represent advanced bulk material handling technology engineered to meet demanding industrial requirements. These robust systems feature heavy-duty chain mechanisms capable of transporting palletized loads with exceptional reliability and precision. Available in both single tier and double tier configurations, our conveyors provide flexible solutions for various spatial and operational constraints. Each unit is manufactured using premium materials and advanced engineering to ensure long-term performance and minimal maintenance requirements, making them ideal for continuous operation environments where consistent performance is critical for operational success and efficiency.

These conveyor systems serve multiple industries where efficient material handling drives operational excellence. The food processing industry utilizes them for moving raw ingredients, packaged goods, and finished products through production facilities while maintaining str...
Our heavy duty palletized chain conveyors represent advanced bulk material handling technology engineered to meet demanding industrial requirements. These robust systems feature heavy-duty chain mechanisms capable of transporting palletized loads with exceptional reliability and precision. Available in both single tier and double tier configurations, our conveyors provide flexible solutions for various spatial and operational constraints. Each unit is manufactured using premium materials and advanced engineering to ensure long-term performance and minimal maintenance requirements, making them ideal for continuous operation environments where consistent performance is critical for operational success and efficiency.

These conveyor systems serve multiple industries where efficient material handling drives operational excellence. The food processing industry utilizes them for moving raw ingredients, packaged goods, and finished products through production facilities while maintaining strict sanitary standards. Manufacturing sectors including automotive, electronics, and consumer goods rely on these conveyors for assembly line integration and component transportation. Logistics and warehouse operations benefit from their ability to streamline loading, unloading, and sorting processes, while pharmaceutical and chemical industries value their durability and reliability in handling sensitive materials under strict compliance requirements and challenging operational conditions.

The business value of our palletized chain conveyors extends beyond transportation to deliver significant operational advantages and cost savings. These systems enhance productivity by ensuring consistent material flow, reducing manual handling requirements, and minimizing production bottlenecks. Their rugged construction and reliable performance translate to reduced maintenance costs and extended service life, providing excellent return on investment. The customizable designs allow for perfect integration with existing infrastructure, while their capacity to handle heavy loads without performance compromise makes them indispensable for businesses optimizing material handling operations and maintaining competitive advantage in dynamic market environments.

Key Features:
- Heavy-duty chain mechanism for reliable palletized load transportation
- Single and double tier configurations for space optimization
- Customizable designs to fit specific facility requirements
- Advanced construction ensuring durability and long service life
- Sanitary design suitable for food and pharmaceutical applications

Benefits:
- Enhanced productivity through consistent material flow
- Reduced manual handling and operational bottlenecks
- Lower maintenance costs and extended service life
- Perfect integration with existing infrastructure
- Heavy load capacity without performance compromise
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Palletized chain conveyors deliver robust solutions for moving heavy loads across production and distribution facilities. Their durable construction handles palletized goods, raw materials, and finished products with consistent reliability, making them essential for high-volume operations requiring uninterrupted material flow and minimal downtime in demanding industrial environments.
These conveyor systems excel in applications demanding sanitary conditions and heavy load capacity. Industries including food processing, beverage production, automotive manufacturing, and warehouse logistics benefit from their ability to maintain smooth operations while withstanding rigorous daily use and varying load weights across different production stages and material handling requirements.
- Automated pallet handling in food processing plants for raw ingredient transport
- Assembly line integration in automotive manufacturing for component movement
- Beverage industry bottling lines moving filled crates and pallets efficiently
- Warehouse and distribution centers for loading and unloading operations
- Pharmaceutical industry for secure and sanitary material transfer between processes
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Abhijeet Enterprise, Maharashtra
 Maharashtra, India
Industrial Equipment & Machinery•Manufacturer
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Heavy Duty Palletized Chain Conveyors For Bulk Material Handling
Heavy duty palletized chain conveyors for bulk material handling in food processing, manufacturing, and logistics. Customizable single and double tier designs ensure reliable transport with industry-leading durability and performance.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Abhijeet Enterprise
 Maharashtra, India
Industrial Equipment & MachineryManufacturer