IN
₹
Apparel & Fashion

Description
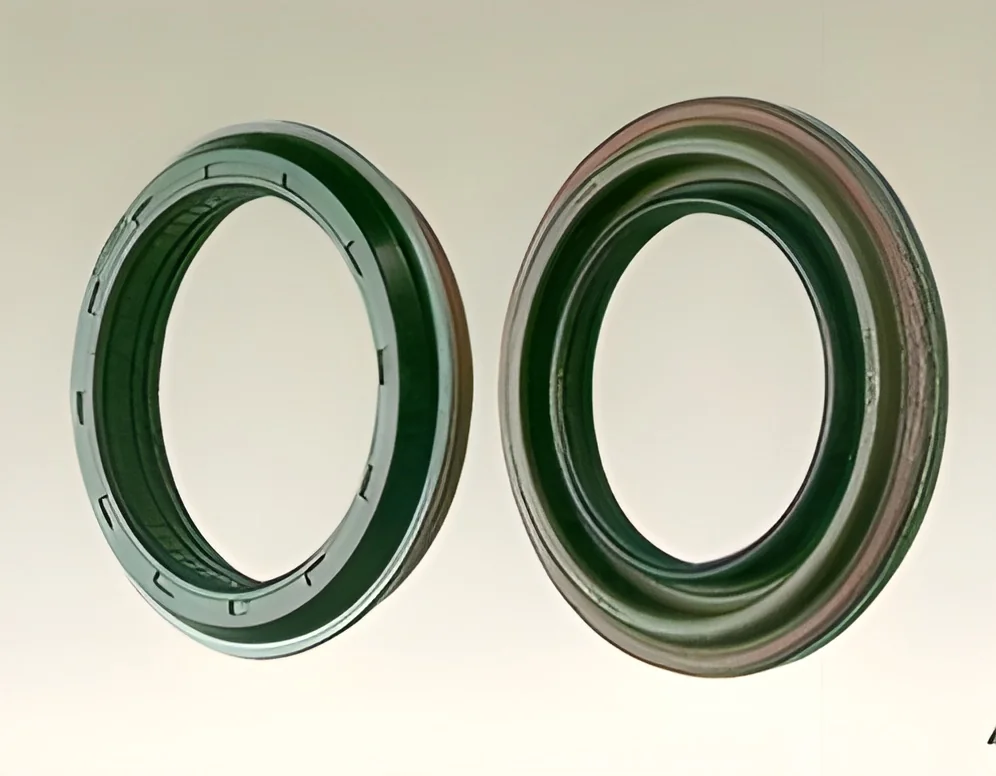
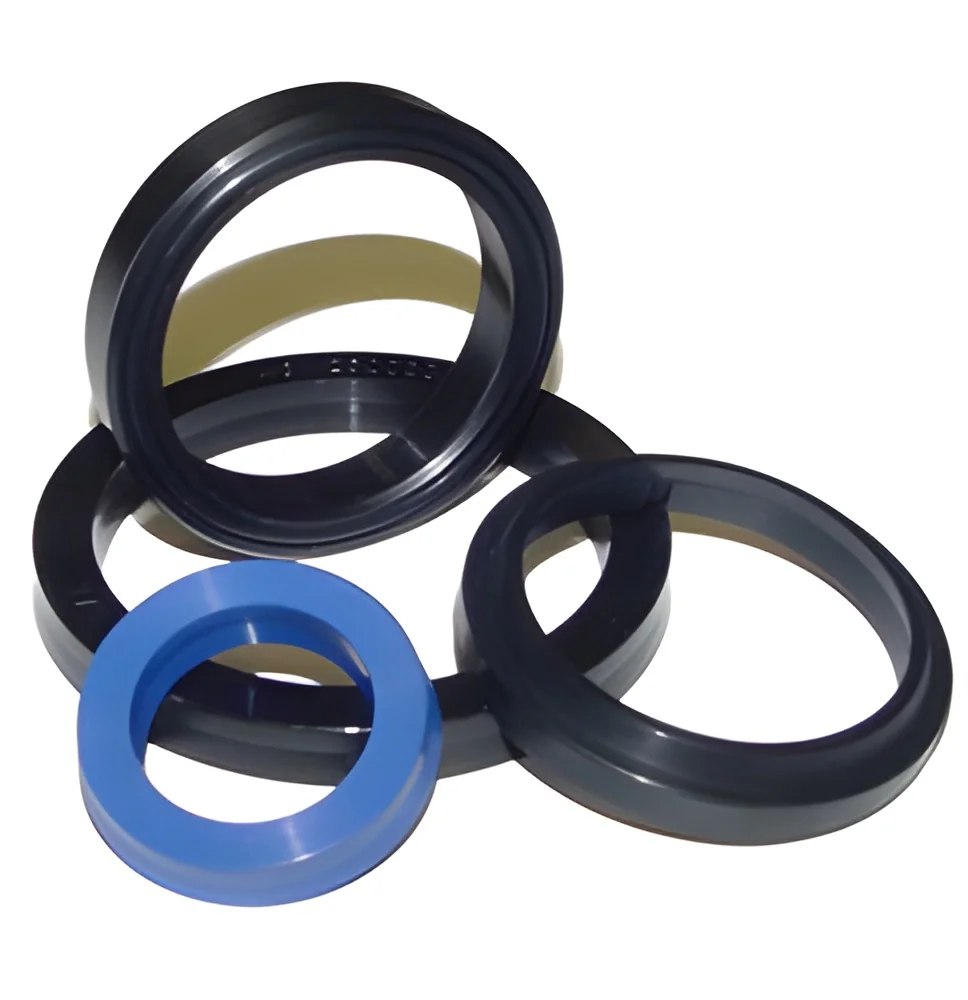
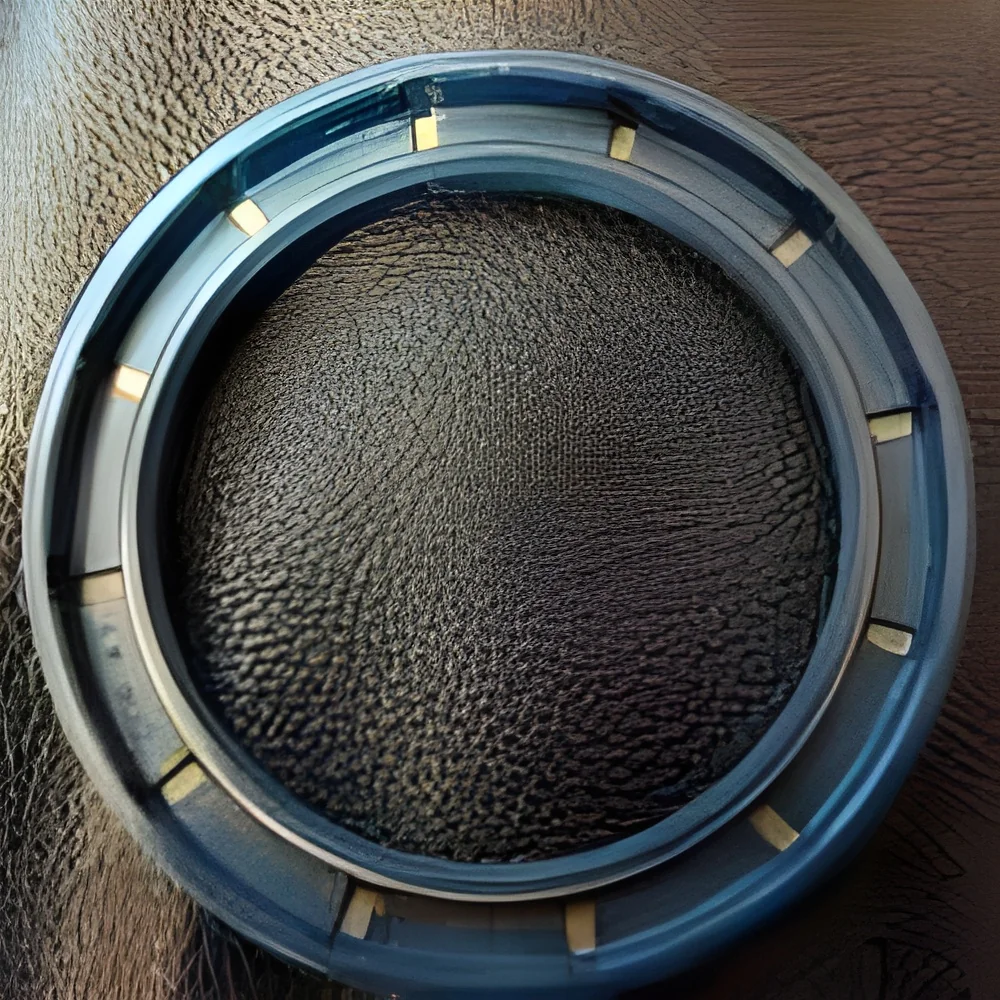
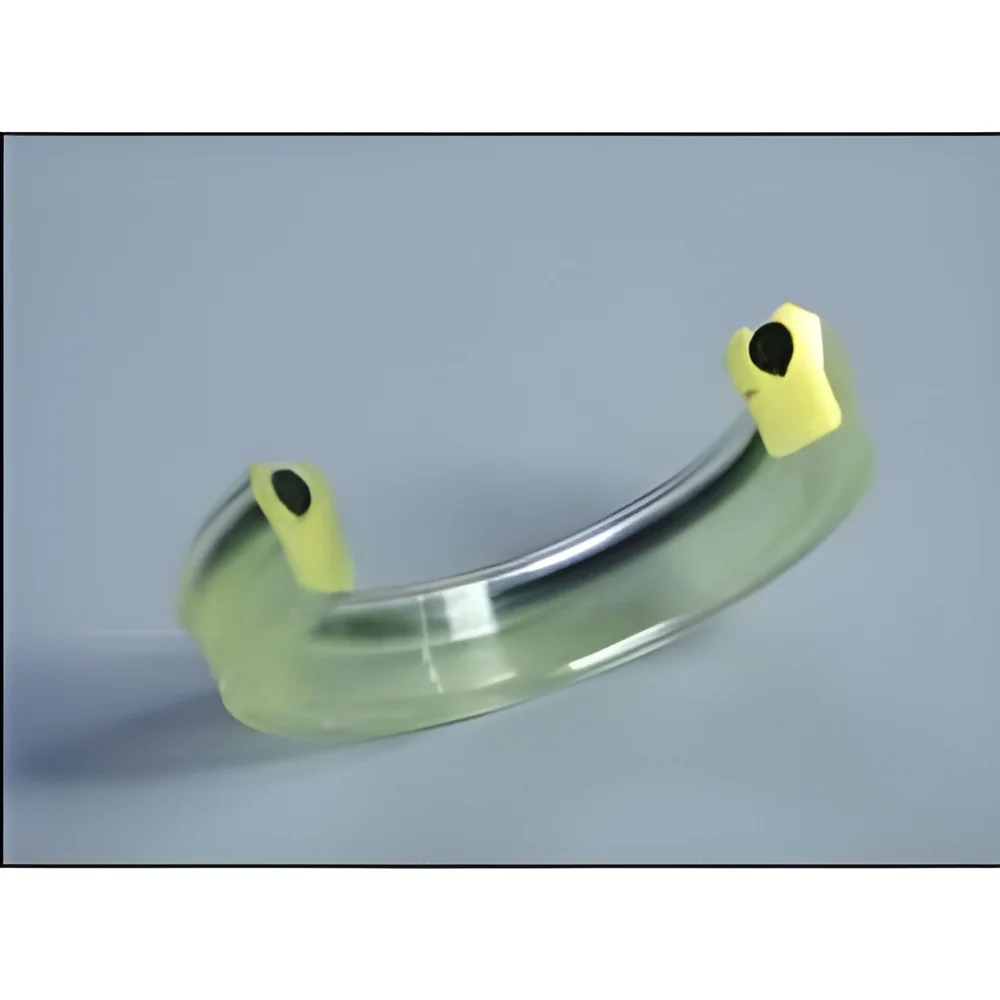
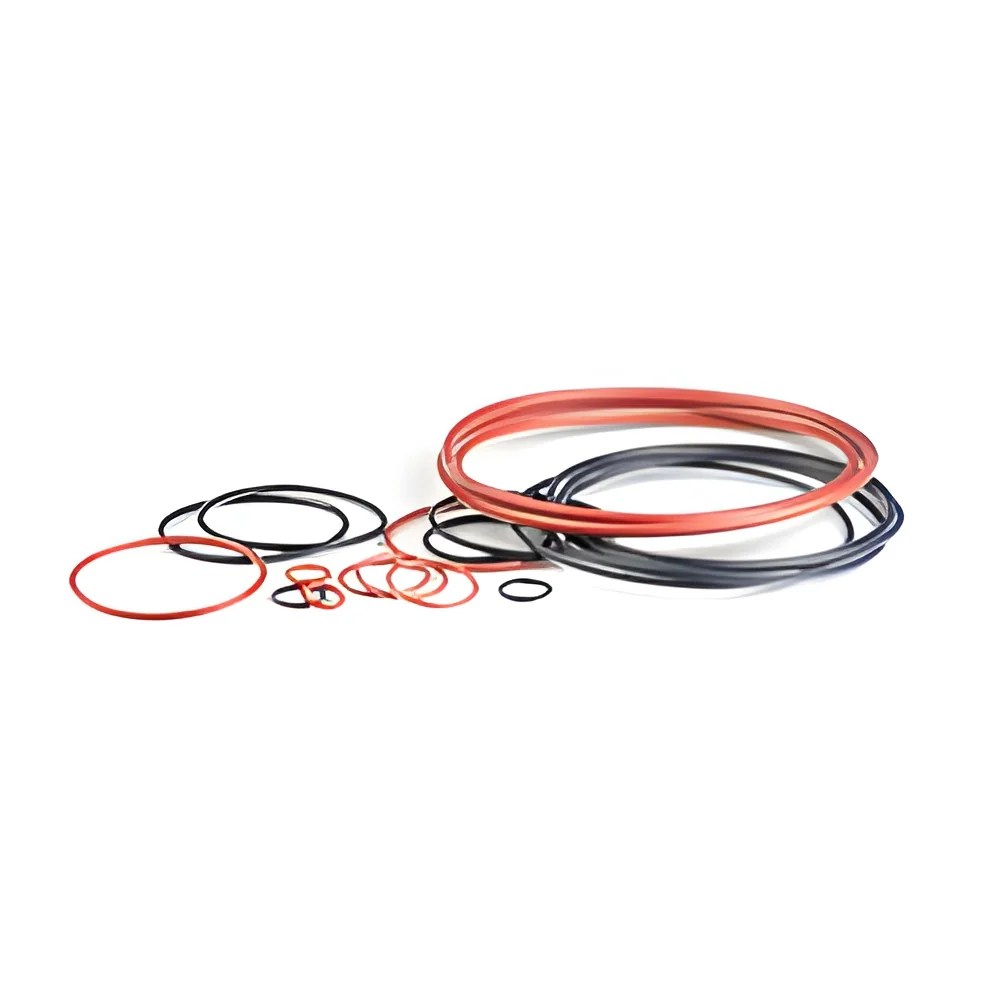
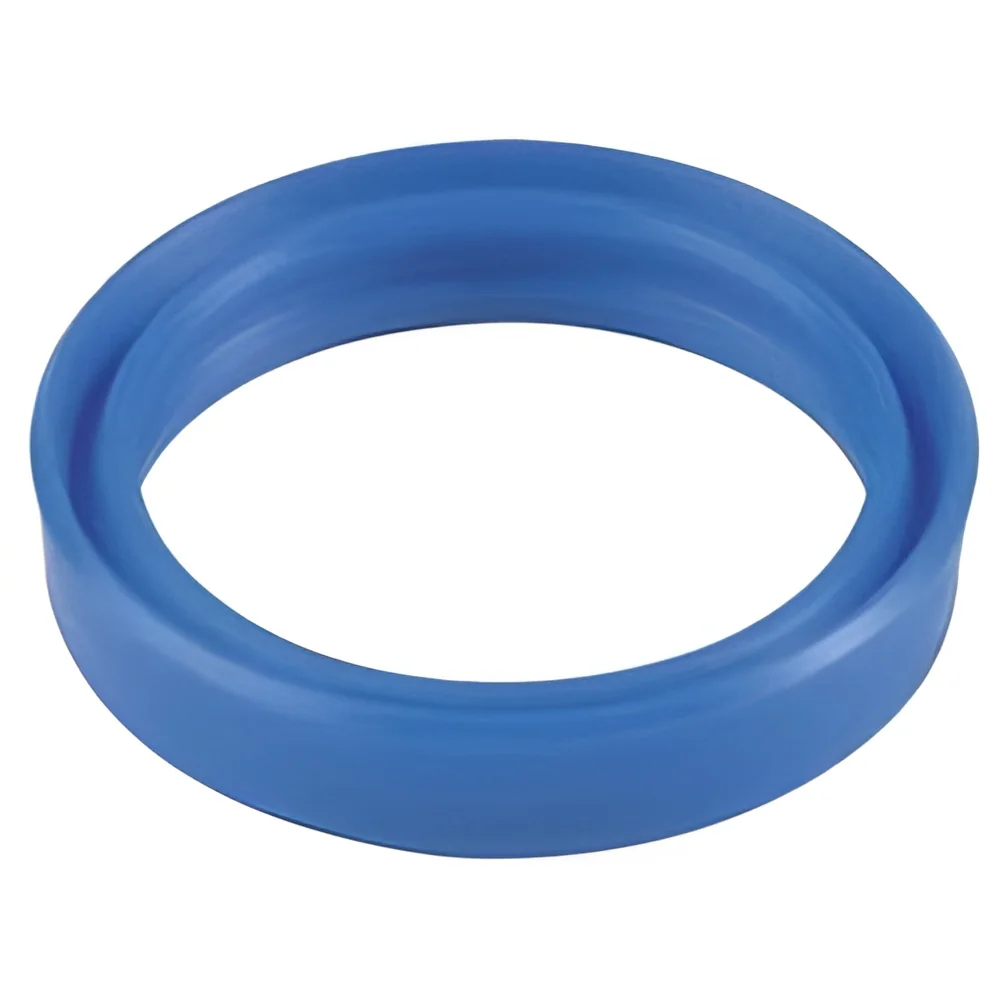
Our premium industrial oil seals represent precision-engineered sealing solutions specifically designed to prevent fluid leakage and exclude contaminants in demanding rotating shaft applications. Manufactured from high-quality materials including nitrile rubber, silicone, and fluorocarbon compounds, these seals deliver exceptional resistance to heat, pressure fluctuations, and chemical exposure. They maintain machinery efficiency and longevity by ensuring lubricants remain contained while preventing dirt, dust, and moisture infiltration. Suitable for diverse industrial environments, these components provide dependable performance even under the most challenging operational conditions, ensuring continuous protection for your valuable equipment and minimizing the risk of unexpected failures.

These oil seals serve critical functions across multiple industrial sectors with specific requirements. Within automotive manufacturing, they prevent oil leaks in engines, transmissions, and axles t...
Our premium industrial oil seals represent precision-engineered sealing solutions specifically designed to prevent fluid leakage and exclude contaminants in demanding rotating shaft applications. Manufactured from high-quality materials including nitrile rubber, silicone, and fluorocarbon compounds, these seals deliver exceptional resistance to heat, pressure fluctuations, and chemical exposure. They maintain machinery efficiency and longevity by ensuring lubricants remain contained while preventing dirt, dust, and moisture infiltration. Suitable for diverse industrial environments, these components provide dependable performance even under the most challenging operational conditions, ensuring continuous protection for your valuable equipment and minimizing the risk of unexpected failures.

These oil seals serve critical functions across multiple industrial sectors with specific requirements. Within automotive manufacturing, they prevent oil leaks in engines, transmissions, and axles to ensure smooth vehicle operation and emission compliance. Manufacturing facilities depend on them for industrial pumps, motors, and gearboxes to maintain operational efficiency while minimizing production interruptions. Agricultural equipment benefits from these seals in tractors and harvesters where they provide protection against harsh environmental elements like dust, mud, and temperature extremes. Marine applications utilize them in boat engines and offshore equipment for superior corrosion resistance in saltwater environments, while aerospace implementations require high-performance seals in aircraft systems where uncompromising reliability and safety standards are paramount for flight-critical components.

The business value delivered by our oil seals includes enhanced equipment reliability, reduced maintenance expenditures, and minimized unplanned operational downtime. Engineered to withstand extreme operating conditions, these components ensure extended service life and consistent performance throughout their usage cycle. Their proven reliability translates to fewer equipment failures and reduced replacement frequency, generating substantial cost savings over time through decreased maintenance requirements and less frequent component changes. Trusted by importers and distributors globally, our products come with guaranteed quality standards and responsive technical support, making them the intelligent choice for professional buyers seeking durable, high-value sealing solutions that protect their machinery investments and maintain productivity.

Key Features:
- Constructed from premium materials including nitrile rubber for enhanced durability and longevity
- Engineered to withstand elevated temperatures and significant pressure variations in industrial environments
- Available in multiple standard sizes to fit common industrial machinery requirements and specifications
- Superior resistance to oils, chemicals, and environmental contaminants for reliable performance
- Precision manufacturing ensures effective sealing contact and extended service life across applications

Benefits:
- Reduces maintenance costs through reliable leak prevention and contaminant exclusion
- Extends equipment lifespan by protecting internal components from wear and damage
- Minimizes operational downtime with consistent performance in demanding conditions
- Provides cost savings through reduced replacement frequency and maintenance requirements
- Ensures operational safety and reliability across various industrial applications and sectors
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Industrial oil seals are essential components designed to prevent fluid leakage and block contaminants in rotating shaft applications. They maintain operational integrity by keeping lubricants in and dirt, dust, and moisture out of critical machinery assemblies. This dual function protects sensitive components, reduces wear, and ensures consistent performance under challenging industrial conditions, directly impacting equipment longevity and operational safety.
These precision seals serve vital roles across diverse sectors including automotive manufacturing, industrial machinery, agriculture, marine engineering, and aerospace. In automotive systems, they prevent oil leaks in engines and transmissions. Manufacturing facilities rely on them for pumps, motors, and gearboxes. Agricultural equipment uses them for protection against harsh environments, while marine and aerospace applications demand their corrosion resistance and reliability for safety-critical systems where failure is not an option.
- Automotive engines and transmissions preventing oil leaks for smooth vehicle operation
- Industrial pumps, compressors, and gearboxes sealing rotating shafts and retaining lubricants
- Agricultural machinery including tractors and harvesters protecting against dirt and moisture ingress
- Marine equipment such as boat engines and offshore systems providing corrosion resistance
- Aerospace systems requiring high-performance seals for safety and reliability in aircraft components
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Benzona Sealing Technologies Private Limited, Andhra Pradesh
 Andhra Pradesh, India
Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Industrial Machinery Premium Oil Seals For Leak Prevention Durability
Premium industrial oil seals from trusted manufacturers provide superior leak prevention and durability for machinery. Engineered for reliable performance in demanding applications across automotive, manufacturing, and heavy equipment industries.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Benzona Sealing Technologies Private Limited
 Andhra Pradesh, India
Distributor / Wholesaler