IN
₹
Apparel & Fashion
Description
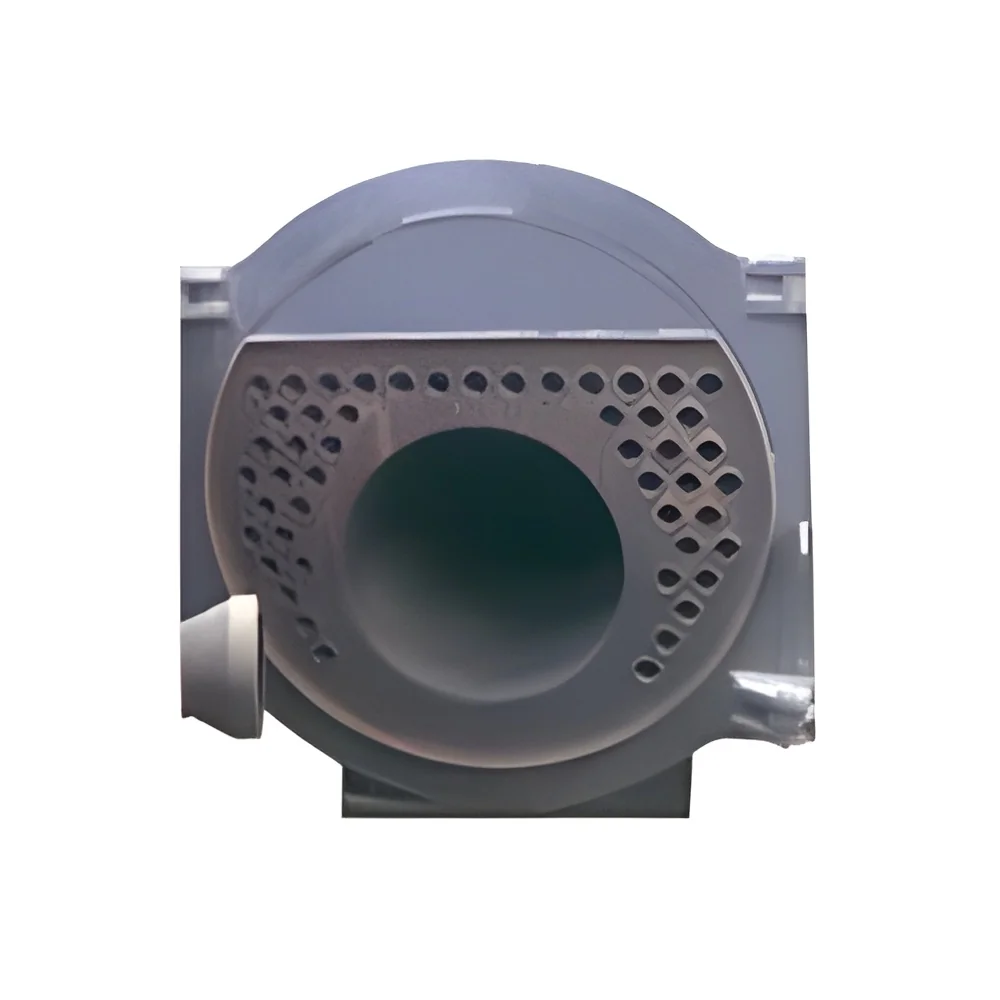
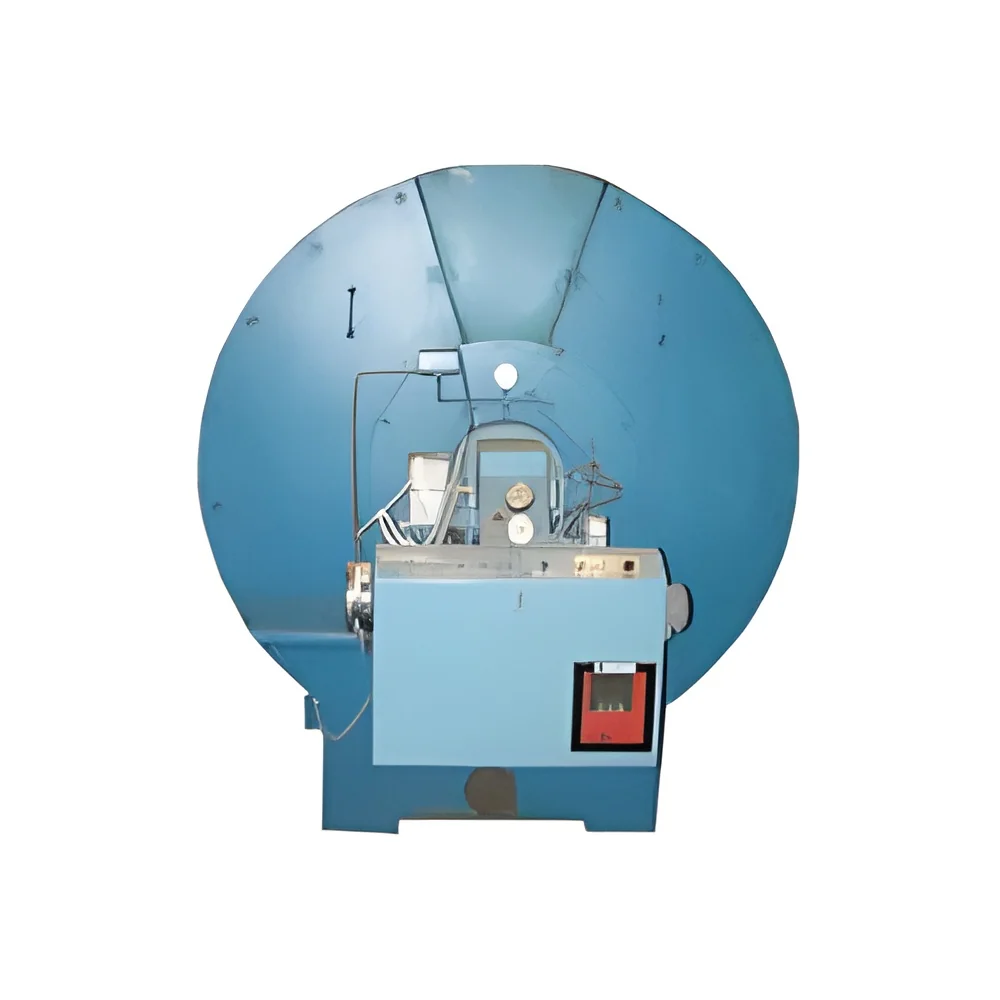
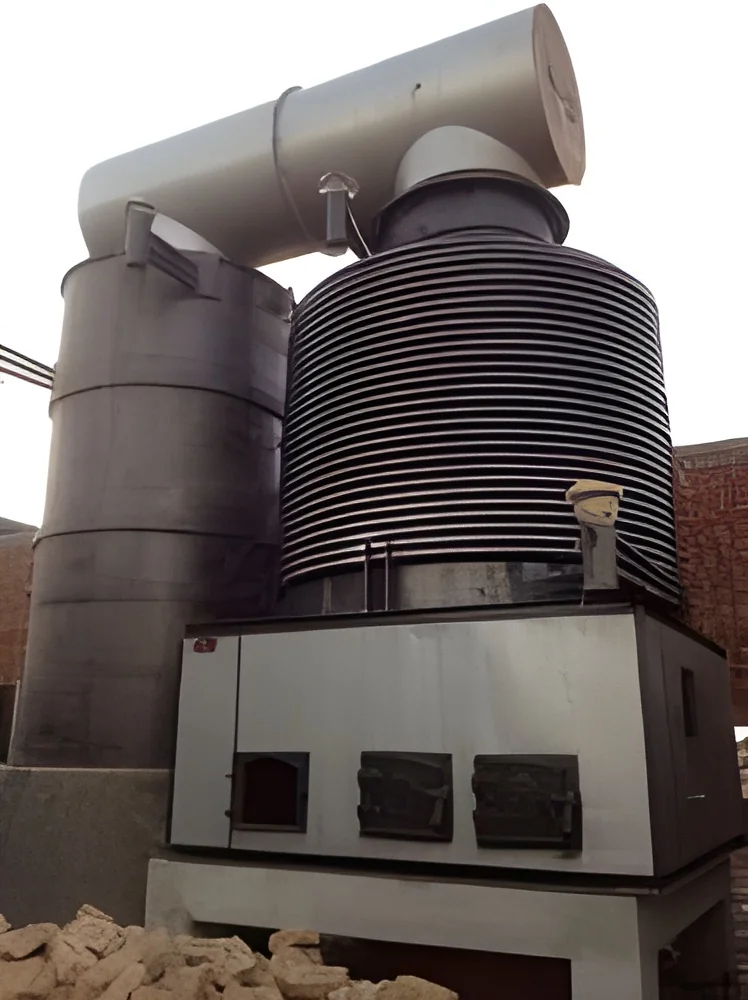
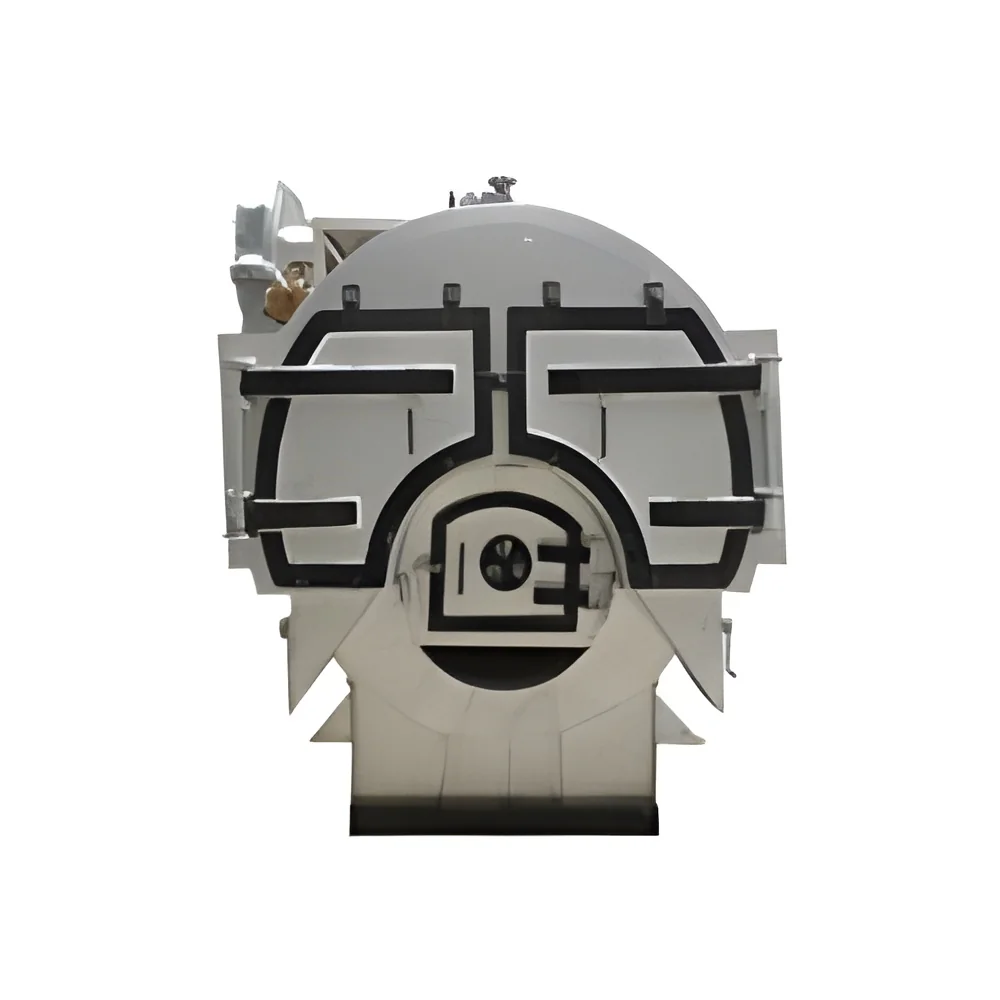
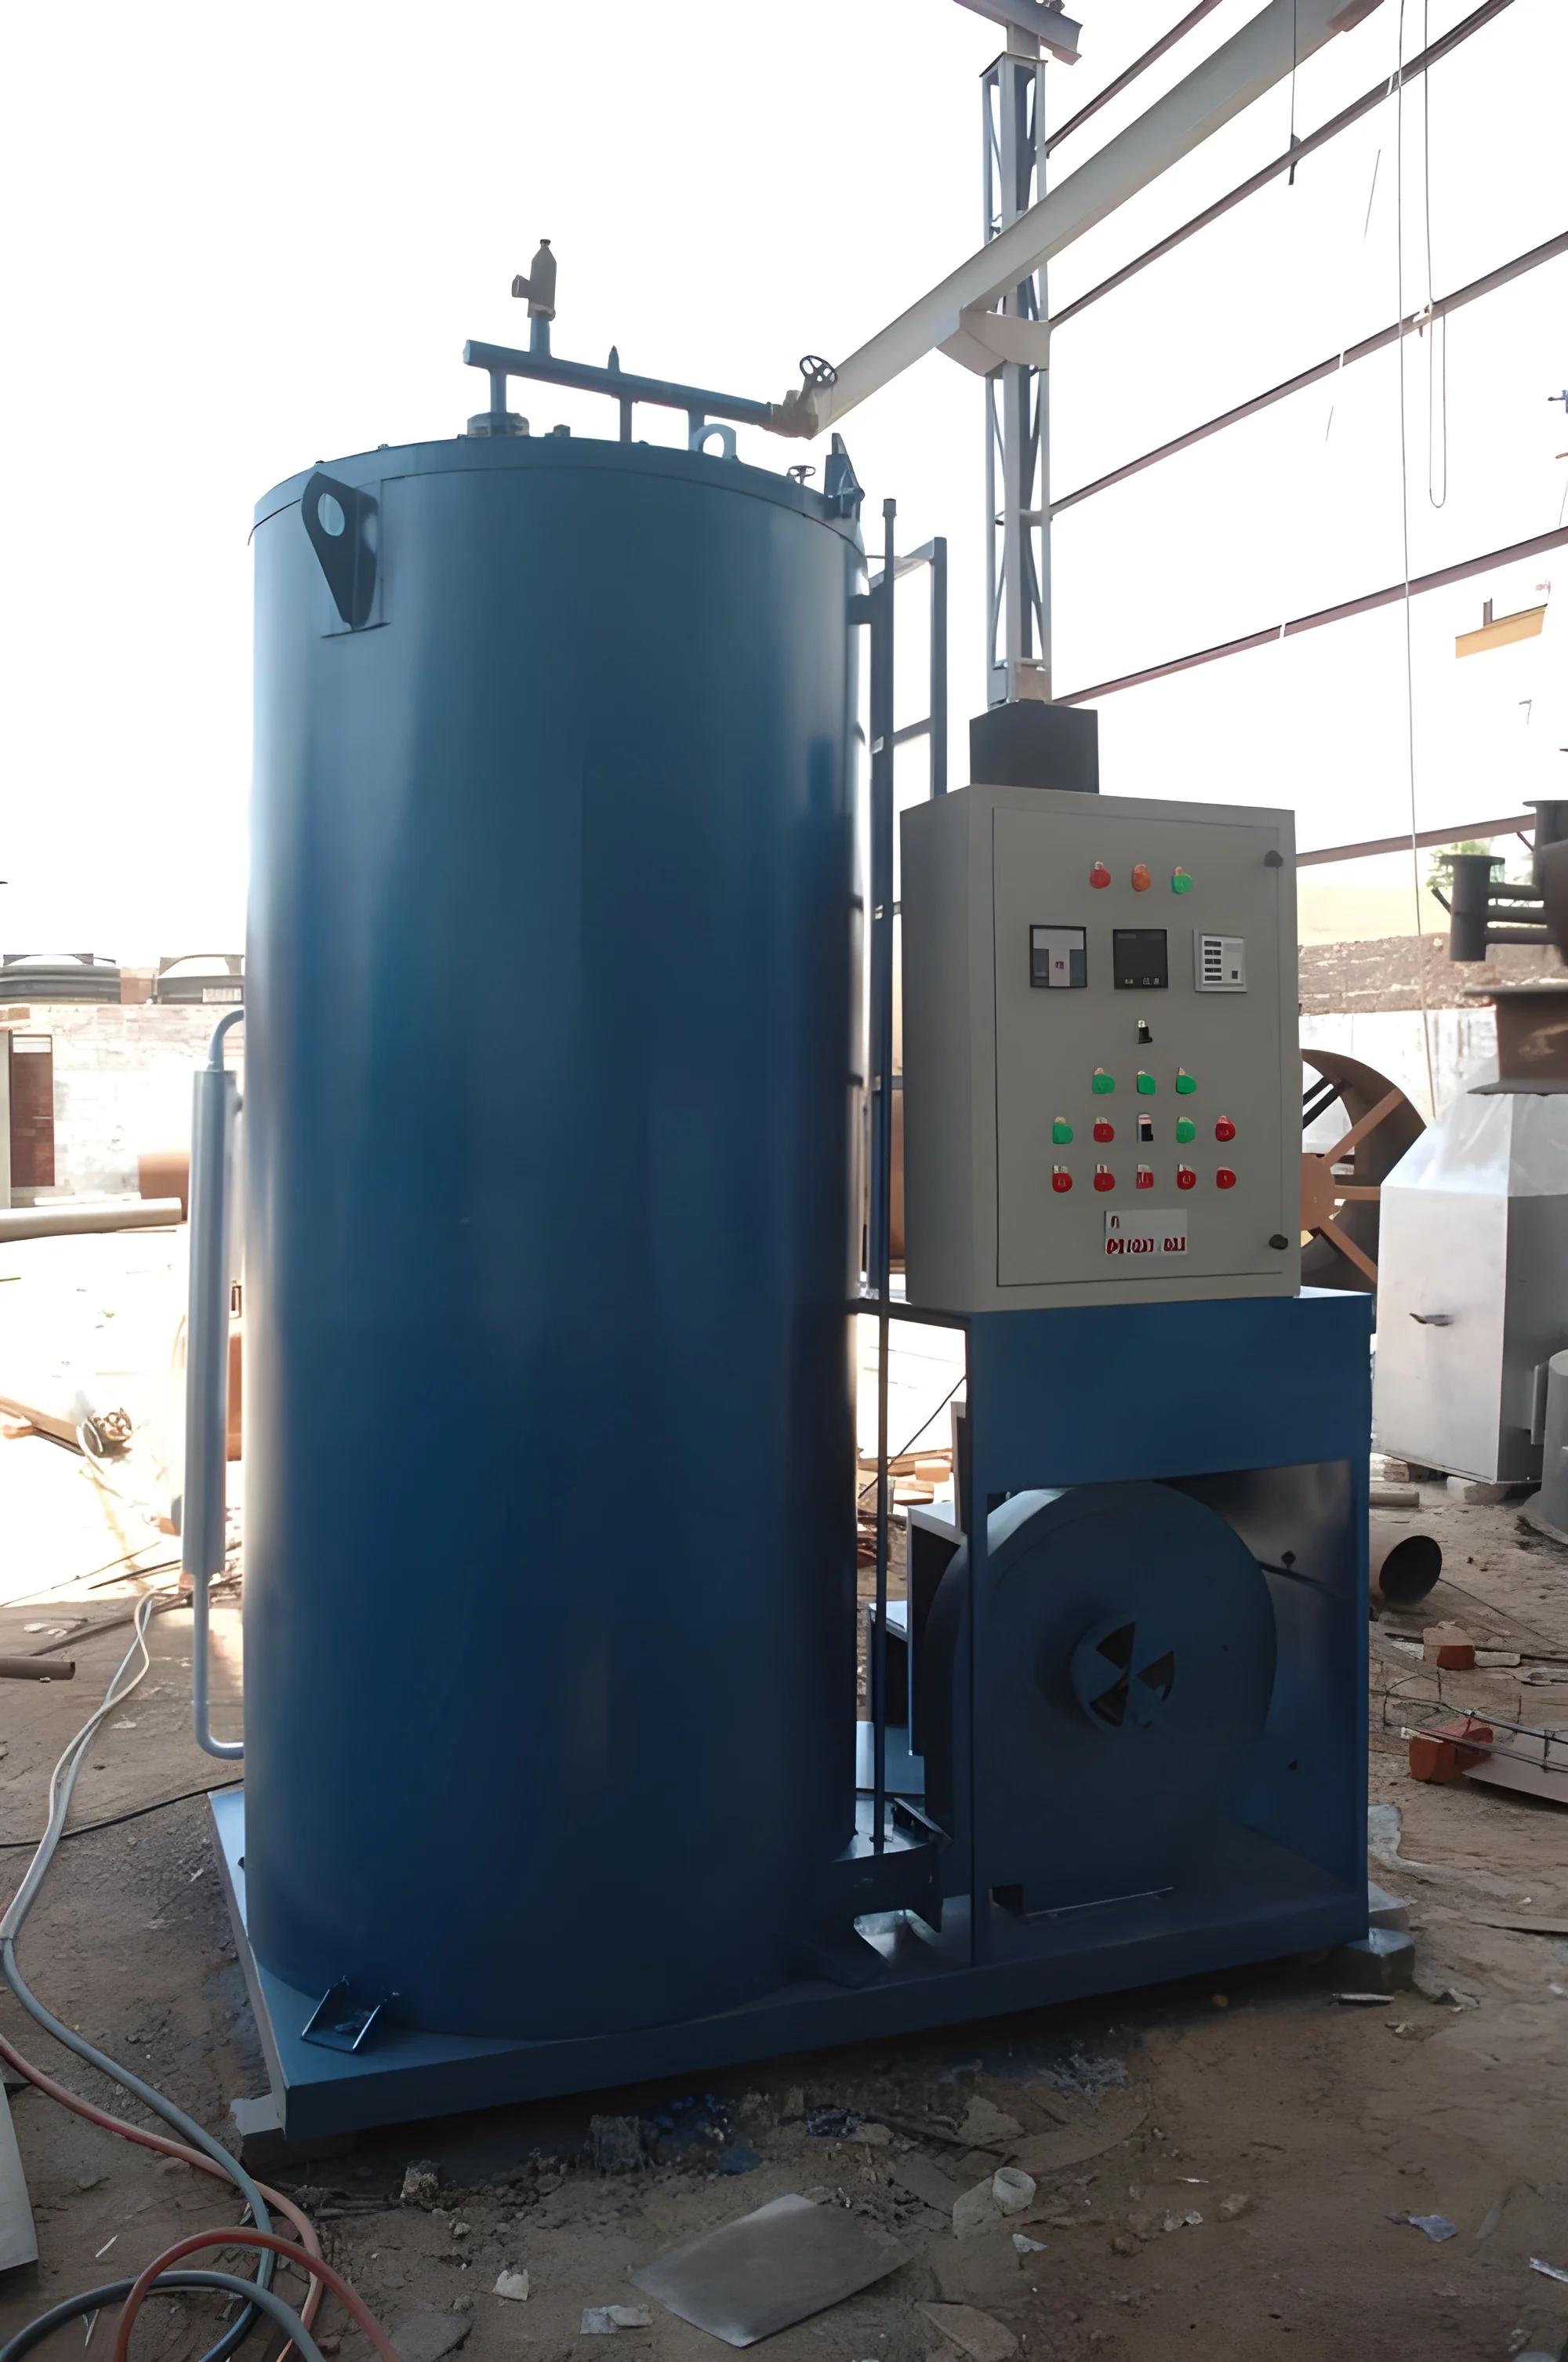
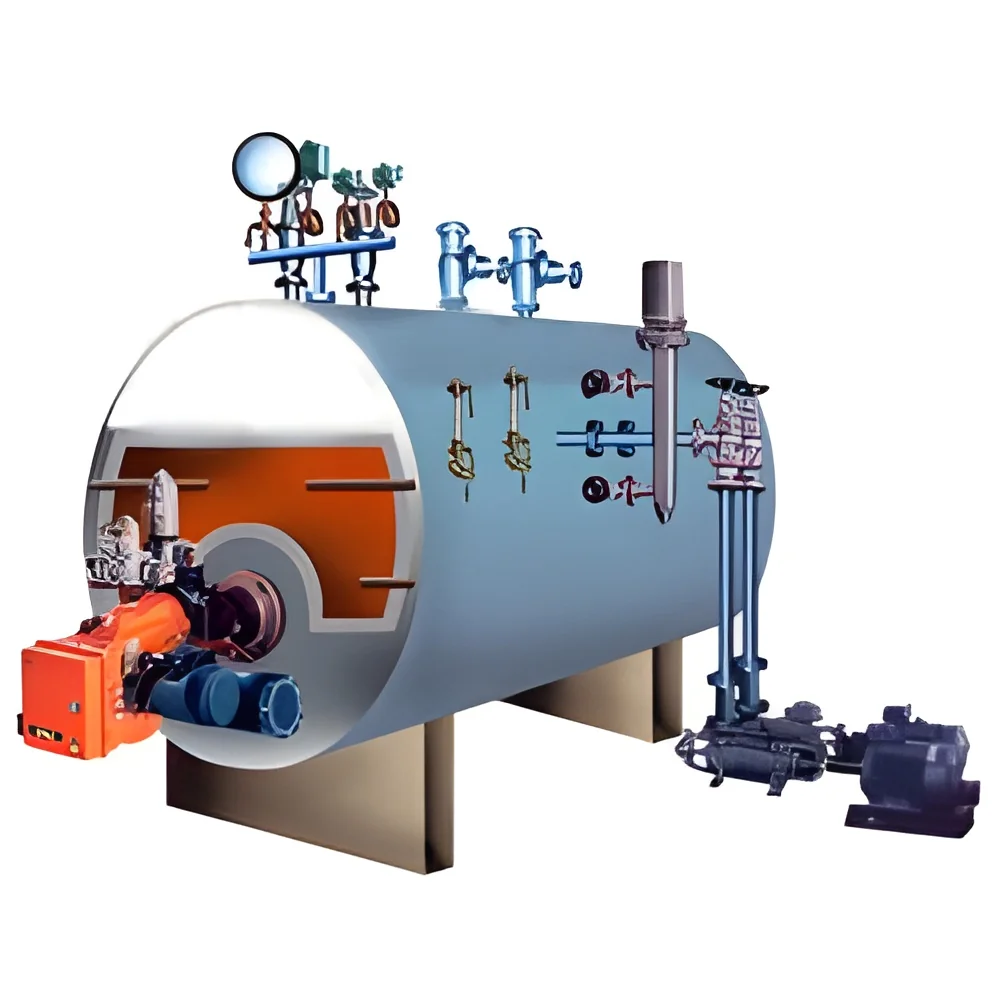
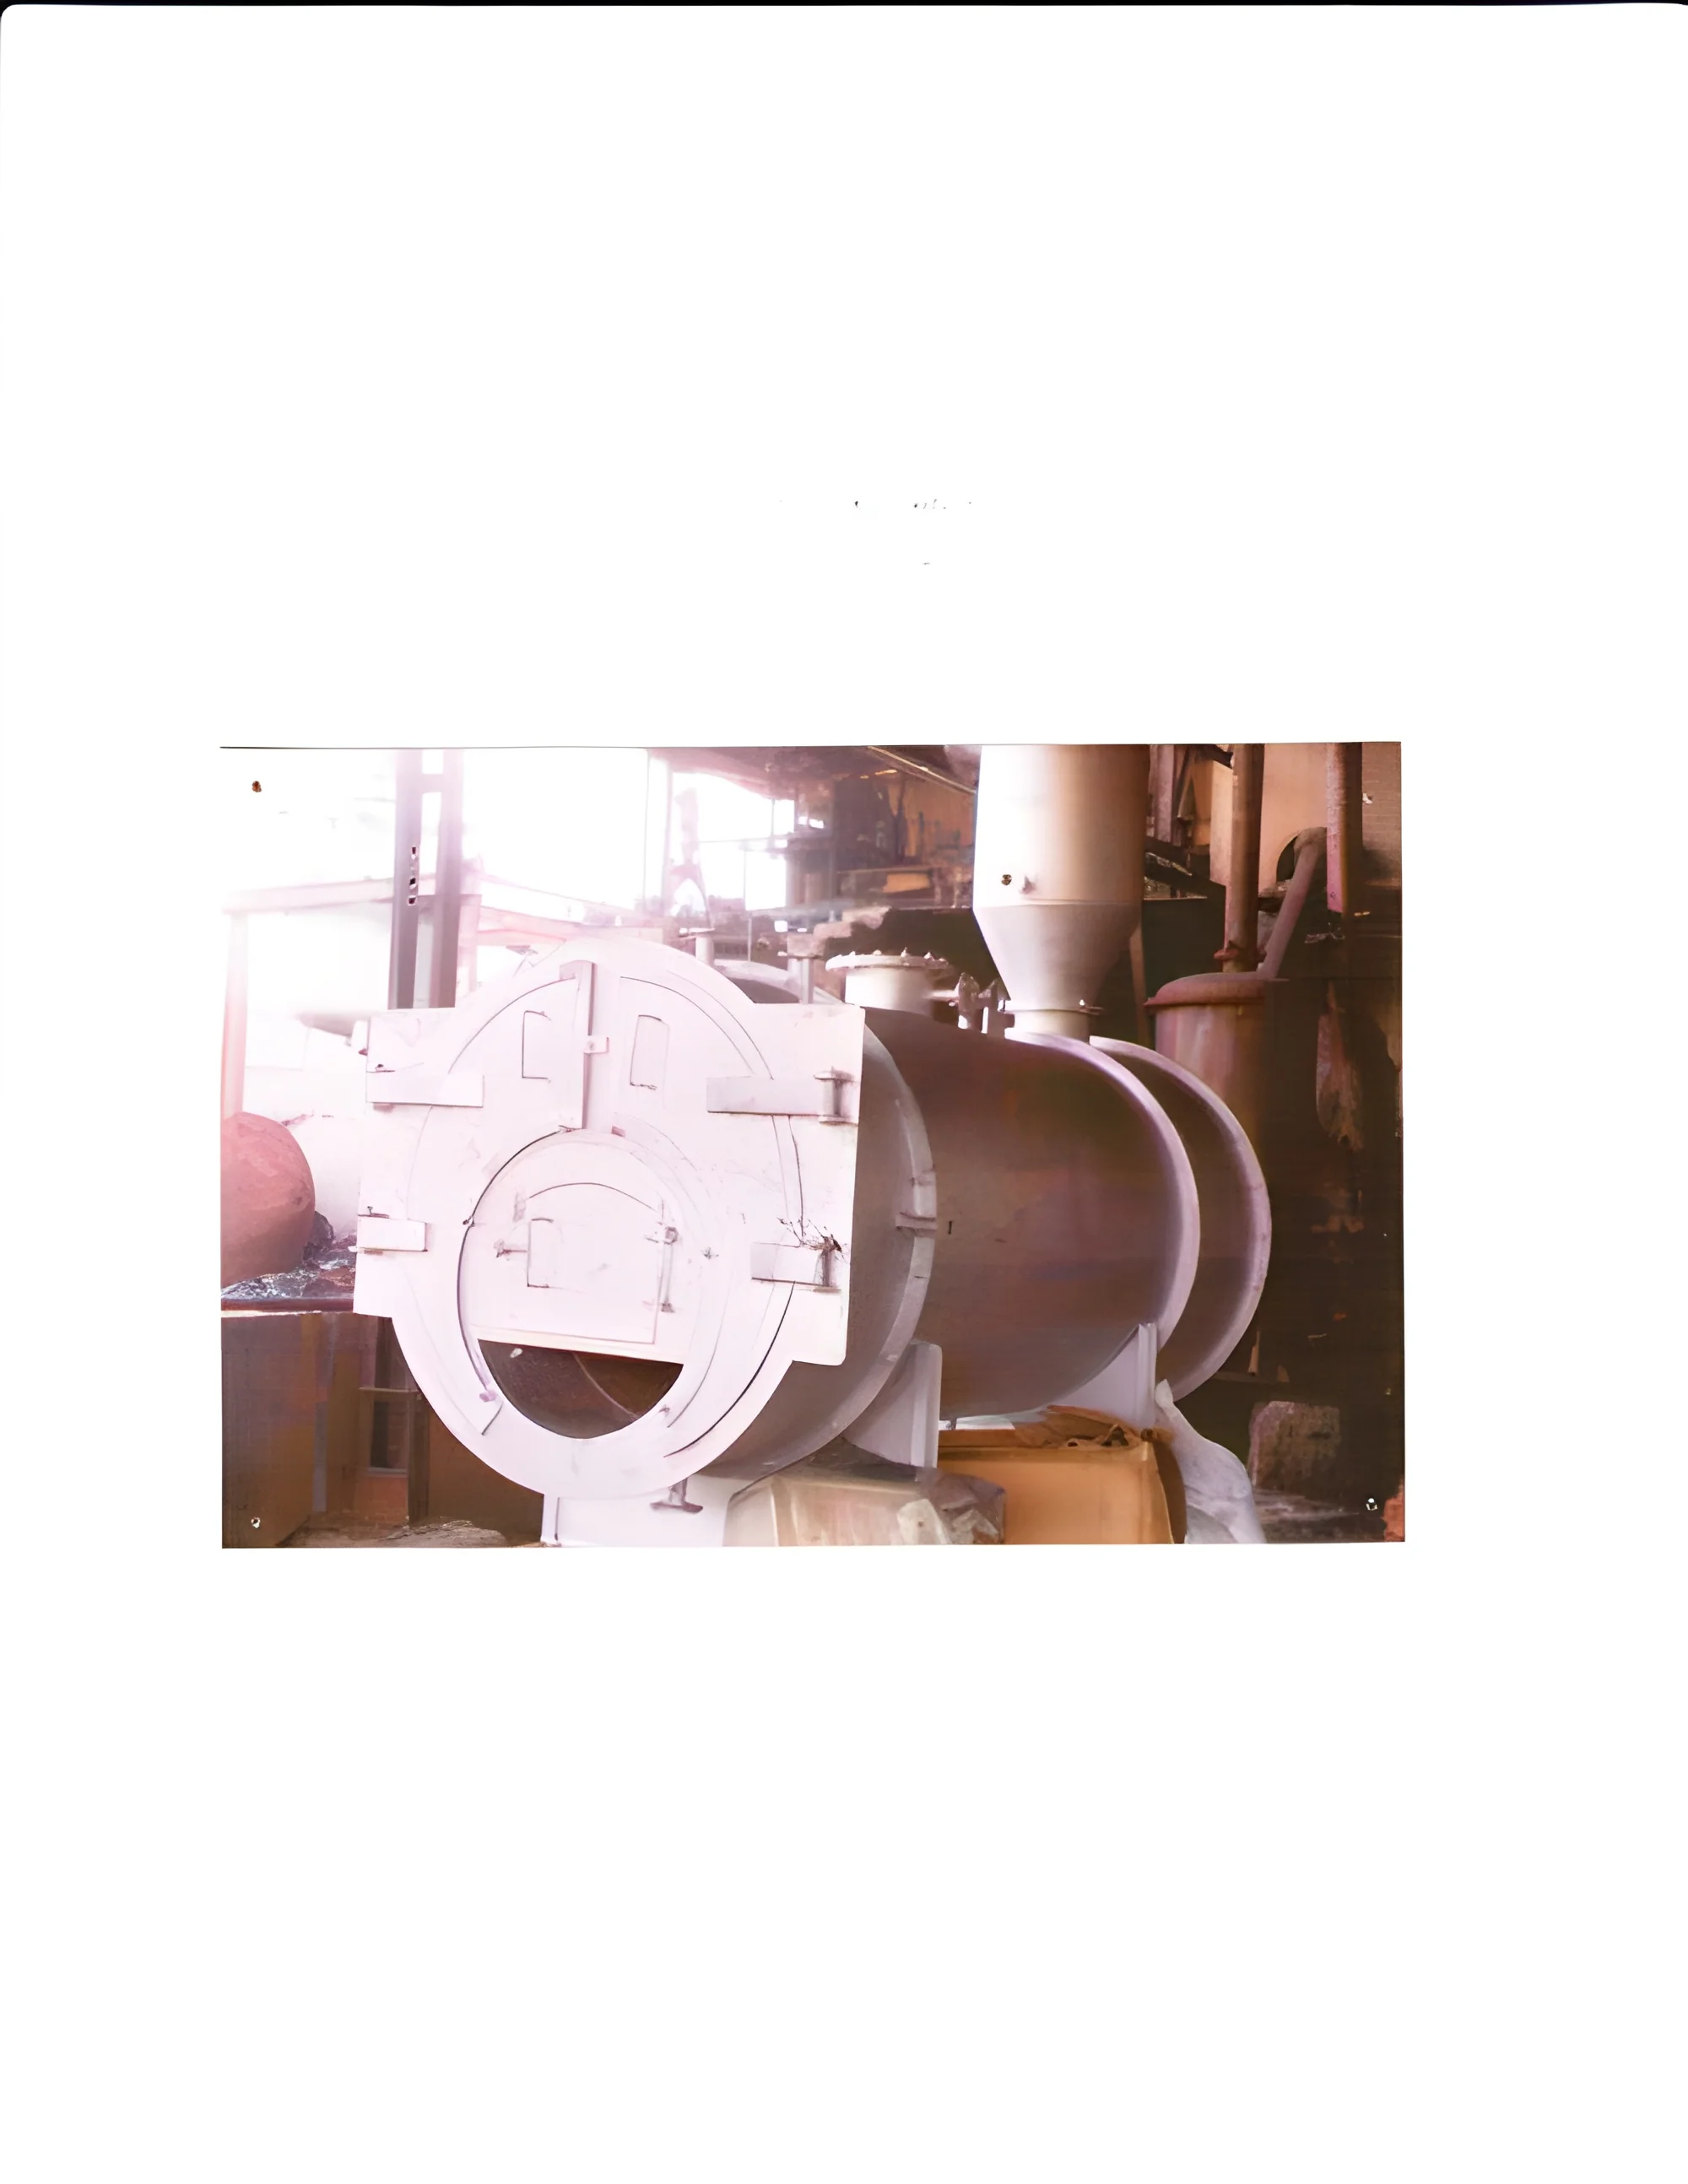
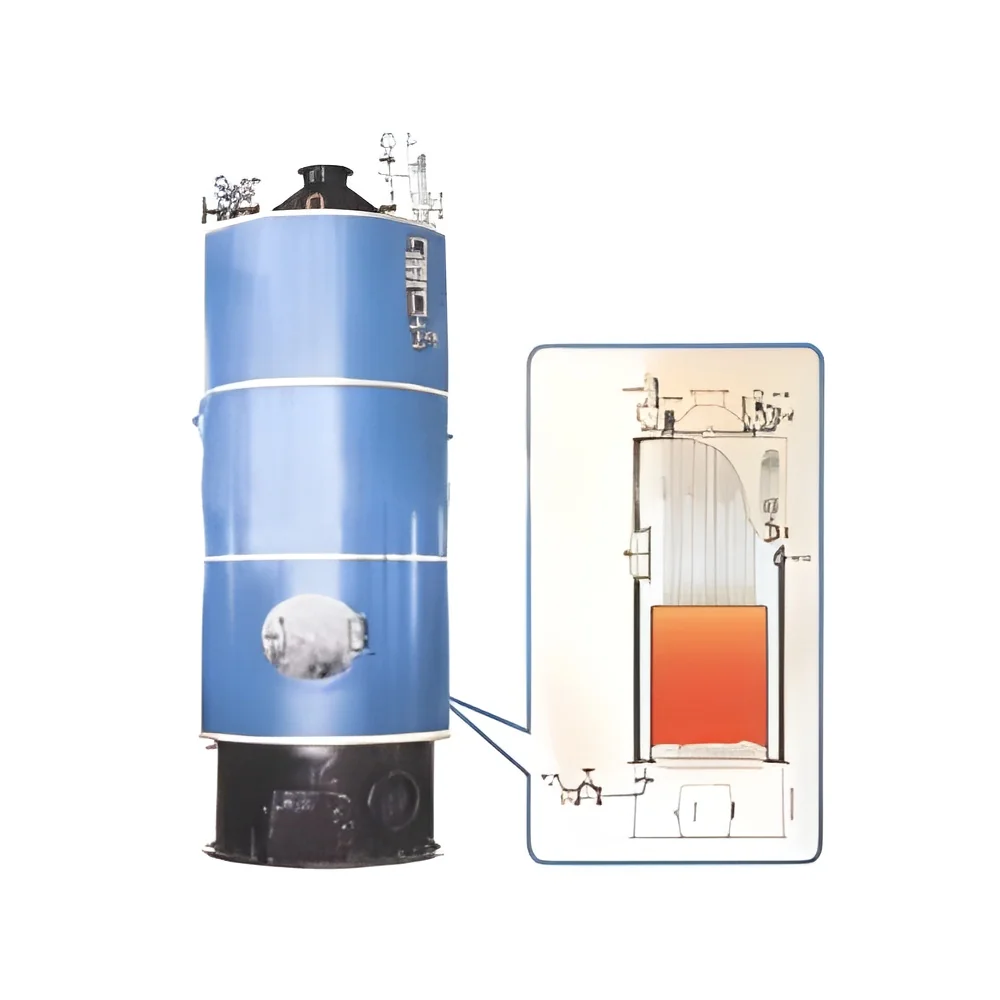
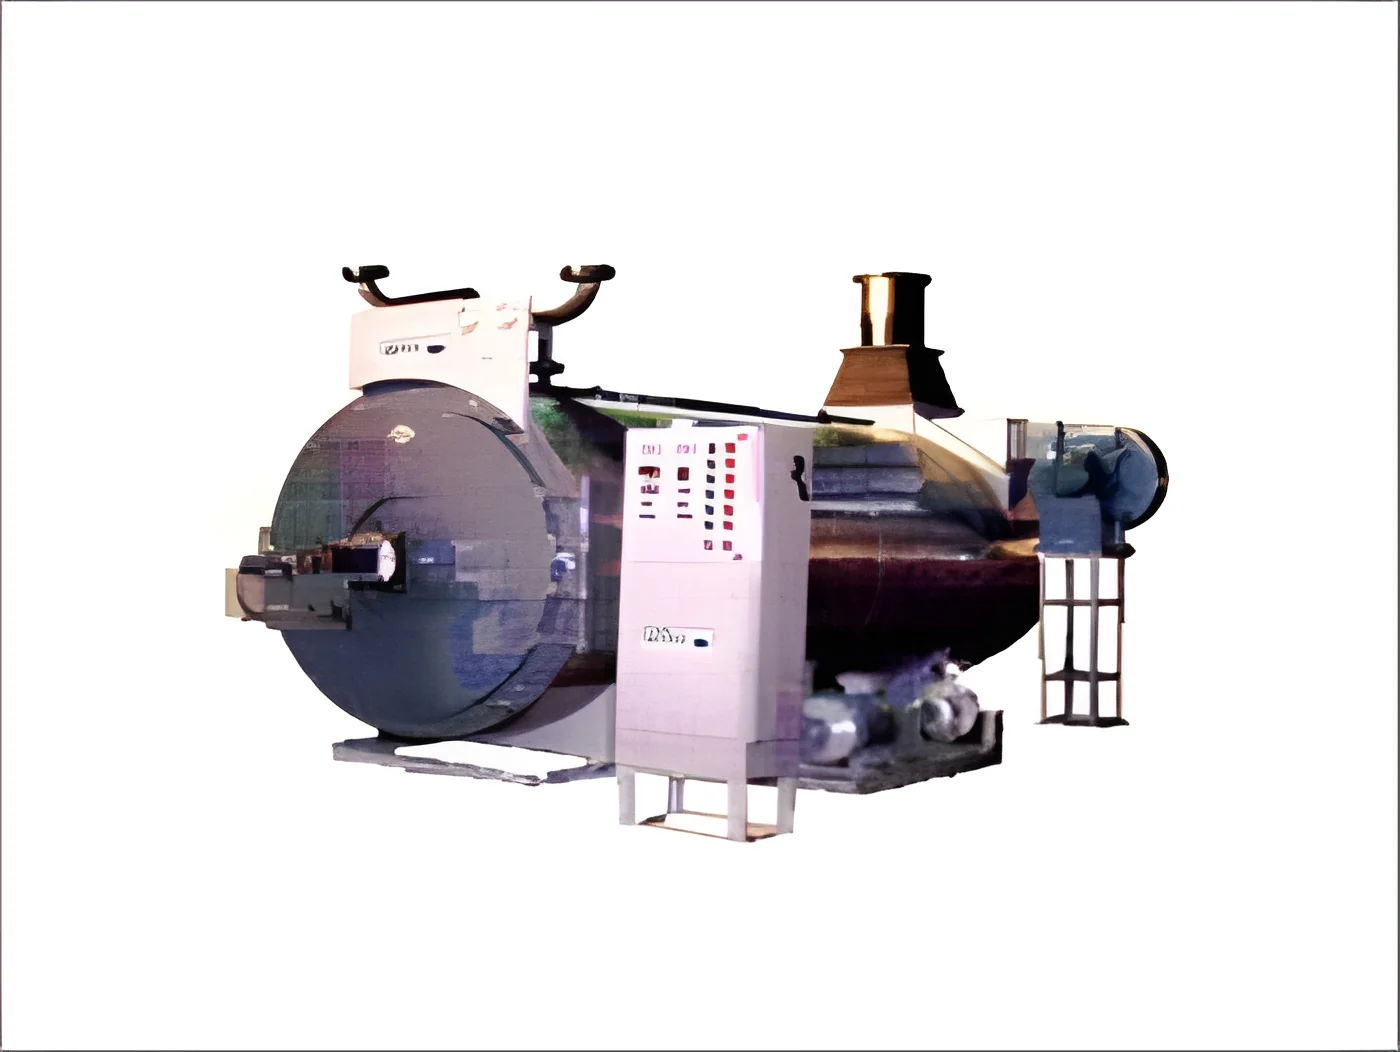
Heat-Max Engineering specializes in manufacturing premium non-IBR oil fired steam boilers designed for industrial applications requiring reliable thermal energy. Our boilers are engineered to deliver instant steam generation with higher thermal efficiency, ensuring optimal performance from startup. The systems feature fully automatic operation that minimizes manual intervention while maintaining consistent steam output for continuous processes. Each unit incorporates comprehensive safety instruments and tools that ensure secure, long-term operation, adhering to industry safety standards without the complexity of IBR certification. The compact yet robust construction allows for space-efficient installation while withstanding the rigors of demanding industrial environments, providing a durable solution for steam generation needs.

These oil fired boilers serve critical functions across multiple industrial sectors where steam is integral to core operations. In food processing, they delive...
Heat-Max Engineering specializes in manufacturing premium non-IBR oil fired steam boilers designed for industrial applications requiring reliable thermal energy. Our boilers are engineered to deliver instant steam generation with higher thermal efficiency, ensuring optimal performance from startup. The systems feature fully automatic operation that minimizes manual intervention while maintaining consistent steam output for continuous processes. Each unit incorporates comprehensive safety instruments and tools that ensure secure, long-term operation, adhering to industry safety standards without the complexity of IBR certification. The compact yet robust construction allows for space-efficient installation while withstanding the rigors of demanding industrial environments, providing a durable solution for steam generation needs.

These oil fired boilers serve critical functions across multiple industrial sectors where steam is integral to core operations. In food processing, they deliver essential steam for cooking, sterilization, and sanitation processes that meet hygiene standards. Textile manufacturers utilize them for precise temperature control in dyeing, drying, and finishing operations that determine product quality. Chemical production facilities depend on these boilers for maintaining consistent process heating and supporting chemical reactions. Pharmaceutical companies implement them in critical sterilization and purification processes where steam quality directly impacts product safety. Large commercial operations, including hospitality and healthcare facilities, rely on these systems for laundry services and heating applications that demand uninterrupted thermal energy supply.

The business value of Heat-Max oil fired boilers extends beyond initial acquisition through significant operational savings and enhanced productivity. Their higher efficiency design reduces fuel consumption, lowering long-term energy expenses and improving cost-effectiveness. Fully automatic operation decreases labor requirements while instant steam generation minimizes production downtime between cycles. Built-in reliability ensures consistent performance that supports continuous manufacturing without unexpected interruptions, protecting production schedules. The exemption from IBR regulations simplifies compliance while maintaining all necessary safety protocols, reducing administrative overhead. These boilers provide adaptable thermal solutions that integrate seamlessly into existing operations, delivering dependable steam that supports business continuity and process consistency.

Key Features:
- Instant steam generation capability for immediate operational readiness
- Fully automatic operation system requiring minimal manual intervention
- Non-IBR design exempt from complex certification requirements
- Comprehensive safety instrument package for secure long-term operation
- Compact and robust construction for space-efficient, durable installation

Benefits:
- Higher thermal efficiency reduces fuel consumption and operating costs
- Reliable performance ensures continuous steam supply for production processes
- Simplified compliance with safety standards without IBR certification complexity
- Reduced labor requirements through fully automated system operation
- Durable construction provides long service life in demanding industrial environments
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Heat-Max oil fired boilers provide dependable steam generation for continuous industrial operations where consistent thermal energy is essential. Engineered for demanding environments, these systems support manufacturing plants and processing facilities by ensuring a reliable steam supply that maintains production efficiency and operational flow without interruption.
These versatile boilers serve a wide range of industries, including food processing, textile manufacturing, chemical production, pharmaceuticals, and large commercial establishments. Their robust design and automated operation make them suitable for applications requiring precise temperature control and high-volume steam output, adapting to various operational scales and specific process requirements.
- Food processing plants for cooking, sterilization, and equipment cleaning cycles
- Textile manufacturing units for fabric dyeing, drying, and finishing operations
- Chemical production facilities for maintaining process heat and reaction temperatures
- Pharmaceutical companies for sterilization processes and clean steam requirements
- Large commercial laundries in hotels and hospitals for high-volume washing and drying
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Heat Max Engineering, Gujarat
 Gujarat, India
Manufacturer•Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Main Markets
South Asia
Industrial Oil Fired Boilers For Steam Generation With Automation
Heat-Max Engineering Oil Fired Boilers deliver instant steam generation with full automation for industrial processes. These high-efficiency, non-IBR boilers offer superior safety and reliable thermal energy for manufacturing and processing applications.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Heat Max Engineering
 Gujarat, India
Manufacturer