IN
₹
Apparel & Fashion
Description
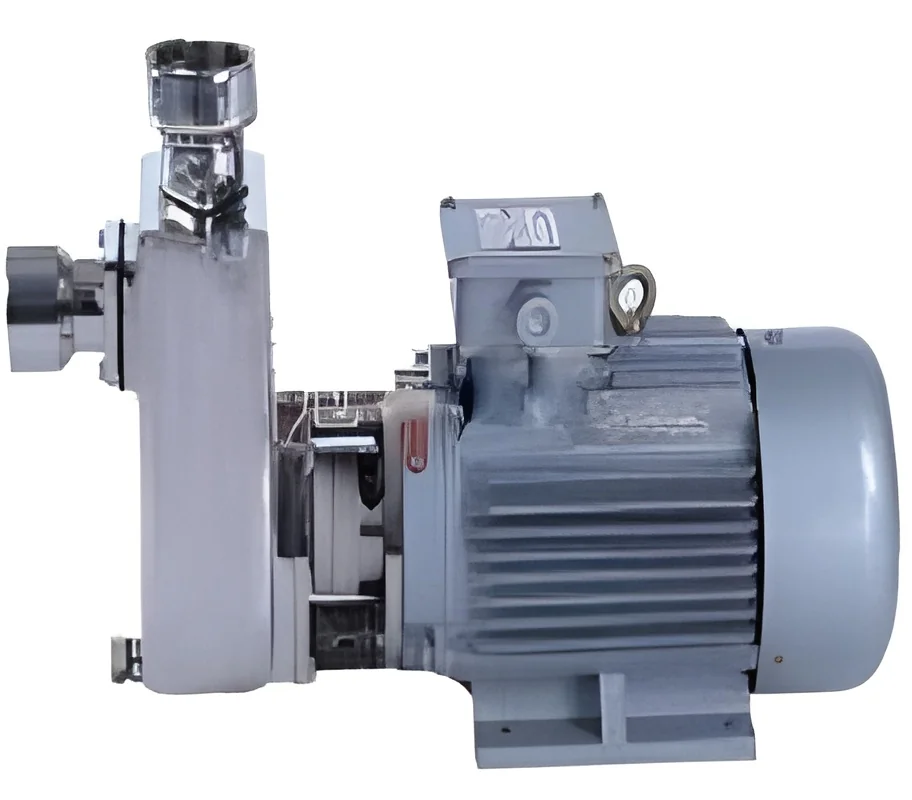
Our industrial oil and chemical pumps are engineered for demanding applications where reliability and performance are essential. These robust pumps are constructed with premium materials that withstand aggressive chemicals, high temperatures, and continuous operation cycles. Designed with input from industry professionals, they feature advanced sealing technology and corrosion-resistant components to match specific operational requirements. Whether handling volatile petroleum products or corrosive industrial chemicals, these pumps deliver consistent performance while maintaining strict safety standards and operational efficiency. Their durable construction ensures they can handle the toughest fluid transfer challenges without compromising on performance or safety.

These pumps serve critical functions across multiple industries including petrochemical refining, pharmaceutical manufacturing, chemical processing, automotive production, and wastewater treatment facilities. In refineries, ...
Our industrial oil and chemical pumps are engineered for demanding applications where reliability and performance are essential. These robust pumps are constructed with premium materials that withstand aggressive chemicals, high temperatures, and continuous operation cycles. Designed with input from industry professionals, they feature advanced sealing technology and corrosion-resistant components to match specific operational requirements. Whether handling volatile petroleum products or corrosive industrial chemicals, these pumps deliver consistent performance while maintaining strict safety standards and operational efficiency. Their durable construction ensures they can handle the toughest fluid transfer challenges without compromising on performance or safety.

These pumps serve critical functions across multiple industries including petrochemical refining, pharmaceutical manufacturing, chemical processing, automotive production, and wastewater treatment facilities. In refineries, they handle crude oil and refined products transfer between storage tanks and loading terminals. Chemical plants utilize them for transferring acids, solvents, and reactive compounds through production processes. Manufacturing facilities rely on them for coolant circulation, lubricant transfer, and waste fluid handling. The pumps are equally effective in marine applications for bilge pumping and fuel transfer, as well as in agricultural operations for fertilizer and pesticide handling. Their versatility makes them suitable for diverse industrial settings with varying fluid transfer needs.

The value of these industrial pumps lies in their exceptional reliability, reduced maintenance requirements, and long service life that directly impact operational costs and productivity. Their leak-proof design and safety features minimize environmental risks and compliance issues while protecting workforce safety. The robust construction allows businesses to achieve optimal performance without over-engineering. With superior quality and proven durability, these pumps represent a smart investment that reduces downtime, maintenance costs, and replacement frequency while ensuring consistent process performance. Their design focuses on delivering maximum uptime and efficiency for operations that cannot afford equipment failures or performance inconsistencies.

Key Features:
- Corrosion-resistant construction with premium materials for extended service life
- Advanced mechanical sealing system preventing leaks and ensuring operational safety
- Engineered to handle various flow rates and pressure requirements for different applications
- Robust motor design capable of handling viscous fluids and continuous operation cycles
- Temperature-resistant components suitable for handling hot fluids and extreme conditions

Benefits:
- Extended equipment life through corrosion-resistant materials and durable construction
- Enhanced safety with leak prevention systems and reliable performance in hazardous environments
- Operational flexibility to handle diverse fluids including fuels, solvents, acids, and viscous materials
- Reduced maintenance requirements and downtime through robust design and quality components
- Consistent performance in extreme conditions including high temperatures and continuous operation
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
These heavy-duty pumps are engineered for demanding industrial environments where reliability and safety are critical. They handle aggressive fluids including petroleum products, solvents, acids, and alkaline solutions with consistent performance and minimal maintenance, ensuring continuous operations without interruption. Built to withstand harsh conditions, they provide dependable fluid transfer for various industrial processes where equipment failure is not an option.
These pumps serve essential functions in chemical processing plants, refineries, manufacturing facilities, and bulk storage operations. They meet strict industry standards for leak prevention, corrosion resistance, and operational safety while maintaining efficient fluid transfer capabilities in both loading/unloading and process applications. Their robust design ensures they perform reliably even when handling challenging fluids that would degrade lesser equipment over time.
- Transferring petroleum products and fuels between storage tanks and transport vehicles
- Handling aggressive chemicals and solvents in pharmaceutical manufacturing processes
- Circulating acids and corrosive fluids in metal treatment and electroplating facilities
- Loading and unloading viscous industrial fluids and lubricants in bulk operations
- Transferring wastewater and treatment chemicals in industrial processing plants
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
A One Industries, New Delhi
 New Delhi, India
Industrial Equipment & Machinery•Manufacturer•Distributor / Wholesaler
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Industrial Oil And Chemical Pumps For Durable Fluid Transfer
Industrial oil and chemical pumps for durable fluid transfer of fuels, solvents, acids, and viscous fluids across manufacturing, petrochemical, and processing industries.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
A One Industries
 New Delhi, India
Industrial Equipment & MachineryManufacturer