IN
₹
Apparel & Fashion
Description
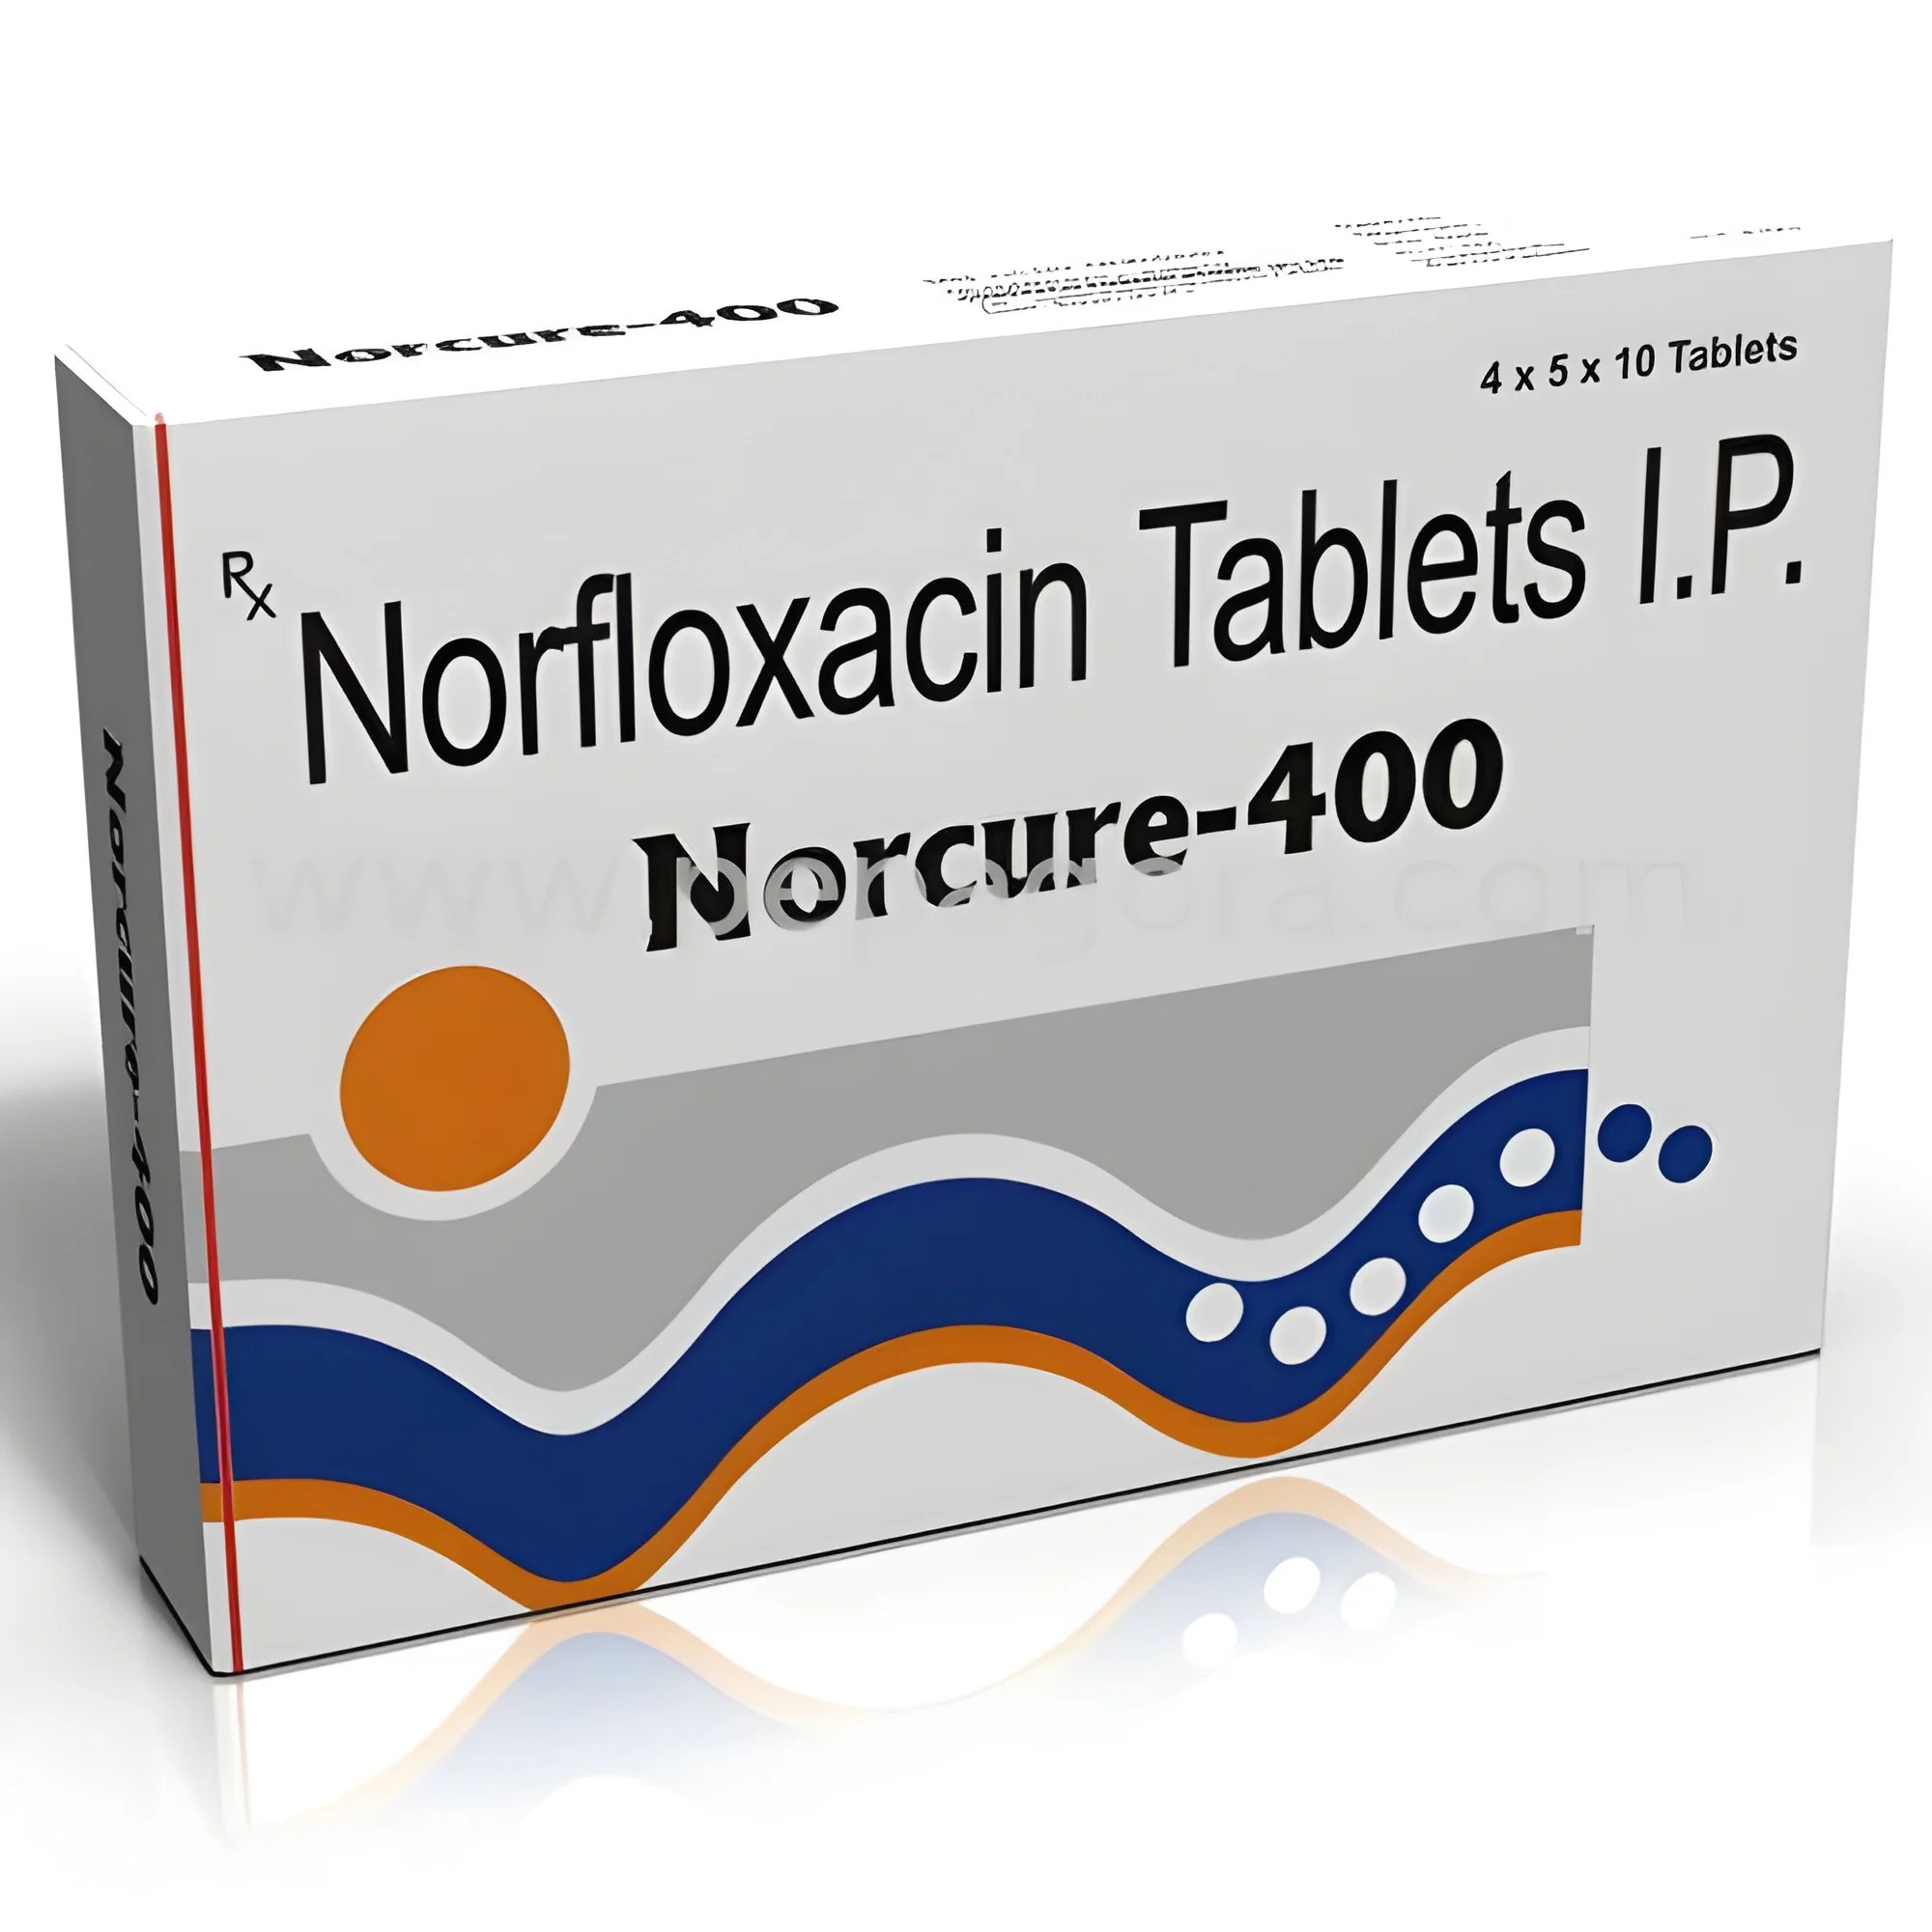
Norcure 400 represents pharmaceutical-grade antibacterial capsules manufactured to 99.90% purity standards for reliable therapeutic applications. These capsules deliver high effectiveness against bacterial infections while maintaining a safety profile with no reported side effects, ensuring patient well-being and treatment confidence. The medicine-grade quality is verified through rigorous manufacturing processes, resulting in a product with extended shelf life that maintains potency throughout storage and distribution cycles. Available in both round and oval forms, these capsules provide flexibility for different pharmaceutical manufacturing requirements and patient preferences.

This antibacterial product serves pharmaceutical manufacturers producing antibiotic medications for various healthcare sectors. Hospitals and clinics utilize medications containing this formulation for treating respiratory, urinary, and skin infections, while distributors supply these treatments to pharmacies...
Norcure 400 represents pharmaceutical-grade antibacterial capsules manufactured to 99.90% purity standards for reliable therapeutic applications. These capsules deliver high effectiveness against bacterial infections while maintaining a safety profile with no reported side effects, ensuring patient well-being and treatment confidence. The medicine-grade quality is verified through rigorous manufacturing processes, resulting in a product with extended shelf life that maintains potency throughout storage and distribution cycles. Available in both round and oval forms, these capsules provide flexibility for different pharmaceutical manufacturing requirements and patient preferences.

This antibacterial product serves pharmaceutical manufacturers producing antibiotic medications for various healthcare sectors. Hospitals and clinics utilize medications containing this formulation for treating respiratory, urinary, and skin infections, while distributors supply these treatments to pharmacies and healthcare facilities. The product's consistency and reliability make it suitable for integration into diverse therapeutic protocols, supporting infection management across different medical specialties and healthcare delivery systems. Its application extends to both institutional and community healthcare settings where verified antibacterial treatments are essential.

The business value of Norcure 400 lies in its combination of therapeutic efficacy and supply chain reliability. The high purity level ensures consistent manufacturing outcomes, while the absence of side effects reduces treatment complications and associated costs. Long shelf life minimizes product waste and inventory management challenges, providing economic advantages throughout the distribution chain. The product's proven effectiveness supports positive treatment outcomes, enhancing customer satisfaction and repeat business opportunities for partners. These factors create a dependable foundation for pharmaceutical businesses seeking quality antibacterial ingredients.

Key Features:
- 99.90% pure antibacterial formulation meeting medicine-grade standards
- High effectiveness against bacterial infections with no reported side effects
- Extended shelf life maintaining therapeutic potency throughout storage
- Available in both round and oval capsule forms for manufacturing flexibility
- Strong and sturdy construction ensuring product integrity during handling

Benefits:
- Consistent therapeutic performance supporting reliable treatment outcomes
- Reduced treatment risks through verified safety profile and purity
- Inventory efficiency with long shelf life minimizing product waste
- Manufacturing flexibility with multiple capsule form options
- Supply chain reliability with stable formulation and quality assurance
Specifications
| Key Attributes | |
|---|---|
| Type | Norcure |
| Dosage Form | Capsules |
| Shape | Round Or Oval |
| Sample | Available |
| Feeling | Warm/Cold |
| Grade Standard | Medicine Grade |
| Form | Capsules |
| Purity | 99.90% |
| Function | Antibacterial Drugs |
| Price | Reasonable |
| Quality | Good |
| Shelf Life | Long |
| Supply Type | OEM |
| Construction | Strong And Sturdy |
| Side Effects | No |
| Effectiveness | High |
| Use | Pharmaceutical |
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Norcure 400 antibacterial capsules serve as a critical component in pharmaceutical production for creating effective infection treatments. Their 99.90% purity and medicine-grade standard ensure consistent therapeutic performance, making them suitable for manufacturing finished dosage forms that meet strict regulatory requirements across global markets. The product's reliability supports production schedules and quality assurance protocols in pharmaceutical facilities.
This antibacterial formulation meets the needs of distributors and wholesalers requiring dependable supply for healthcare systems. The long shelf life and stable formulation reduce inventory concerns, while the proven effectiveness supports treatment protocols in various medical settings. Available samples allow for quality verification before large-scale procurement, ensuring partners receive products that match their specifications and market demands.
- Manufacturing finished antibiotic medications for respiratory infections
- Production of urinary tract infection treatments for clinical distribution
- Formulating skin and soft tissue infection therapies for medical use
- Creating surgical prophylaxis medications for hospital pharmacies
- Developing general antibacterial treatments for healthcare facilities
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile

Curetech Formulations Pvt Ltd, Himachal Pradesh
 Himachal Pradesh, India
Health & Personal Care•Manufacturer•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Main Markets
North America
South America
Mid East
Southern Europe
Pharmaceutical OEM Norcure 400 Antibacterial Capsules 99.90% Pure
Norcure 400 antibacterial capsules offer 99.90% pure medicine-grade quality for pharmaceutical manufacturing, featuring high effectiveness, no side effects, and long shelf life for reliable OEM supply.
Min. Order Quantity: 100 Pieces
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Curetech Formulations Pvt Ltd
 Himachal Pradesh, India
Health & Personal CareManufacturer