IN
₹
Description
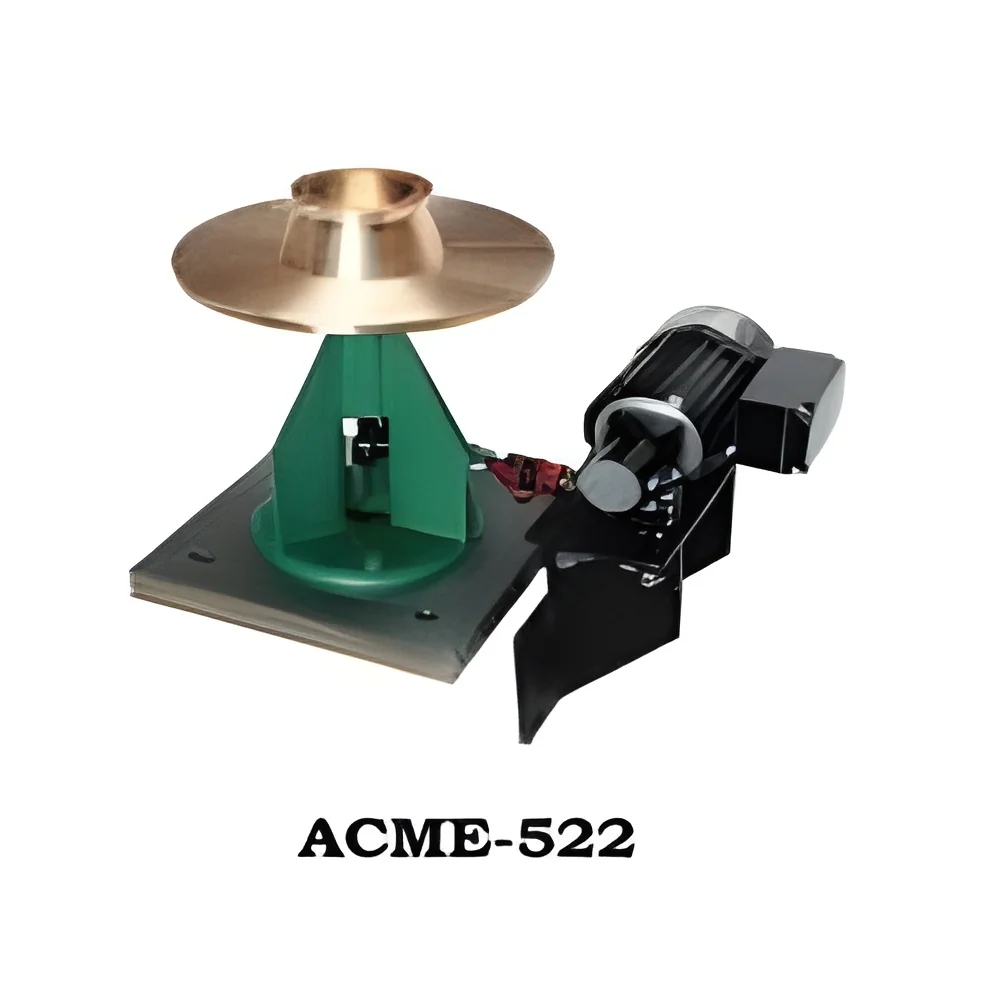
Industrial motorized flow tables are engineered to enhance material handling operations with automated, precision-controlled movement for various manufacturing applications. These tables feature robust construction, precision motor drives, and customizable surfaces to support loads ranging from light components to heavy assemblies. Designed for seamless integration into existing production lines, they offer adjustable speed controls, smooth operation, and reliable performance in demanding industrial environments. The tables improve workflow consistency, reduce operator fatigue, and minimize handling errors while providing the flexibility to adapt to specific operational requirements including size, load capacity, and control interfaces.

Multiple industries leverage motorized flow tables to optimize production efficiency and maintain quality standards. Automotive manufacturers utilize them for precise positioning during assembly and testing phases, while electronics manufacturers rely ...
Industrial motorized flow tables are engineered to enhance material handling operations with automated, precision-controlled movement for various manufacturing applications. These tables feature robust construction, precision motor drives, and customizable surfaces to support loads ranging from light components to heavy assemblies. Designed for seamless integration into existing production lines, they offer adjustable speed controls, smooth operation, and reliable performance in demanding industrial environments. The tables improve workflow consistency, reduce operator fatigue, and minimize handling errors while providing the flexibility to adapt to specific operational requirements including size, load capacity, and control interfaces.

Multiple industries leverage motorized flow tables to optimize production efficiency and maintain quality standards. Automotive manufacturers utilize them for precise positioning during assembly and testing phases, while electronics manufacturers rely on their vibration-free operation for handling delicate components. The food processing and pharmaceutical sectors benefit from their easy-to-clean surfaces and compliance with strict hygiene regulations. These tables are equally valuable in packaging facilities where they streamline product movement between various stages including sealing, labeling, and palletizing operations. Their adaptability makes them suitable for both high-volume production lines and specialized operations requiring exceptional precision and reliability.

Investing in motorized flow tables delivers substantial business value through enhanced productivity, reduced labor costs, and improved operational reliability. These systems are built to withstand continuous use, minimizing downtime and maintenance requirements while ensuring consistent performance. The customization capabilities allow them to meet exact operational needs whether for specific load capacities, speed requirements, or integration with other automation equipment. By automating material movement processes, businesses achieve greater operational consistency, faster cycle times, and higher output quality. The inherent reliability of these tables translates into long-term operational savings and strong return on investment, supported by durable components and engineering focused on industrial performance standards.

Key Features:
- Precision motor drive system for smooth and adjustable speed control
- Robust steel or aluminum construction ensuring durability and load capacity
- Customizable table surface sizes and materials to suit specific applications
- Easy integration with existing conveyor systems and automation setups
- Low maintenance design with reliable components for continuous operation

Benefits:
- Enhanced production efficiency through automated material handling
- Reduced labor costs and minimized manual handling errors
- Improved workflow consistency and operational reliability
- Adaptable to various industrial environments and requirements
- Long-term durability with minimal maintenance requirements
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Motorized flow tables streamline production by providing controlled movement for assembly, testing, and packaging operations. They are essential in manufacturing environments where consistent material flow and precise positioning are critical for maintaining efficiency and quality standards. These systems reduce manual handling, minimize errors, and adapt to various load capacities and speed requirements across different industrial settings.
Industries including automotive, electronics, food processing, and pharmaceuticals benefit from motorized flow tables due to their durability, precision, and automation capabilities. They support lean manufacturing principles by optimizing workflow, reducing cycle times, and integrating seamlessly with conveyor systems and robotic equipment for complete automation solutions. Their robust construction ensures reliable performance even in demanding production environments.
- Assembly line positioning for precise component placement in automotive manufacturing
- Quality control inspection stations with smooth, adjustable movement for thorough testing
- Packaging lines for transporting products between sealing, labeling, and boxing stages
- Electronics manufacturing for handling sensitive components with vibration-free operation
- Pharmaceutical production areas where hygienic, easy-to-clean surfaces meet compliance standards
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
ACME Scientific International, New Delhi
 New Delhi, India
Manufacturer•Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Industrial Motorized Flow Tables For Assembly And Packaging Automation
Industrial motorized flow tables automate material handling with precision control for assembly, packaging, and quality testing. Durable construction ensures reliable performance in demanding industrial environments with customizable options for specific applications.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
ACME Scientific International
 New Delhi, India
Manufacturer