IN
₹
Apparel & Fashion
Description
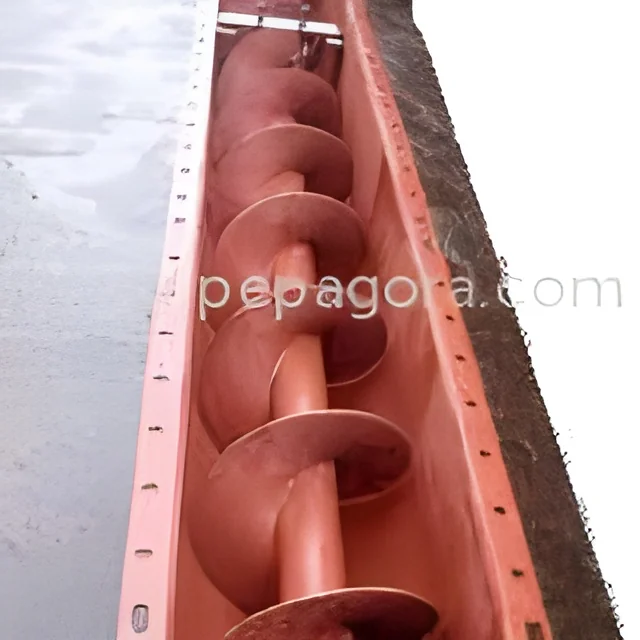
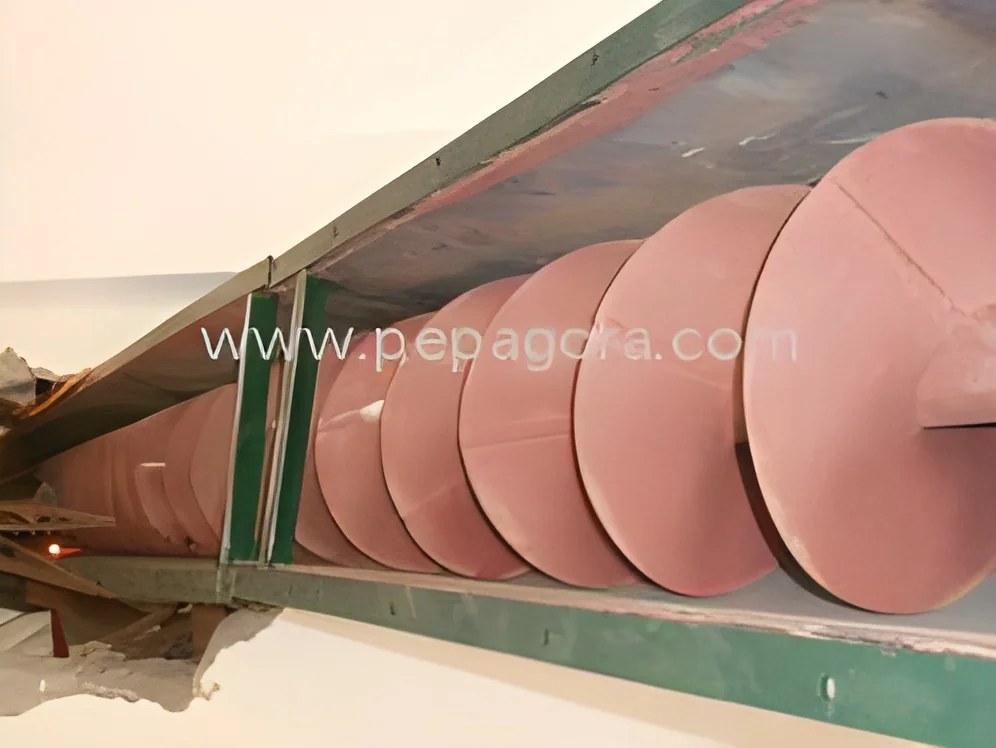
The Industrial Screw Conveyor System represents advanced material handling technology engineered for demanding industrial applications. Constructed from heat-resistant stainless steel, this conveyor delivers reliable performance when transporting various bulk materials including powders, granules, and processed substances. The robust screw mechanism ensures consistent material flow with minimal energy consumption, while the durable construction withstands continuous operation in challenging environments. Designed for easy integration into existing production lines, this system maintains structural integrity under heavy use while providing efficient material transfer between processing stages with minimal maintenance requirements.

This conveyor system serves critical functions across multiple industrial sectors where reliable material handling is essential. Food processing facilities benefit from its hygienic stainless steel construction and efficient transportation of ingredients betw...
The Industrial Screw Conveyor System represents advanced material handling technology engineered for demanding industrial applications. Constructed from heat-resistant stainless steel, this conveyor delivers reliable performance when transporting various bulk materials including powders, granules, and processed substances. The robust screw mechanism ensures consistent material flow with minimal energy consumption, while the durable construction withstands continuous operation in challenging environments. Designed for easy integration into existing production lines, this system maintains structural integrity under heavy use while providing efficient material transfer between processing stages with minimal maintenance requirements.

This conveyor system serves critical functions across multiple industrial sectors where reliable material handling is essential. Food processing facilities benefit from its hygienic stainless steel construction and efficient transportation of ingredients between production stages. Manufacturing plants utilize these conveyors for moving raw materials and components through assembly processes. Agricultural operations depend on them for handling grains and processed materials, while chemical plants value their corrosion-resistant properties. The heat-resistant design ensures stable performance in elevated temperature environments, making it suitable for applications involving heated materials or high-temperature processing areas.

Businesses implementing this Industrial Screw Conveyor System gain significant operational advantages through enhanced efficiency and reduced downtime. The reliable construction minimizes maintenance requirements while ensuring continuous operation, directly impacting productivity and operational costs. The durable stainless steel materials resist corrosion and wear, ensuring long-term performance and reducing replacement frequency. This equipment provides excellent return on investment through consistent performance, minimal operational interruptions, and adaptability to various material types and processing requirements, making it a valuable long-term asset for industrial operations.

Key Features:
- Heat-resistant stainless steel construction for durability in high-temperature environments
- Efficient screw conveyor mechanism for consistent material transportation
- Corrosion-resistant materials suitable for various industrial applications
- Robust design capable of handling powders, granules, and bulk materials
- Easy integration into existing production lines and material handling systems

Benefits:
- Reliable performance with minimal maintenance requirements and downtime
- Long service life due to durable, corrosion-resistant stainless steel construction
- Energy-efficient operation reducing overall operational costs
- Versatile handling of various material types from fine powders to granules
- Consistent material flow maintaining production efficiency and throughput
Specifications
| Key Attributes | |
|---|---|
| Material | Stainless Steel |
| Material Feature | Heat Resistant |
| Structure | Conveyor System |
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Our Industrial Screw Conveyor System delivers reliable material handling across diverse industrial environments. The heat-resistant stainless steel construction ensures consistent performance when moving powders, granules, and bulk materials between processing stages. This robust system maintains operational efficiency while withstanding demanding conditions, making it suitable for continuous production cycles and high-temperature applications where equipment reliability is critical for maintaining workflow and productivity standards.
The conveyor's versatile design adapts to various industrial layouts and material types, from fine food-grade powders to industrial raw materials. Its efficient screw mechanism provides controlled material flow with minimal energy consumption, reducing operational costs while maintaining throughput. The stainless steel composition resists corrosion and contamination, meeting strict hygiene requirements for sensitive applications while ensuring long-term durability in challenging manufacturing and processing environments.
- Food processing plants for hygienic transportation of ingredients and finished products
- Agricultural facilities for efficient handling of grains, seeds, and processed materials
- Manufacturing operations for reliable movement of raw materials and production components
- Chemical processing plants for safe transport of industrial powders and granules
- Recycling facilities for efficient handling of bulk materials and production waste
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Sri Aanoor Amman Engineerings, Tamil Nadu
 Tamil Nadu, India
Manufacturer•Distributor / Wholesaler
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Main Markets
Northern Europe
Southern Europe
South Asia
Industrial Screw Conveyor Heat Resistant Stainless Steel Conveyor System
Industrial Screw Conveyor made from heat-resistant stainless steel efficiently transports bulk materials for food processing, manufacturing, and agricultural applications with reliable performance and durable construction.
Min. Order Quantity: 1 piece
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Sri Aanoor Amman Engineerings
 Tamil Nadu, India
Manufacturer