IN
₹
Apparel & Fashion
Description
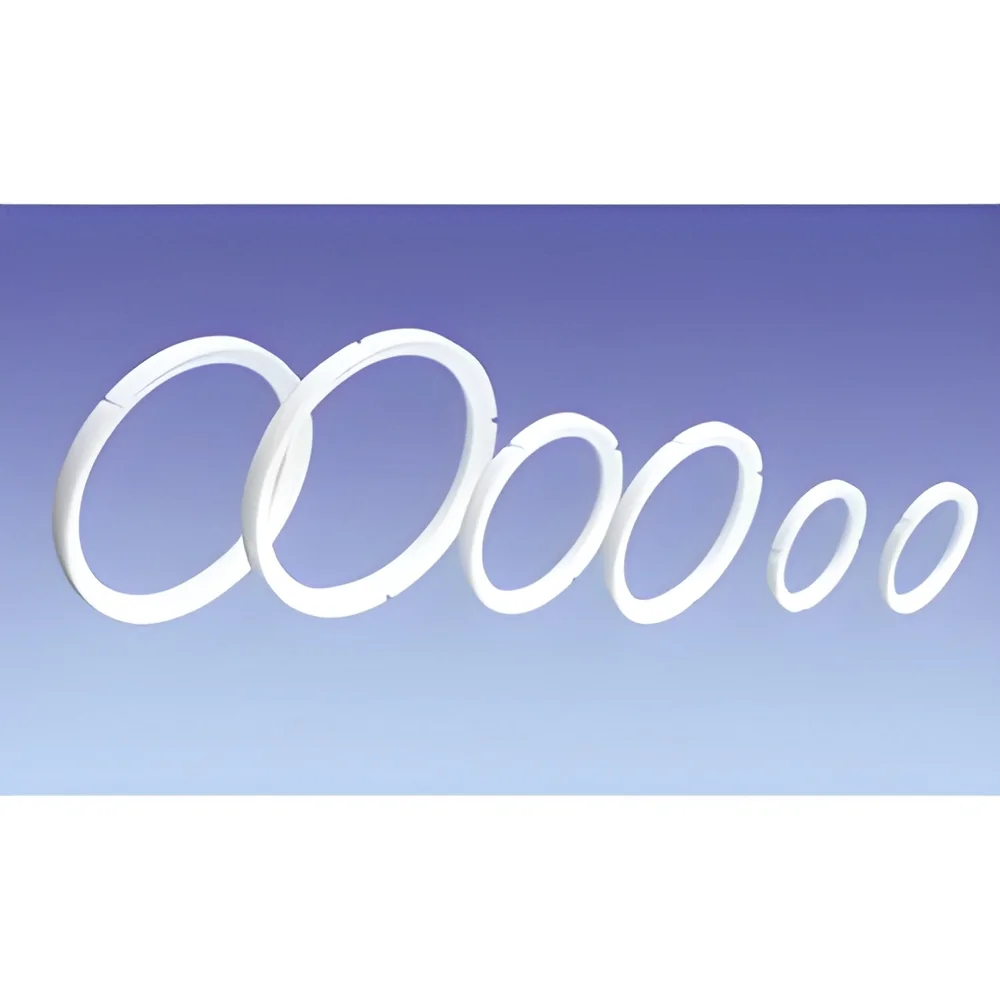
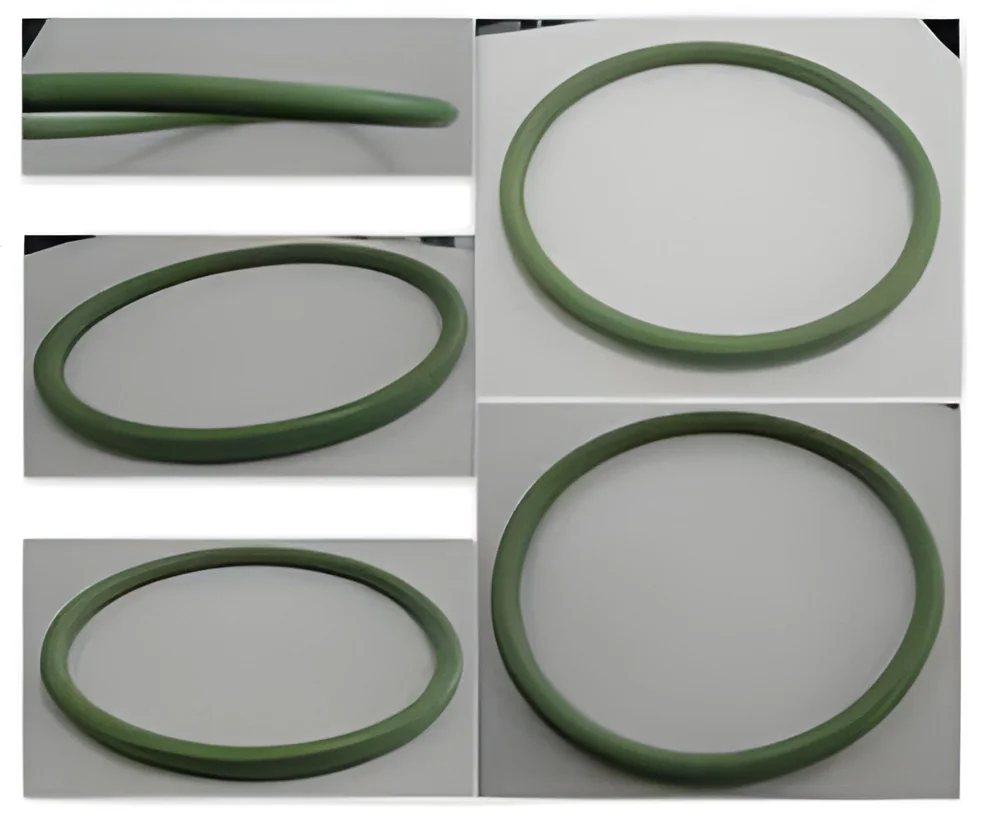
Kalrez and Viton high-performance seals represent advanced sealing solutions engineered for extreme industrial environments where reliability is non-negotiable. Kalrez, as a perfluoroelastomer, delivers superior performance in the most demanding conditions with temperature resistance up to 327°C and virtually unmatched chemical compatibility across aggressive media. Viton, as a fluoroelastomer, provides excellent performance at a more accessible price point with temperature resistance up to 204°C, making it suitable for numerous industrial applications requiring strong chemical resistance. Understanding the technical specifications, performance characteristics, and operational requirements between these materials enables procurement specialists and engineers to make informed decisions that balance performance needs with budget considerations for their specific application requirements.

These advanced sealing materials serve critical functions across multiple industries where operation...
Kalrez and Viton high-performance seals represent advanced sealing solutions engineered for extreme industrial environments where reliability is non-negotiable. Kalrez, as a perfluoroelastomer, delivers superior performance in the most demanding conditions with temperature resistance up to 327°C and virtually unmatched chemical compatibility across aggressive media. Viton, as a fluoroelastomer, provides excellent performance at a more accessible price point with temperature resistance up to 204°C, making it suitable for numerous industrial applications requiring strong chemical resistance. Understanding the technical specifications, performance characteristics, and operational requirements between these materials enables procurement specialists and engineers to make informed decisions that balance performance needs with budget considerations for their specific application requirements.

These advanced sealing materials serve critical functions across multiple industries where operational reliability under harsh conditions determines success. Kalrez finds primary application in semiconductor manufacturing, aerospace, pharmaceutical production, and oil and gas industries where extreme temperatures and aggressive chemicals are routinely encountered. The semiconductor industry particularly values Kalrez for its ultra-clean properties and minimal particle generation in sensitive manufacturing environments. Viton sees extensive use in automotive manufacturing, chemical processing plants, general industrial equipment, and energy sectors where strong chemical resistance is essential without the extreme temperature demands that necessitate Kalrez. Both materials perform reliably in sealing applications for pumps, valves, compressors, and fluid handling systems across these diverse industrial sectors.

The business value proposition between Kalrez and Viton centers on total cost of ownership and operational reliability throughout the product lifecycle. Kalrez commands a higher initial investment but delivers exceptional long-term value in applications where seal failure would result in catastrophic downtime, substantial production losses, or safety incidents. Its extended service life in extreme conditions often justifies the premium cost through reduced maintenance frequency, fewer replacements, and improved system reliability. Viton offers an optimal balance of performance and affordability for applications that don't require the extreme capabilities of Kalrez, providing excellent chemical resistance and thermal stability at a more accessible price point. Both materials contribute significantly to operational efficiency by minimizing unplanned downtime, reducing maintenance costs, and ensuring consistent performance in challenging industrial environments.

Key Features:
- Kalrez provides extreme temperature resistance up to 327°C compared to Viton's 204°C maximum
- Superior chemical resistance to aggressive solvents, acids, bases, and fuels across both materials
- Excellent compression set resistance for long-term sealing performance and reliability
- Custom formulation options available for specific application requirements and environments
- Comprehensive material certifications and compliance with industry standards and specifications

Benefits:
- Extended service life reduces maintenance frequency and replacement costs
- Reliable performance in harsh conditions minimizes unplanned downtime
- Chemical compatibility prevents degradation and ensures system integrity
- Temperature stability maintains sealing effectiveness across operating ranges
- Industry certifications provide assurance of quality and performance standards
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Kalrez and Viton seals provide critical sealing solutions across industries requiring superior chemical and thermal resistance. Kalrez excels in extreme temperatures up to 327°C with exceptional resistance to aggressive chemicals, making it ideal for semiconductor manufacturing, aerospace, and oil and gas applications where failure carries significant consequences. Viton delivers reliable performance at lower cost for temperatures up to 204°C, widely used in automotive, chemical processing, and general industrial sealing where strong chemical resistance is needed without extreme heat conditions.
Selecting between Kalrez and Viton depends on specific application requirements and operational parameters. Kalrez represents the premium choice for the most demanding environments where downtime costs far exceed seal price, while Viton offers dependable performance for standard harsh conditions. Both materials provide excellent compression set resistance and extended service life, reducing maintenance frequency and operational costs across various sealing applications in pumps, valves, compressors, and fluid handling systems.
- Chemical processing plants for sealing pumps and valves handling aggressive acids and solvents
- Aerospace and aviation systems requiring seals that withstand extreme temperatures and aviation fuels
- Semiconductor manufacturing equipment needing ultra-clean, high-temperature resistant seals
- Automotive industry applications including fuel systems, transmission seals, and engine components
- Oil and gas industry for downhole tools, blowout preventers, and refinery equipment sealing
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Arizona Tech- Zeal, Maharashtra
 Maharashtra, India
Industrial Equipment & Machinery•Trading Company•Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Industrial High Performance Kalrez And Viton Seals For Extreme Environments
Industrial Kalrez and Viton high-performance seals deliver extreme temperature and chemical resistance for demanding applications in aerospace, semiconductor, oil and gas industries. Compare material properties for your specific needs.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Arizona Tech- Zeal
 Maharashtra, India
Industrial Equipment & MachineryTrading Company