IN
₹
Apparel & Fashion
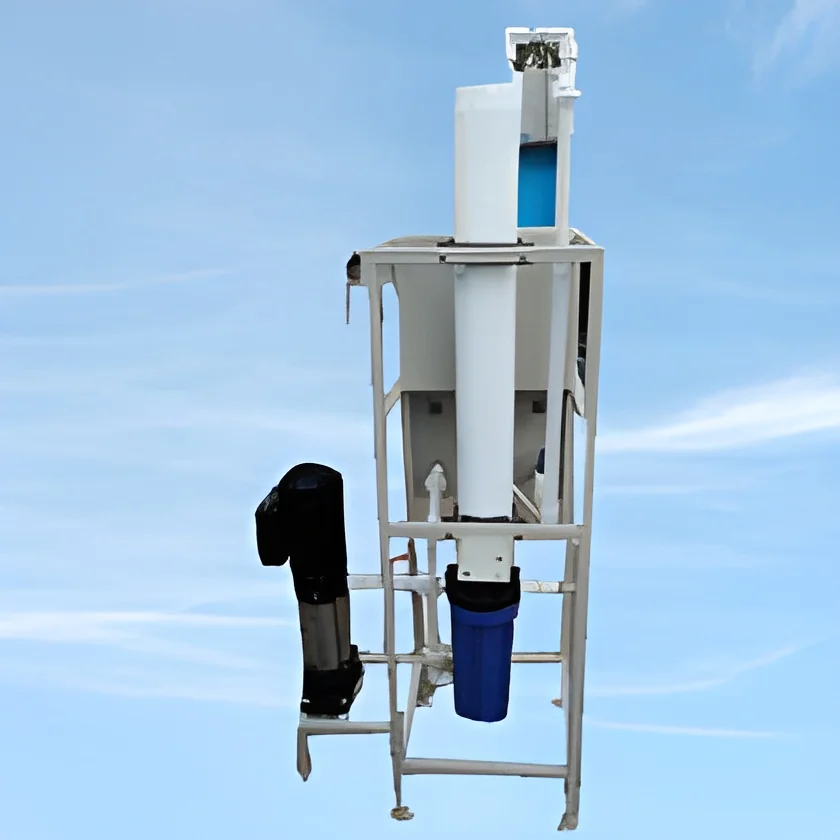
Description
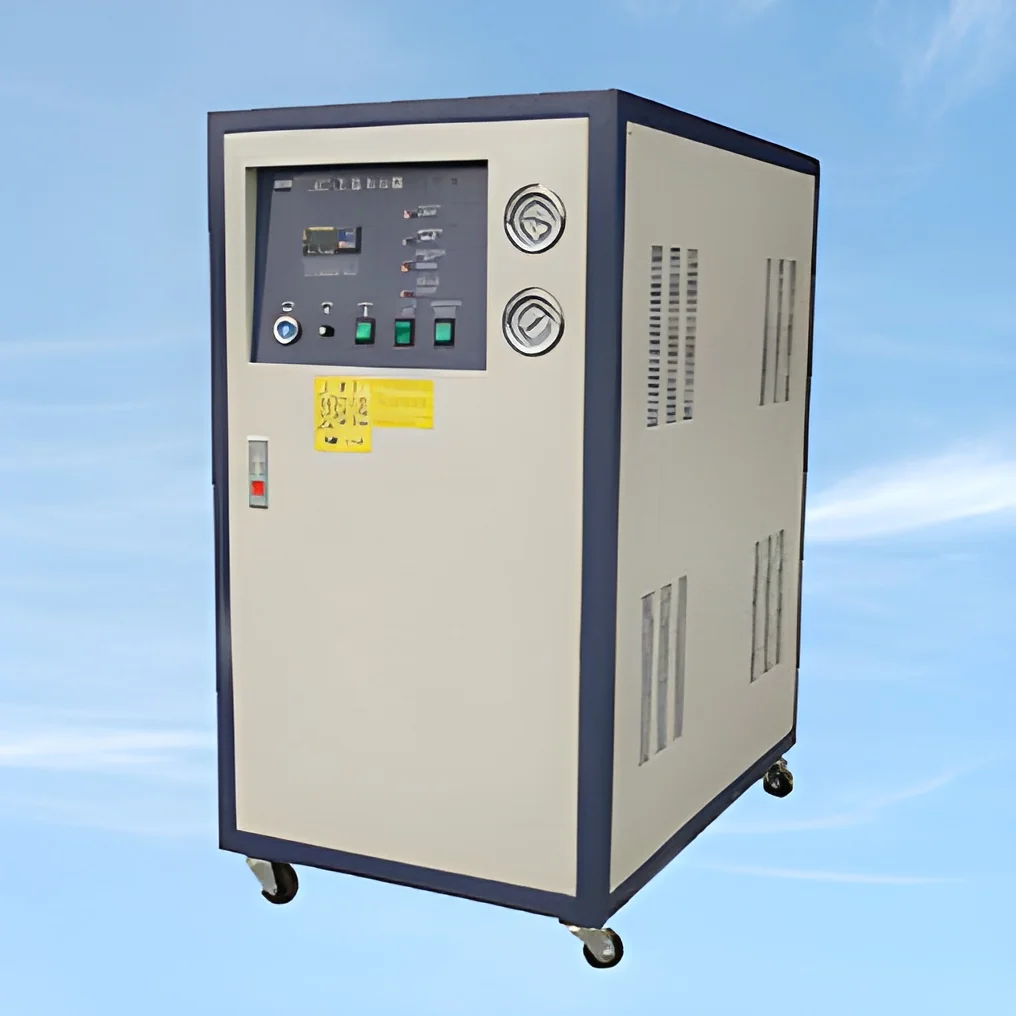
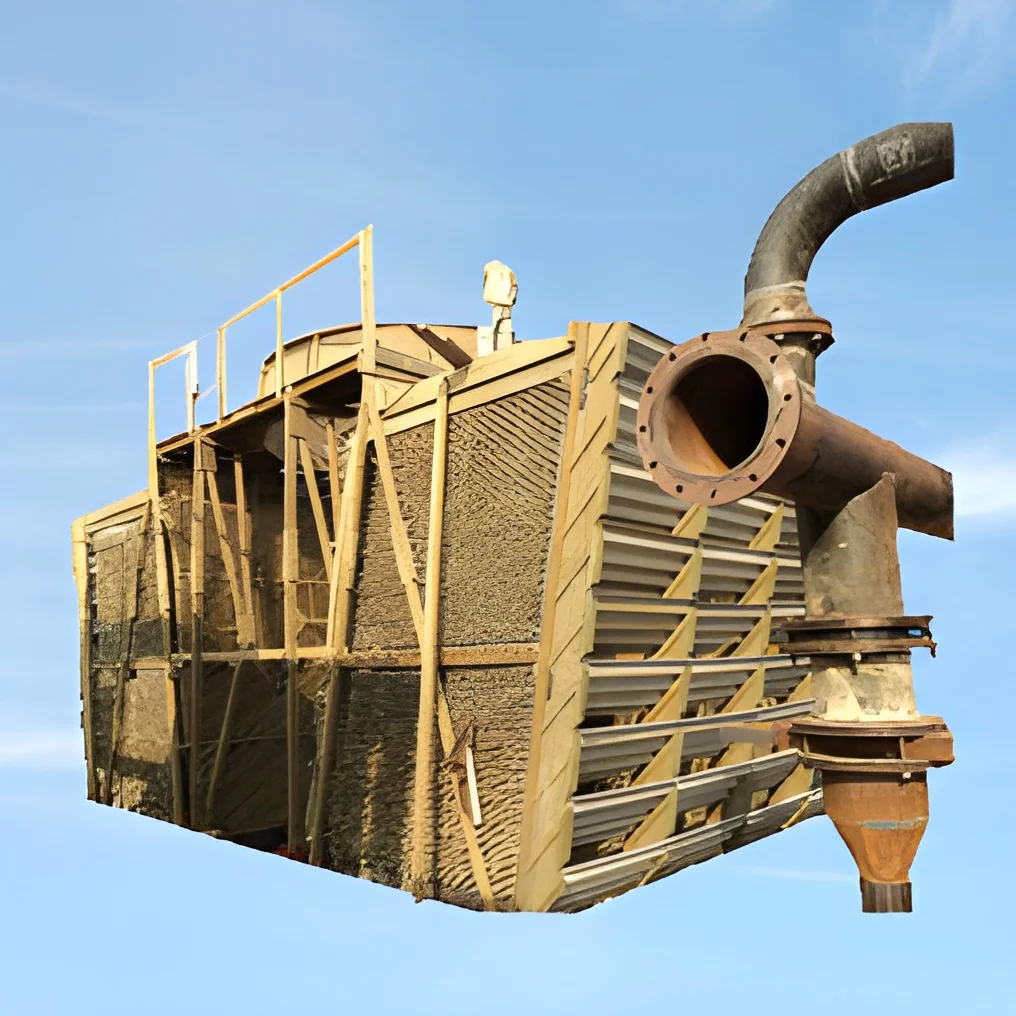
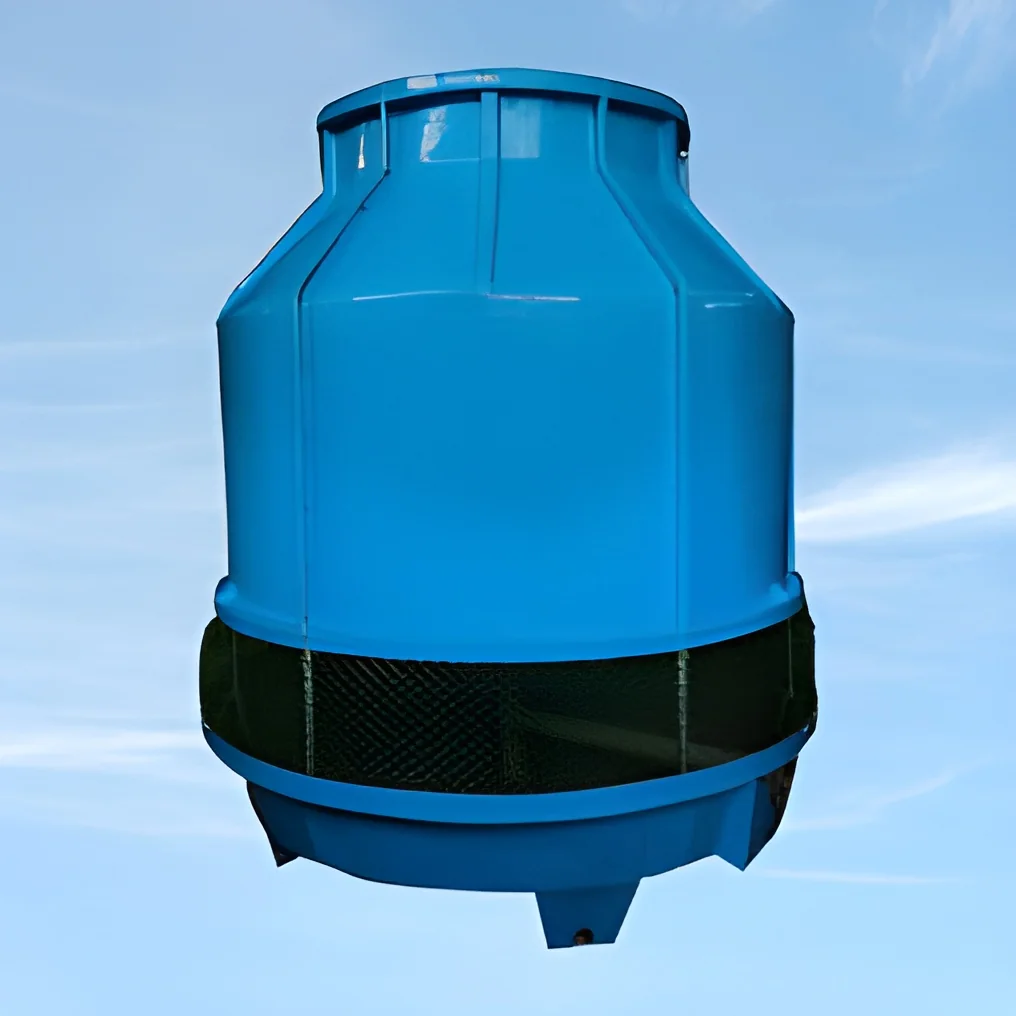
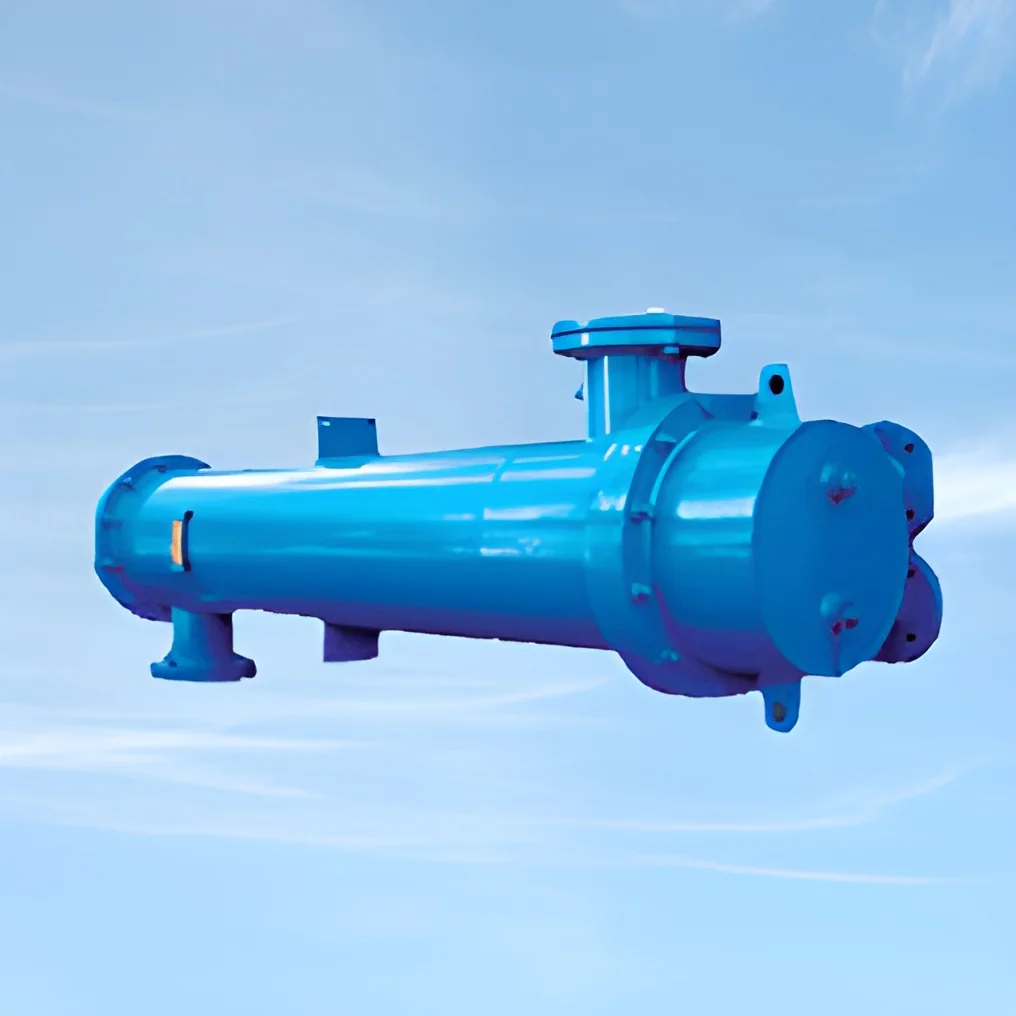
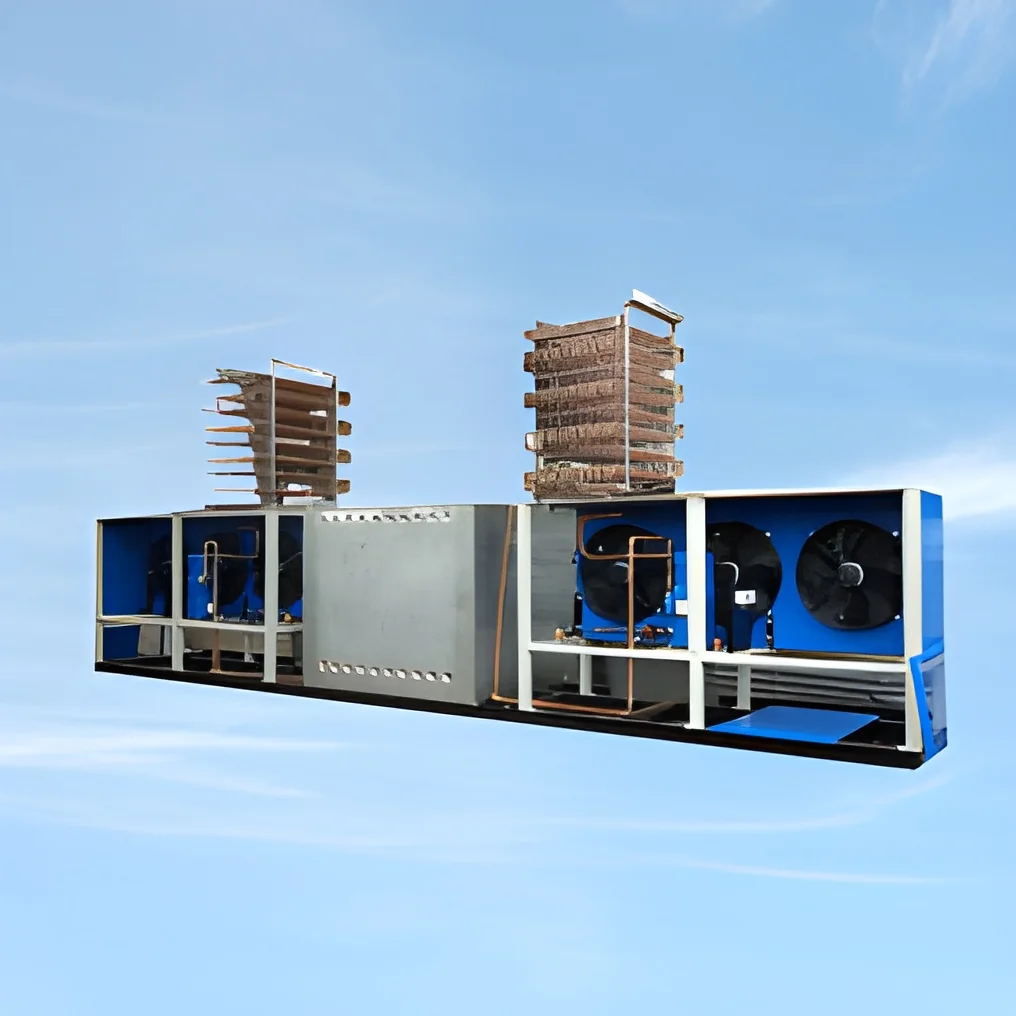
Our Industrial RO Softening Plant represents advanced water treatment technology designed specifically for industrial applications requiring high-purity water. These systems effectively remove hardness-causing minerals like calcium and magnesium while eliminating various contaminants through reverse osmosis and softening processes. Manufactured using fine-grade materials that meet international quality standards, each plant undergoes rigorous testing in our advanced laboratories to verify performance, efficiency, and durability before delivery. The robust construction ensures reliable operation in demanding environments while maintaining consistent output quality. Designed for straightforward operation and minimal maintenance requirements, these plants provide a practical solution for businesses seeking dependable water treatment without operational complications.

These water treatment systems find extensive application across numerous industries where water quality directly influence...
Our Industrial RO Softening Plant represents advanced water treatment technology designed specifically for industrial applications requiring high-purity water. These systems effectively remove hardness-causing minerals like calcium and magnesium while eliminating various contaminants through reverse osmosis and softening processes. Manufactured using fine-grade materials that meet international quality standards, each plant undergoes rigorous testing in our advanced laboratories to verify performance, efficiency, and durability before delivery. The robust construction ensures reliable operation in demanding environments while maintaining consistent output quality. Designed for straightforward operation and minimal maintenance requirements, these plants provide a practical solution for businesses seeking dependable water treatment without operational complications.

These water treatment systems find extensive application across numerous industries where water quality directly influences operational outcomes. In manufacturing sectors, they protect boilers, cooling systems, and processing equipment from scale formation and corrosion. Healthcare facilities utilize them to ensure water purity for medical procedures, laboratory testing, and equipment sterilization. The food and beverage industry depends on these plants for consistent water quality in production processes, while textile manufacturers benefit from improved dye uptake and fabric quality. Hospitality establishments use them to enhance laundry operations and guest water services, demonstrating the system's versatility across different operational scales and requirements.

Businesses investing in our Industrial RO Softening Plants experience significant operational advantages including reduced maintenance costs, extended equipment lifespan, and improved process efficiency. The reliable water softening performance minimizes downtime and prevents scale-related equipment failures, leading to consistent production output. Built with corrosion-resistant components and durable construction, these plants deliver long-term value with minimal operational interruptions. The standardized design ensures compatibility with various industrial setups while maintaining optimal performance characteristics. Trusted by importers and distributors worldwide, our products have established a reputation for quality craftsmanship and dependable performance in diverse water treatment applications.

Key Features:
- Advanced reverse osmosis and softening technology for comprehensive water treatment
- Fine-grade materials construction ensuring long-term durability and corrosion resistance
- International standard compliance for consistent global performance
- User-friendly design facilitating easy installation and operation
- Rigorous laboratory testing verifying efficiency and reliability before delivery

Benefits:
- Extended equipment lifespan through effective scale prevention
- Reduced maintenance requirements and associated operational costs
- Consistent high-purity water output for various industrial processes
- Reliable performance in diverse operating environments and conditions
- Improved process efficiency and product quality across applications
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Industrial RO softening plants are engineered to remove calcium, magnesium, and contaminants from water, producing high-purity output essential for critical industrial processes. These systems ensure consistent water quality that meets international standards, making them suitable for environments where water purity directly impacts operational efficiency and product quality. Their robust construction allows reliable performance across diverse operating conditions and industry requirements.
These water treatment systems serve multiple sectors requiring softened, purified water for daily operations. From manufacturing facilities to healthcare institutions, the plants provide dependable hardness removal that protects equipment and enhances process outcomes. The versatility of these systems makes them adaptable for both large-scale industrial complexes and specialized commercial setups where water quality is paramount for success and compliance.
- Boiler feed water treatment in power generation and manufacturing to prevent scaling
- Beverage production facilities ensuring consistent water purity for product quality
- Hospital water systems supporting sterile processing and medical equipment
- Textile manufacturing for improved dye absorption and fabric treatment
- Hospitality operations for laundry services and water-based amenities
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Gireesh Heat Exchangers & Cooling Towers, Tamil Nadu
 Tamil Nadu, India
Industrial Equipment & Machinery•Manufacturer•Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Main Markets
Mid East
Africa
Domestic
Industrial RO Softening Plant For High Purity Water Treatment
Industrial RO Softening Plant delivers high-purity water treatment by removing hardness and contaminants. Built with fine-grade materials to international standards for reliable performance across various industrial applications.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Gireesh Heat Exchangers & Cooling Towers
 Tamil Nadu, India
Industrial Equipment & MachineryManufacturer