IN
₹
Apparel & Fashion
Description
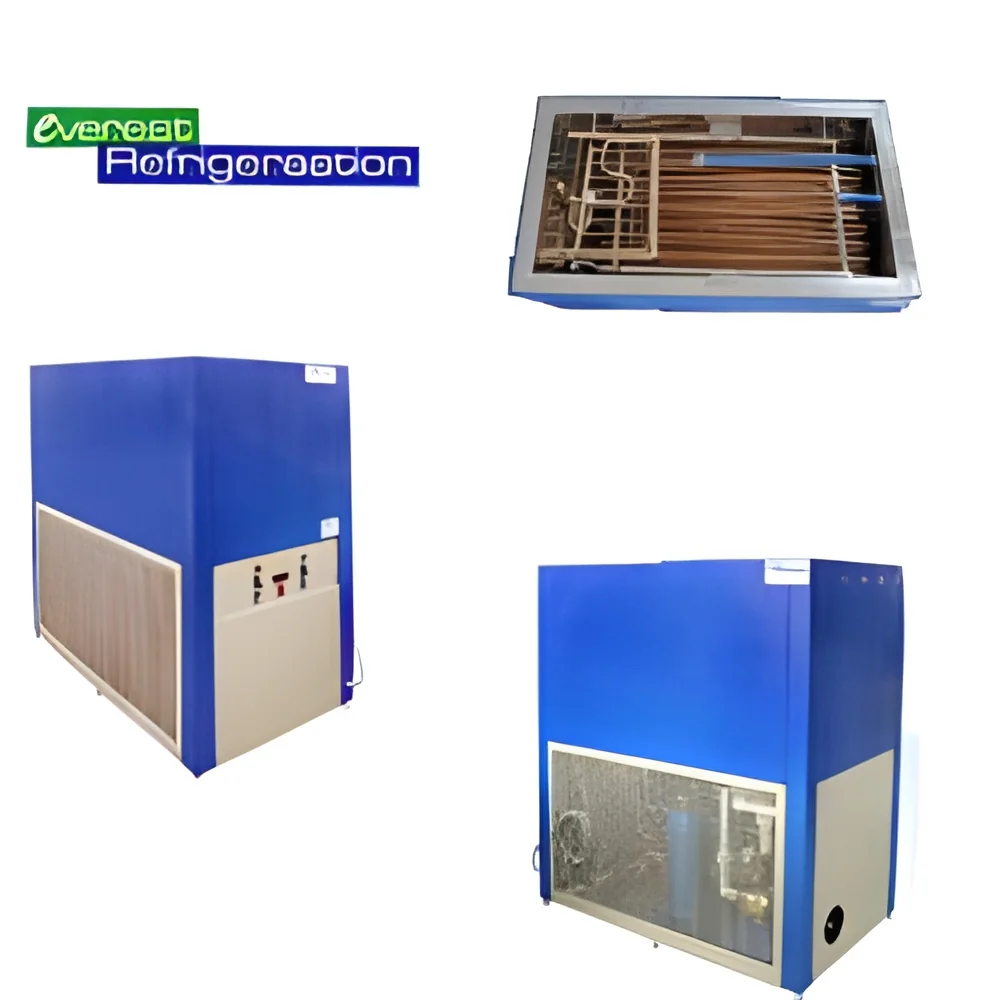
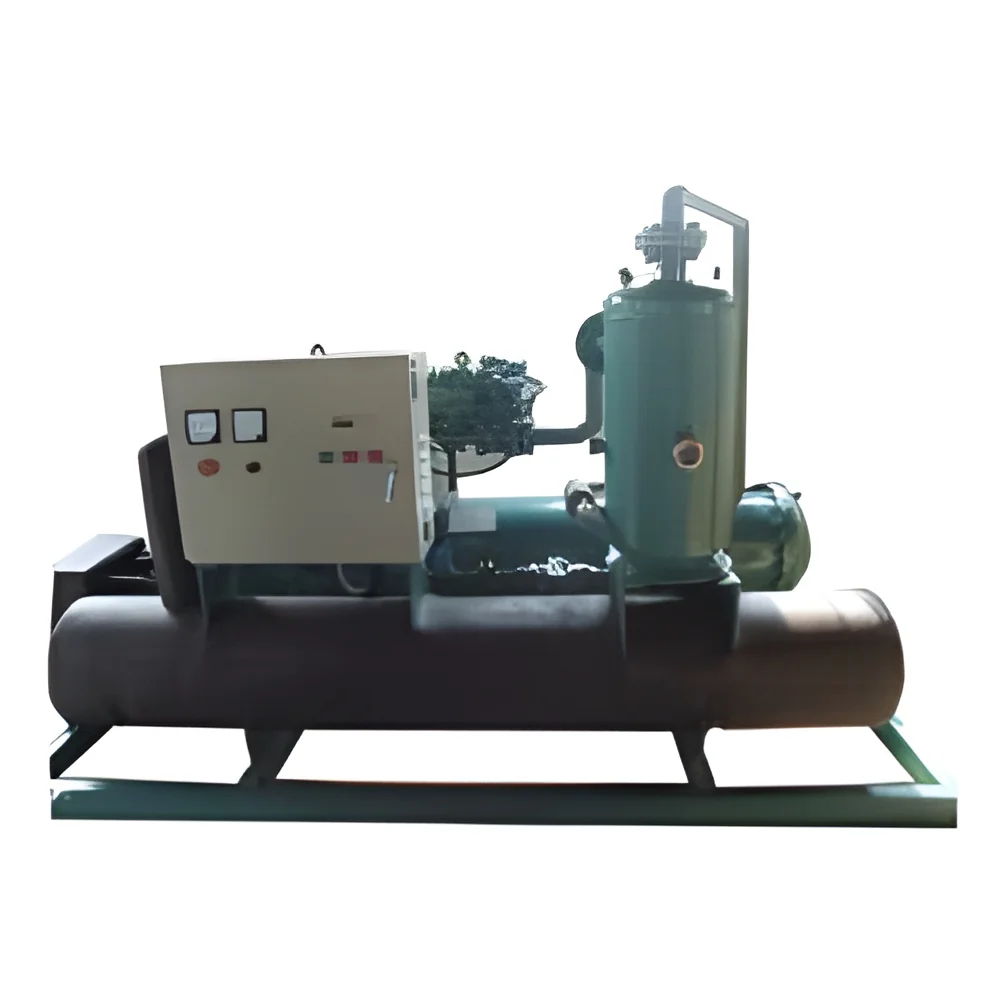
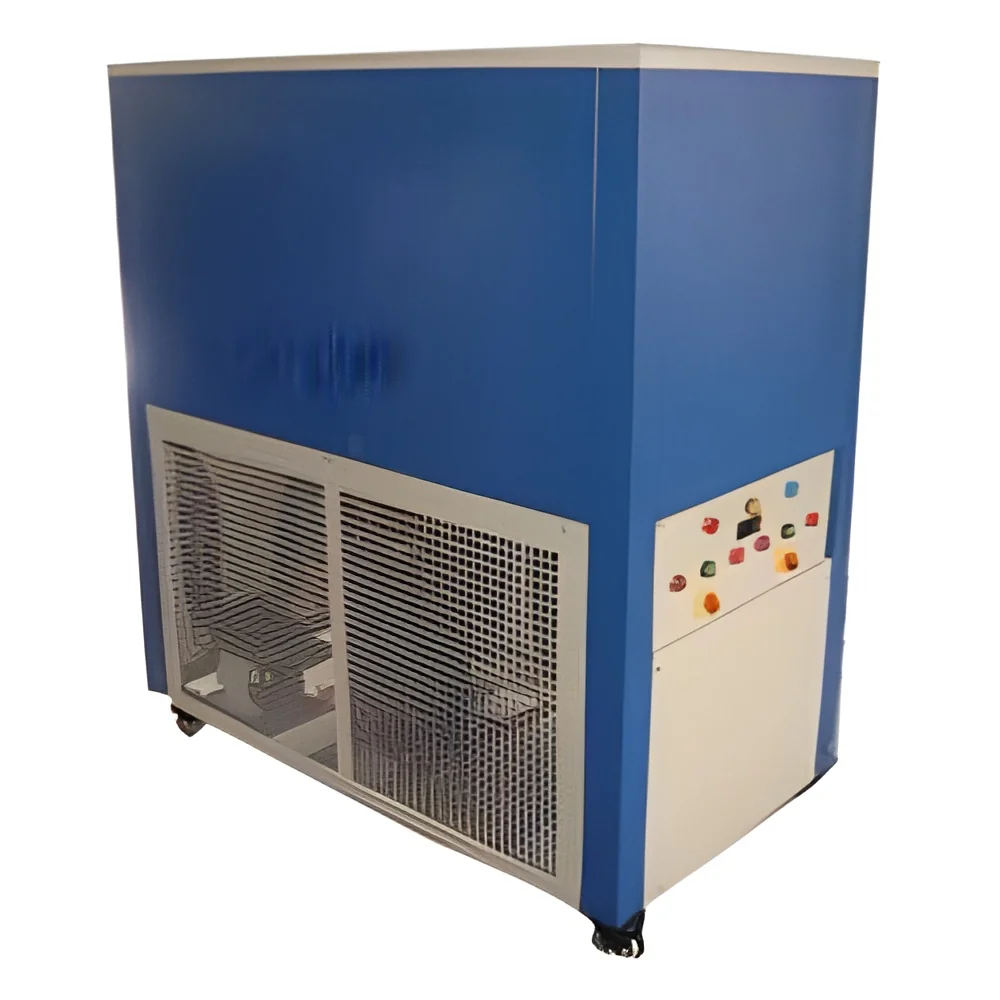
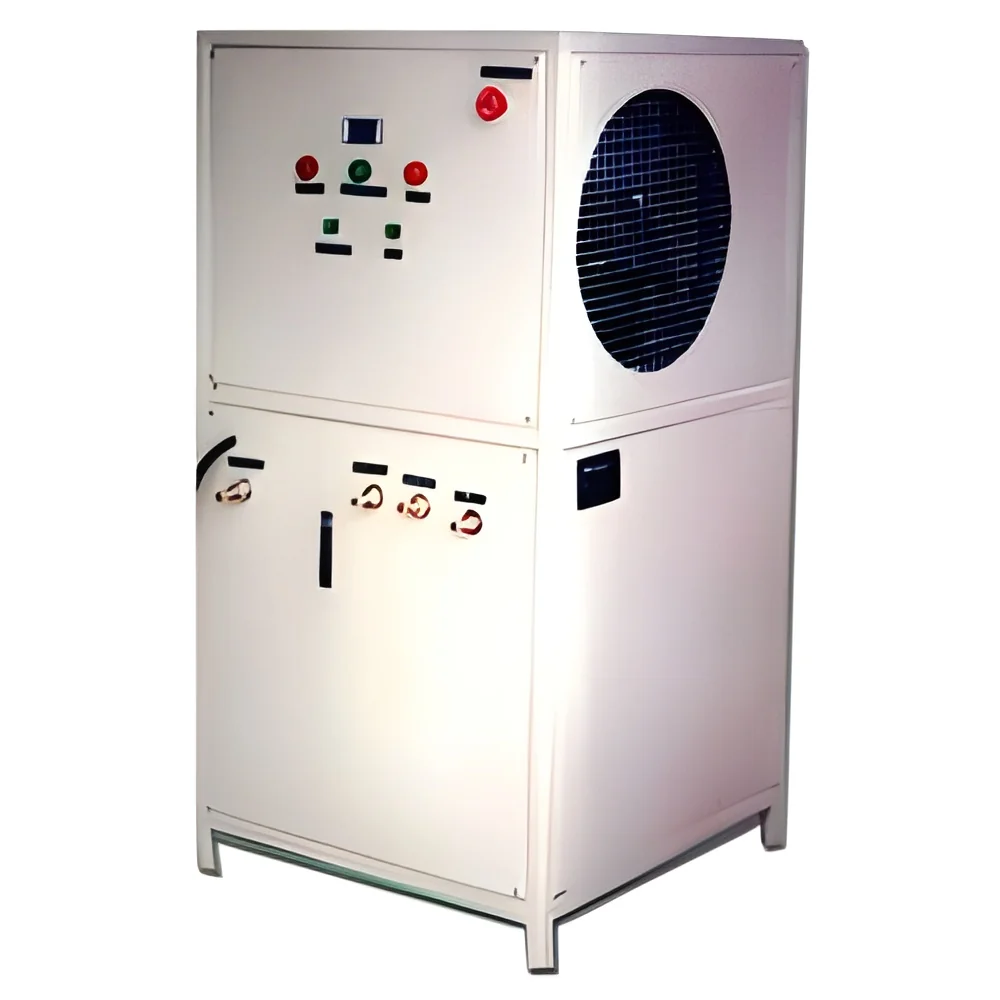
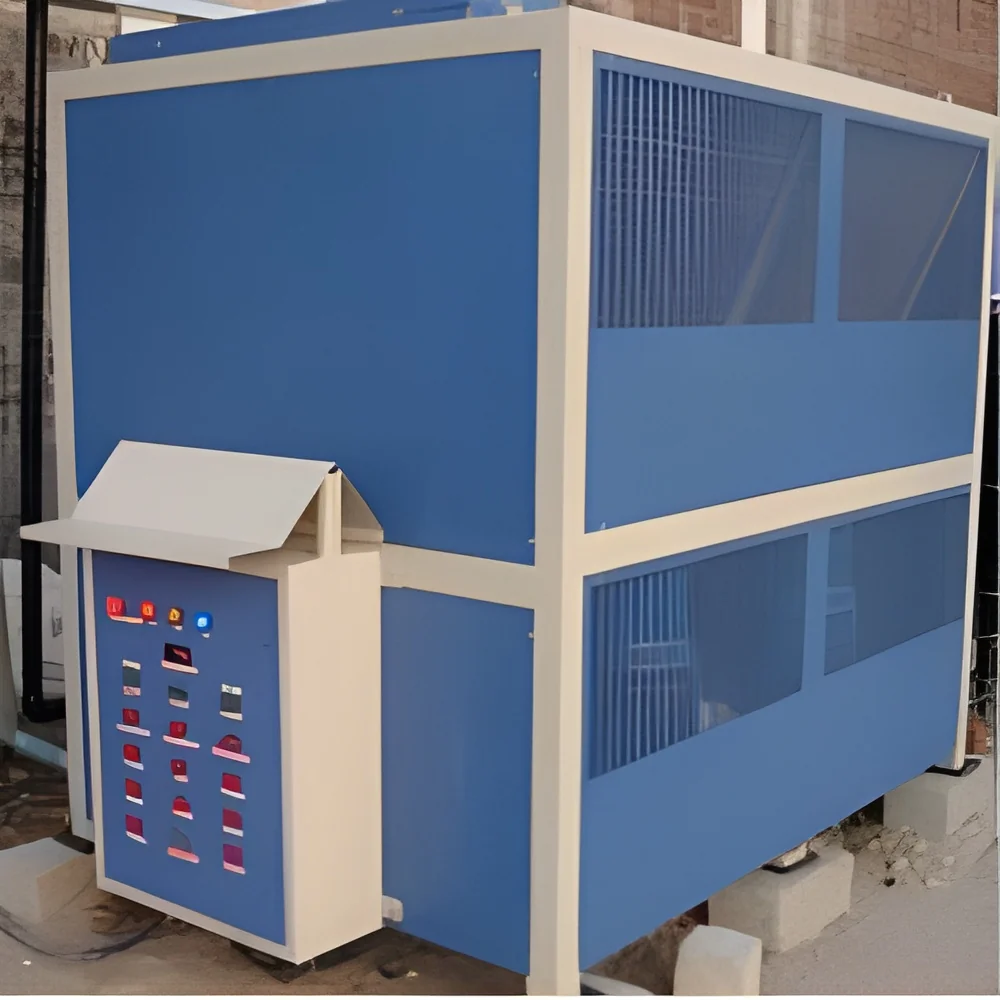
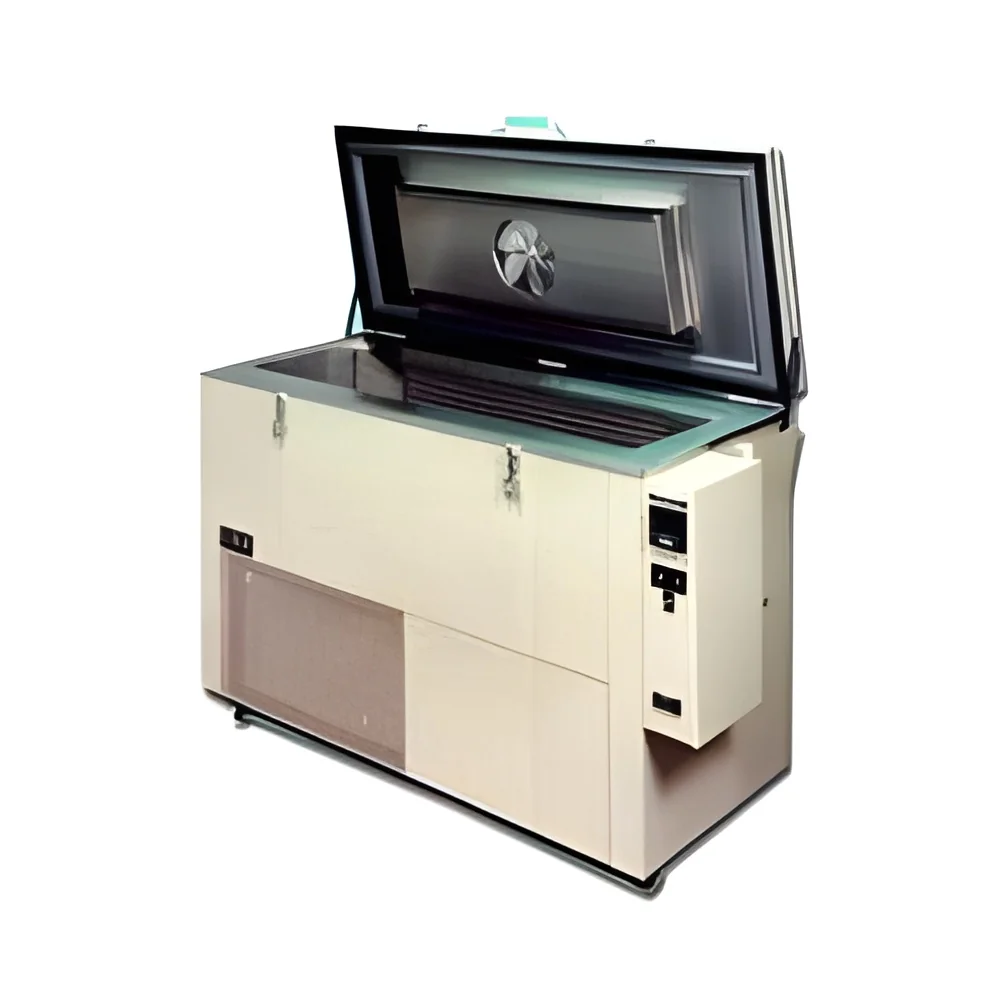
Industrial ultra low temperature freezers represent advanced cold storage solutions engineered for demanding operational environments. These heavy-duty units feature robust construction and precision temperature control systems designed to maintain consistent ultra-low temperatures. The freezers incorporate reliable cooling technology with uniform temperature distribution throughout the storage chamber. Built for continuous operation with minimal maintenance requirements, these units provide dependable performance for critical storage applications where temperature stability is paramount. The design focuses on operational efficiency while ensuring product integrity through advanced temperature management and secure storage conditions.

These freezers serve essential functions across food processing, pharmaceutical, and manufacturing industries. In food processing facilities, they ensure proper preservation of perishable goods while maintaining quality standards throughout processing cy...
Industrial ultra low temperature freezers represent advanced cold storage solutions engineered for demanding operational environments. These heavy-duty units feature robust construction and precision temperature control systems designed to maintain consistent ultra-low temperatures. The freezers incorporate reliable cooling technology with uniform temperature distribution throughout the storage chamber. Built for continuous operation with minimal maintenance requirements, these units provide dependable performance for critical storage applications where temperature stability is paramount. The design focuses on operational efficiency while ensuring product integrity through advanced temperature management and secure storage conditions.

These freezers serve essential functions across food processing, pharmaceutical, and manufacturing industries. In food processing facilities, they ensure proper preservation of perishable goods while maintaining quality standards throughout processing cycles. Pharmaceutical operations rely on them for storing temperature-sensitive medications, vaccines, and research materials under strictly controlled conditions. Manufacturing industries utilize these freezers for material testing, component hardening, and production processes requiring precise temperature environments. The versatility and reliability make them indispensable equipment for businesses handling temperature-sensitive products or materials.

The operational value of these industrial freezers lies in their exceptional reliability, energy efficiency, and consistent performance. They reduce operational costs through optimized energy consumption and minimize downtime with robust construction and advanced safety systems. The units provide peace of mind through built-in safety features including comprehensive monitoring systems and circuit protection. Long-term reliability and low maintenance requirements ensure excellent return on investment while protecting valuable inventory. The durable construction and advanced temperature management systems deliver consistent performance for demanding industrial applications.

Key Features:
- Heavy-duty angular structure with triple-walled chamber construction using durable materials
- Advanced forced air circulation system ensuring uniform temperature distribution
- Double door design for vertical models and top-opening single door for horizontal units
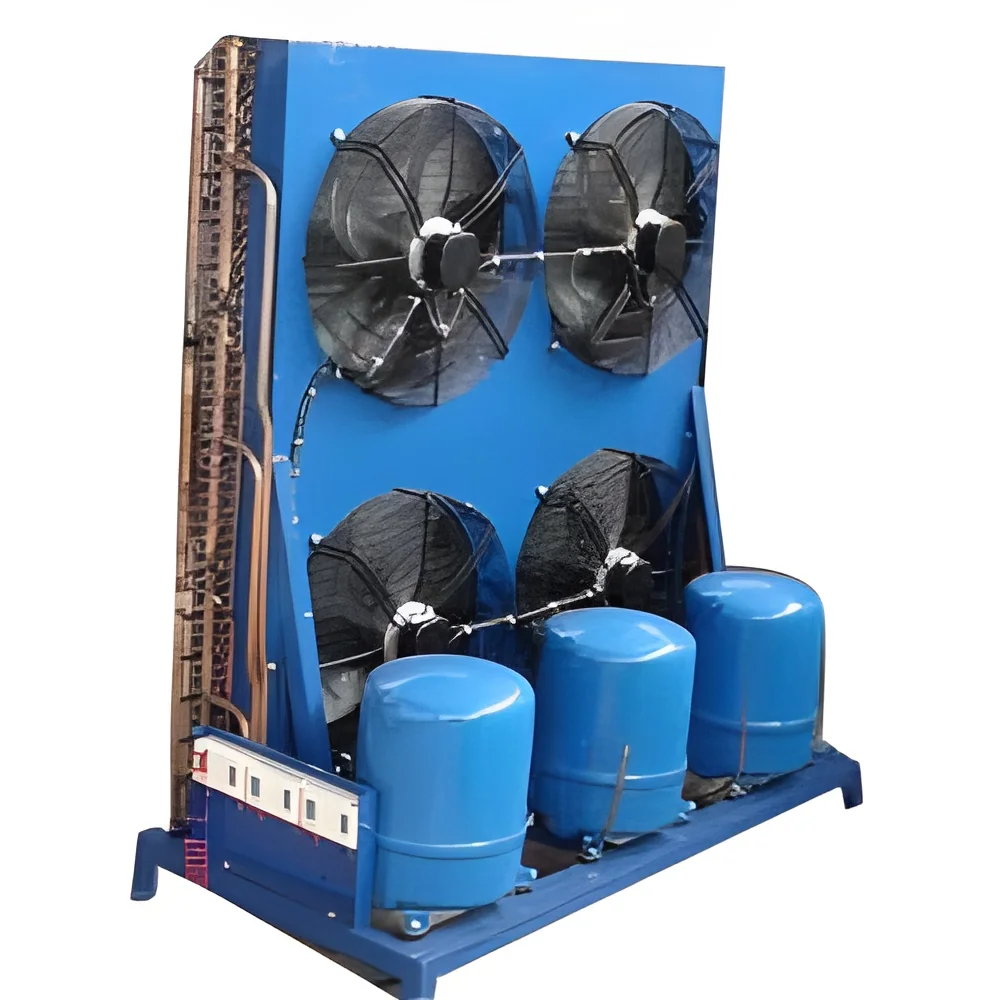
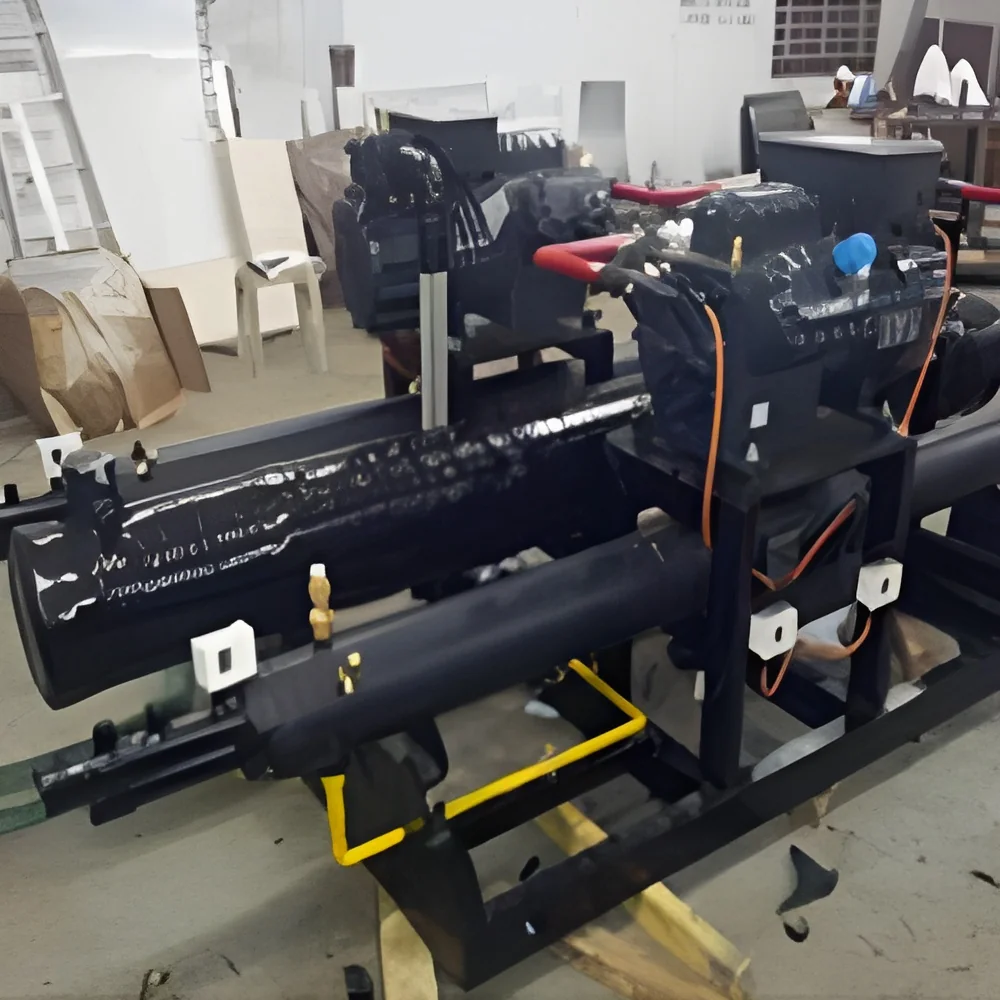
- Hermetically sealed compressor system with efficient cooling and condensing coils
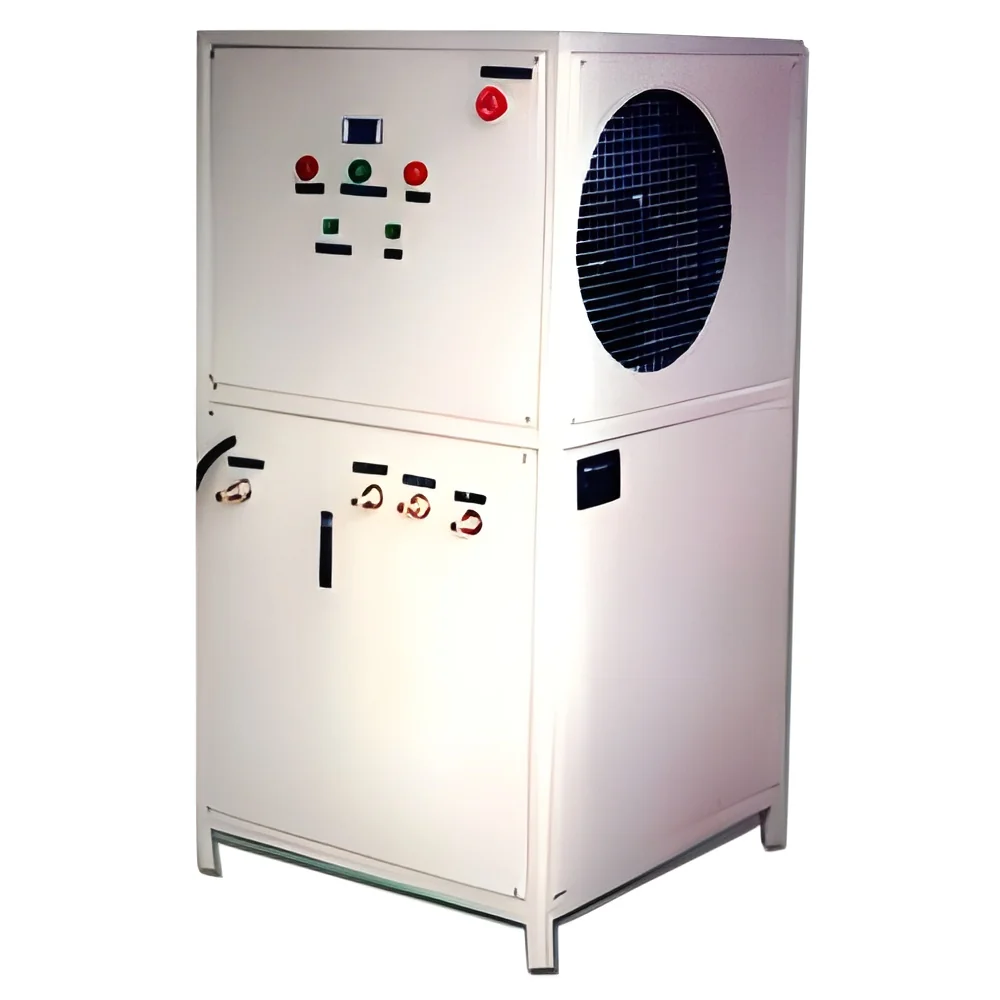
- Digital temperature control system with programmable timer and monitoring interface

Benefits:
- Consistent temperature maintenance ensures product integrity and quality preservation
- Robust construction provides long-term durability and reliable performance
- Energy-efficient operation reduces power consumption and operational costs
- Advanced safety systems protect valuable inventory and prevent temperature deviations
- Low maintenance requirements minimize downtime and ensure continuous operation
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
These industrial ultra low temperature freezers maintain precise temperature control for critical preservation and processing applications across multiple sectors. Their robust construction ensures reliable performance in demanding environments where temperature stability directly impacts product quality and safety standards. The units provide consistent cooling performance for both short-term processing needs and long-term storage requirements without compromising efficiency.
From food production facilities to pharmaceutical manufacturing plants, these freezers support diverse operational requirements with advanced temperature management systems. They handle continuous operation while protecting valuable inventory through uniform cooling distribution and secure storage conditions. The reliable performance makes them suitable for industries where temperature-sensitive materials require strict environmental control throughout processing and storage cycles.
- Food processing plants for preserving meat, seafood, and dairy products during processing and distribution
- Pharmaceutical manufacturing for storing vaccines, medications, and biological materials at required temperatures
- Research laboratories for preserving scientific samples, reagents, and experimental materials
- Chemical processing facilities for safe storage of temperature-sensitive compounds and raw materials
- Manufacturing operations for material testing, component hardening, and production process cooling
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Everest Refrigeraation, Tamil Nadu
 Tamil Nadu, India
Industrial Equipment & Machinery•Manufacturer•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Main Markets
Mid East
Eastern Asia
Africa
Domestic
Industrial Ultra Low Temperature Freezers For Food Processing And Pharmaceuticals
Industrial ultra low temperature freezers provide reliable cold storage solutions for food processing and pharmaceutical industries. These heavy-duty units feature precise temperature control and durable construction for critical preservation needs.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Everest Refrigeraation
 Tamil Nadu, India
Industrial Equipment & MachineryManufacturer