IN
₹
Apparel & Fashion

Description
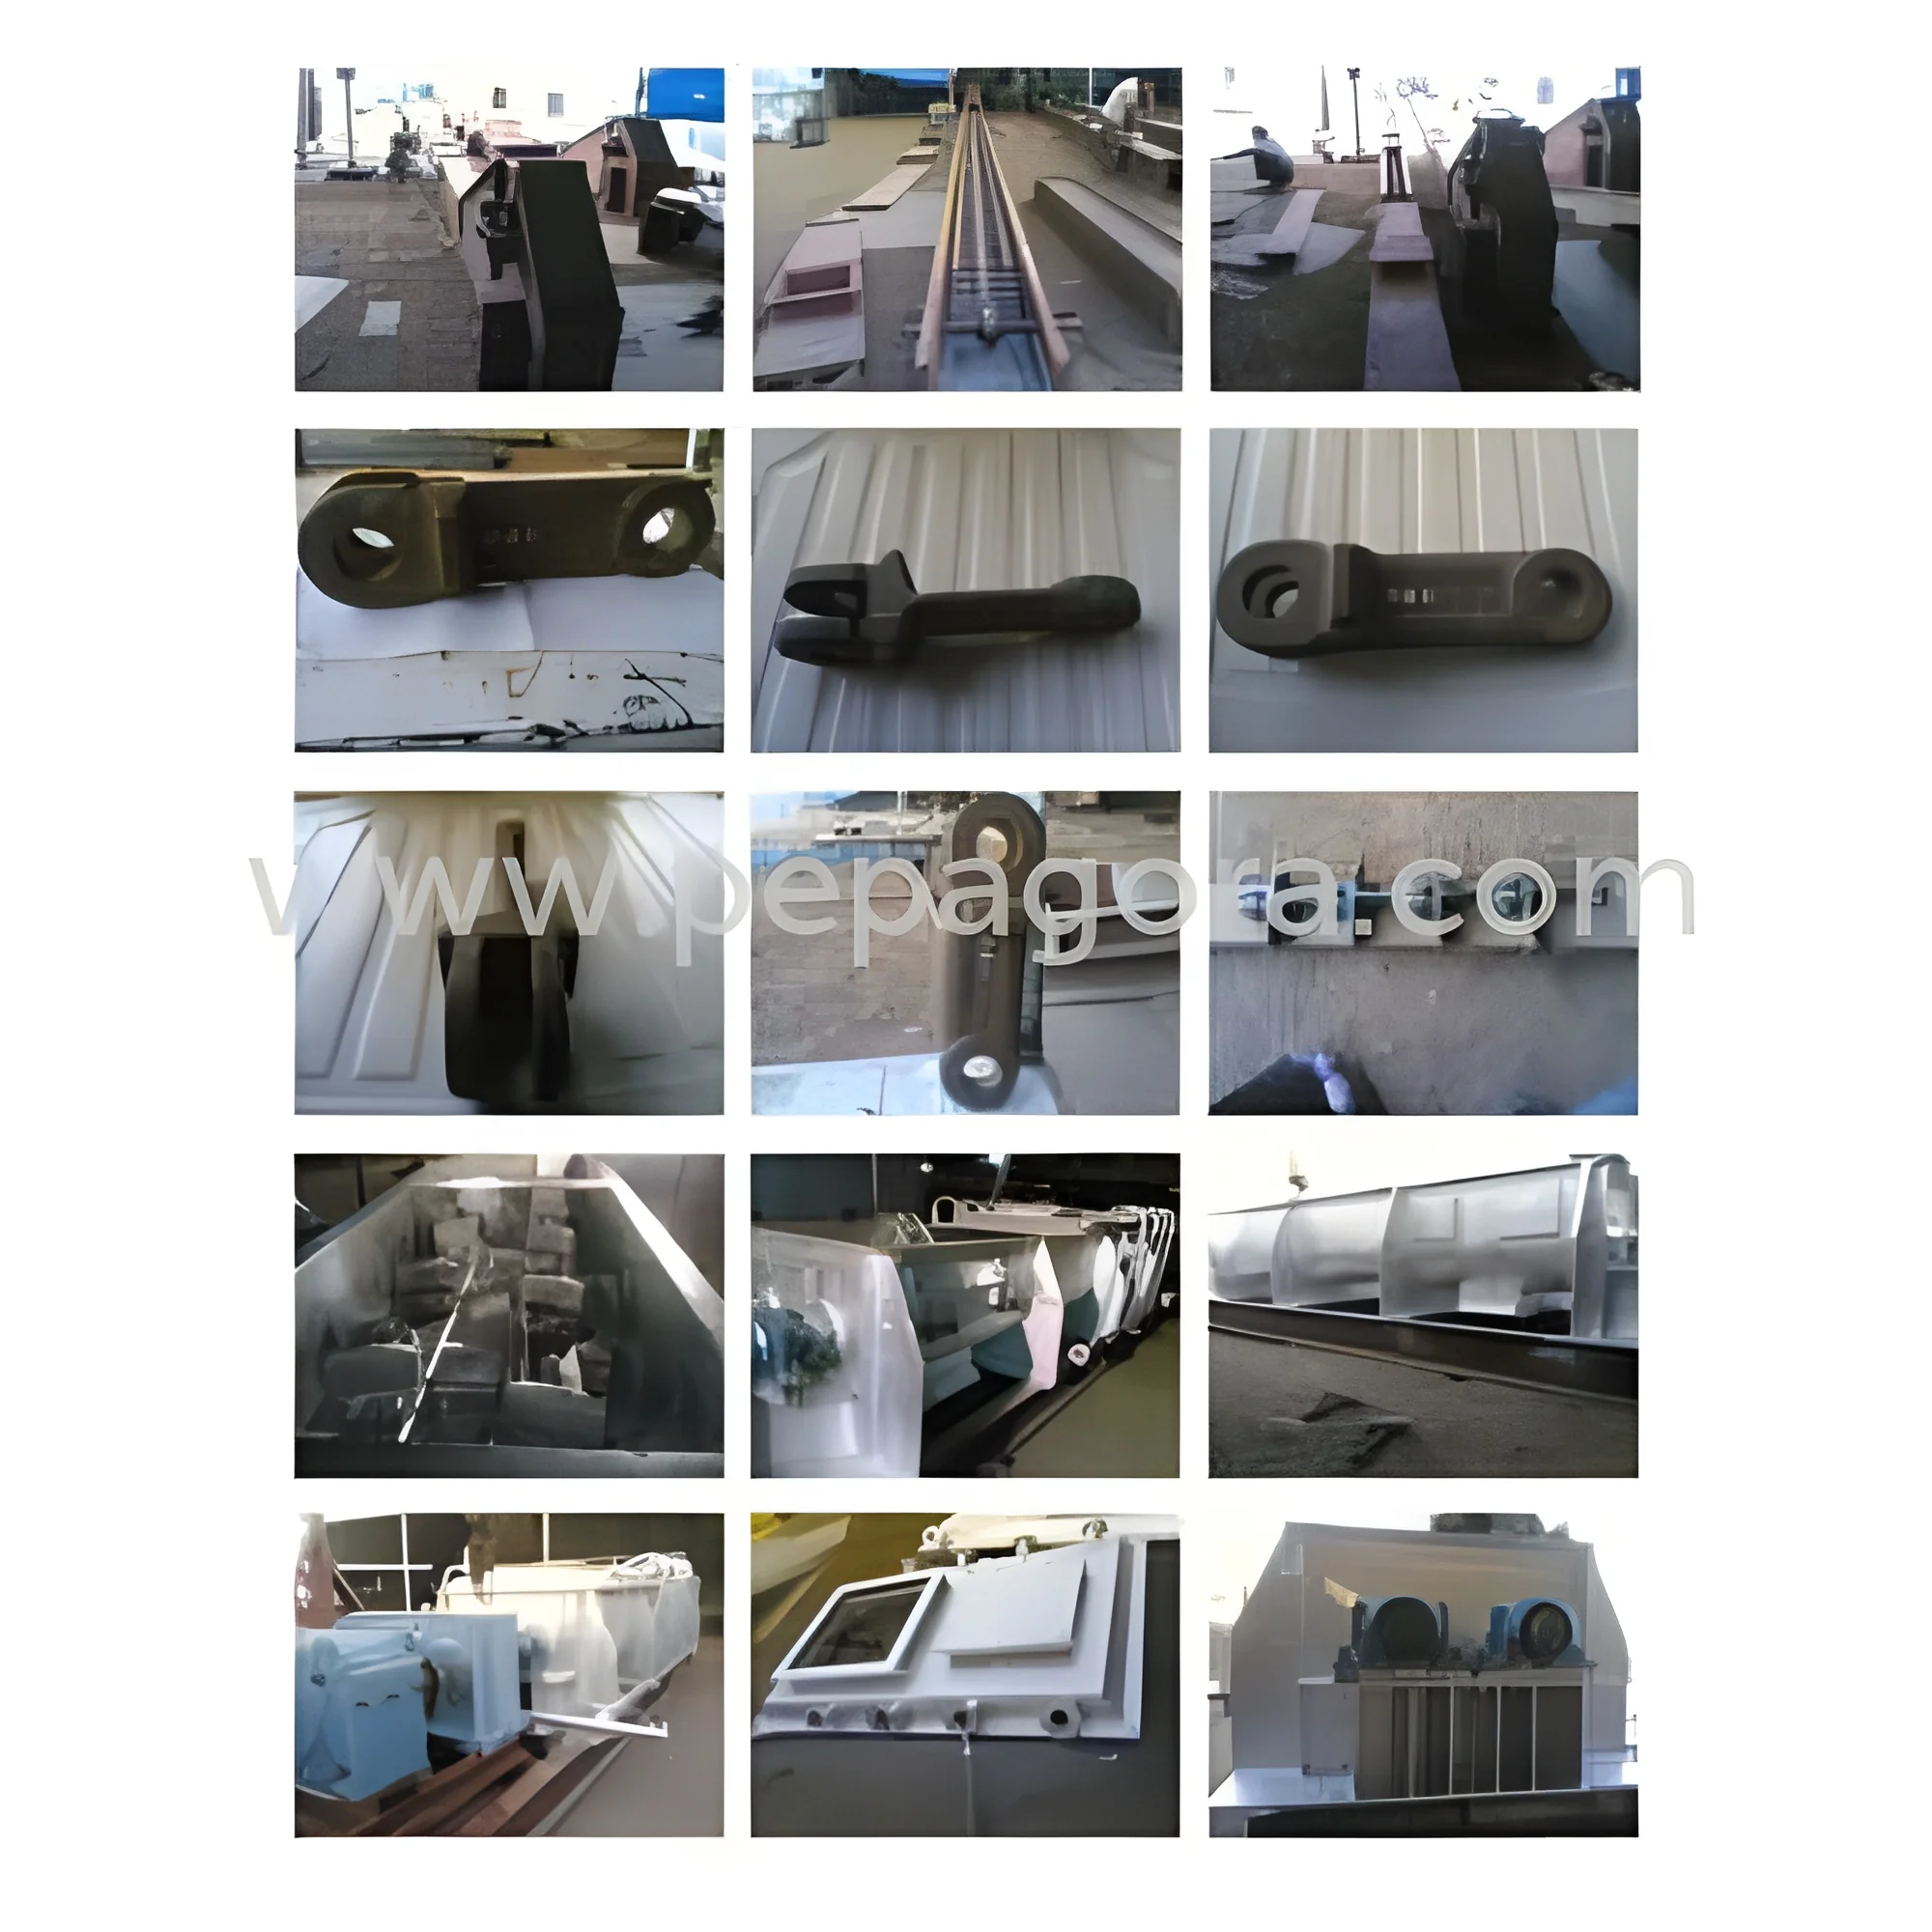
Our industrial drag chain conveyors represent reliable bulk material handling technology engineered for demanding industrial applications. Constructed from premium stainless steel with oil-resistant components, these conveyors move materials through enclosed troughs using durable chains and flights that provide consistent performance even under extreme conditions. Available in multiple standard sizes, our systems are designed to handle everything from fine powders to coarse aggregates with maximum efficiency and minimal maintenance requirements. Each conveyor is built to exacting standards, ensuring perfect integration into your existing operations while providing years of trouble-free service in challenging environments.

These robust conveyors serve critical roles across numerous industries where reliable material transport is essential for operational success. In cement manufacturing, they handle clinker and raw materials in high-temperature environments with consistent performance....
Our industrial drag chain conveyors represent reliable bulk material handling technology engineered for demanding industrial applications. Constructed from premium stainless steel with oil-resistant components, these conveyors move materials through enclosed troughs using durable chains and flights that provide consistent performance even under extreme conditions. Available in multiple standard sizes, our systems are designed to handle everything from fine powders to coarse aggregates with maximum efficiency and minimal maintenance requirements. Each conveyor is built to exacting standards, ensuring perfect integration into your existing operations while providing years of trouble-free service in challenging environments.

These robust conveyors serve critical roles across numerous industries where reliable material transport is essential for operational success. In cement manufacturing, they handle clinker and raw materials in high-temperature environments with consistent performance. Chemical processing plants utilize them for moving powders and granules while maintaining complete containment of various substances. Food processing facilities benefit from their hygienic design when transporting ingredients, while mining operations rely on their exceptional durability for moving extracted minerals and ores. Waste treatment plants use these conveyors for sludge and biomass handling, demonstrating their remarkable versatility across virtually every bulk material handling sector with demanding requirements.

The business value of our drag chain conveyors extends far beyond initial purchase price, delivering long-term operational reliability and cost efficiency that benefits your bottom line. These systems significantly reduce maintenance downtime through robust construction and quality components, while their energy-efficient operation lowers power consumption compared to alternative conveying methods. The enclosed design minimizes material loss and environmental contamination, reducing cleanup costs and regulatory compliance issues while improving workplace safety. Standard sizes ensure quick availability while maintaining high performance standards for various applications. Backed by comprehensive support and industry expertise, these conveyors represent a smart investment in operational infrastructure that pays dividends through years of reliable service and minimal operational disruptions.

Key Features:
- Constructed from durable stainless steel for corrosion resistance and long service life
- Oil-resistant components ensure reliable operation in lubricated or wet environments
- Enclosed trough design prevents material spillage and environmental contamination
- Multiple standard sizes available to suit various operational requirements
- Robust chain and flight system designed for heavy loads and abrasive materials

Benefits:
- Reduced maintenance downtime through durable construction and quality components
- Energy-efficient operation lowers power consumption and operational costs
- Minimal material loss and environmental contamination for cleaner operations
- Quick availability in standard sizes for faster implementation timelines
- Long-term reliability ensures consistent performance and operational continuity
Specifications
| Key Attributes | |
|---|---|
| Material | Stainless Steel |
| Material Feature | Oil Resistant |
| Structure | Conveyor System |
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Industrial drag chain conveyors efficiently transport bulk materials through enclosed troughs using interconnected chains and flights. These systems handle everything from fine powders to large aggregates with minimal spillage and dust generation, making them ideal for harsh industrial environments where containment and reliability are critical requirements for continuous operations.
These conveyors excel in horizontal, inclined, and vertical material transport applications across multiple processing industries. Their enclosed design protects materials from contamination while preventing environmental exposure, ensuring safe operation in facilities with strict hygiene or safety standards. The robust stainless steel construction withstands heavy loads and abrasive materials while maintaining consistent performance in demanding conditions.
- Cement plants for transporting clinker, raw meal, and finished cement products
- Chemical processing facilities handling powders, granules, and industrial materials
- Food processing plants moving grains, sugars, and bulk ingredients safely
- Mining operations transporting coal, minerals, and extracted materials efficiently
- Waste treatment facilities moving sludge, biomass, and recycled materials
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
R & G Enterprises, Maharashtra
 Maharashtra, India
Manufacturer
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Industrial Drag Chain Conveyor Stainless Steel Oil Resistant
Industrial drag chain conveyor stainless steel oil resistant for heavy-duty bulk material handling. Multiple sizes available for reliable transport across industries with durable construction.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
R & G Enterprises
 Maharashtra, India
Manufacturer