IN
₹
Apparel & Fashion

Description
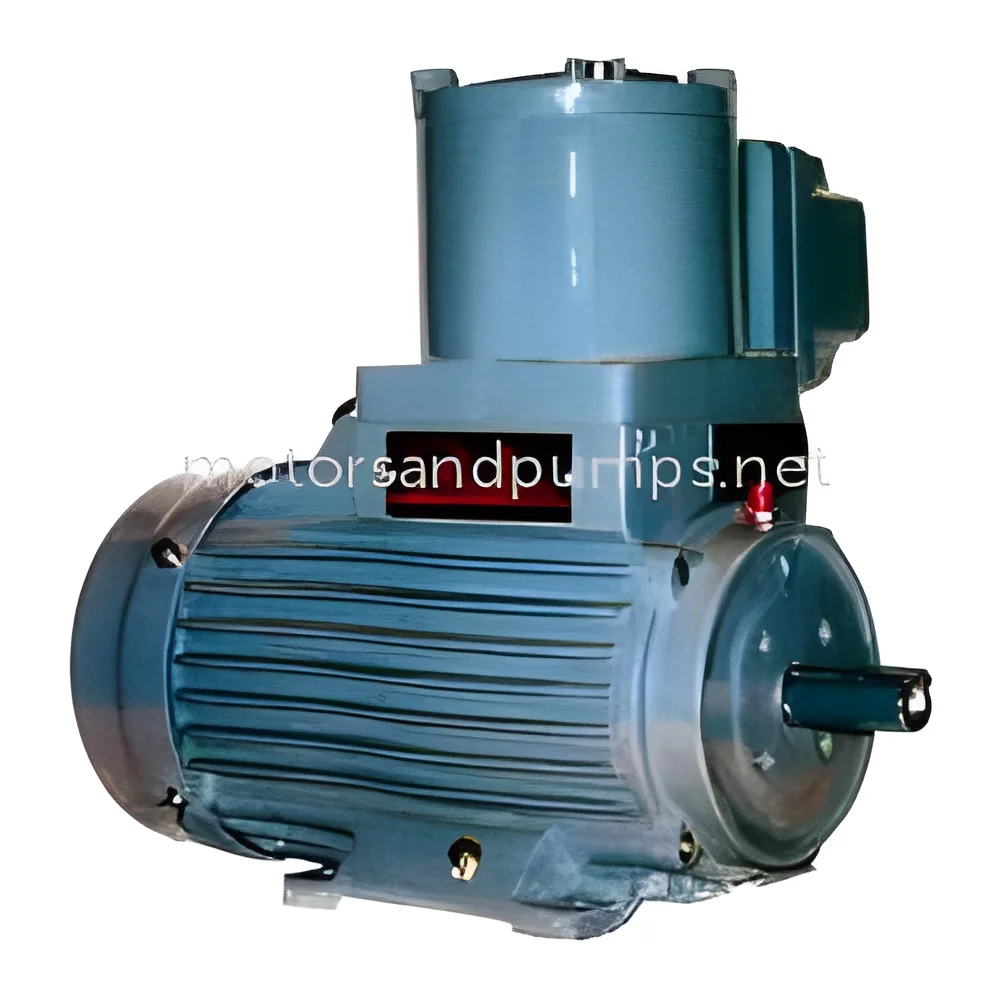
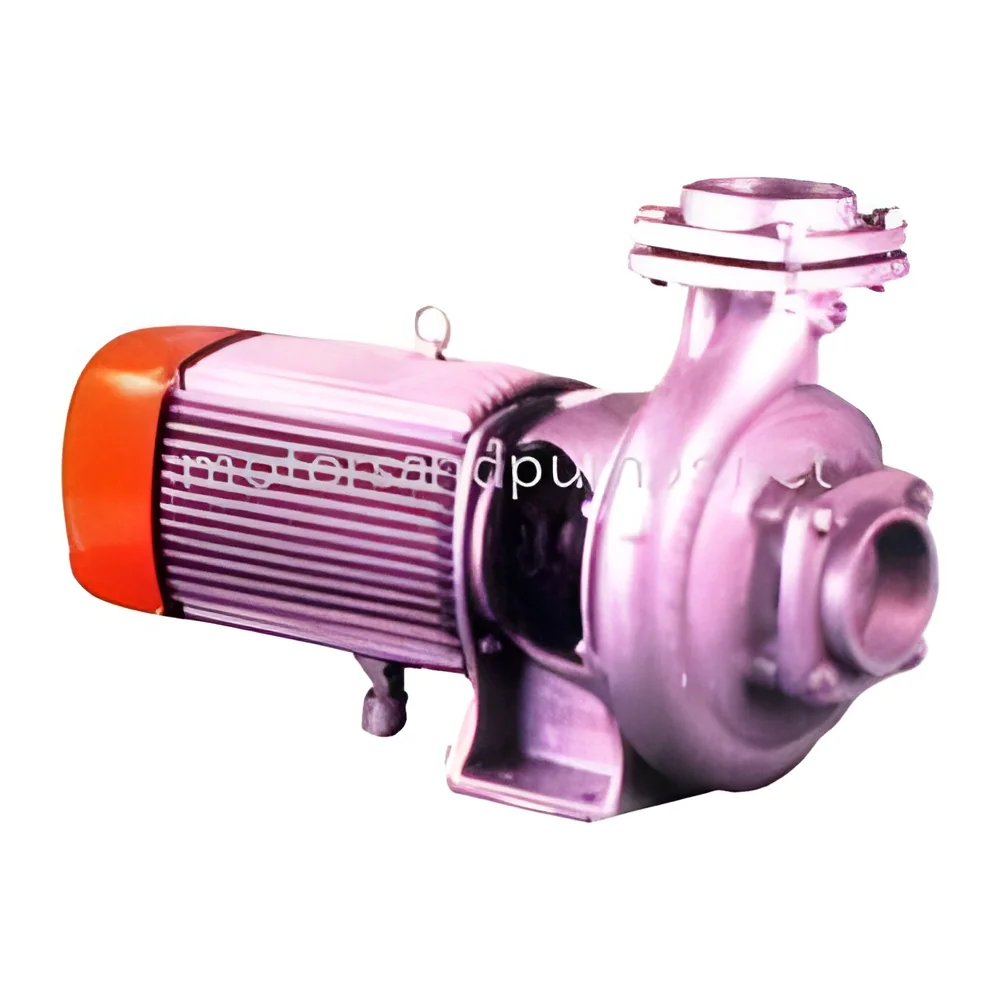
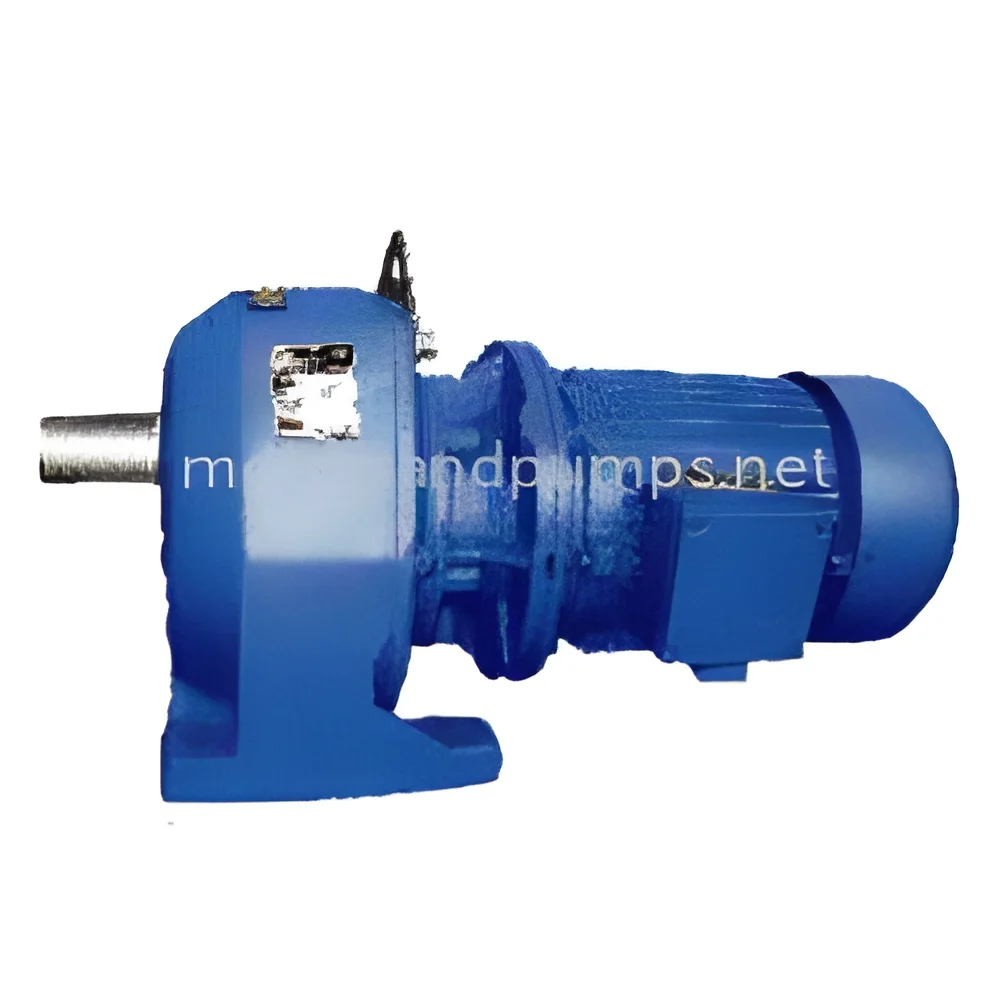
HSC Industrial Fluid Transfer Pumps represent premium-grade fluid handling solutions engineered for exceptional reliability and performance in demanding environments. These heavy-duty pumps are designed to handle various liquids including water, chemicals, and viscous fluids across multiple pressure ranges while maintaining operational consistency. Built with durability as a core principle, they feature robust construction materials that withstand harsh industrial conditions and extended operational cycles. The pumps offer comprehensive customization options to meet specific flow rate, pressure, and material compatibility requirements, ensuring perfect adaptation to diverse industrial settings. Businesses consistently choose HSC Pumps for their proven performance, ease of maintenance, and extended service life, which collectively contribute to reduced total cost of ownership. These versatile units are suitable for both stationary installations and mobile applications, providing excepti...
HSC Industrial Fluid Transfer Pumps represent premium-grade fluid handling solutions engineered for exceptional reliability and performance in demanding environments. These heavy-duty pumps are designed to handle various liquids including water, chemicals, and viscous fluids across multiple pressure ranges while maintaining operational consistency. Built with durability as a core principle, they feature robust construction materials that withstand harsh industrial conditions and extended operational cycles. The pumps offer comprehensive customization options to meet specific flow rate, pressure, and material compatibility requirements, ensuring perfect adaptation to diverse industrial settings. Businesses consistently choose HSC Pumps for their proven performance, ease of maintenance, and extended service life, which collectively contribute to reduced total cost of ownership. These versatile units are suitable for both stationary installations and mobile applications, providing exceptional flexibility in various operational configurations.

Multiple critical industries depend on HSC Pumps for essential fluid handling operations where reliability cannot be compromised. Water treatment facilities utilize these pumps for precise chemical dosing and transfer applications where accuracy and consistent performance are paramount. Manufacturing plants implement them throughout coolant systems, processing lines, and equipment cooling applications where uninterrupted operation is crucial for production continuity. The chemical processing industry benefits significantly from their proven capability to safely handle corrosive, abrasive, and hazardous fluids while maintaining operational integrity. Agricultural operations rely on these pumps for large-scale irrigation systems and precise liquid fertilizer distribution across extensive farming operations. The mining, construction, and energy sectors incorporate HSC Pumps where robust, reliable fluid transfer solutions are essential for operational success and safety compliance.

Businesses achieve substantial operational value through HSC Pumps' demonstrated reliability and significantly reduced maintenance requirements. These pumps are engineered for continuous, uninterrupted operation with minimal downtime, directly supporting enhanced production efficiency and workflow consistency across all applications. Their energy-optimized design helps substantially lower operational costs while consistently maintaining high performance standards across varying load conditions. The extensive customization capabilities ensure seamless integration with existing systems, completely eliminating compatibility concerns and installation challenges. Companies benefit from extended equipment lifespan and dramatically reduced replacement costs due to the pumps' exceptionally durable construction and quality components. Each pump undergoes rigorous quality assurance testing that meets or exceeds industrial standards, providing complete confidence in investment decisions and long-term operational success.

Key Features:
- Heavy-duty construction withstands demanding industrial environments
- Customizable specifications for precise flow rate and pressure requirements
- Broad compatibility with water, chemicals, and viscous fluids
- Energy-efficient operation minimizes power consumption
- Simplified maintenance design with easily accessible components

Benefits:
- Enhanced operational reliability reduces production downtime
- Custom configurations ensure perfect application fit
- Versatile fluid handling capabilities across multiple industries
- Lower energy consumption decreases operational costs
- Extended service life reduces total ownership costs
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
HSC Pumps handle demanding fluid transfer applications across multiple industrial sectors. These heavy-duty pumps efficiently manage water, chemicals, and viscous liquids while maintaining consistent performance in challenging operational conditions. Their robust construction withstands high-pressure requirements while ensuring energy efficiency and reduced maintenance costs for continuous industrial processes.
Customization capabilities allow HSC Pumps to adapt to specific operational requirements across various industries. These pumps integrate seamlessly with existing systems, providing reliable performance for both transfer and circulation applications. Industries benefit from tailored solutions that enhance operational efficiency while maintaining reliability across standard and custom configurations for diverse fluid handling needs.
- Water treatment facilities for chemical dosing and fluid transfer operations
- Manufacturing plants for coolant circulation and processing applications
- Chemical processing for safe handling of corrosive and abrasive substances
- Agricultural operations for efficient irrigation and liquid fertilizer distribution
- HVAC systems for building climate control and water circulation management
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Petece Enviro Engineers, Tamil Nadu
 Tamil Nadu, India
Electronics & Electrical•Trading Company•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Main Markets
North America
Northern Europe
Mid East
Southern Europe
Eastern Europe
South Asia
Western Europe
Africa
Domestic
Industrial Fluid Transfer Pumps Heavy Duty Durable Applications
HSC Industrial Fluid Transfer Pumps deliver heavy-duty performance for demanding applications. Trusted for durability and reliability in chemical processing, water treatment, and manufacturing fluid handling operations.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Petece Enviro Engineers
 Tamil Nadu, India
Electronics & ElectricalTrading Company