IN
₹
Apparel & Fashion
Description
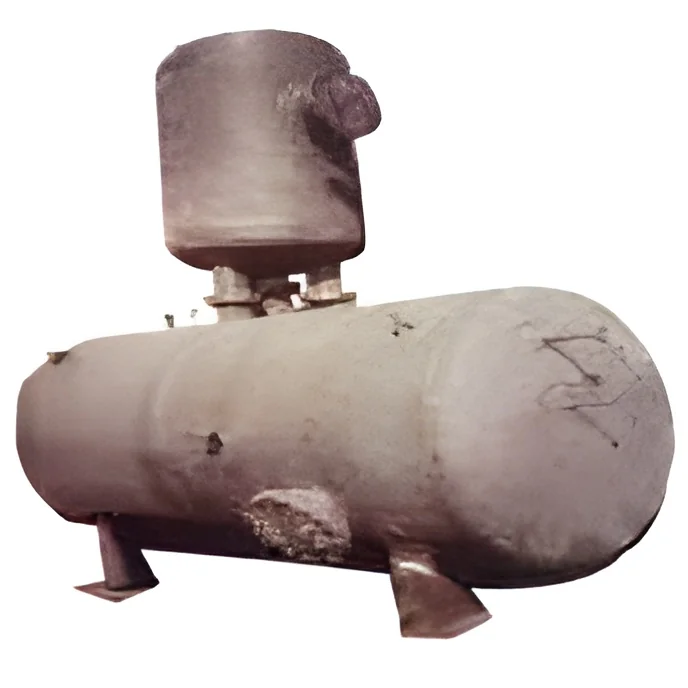
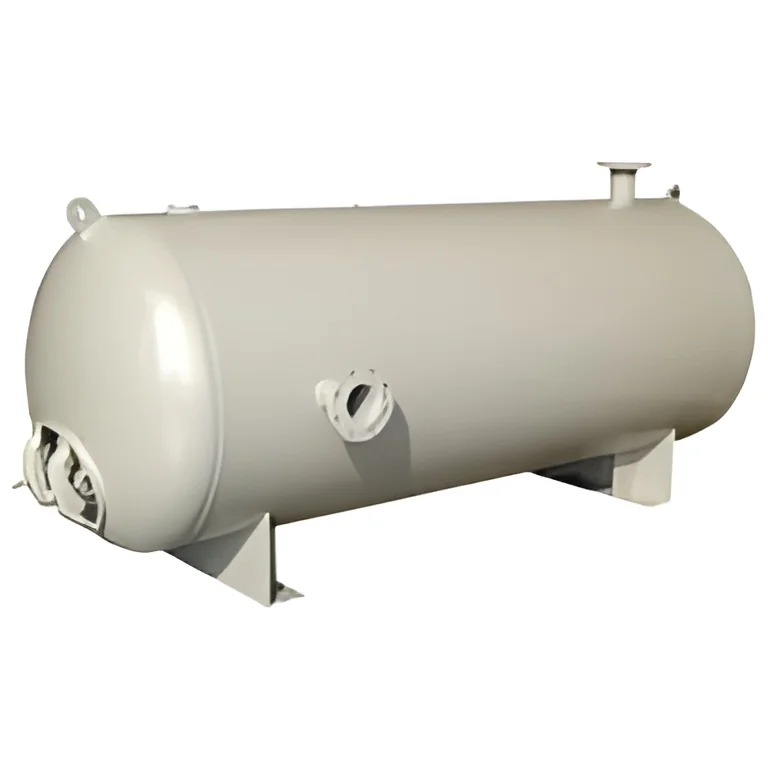
Our industrial horizontal storage tanks represent precision-engineered solutions for secure liquid containment in demanding operational environments. Designed with a focus on reliability and efficiency, these tanks accommodate specific requirements including working temperature ranges, space limitations, and material compatibility. The horizontal configuration offers distinct advantages where vertical space is constrained or where specific gravity flow requirements must be met. Each tank is manufactured to provide secure containment while optimizing available footprint through its intelligent design, incorporating practical considerations for easy installation, maintenance access, and seamless integration with existing industrial systems.

Multiple industries depend on these horizontal storage tanks for their critical liquid management needs. Chemical processing facilities utilize them for safe storage of corrosive and hazardous materials, while water management operations rely on them...
Our industrial horizontal storage tanks represent precision-engineered solutions for secure liquid containment in demanding operational environments. Designed with a focus on reliability and efficiency, these tanks accommodate specific requirements including working temperature ranges, space limitations, and material compatibility. The horizontal configuration offers distinct advantages where vertical space is constrained or where specific gravity flow requirements must be met. Each tank is manufactured to provide secure containment while optimizing available footprint through its intelligent design, incorporating practical considerations for easy installation, maintenance access, and seamless integration with existing industrial systems.

Multiple industries depend on these horizontal storage tanks for their critical liquid management needs. Chemical processing facilities utilize them for safe storage of corrosive and hazardous materials, while water management operations rely on them for both potable water reserves and treatment chemicals. Fuel distribution networks benefit from their robust construction for petroleum products storage and dispensing. Agricultural enterprises use them for irrigation water and fertilizer solutions, and manufacturing plants employ them for process water and industrial fluid containment. The food processing sector utilizes food-grade certified versions for edible liquids, ensuring compliance with stringent hygiene and safety standards.

These storage tanks deliver exceptional value through their durability and operational reliability, significantly reducing replacement cycles and minimizing system downtime. Built to withstand demanding industrial environments, they offer long-term performance with minimal maintenance requirements. The robust construction guarantees safety and regulatory compliance across various applications. Operations benefit from reduced handling risks, improved storage efficiency, and enhanced system integration capabilities that contribute to overall operational excellence and cost-effectiveness. The tanks' design prioritizes user safety and environmental protection while maintaining consistent performance under varying operational conditions.

Key Features:
- Customizable capacity configurations to meet specific volume requirements
- Temperature-resistant construction suitable for diverse operational environments
- Robust horizontal design optimized for space efficiency and stability
- Multiple material compatibility options for various liquid types
- Integrated access points and fittings for maintenance and monitoring

Benefits:
- Enhanced operational safety through secure containment and reduced handling risks
- Improved storage efficiency with space-optimized horizontal design
- Long-term reliability minimizing replacement costs and operational downtime
- Flexible integration with existing systems and workflows
- Compliance with industry standards and regulatory requirements
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Industrial horizontal storage tanks provide versatile and secure containment for a wide range of liquids across multiple sectors. Their robust construction and adaptable design make them suitable for both temporary setups and permanent installations, ensuring reliable performance in diverse environmental conditions. These tanks are engineered to meet specific material compatibility needs while optimizing available space through their horizontal orientation.
These storage solutions integrate seamlessly with existing industrial systems, offering practical access points for maintenance, monitoring, and efficient liquid management. Industries value their ability to conform to unique site layouts and operational workflows. The tanks support continuous operations by providing safe, compliant storage that minimizes handling risks and maintains product integrity throughout the storage cycle.
- Chemical manufacturing plants use these tanks for safe storage of acids, solvents, and reactive process liquids
- Municipal and industrial water treatment facilities rely on them for potable water reserves and chemical treatment solutions
- Fuel distribution centers and transportation hubs utilize them for storing diesel, petrol, and lubricating oils
- Agricultural operations employ them for large-scale irrigation water storage and liquid fertilizer containment
- Food production facilities use food-grade certified versions for edible oils, syrups, and beverage ingredients
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Anish Enterprises, Maharashtra
 Maharashtra, India
Raw Materials & Chemicals•Manufacturer•Trading Company•Distributor / Wholesaler
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Main Markets
Domestic
Industrial Horizontal Storage Tanks For Chemicals Water Fuel
Industrial horizontal storage tanks for chemicals, water, and fuel storage. Reliable, efficient solutions with customizable capacity and temperature specifications to meet specific operational requirements.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Anish Enterprises
 Maharashtra, India
Raw Materials & ChemicalsManufacturer