IN
₹
Apparel & Fashion
Description
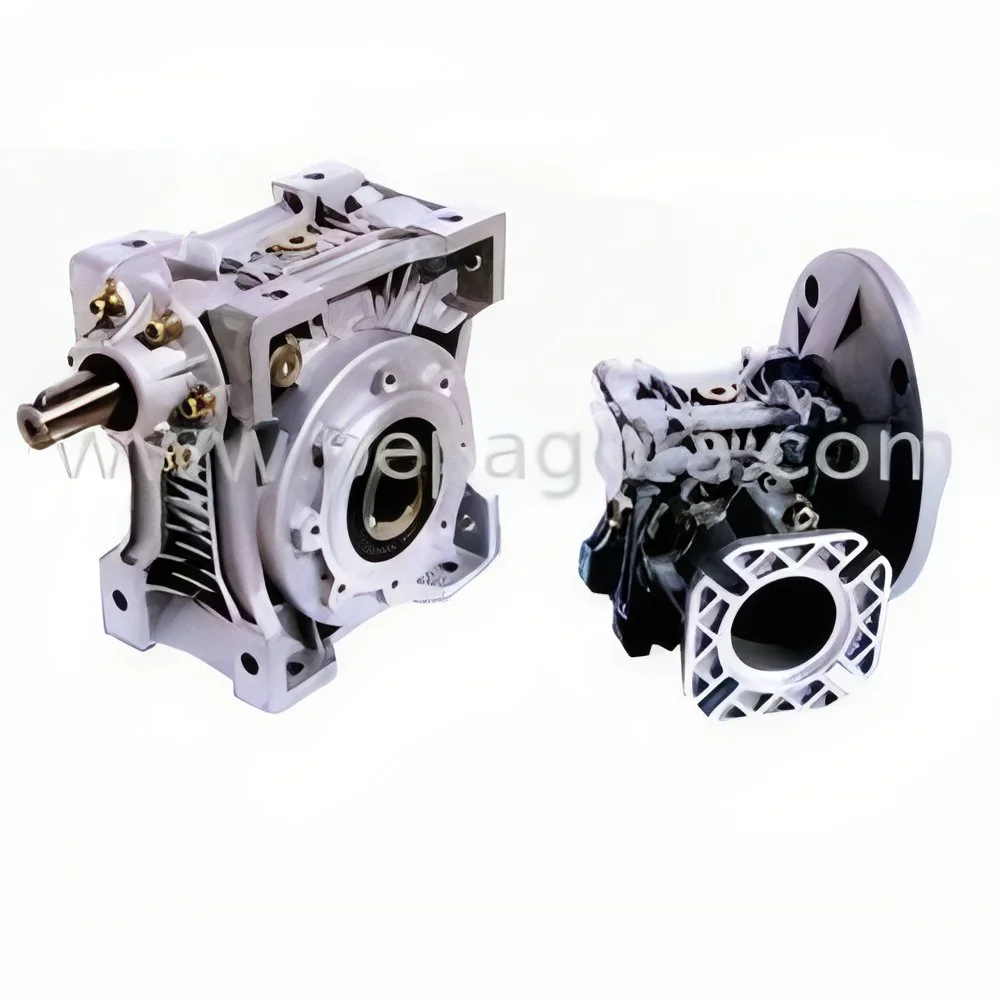
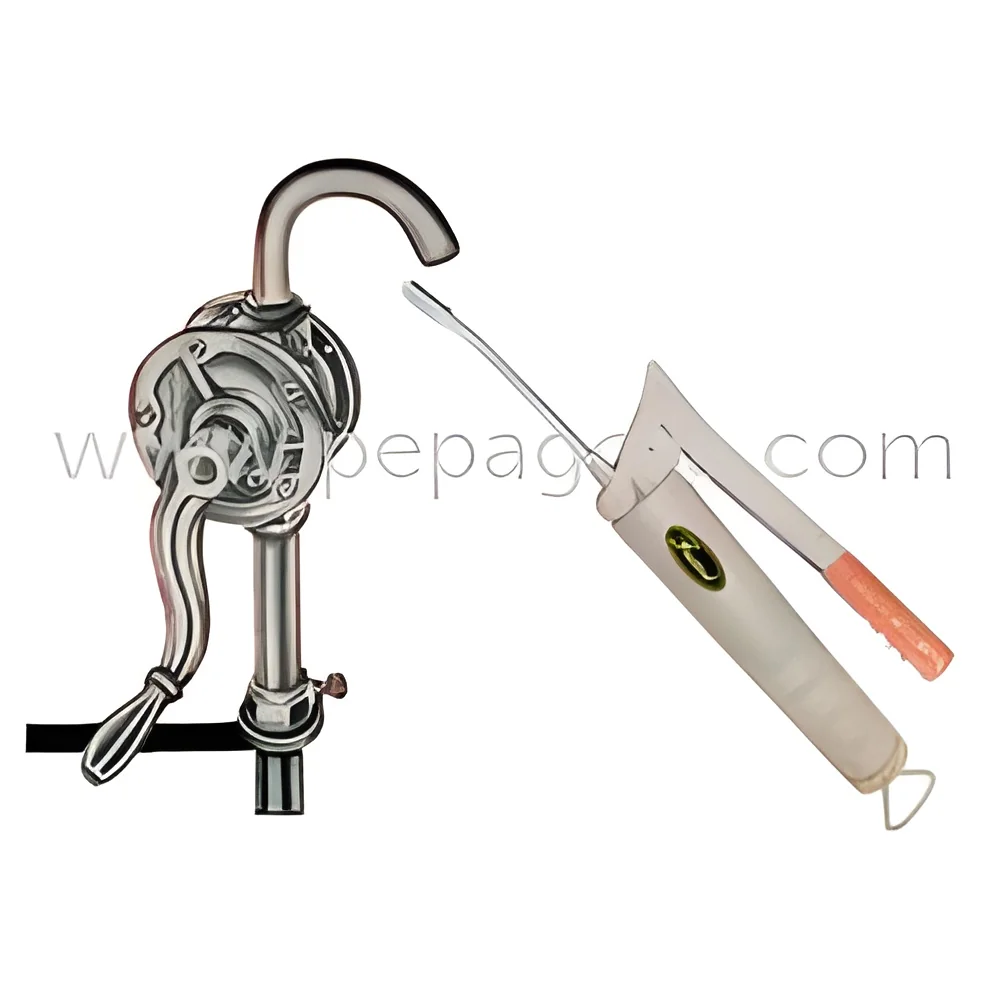
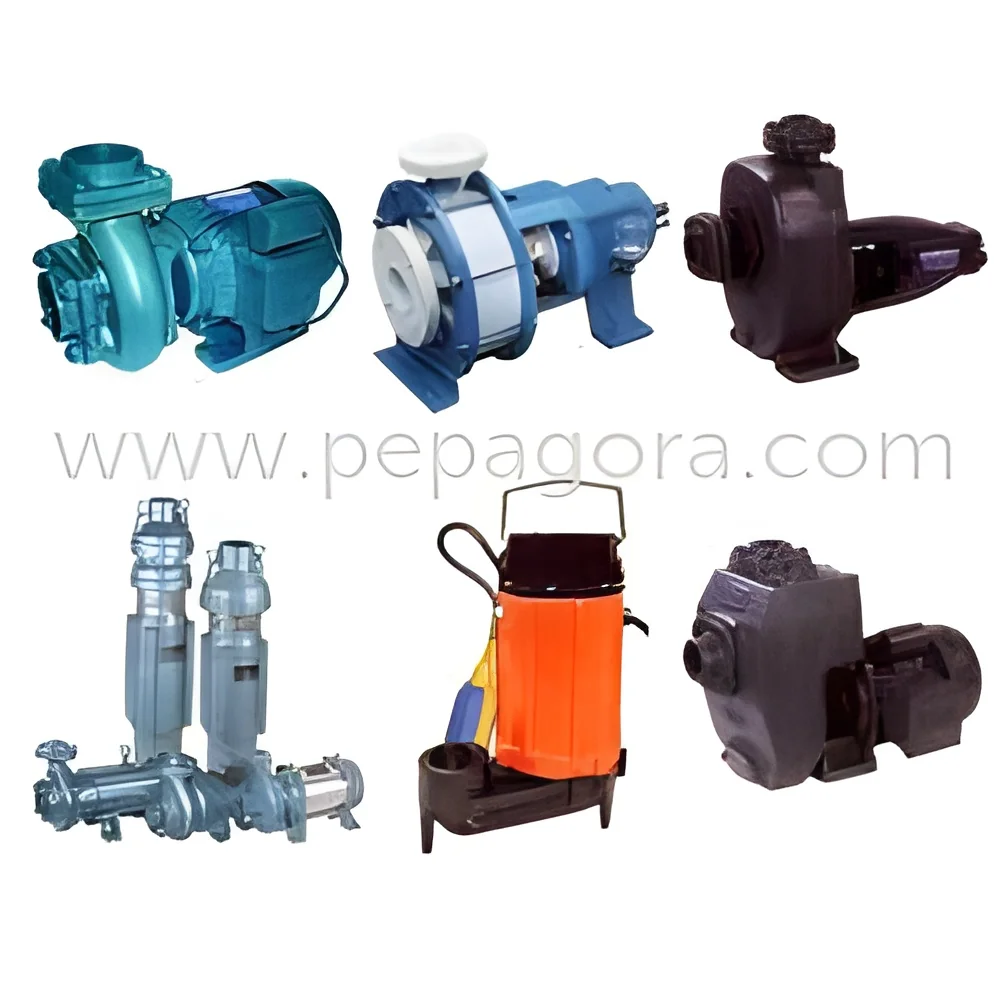
Our industrial gear and chemical pumps represent advanced fluid handling technology designed for demanding applications. Engineered with precision and built from corrosion-resistant materials, these pumps deliver reliable performance when transferring aggressive chemicals, viscous substances, and abrasive materials. The advanced construction ensures consistent flow rates and pressure capabilities even in challenging environments. Rigorous testing guarantees each pump meets high standards for quality and durability before installation, providing confidence in their long-term operation and minimal maintenance requirements.

These pumps serve critical functions across essential industries. In chemical processing, they safely transfer corrosive substances without degradation. Water treatment facilities utilize them for accurate chemical dosing and efficient fluid movement. Pharmaceutical manufacturing benefits from their precision capabilities for sensitive fluid handling. The food product...
Our industrial gear and chemical pumps represent advanced fluid handling technology designed for demanding applications. Engineered with precision and built from corrosion-resistant materials, these pumps deliver reliable performance when transferring aggressive chemicals, viscous substances, and abrasive materials. The advanced construction ensures consistent flow rates and pressure capabilities even in challenging environments. Rigorous testing guarantees each pump meets high standards for quality and durability before installation, providing confidence in their long-term operation and minimal maintenance requirements.

These pumps serve critical functions across essential industries. In chemical processing, they safely transfer corrosive substances without degradation. Water treatment facilities utilize them for accurate chemical dosing and efficient fluid movement. Pharmaceutical manufacturing benefits from their precision capabilities for sensitive fluid handling. The food production sector relies on their reliable operation for ingredient transfer, while general industrial applications depend on them for various process fluids where consistent performance is vital for operational continuity and output quality.

The value of these pumps lies in their exceptional reliability, reduced maintenance needs, and extended service life, which contribute to a lower total cost of ownership. Their robust design minimizes unexpected downtime, ensuring your critical processes run continuously. The energy-efficient operation helps reduce ongoing power consumption. Engineered to handle challenging applications with consistent performance, they provide operational stability and peace of mind. Their proven track record across industries demonstrates tangible value through reliable operation, reduced maintenance costs, and dependable service.

Key Features:
- Corrosion-resistant construction for handling aggressive chemicals and fluids
- Precision engineering ensuring consistent performance and extended service life
- Advanced sealing systems to prevent leaks and contamination
- Robust design built for demanding industrial environments
- Energy-efficient operation for reduced power consumption

Benefits:
- Reliable fluid transfer minimizing operational disruptions and downtime
- Long service life reducing replacement frequency and total cost
- Safe handling of aggressive and sensitive fluids for various processes
- Consistent performance ensuring production quality and continuity
- Durable construction requiring minimal maintenance over time
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Our industrial gear and chemical pumps are engineered for demanding environments where reliable fluid transfer is non-negotiable. They handle aggressive chemicals, viscous fluids, and abrasive slurries with consistent performance, maintaining efficiency under continuous operation in harsh conditions. Their robust construction ensures minimal downtime, making them a trusted component in critical processes where failure would disrupt operations.
These units serve vital roles across multiple sectors including chemical processing, water treatment, pharmaceuticals, and general manufacturing. The pumps adapt to specific operational needs with their reliable performance, ensuring safe and efficient movement of various fluids. Industries rely on them for processes where precision, durability, and consistent output are essential for maintaining production quality and operational continuity.
- Chemical processing plants for safe transfer of acids, solvents, and corrosive liquids
- Water and wastewater treatment facilities for chemical dosing and fluid movement
- Pharmaceutical manufacturing for handling sensitive fluids with precision
- Food production facilities for transferring ingredients and food-grade products
- Industrial settings for managing abrasive slurries and various process fluids
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Metal Bond (India), Punjab
 Punjab, India
Construction•Distributor / Wholesaler•Retailer
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Industrial Gear And Chemical Pumps For Fluid Transfer And Wastewater
Industrial gear and chemical pumps for reliable fluid transfer and wastewater management. Built with corrosion-resistant materials for long service life in demanding industrial applications.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Metal Bond (India)
 Punjab, India
ConstructionDistributor / Wholesaler