IN
₹
Apparel & Fashion
Description
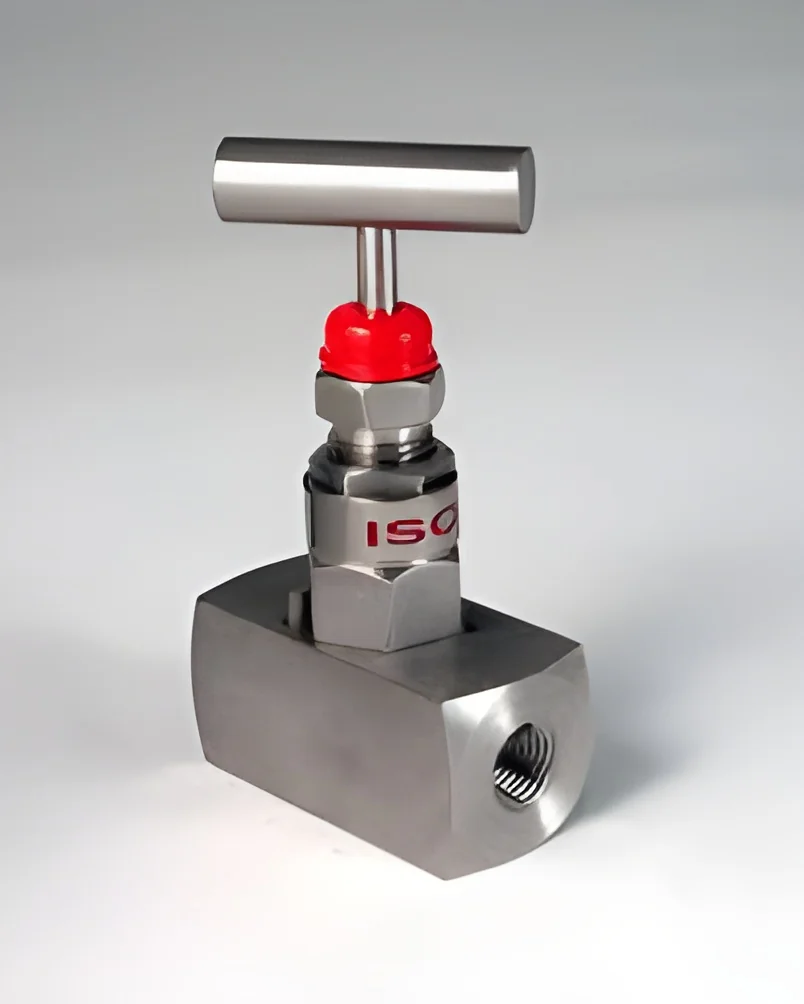
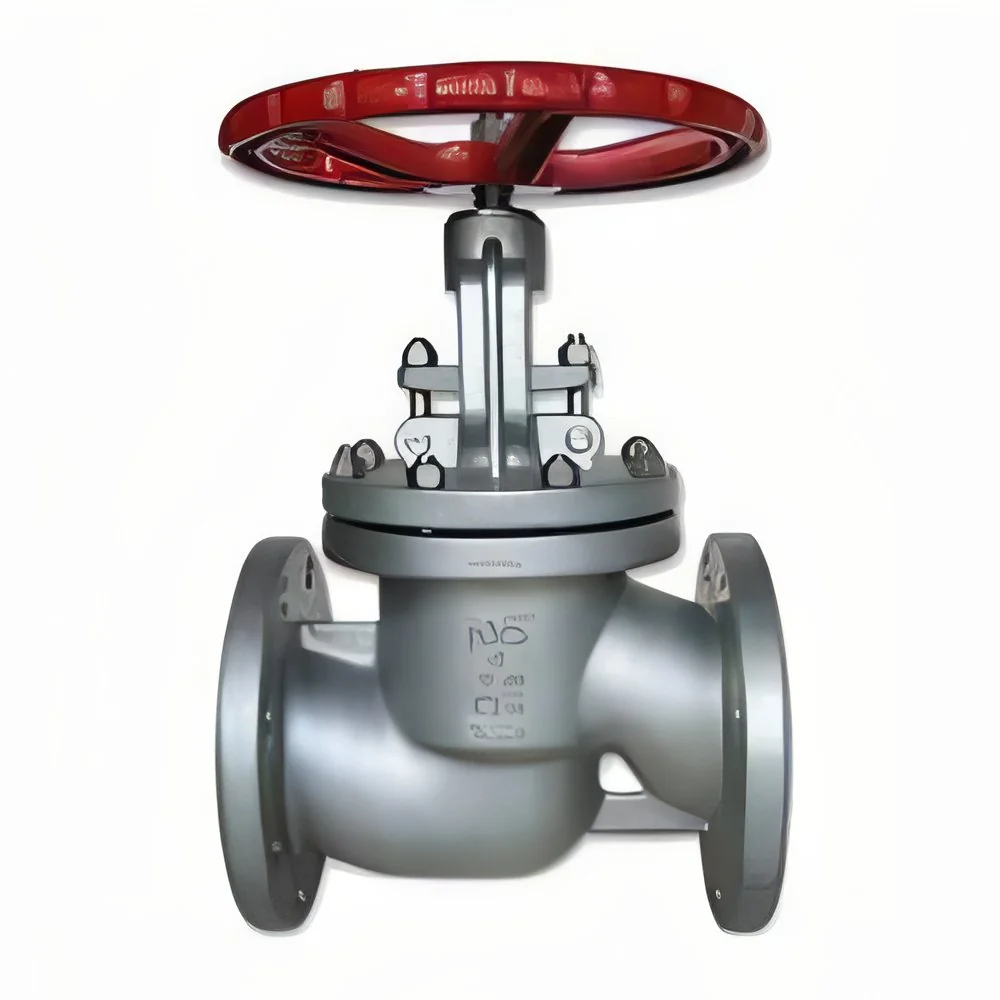
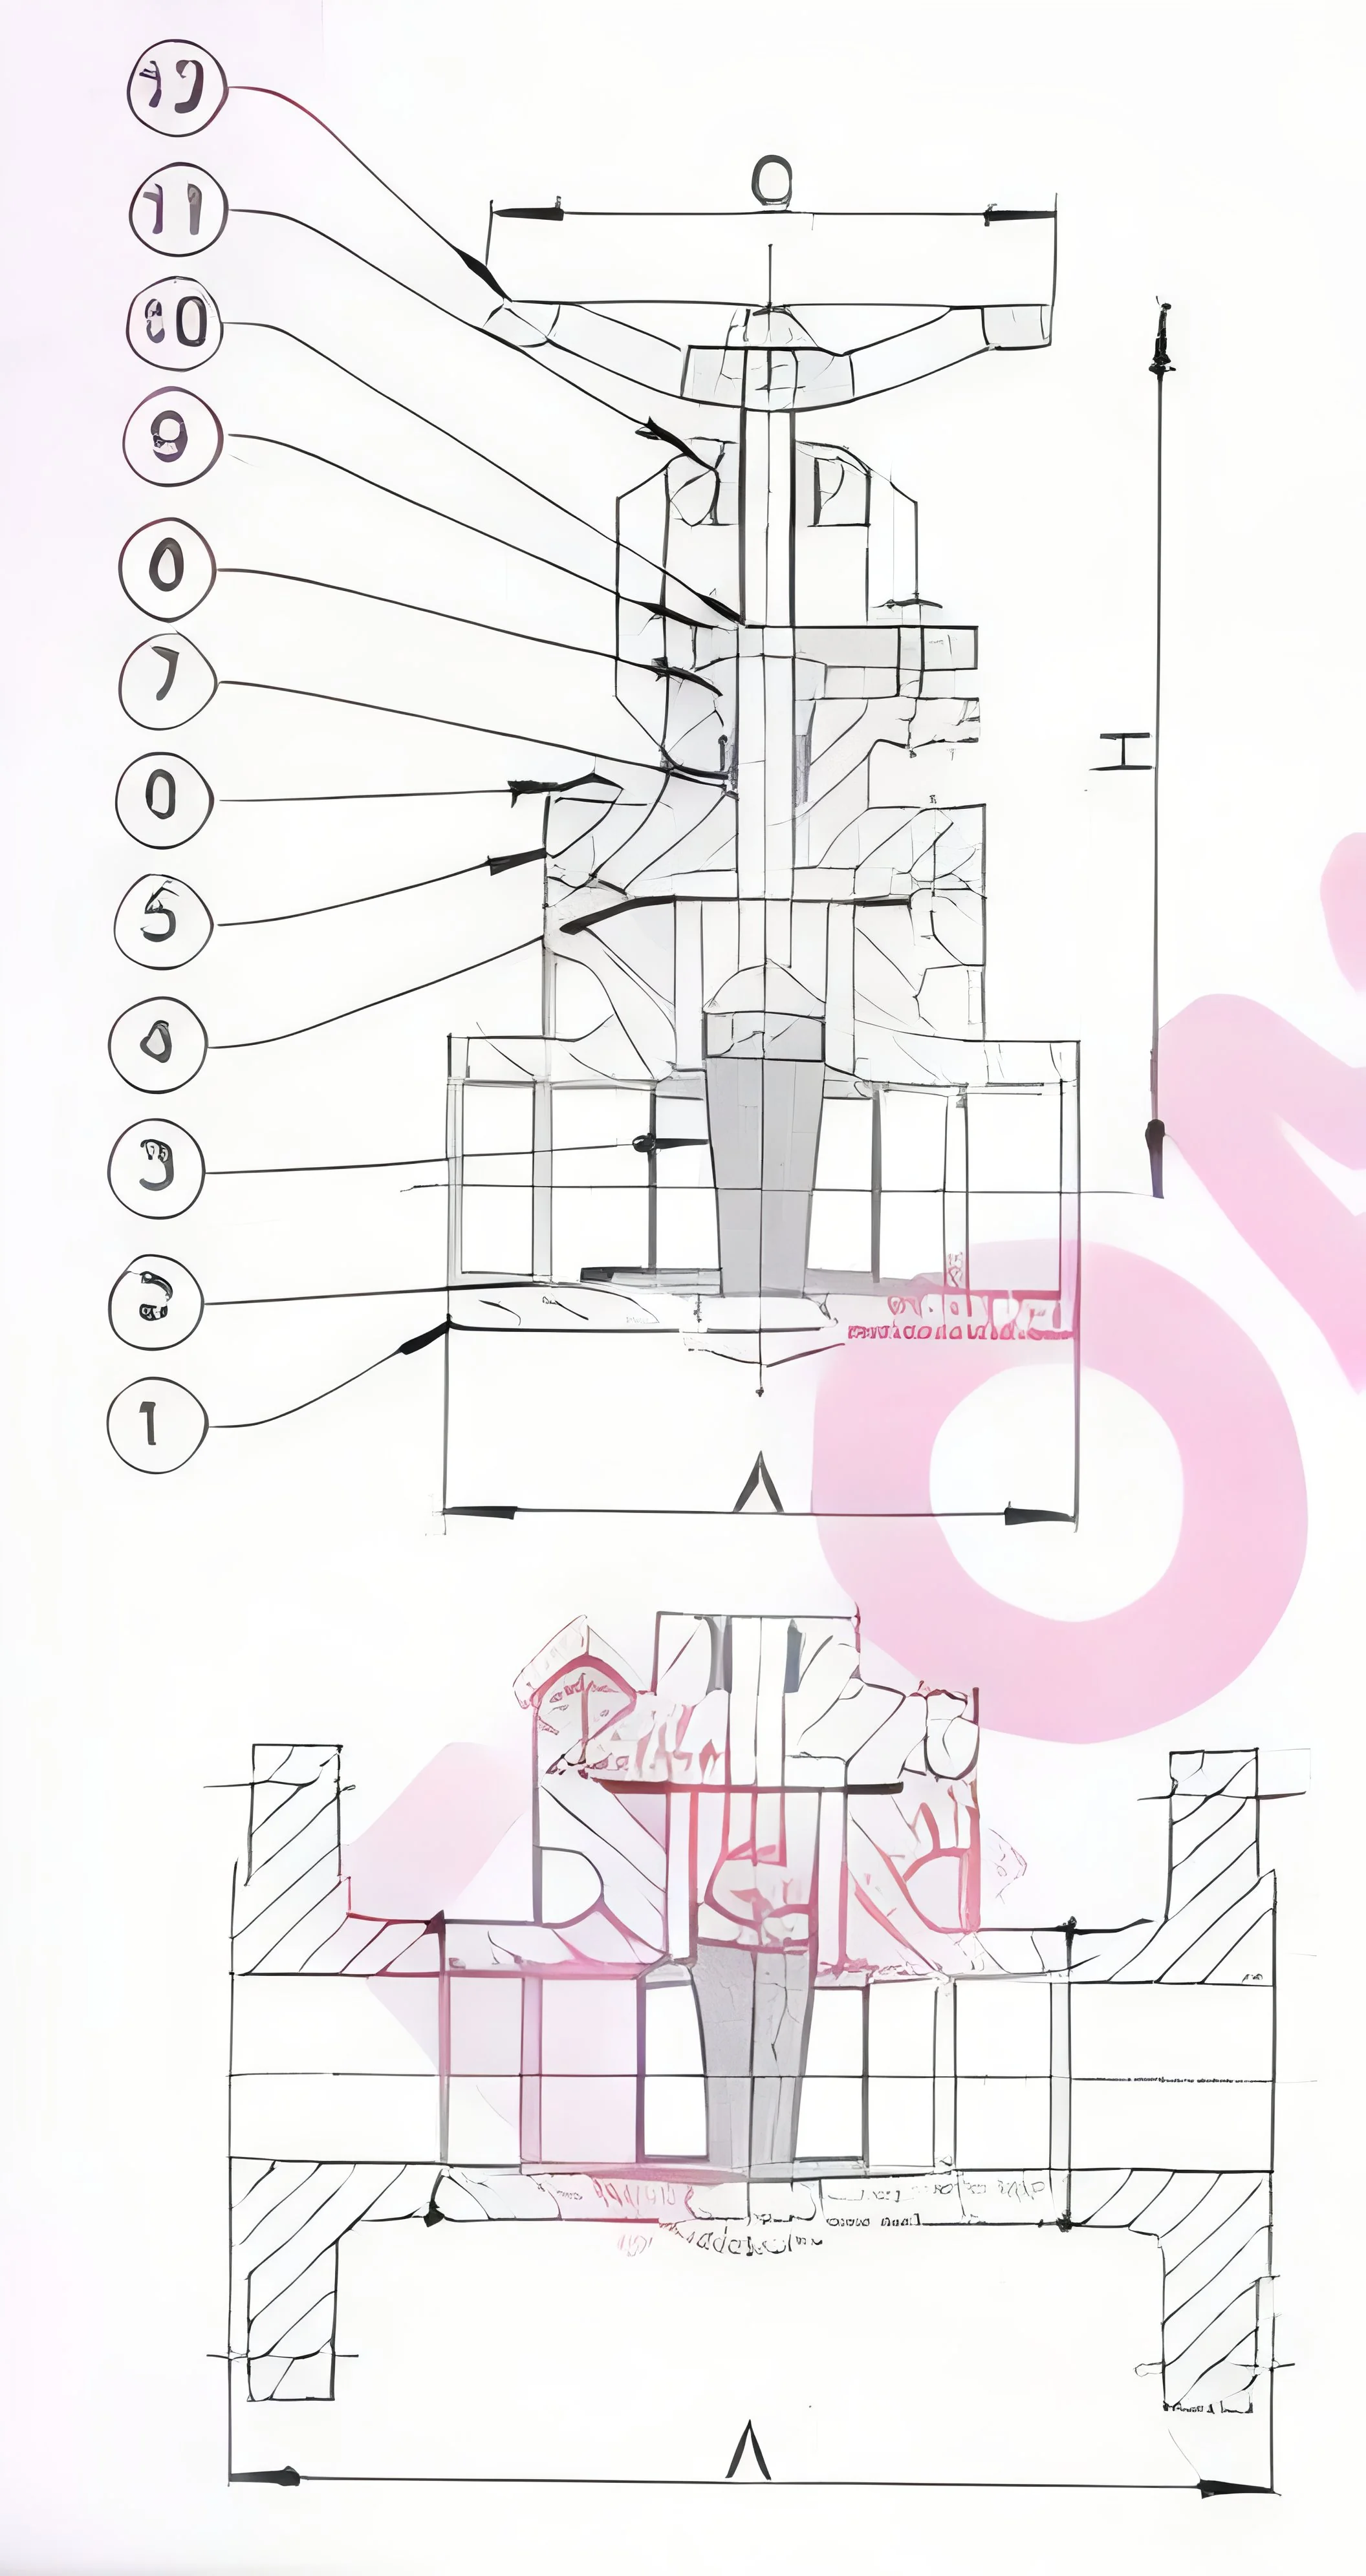
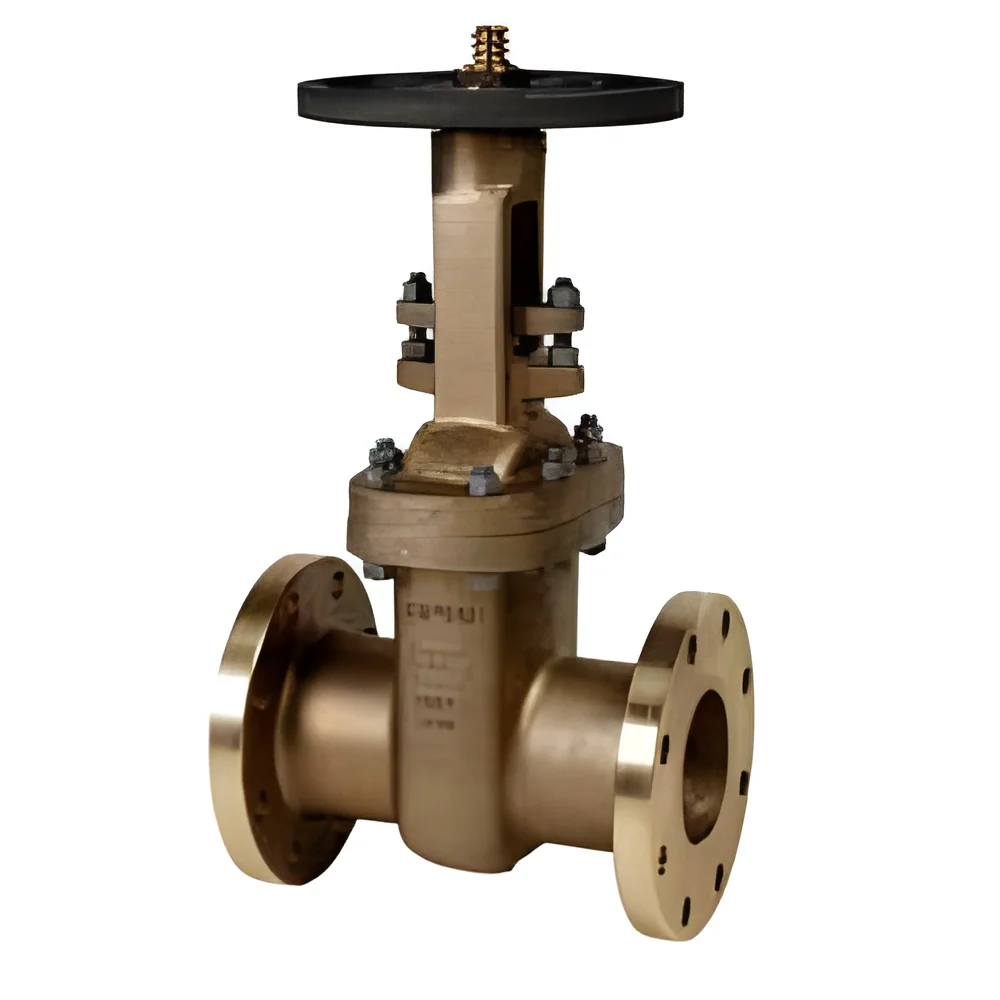
Industrial gate valves, also known as slide or knife valves, are fundamental components designed for precise on/off control and complete isolation in fluid handling systems. Their primary function is to either permit unobstructed flow or provide a leak-tight seal to halt it entirely. The mechanism employs a flat disc or wedge (the gate) that moves linearly, perpendicular to the flow direction, rising into a bonnet when open and lowering into a seat when closed. This design is celebrated for creating a straight-through flow path with minimal turbulence, resulting in virtually zero pressure drop when the valve is in the fully open position. Engineered for durability, these valves are built to perform reliably in some of the most challenging industrial environments, offering a straightforward yet highly effective solution for critical flow management tasks.

The usage of industrial gate valves spans a wide spectrum of sectors where reliable fluid control is paramount. In the oil and gas i...
Industrial gate valves, also known as slide or knife valves, are fundamental components designed for precise on/off control and complete isolation in fluid handling systems. Their primary function is to either permit unobstructed flow or provide a leak-tight seal to halt it entirely. The mechanism employs a flat disc or wedge (the gate) that moves linearly, perpendicular to the flow direction, rising into a bonnet when open and lowering into a seat when closed. This design is celebrated for creating a straight-through flow path with minimal turbulence, resulting in virtually zero pressure drop when the valve is in the fully open position. Engineered for durability, these valves are built to perform reliably in some of the most challenging industrial environments, offering a straightforward yet highly effective solution for critical flow management tasks.

The usage of industrial gate valves spans a wide spectrum of sectors where reliable fluid control is paramount. In the oil and gas industry, they are indispensable for pipeline isolation, wellhead control, and refinery operations, handling everything from crude to refined products. Water and wastewater treatment facilities utilize them to isolate sections of piping for maintenance, control flow into treatment basins, and manage distribution networks. Chemical and petrochemical plants rely on their sealing capability to safely contain aggressive and hazardous fluids. Furthermore, they are integral to power generation for managing steam and coolant lines, and in general manufacturing for processes involving various process media. Their robust design makes them suitable for applications involving high pressure, high temperature, and even abrasive or viscous fluids, confirming their status as a versatile and trusted hardware.

The inherent business value of these gate valves is rooted in their reliability, operational efficiency, and contribution to system longevity. By providing a bubble-tight seal, they prevent product loss and environmental contamination, directly impacting safety and regulatory compliance. Their simple, robust construction translates to lower lifetime costs through reduced maintenance frequency and extended service intervals. The zero-pressure-drop characteristic when fully open optimizes overall system efficiency, reducing pumping costs and energy consumption. For procurement specialists and plant managers, this means a dependable component that minimizes unplanned downtime, enhances operational safety, and delivers a strong return on investment through sustained, trouble-free performance.

Key Features:
- Linear motion gate mechanism designed for full open or full closed operation, ensuring precise flow control.
- Straight-through flow design that minimizes resistance and provides near-zero pressure drop when fully open.
- Robust body and trim construction from durable materials, built to withstand high-pressure and high-temperature service conditions.
- Engineered for a tight, leak-proof seal in the closed position, offering reliable isolation of process fluids.
- Available in various sizes, pressure ratings, and material specifications to match specific system requirements.

Benefits:
- Ensures maximum flow efficiency with minimal pressure loss, reducing energy costs in pumping systems.
- Provides secure, leak-tight isolation for maintenance, safety, and process control, enhancing operational integrity.
- Delivers long service life and durability in demanding environments, lowering total cost of ownership.
- Simple and reliable design minimizes operational complexity and reduces the potential for failure.
- Versatile application across multiple industries from oil and gas to water treatment, offering a proven solution for fluid management.
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Industrial gate valves are engineered for applications requiring absolute flow control and secure isolation of liquids and gases. Their linear motion design allows a flat gate to slide perpendicularly into the flow path, making them ideal for operations that are either fully open or fully closed. This functionality is critical for maintaining system integrity, preventing leaks, and ensuring operational safety in high-stakes environments where fluid management is non-negotiable.
These robust valves serve as reliable workhorses across demanding sectors. Their construction withstands high pressures and temperatures, making them suitable for the rigorous conditions found in pipeline transmission, processing plants, and utility networks. From managing the flow of crude oil to isolating sections of a municipal water supply, their durability and tight-sealing capability provide long service life and reduce the need for frequent maintenance, delivering consistent performance where it matters most.
- Isolating and controlling crude oil and natural gas flow within pipeline transmission and distribution networks.
- Sectional isolation in municipal water supply and wastewater treatment systems for maintenance and emergency protocols.
- Managing the transfer of chemicals, acids, and solvents in processing and manufacturing plants to ensure safe containment.
- Regulating steam, feedwater, and coolant flows in thermal power generation and industrial boiler systems.
- Handling abrasive slurries, viscous fluids, and process media in mining, pulp and paper, and heavy manufacturing operations.
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Flomech Valves, West Bengal
 West Bengal, India
Industrial Equipment & Machinery•Manufacturer•Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Industrial Gate Valves For Fluid Flow Control And Isolation
Premium industrial gate valves for precise fluid flow control and complete isolation in oil, gas, water, and chemical industries. These slide valves ensure zero pressure drop when fully open and reliable shutoff.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Flomech Valves
 West Bengal, India
Industrial Equipment & MachineryManufacturer