IN
₹
Apparel & Fashion
Description
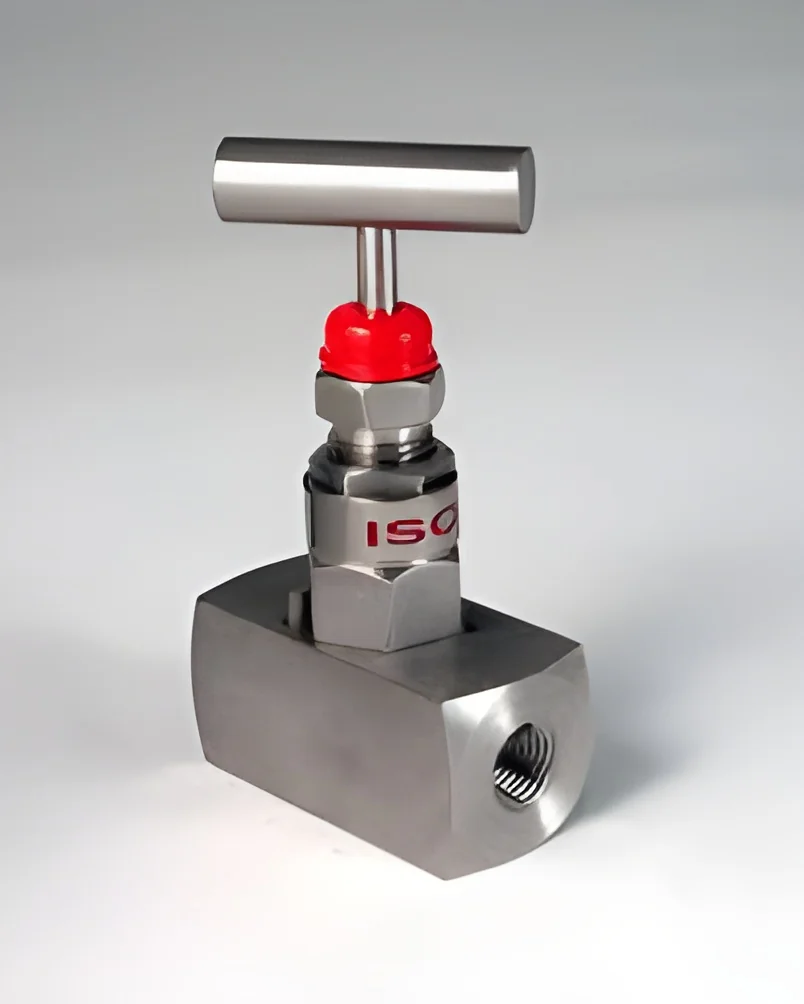
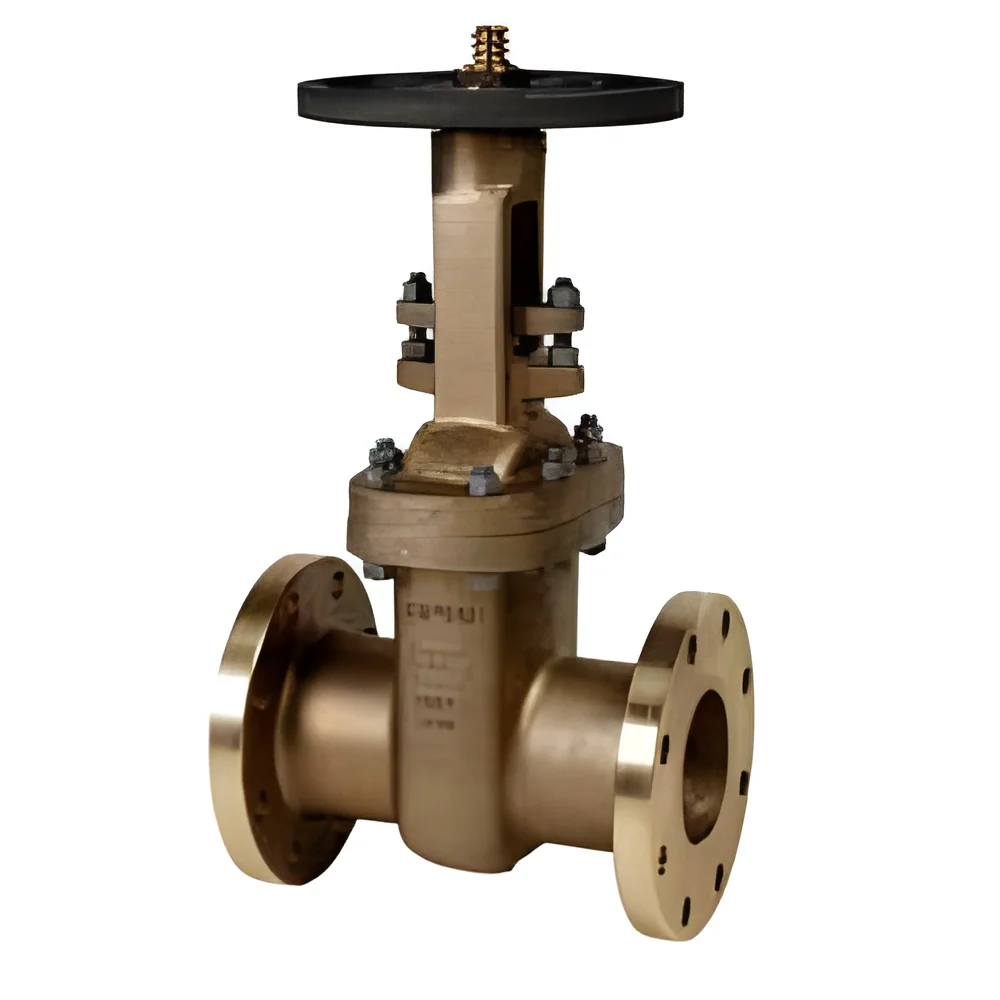
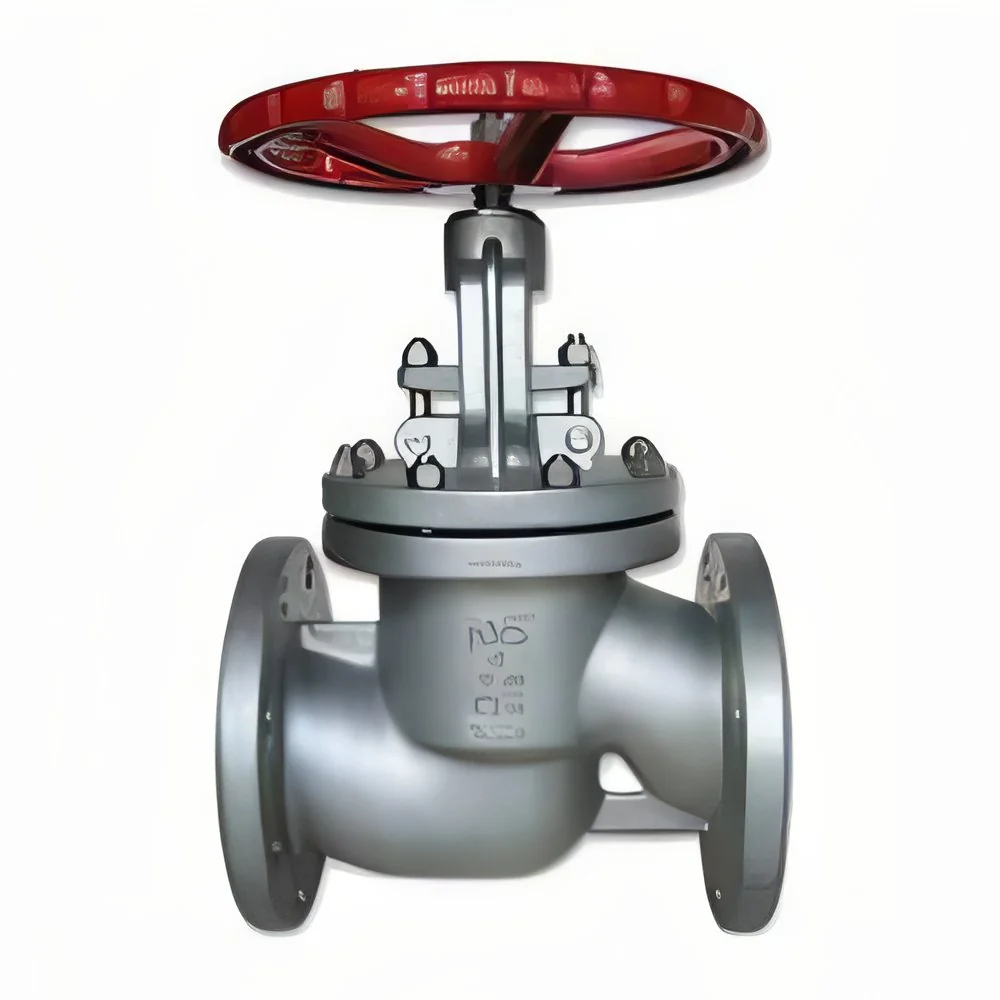
Engineered for superior performance, these industrial globe valves are the definitive solution for precise flow control in high-pressure applications. They are constructed from premium materials and are available in multiple operational patterns—including angle, oblique, straight, and needle designs—to suit specific system layouts and control requirements. Each valve is precision-built to offer exceptional sealing, reliable shut-off, and accurate flow modulation, ensuring dependable operation when managing water, steam, oil, and other industrial media. Their robust design is focused on delivering longevity and consistent performance, reducing the risk of failure in critical processes.

These valves are integral components across heavy industries that depend on flawless fluid management. In the oil and gas sector, they are deployed in pipelines, refineries, and offshore platforms for isolation and regulation. Power generation facilities utilize them extensively in boiler feed systems, t...
Engineered for superior performance, these industrial globe valves are the definitive solution for precise flow control in high-pressure applications. They are constructed from premium materials and are available in multiple operational patterns—including angle, oblique, straight, and needle designs—to suit specific system layouts and control requirements. Each valve is precision-built to offer exceptional sealing, reliable shut-off, and accurate flow modulation, ensuring dependable operation when managing water, steam, oil, and other industrial media. Their robust design is focused on delivering longevity and consistent performance, reducing the risk of failure in critical processes.

These valves are integral components across heavy industries that depend on flawless fluid management. In the oil and gas sector, they are deployed in pipelines, refineries, and offshore platforms for isolation and regulation. Power generation facilities utilize them extensively in boiler feed systems, turbine bypass lines, and cooling circuits. The chemical processing industry relies on their capability to handle aggressive and hazardous fluids safely. Furthermore, they are essential in water treatment plants for accurate flow control and in large commercial or industrial HVAC systems for managing heating and cooling distribution, proving their versatility and reliability.

The inherent value of these globe valves lies in their direct contribution to operational safety, efficiency, and cost-effectiveness. Their reliable, leak-proof performance minimizes unplanned downtime and maintenance interventions, leading to a lower total cost of ownership over the valve's lifecycle. The availability of different patterns and specifications allows for optimal integration into existing systems, enhancing process stability without compromise. This reliability under fluctuating pressures ensures consistent process outcomes, protecting valuable infrastructure and ensuring continuity in operations where system failure carries significant risk.

Key Features:
- Constructed from high-grade materials for maximum durability and corrosion resistance.
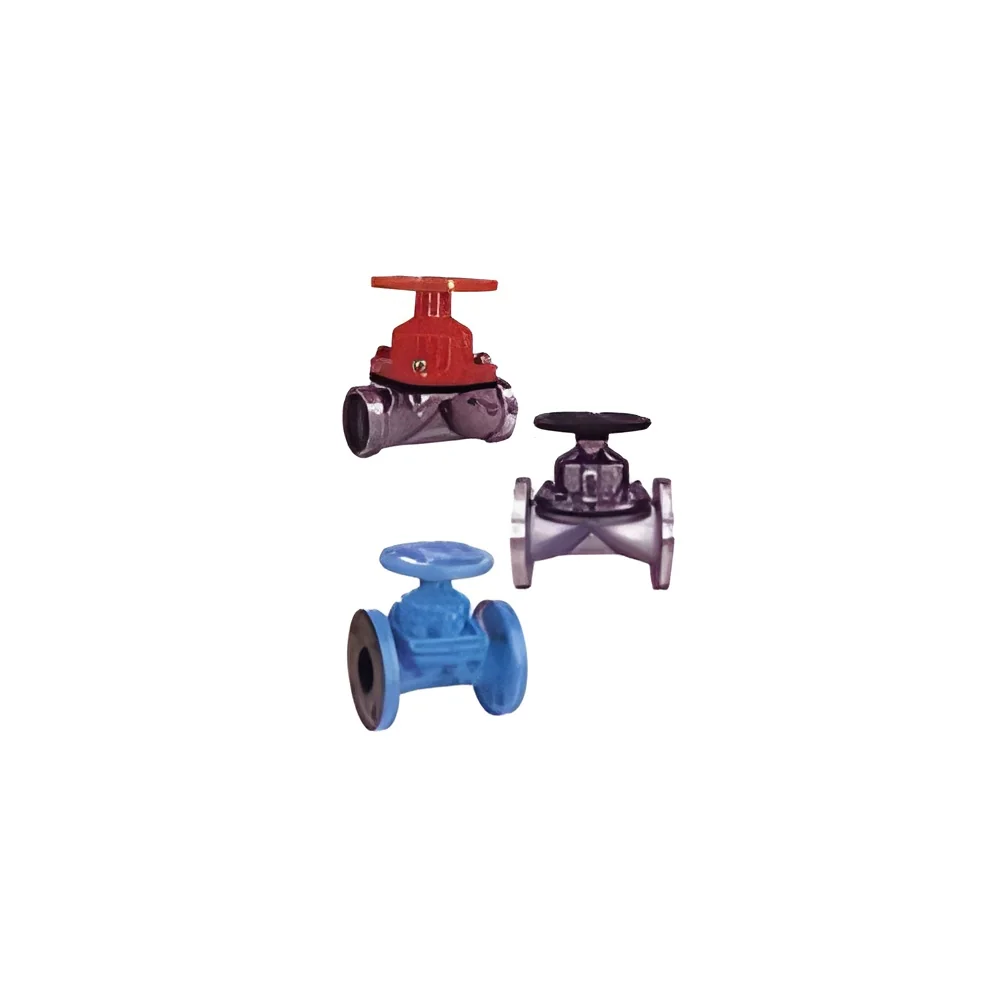
- Available in angle, oblique, straight, and needle patterns to fit various piping configurations.
- Precision-engineered for accurate flow throttling and bubble-tight shut-off capability.
- Robust design validated for reliable operation in high-pressure and high-temperature environments.
- Engineered for long service life with consistent performance across diverse industrial media.

Benefits:
- Enhances process safety and system integrity with reliable, leak-proof operation.
- Reduces maintenance costs and operational downtime through durable, long-lasting construction.
- Delivers precise flow control for optimized process efficiency and consistent output.
- Provides versatile application across multiple industries due to its robust and adaptable design.
- Offers a dependable solution that lowers the total cost of ownership by minimizing replacements and repairs.
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Industrial globe valves provide essential flow regulation where precision and reliability are non-negotiable. Their design allows for accurate throttling and secure shut-off of liquids, gases, and steam, maintaining consistent operation under high pressure and variable temperatures. This makes them a cornerstone for system integrity and safety.
These versatile valves support a wide range of critical sectors due to their robust construction and adaptability. They are engineered to meet the stringent demands of industries where controlling fluid flow directly impacts process efficiency, safety protocols, and operational uptime, ensuring long-term service in challenging environments.
- Regulating and isolating flow in oil and gas pipeline transmission and distribution systems.
- Managing steam and feedwater circuits within power generation plants and boiler systems.
- Handling corrosive chemicals and aggressive process fluids in chemical manufacturing plants.
- Controlling water flow for filtration, dosing, and distribution in municipal and industrial water treatment facilities.
- Modulating coolant and heating media in large-scale HVAC and industrial cooling systems.
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Flomech Valves, West Bengal
 West Bengal, India
Industrial Equipment & Machinery•Manufacturer•Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Industrial Globe Valves For High Pressure Flow Control
Industrial Globe Valves for high-pressure flow control deliver precise regulation in demanding systems. Available in angle, oblique, straight, and needle patterns, these reliable valves are built for industrial fluid management applications requiring durability and performance.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Flomech Valves
 West Bengal, India
Industrial Equipment & MachineryManufacturer