IN
₹
Apparel & Fashion

Description
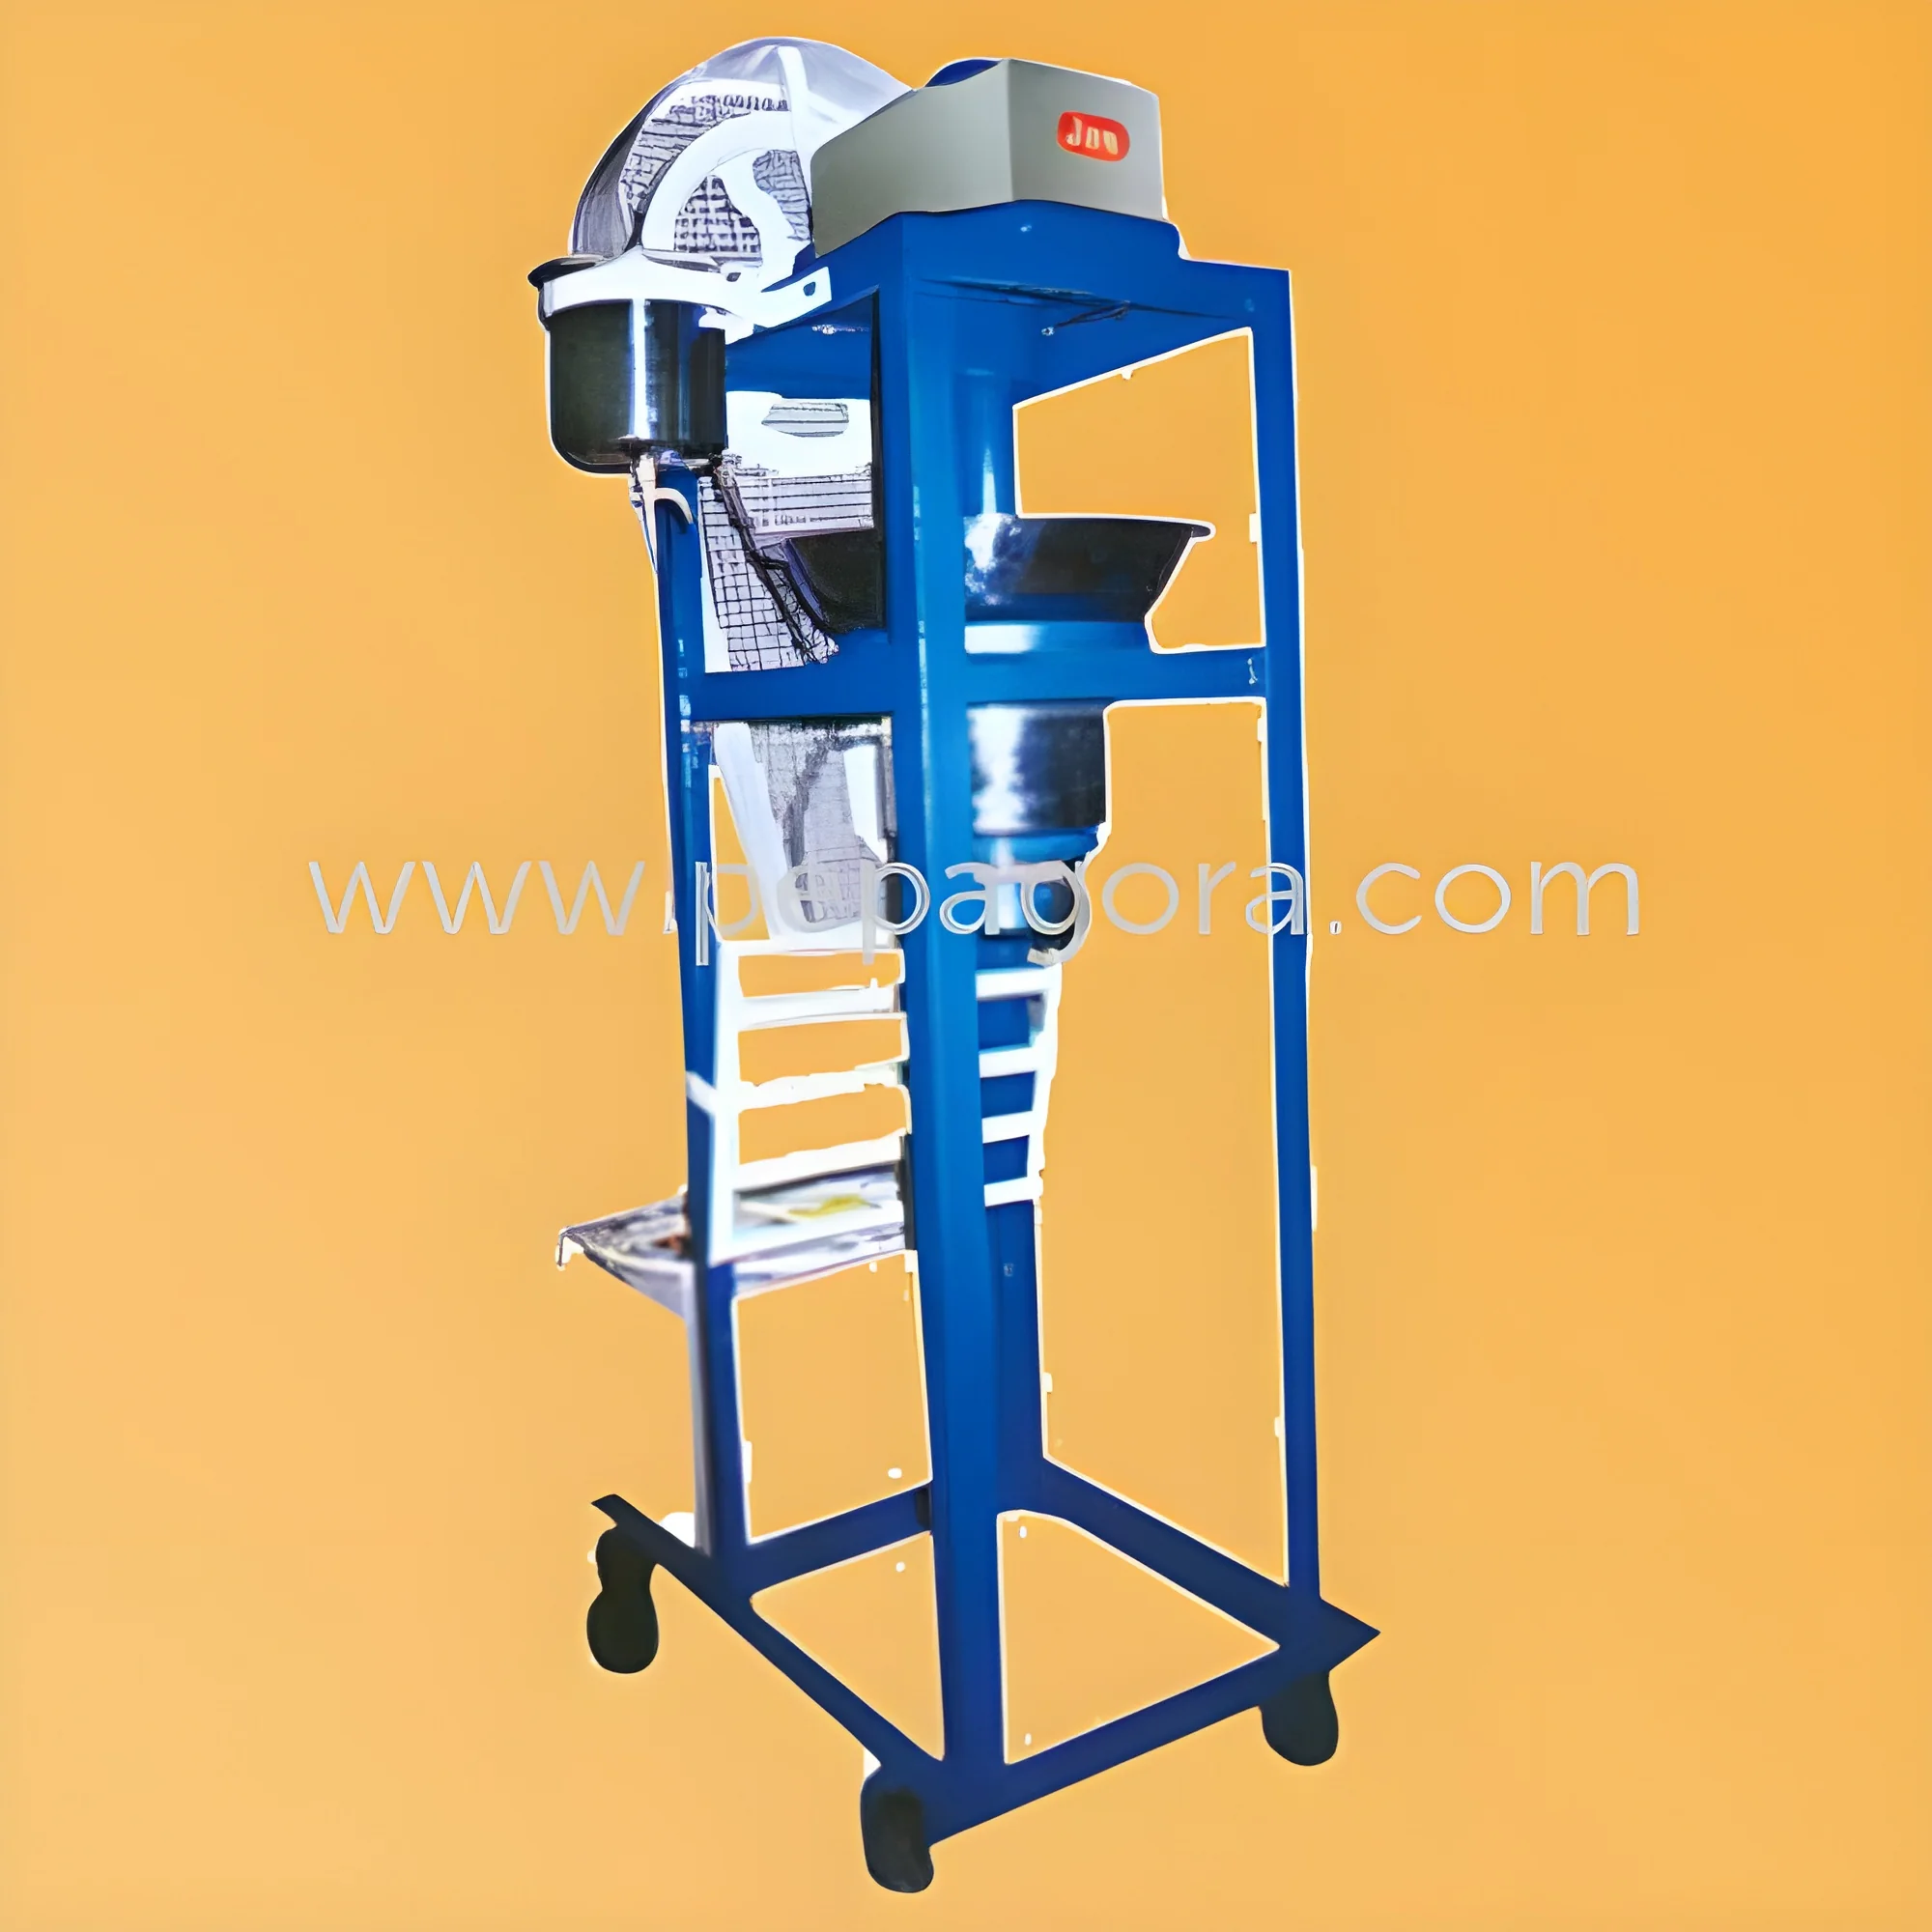
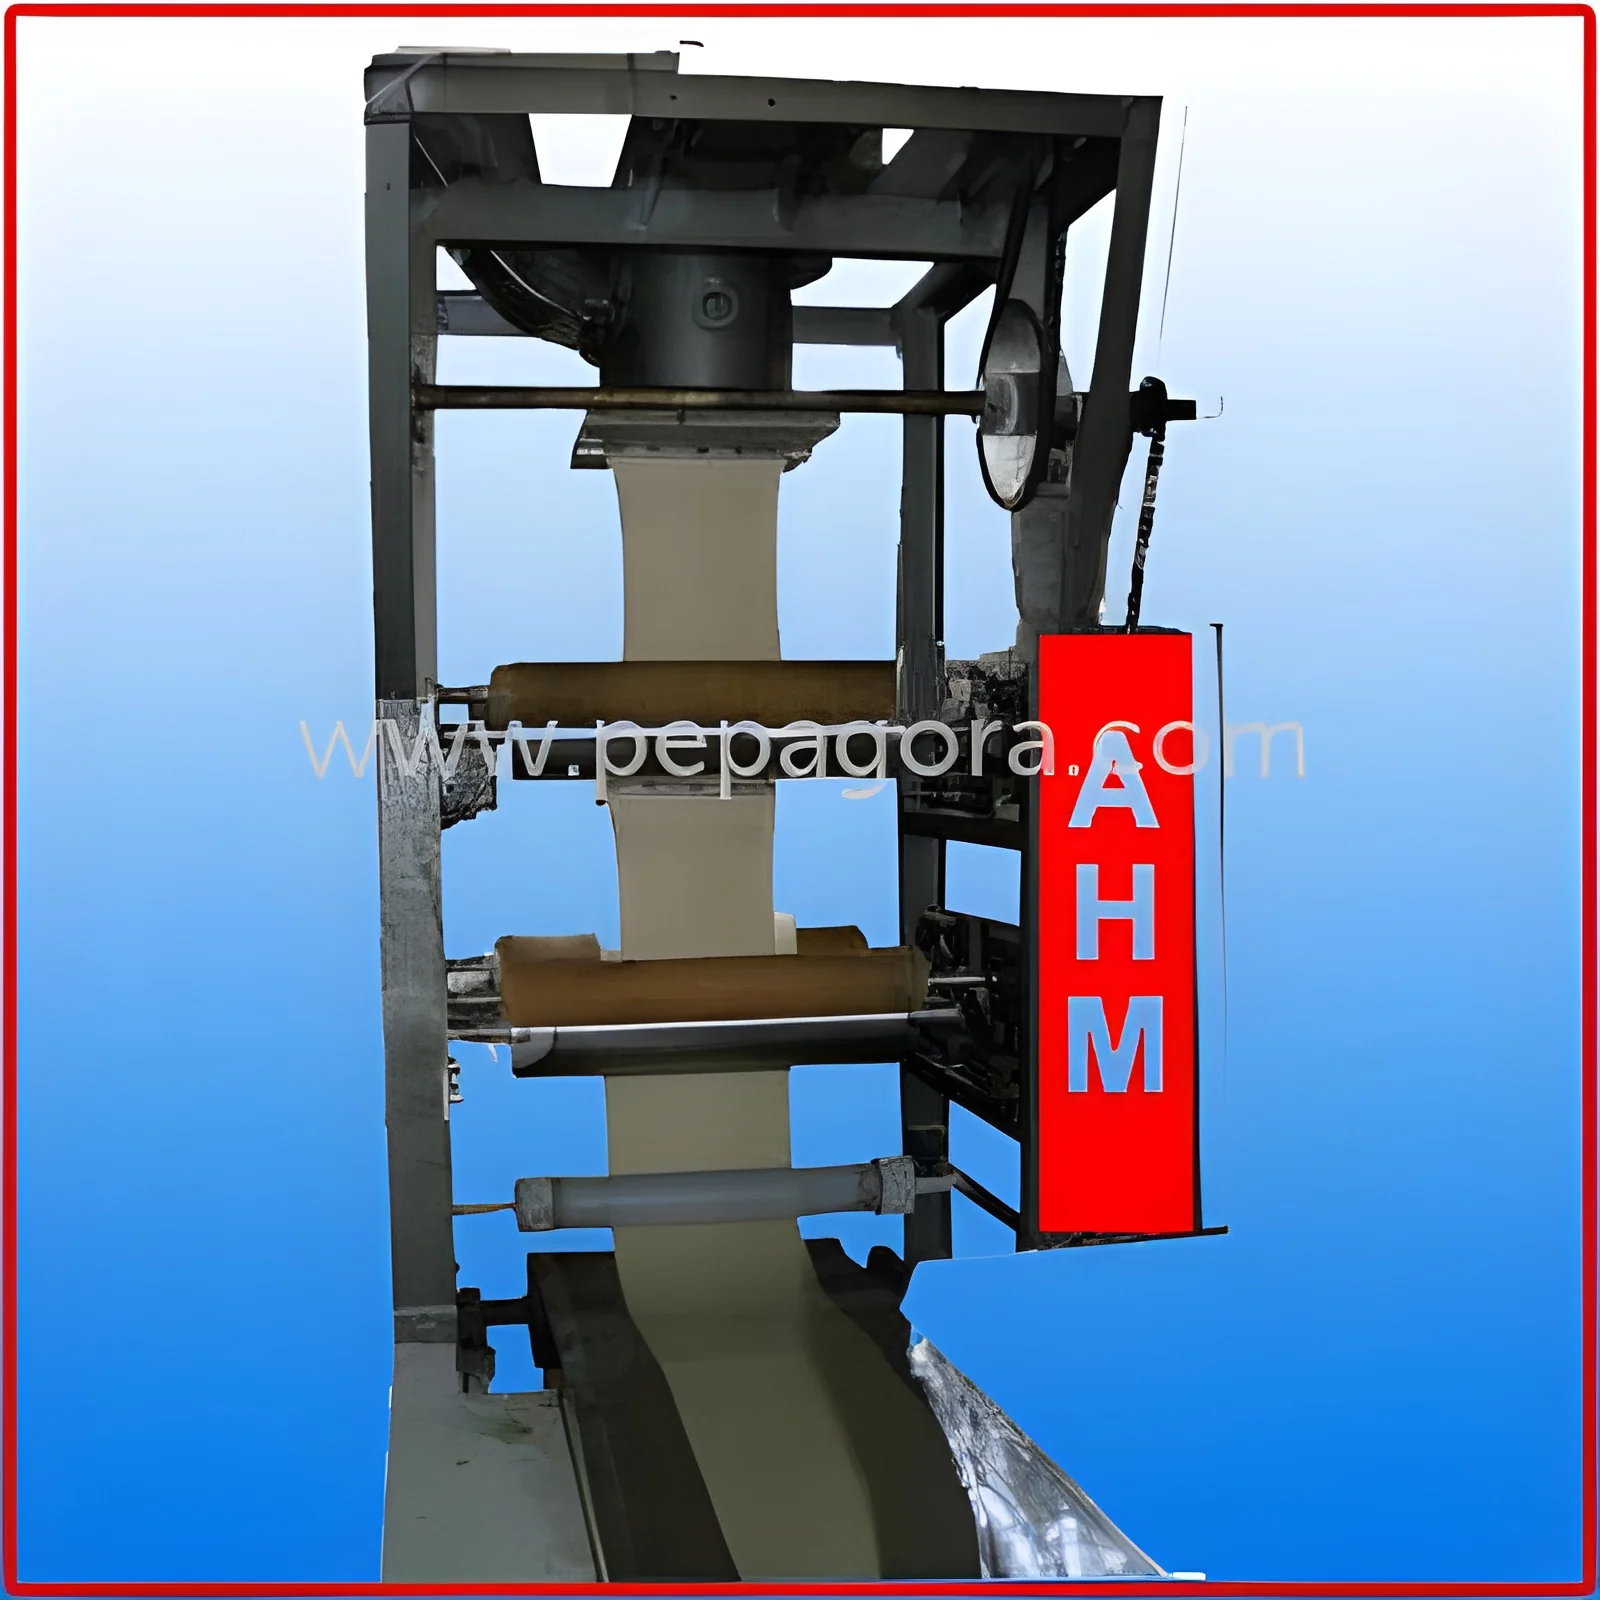
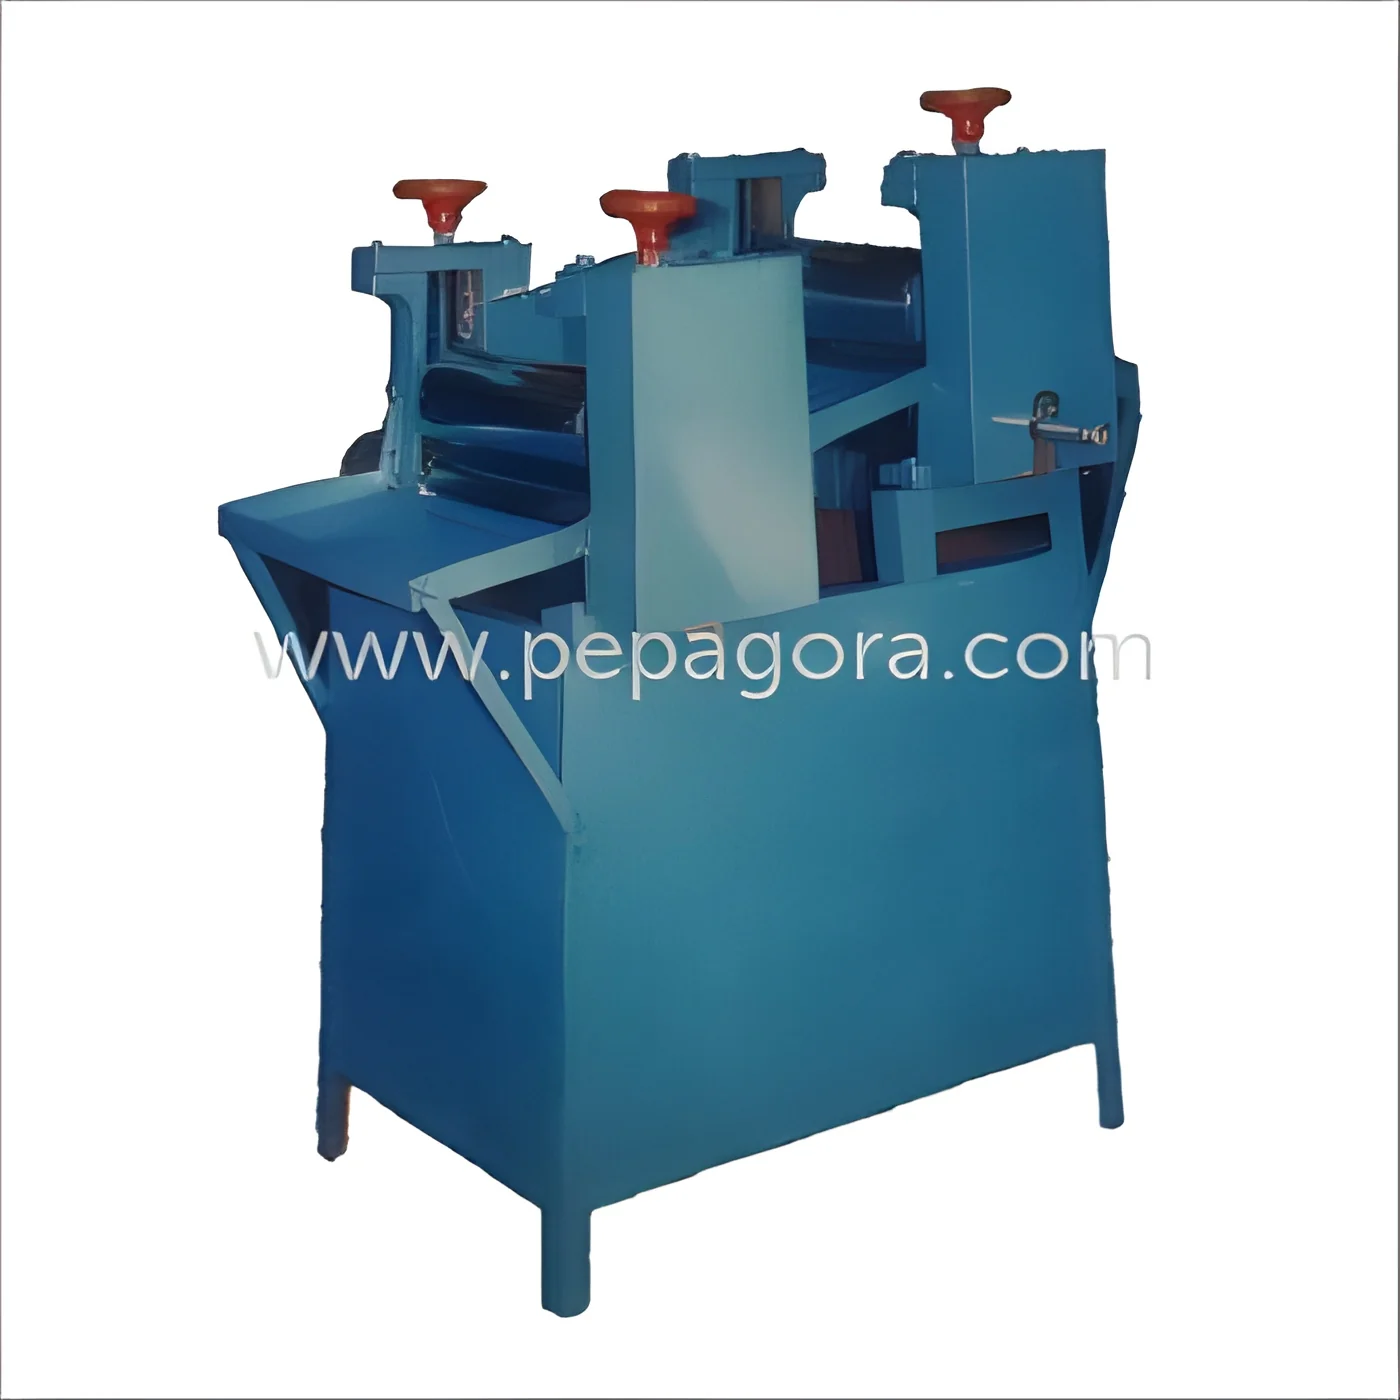
Our flexible stainless steel fire resistant belt conveyors are engineered for superior performance in demanding industrial environments. Constructed from high-grade stainless steel, these systems offer exceptional durability and corrosion resistance, ensuring long-term reliability with minimal maintenance requirements. The fire-resistant belt design provides enhanced safety for various operational settings, while the robust construction maintains structural integrity while offering the flexibility needed for modern material handling challenges. These conveyors deliver consistent performance even in the most demanding industrial conditions, providing reliable transportation of materials across diverse operational environments.

These flexible conveyor systems serve diverse industries including packaging, food processing, pharmaceuticals, warehousing, and manufacturing operations. In packaging facilities, they ensure smooth product flow through bottling and labeling lines with reliable p...
Our flexible stainless steel fire resistant belt conveyors are engineered for superior performance in demanding industrial environments. Constructed from high-grade stainless steel, these systems offer exceptional durability and corrosion resistance, ensuring long-term reliability with minimal maintenance requirements. The fire-resistant belt design provides enhanced safety for various operational settings, while the robust construction maintains structural integrity while offering the flexibility needed for modern material handling challenges. These conveyors deliver consistent performance even in the most demanding industrial conditions, providing reliable transportation of materials across diverse operational environments.

These flexible conveyor systems serve diverse industries including packaging, food processing, pharmaceuticals, warehousing, and manufacturing operations. In packaging facilities, they ensure smooth product flow through bottling and labeling lines with reliable performance. Food processing plants benefit from the stainless steel construction that meets strict hygiene standards and withstands rigorous cleaning protocols. Pharmaceutical companies appreciate the contamination-resistant properties and easy-to-clean surfaces, while warehouses and distribution centers utilize these conveyors for efficient sorting operations and material flow optimization.

The business value of these flexible conveyors lies in their ability to enhance operational efficiency while reducing long-term costs. Their durable stainless steel construction ensures extended service life with minimal maintenance requirements, leading to reduced downtime and lower operational expenses. The fire-resistant properties contribute to workplace safety compliance and risk reduction, while the flexible design allows businesses to adapt to changing production needs without significant additional investment. These conveyors integrate seamlessly with existing equipment, providing immediate productivity improvements and reliable performance that serious buyers demand for their material handling operations.

Key Features:
- Premium stainless steel construction for corrosion resistance and durability
- Fire-resistant conveyor belt design for enhanced operational safety
- Flexible design allowing repositioning as production needs evolve
- Robust structure maintaining stability during continuous operation
- Easy integration with existing production lines and equipment

Benefits:
- Enhanced workplace safety with fire-resistant belt construction
- Long-term reliability with minimal maintenance requirements
- Operational flexibility to adapt to changing production layouts
- Corrosion-resistant stainless steel for extended equipment life
- Seamless integration with existing systems for immediate productivity gains
Specifications
| Key Attributes | |
|---|---|
| Material | Stainless Steel |
| Material Feature | Fire Resistant |
| Structure | Belt Conveyor |
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Flexible stainless steel conveyors with fire-resistant belts provide adaptable material handling solutions for dynamic industrial environments. Their adjustable design allows seamless integration with existing production lines and workflows, supporting efficient operations across various sectors where space optimization and safety are paramount. These systems excel in facilities requiring frequent layout modifications or temporary setups, making them ideal for modern manufacturing and logistics challenges where operational flexibility is essential for productivity.
Common applications include packaging lines, assembly stations, sorting systems, and processing facilities where adaptability and reliability are crucial. The stainless steel construction and fire-resistant properties make these conveyors suitable for diverse industries including food processing, pharmaceuticals, warehousing, and manufacturing plants with specific safety requirements or space constraints that demand robust, reliable equipment for continuous operation.
- Packaging and bottling lines for continuous product flow and operational efficiency
- Assembly operations for smooth component transportation between workstations
- Warehouse sorting systems and distribution center logistics operations
- Food processing facilities requiring hygienic, corrosion-resistant equipment
- Manufacturing plants with limited space or evolving layout requirements
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Shipping & Logistics
| Port of Dispatch | Madurai |
Company Profile

ADHITHYA HITECH MACHINES, Tamil Nadu
 Tamil Nadu, India
Food & Agriculture•Manufacturer•Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Main Markets
Eastern Asia
South Asia
Southeast Asia
Flexible Stainless Steel Fire Resistant Belt Conveyor
Flexible stainless steel fire resistant belt conveyor for reliable material handling in packaging, assembly, and logistics operations. Premium construction ensures durable, efficient performance across industrial applications.
Min. Order Quantity: 1 piece
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
ADHITHYA HITECH MACHINES
 Tamil Nadu, India
Food & AgricultureManufacturer