IN
₹
Apparel & Fashion
Description
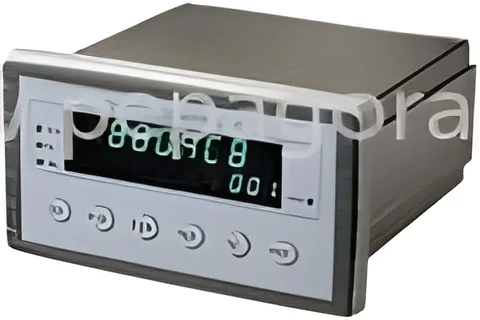
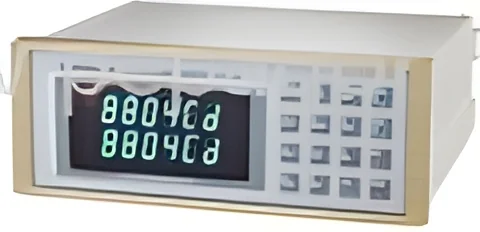
The dual-hopper packaging controller represents a significant advancement in packaging technology, specifically designed for businesses seeking superior efficiency and precision in multi-hopper applications. As an industry-first innovation, this controller integrates two separate hoppers on a single weighing scale, providing a streamlined solution that reduces equipment costs while simplifying operational complexity. Engineered with cutting-edge technology, it maintains exceptional performance standards while delivering outstanding value through its unique capability to control two independent dispensing points with one reliable unit. This controller proves ideal for industries where measurement accuracy, operational speed, and system versatility are paramount, establishing itself as the premier choice for importers and distributors requiring dependable packaging solutions that drive productivity and reduce waste.

This advanced packaging controller finds extensive application across m...
The dual-hopper packaging controller represents a significant advancement in packaging technology, specifically designed for businesses seeking superior efficiency and precision in multi-hopper applications. As an industry-first innovation, this controller integrates two separate hoppers on a single weighing scale, providing a streamlined solution that reduces equipment costs while simplifying operational complexity. Engineered with cutting-edge technology, it maintains exceptional performance standards while delivering outstanding value through its unique capability to control two independent dispensing points with one reliable unit. This controller proves ideal for industries where measurement accuracy, operational speed, and system versatility are paramount, establishing itself as the premier choice for importers and distributors requiring dependable packaging solutions that drive productivity and reduce waste.

This advanced packaging controller finds extensive application across multiple industrial sectors including food processing, pharmaceutical manufacturing, chemical production, and agricultural operations. Within food production environments, it expertly handles mixed ingredients such as spices, grains, flours, and specialty powders with remarkable precision and consistency. Pharmaceutical manufacturers depend on its accurate dispensing capabilities for medications, nutritional supplements, and healthcare products where dosage accuracy is non-negotiable. The chemical and agricultural sectors utilize this controller for packaging fertilizers, seeds, specialty compounds, and industrial materials. Its inherent adaptability makes it suitable for any production environment requiring sophisticated dual-hopper management, ensuring consistent results while maintaining compliance with stringent industry standards and regulatory requirements.

The dual-hopper packaging controller delivers substantial business value by significantly reducing operational costs while enhancing overall productivity. Its innovative design eliminates the requirement for multiple separate controllers, thereby lowering initial capital investment and ongoing maintenance expenses. Reliability stands as a key differentiator, with built-in features specifically engineered to minimize operational downtime and ensure consistent, dependable performance across extended production runs. The system's flexible configuration options allow seamless adaptation to specific packaging line requirements, providing exceptional versatility for diverse application needs. Trusted by global buyers and production facilities, this controller offers a distinct competitive advantage through its technological innovation, durable construction, and proven cost-effectiveness, making it a strategic investment for businesses focused on quality improvement and operational excellence.

Key Features:
- Dual-hopper design enabling simultaneous control of two hoppers on one integrated scale system
- High-precision weighing technology ensuring accurate dispensing with minimal variance
- Customizable operational settings adaptable to various materials and packaging requirements
- Robust industrial construction designed for durability in demanding production environments
- User-friendly interface facilitating straightforward operation and real-time performance monitoring

Benefits:
- Reduced equipment costs by eliminating need for multiple separate controller units
- Enhanced packaging accuracy minimizing product waste and improving quality control
- Increased operational efficiency through synchronized dual-hopper management
- Lower maintenance requirements due to simplified system architecture and robust construction
- Flexible integration capabilities with existing packaging lines and production systems
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
The dual-hopper packaging controller is specifically engineered for industries requiring simultaneous management of multiple products on a single weighing system. It seamlessly coordinates two separate hoppers, delivering precise synchronized dispensing for different materials or blended compositions. This advanced controller eliminates the need for multiple standalone units, significantly reducing system complexity while enhancing operational efficiency in high-demand production environments where accuracy and speed are critical.
Commonly deployed across food processing, pharmaceutical manufacturing, chemical production, and agricultural operations, this controller supports diverse packaging requirements with exceptional versatility. It handles everything from fine powders and granular materials to liquid compounds, maintaining consistent weight accuracy while minimizing product waste. Businesses benefit from its reliable performance, adaptable configuration options, and seamless integration capabilities with existing packaging lines, making it the preferred choice for importers and distributors seeking robust packaging solutions.
- Precisely packaging blended food products including spices, flour mixtures, and custom seasoning blends in food manufacturing facilities
- Accurately dispensing pharmaceutical powders and granules for medication sachets, bottle filling, and supplement packaging operations
- Handling chemical compounds, fertilizers, and agricultural products in industrial packaging and distribution centers
- Managing dual-ingredient filling processes for cosmetics, personal care products, and specialty chemical formulations
- Supporting automated high-volume production lines in manufacturing plants requiring efficient, reliable packaging systems
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Orbitron Tradelink, Gujarat
 Gujarat, India
Manufacturer•Trading Company•Distributor / Wholesaler
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Dual Hopper Packaging Controller For High Speed Multi Product Accuracy
Dual Hopper Packaging Controller delivers integrated precision for multiple hoppers on a single scale. This high-speed system ensures multi-product accuracy for food, chemicals, and pharmaceuticals, reducing costs while boosting packaging efficiency for serious production needs.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Orbitron Tradelink
 Gujarat, India
Manufacturer