IN
₹
Apparel & Fashion
Description
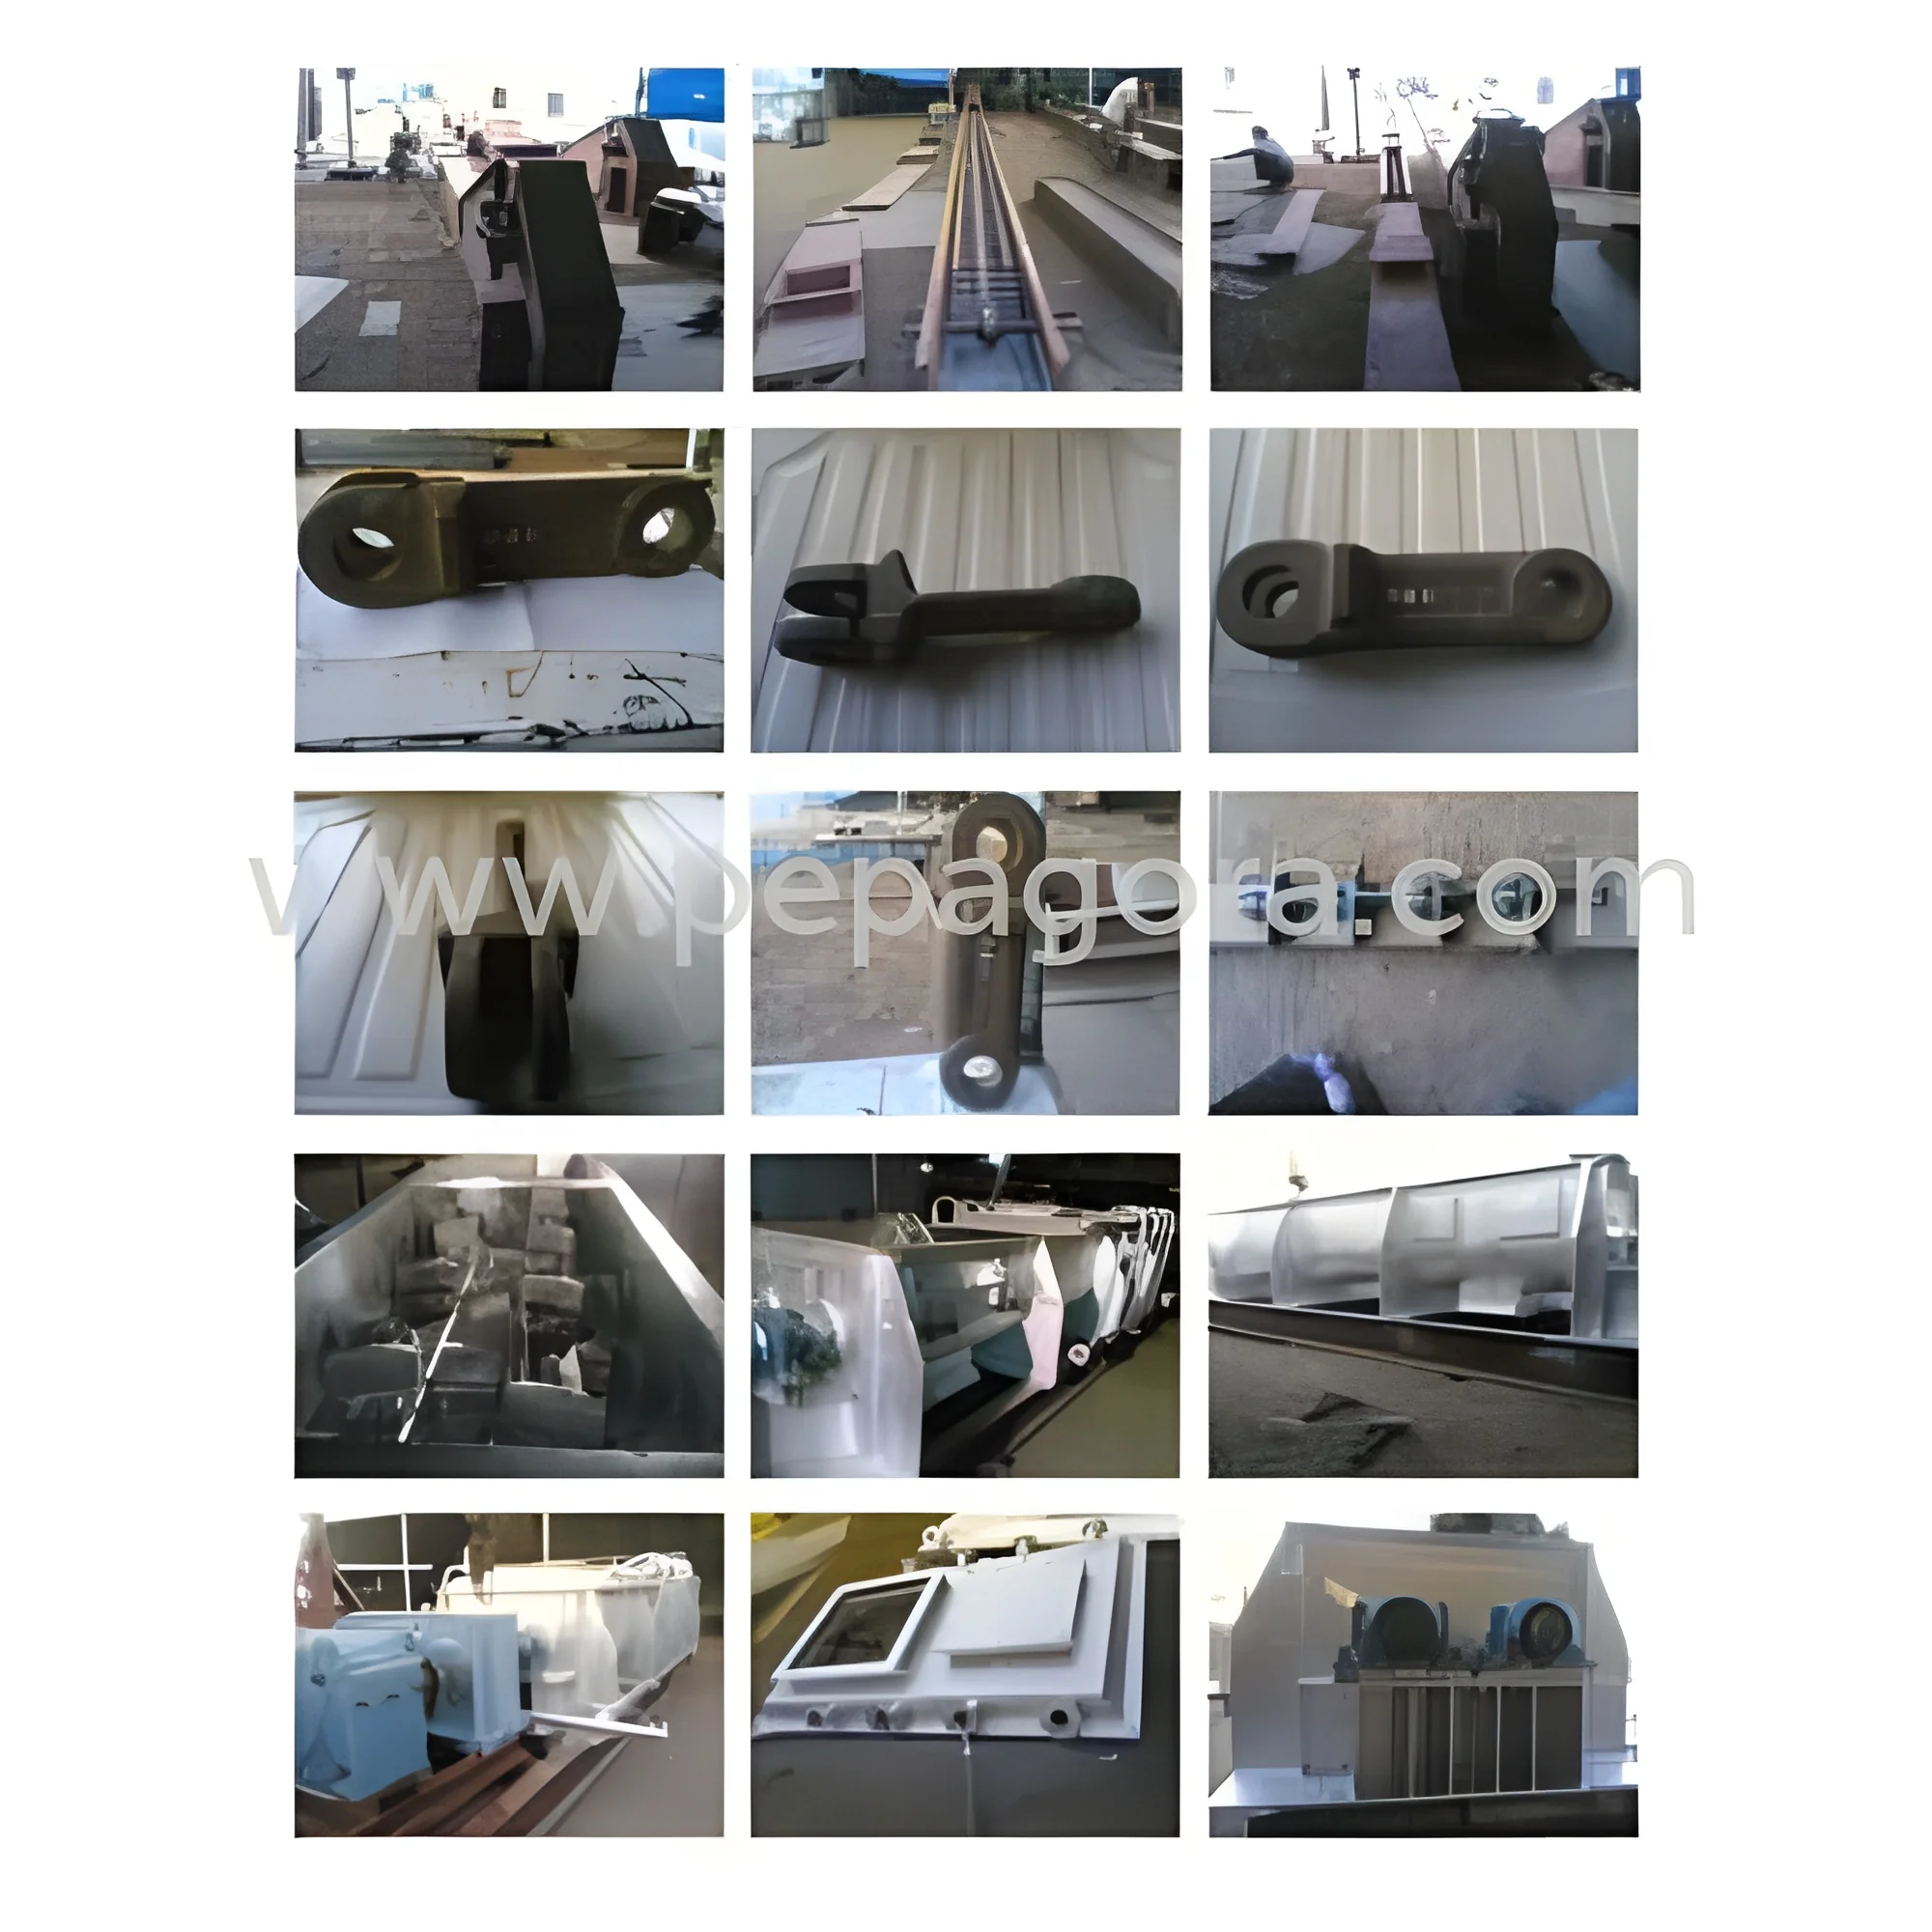
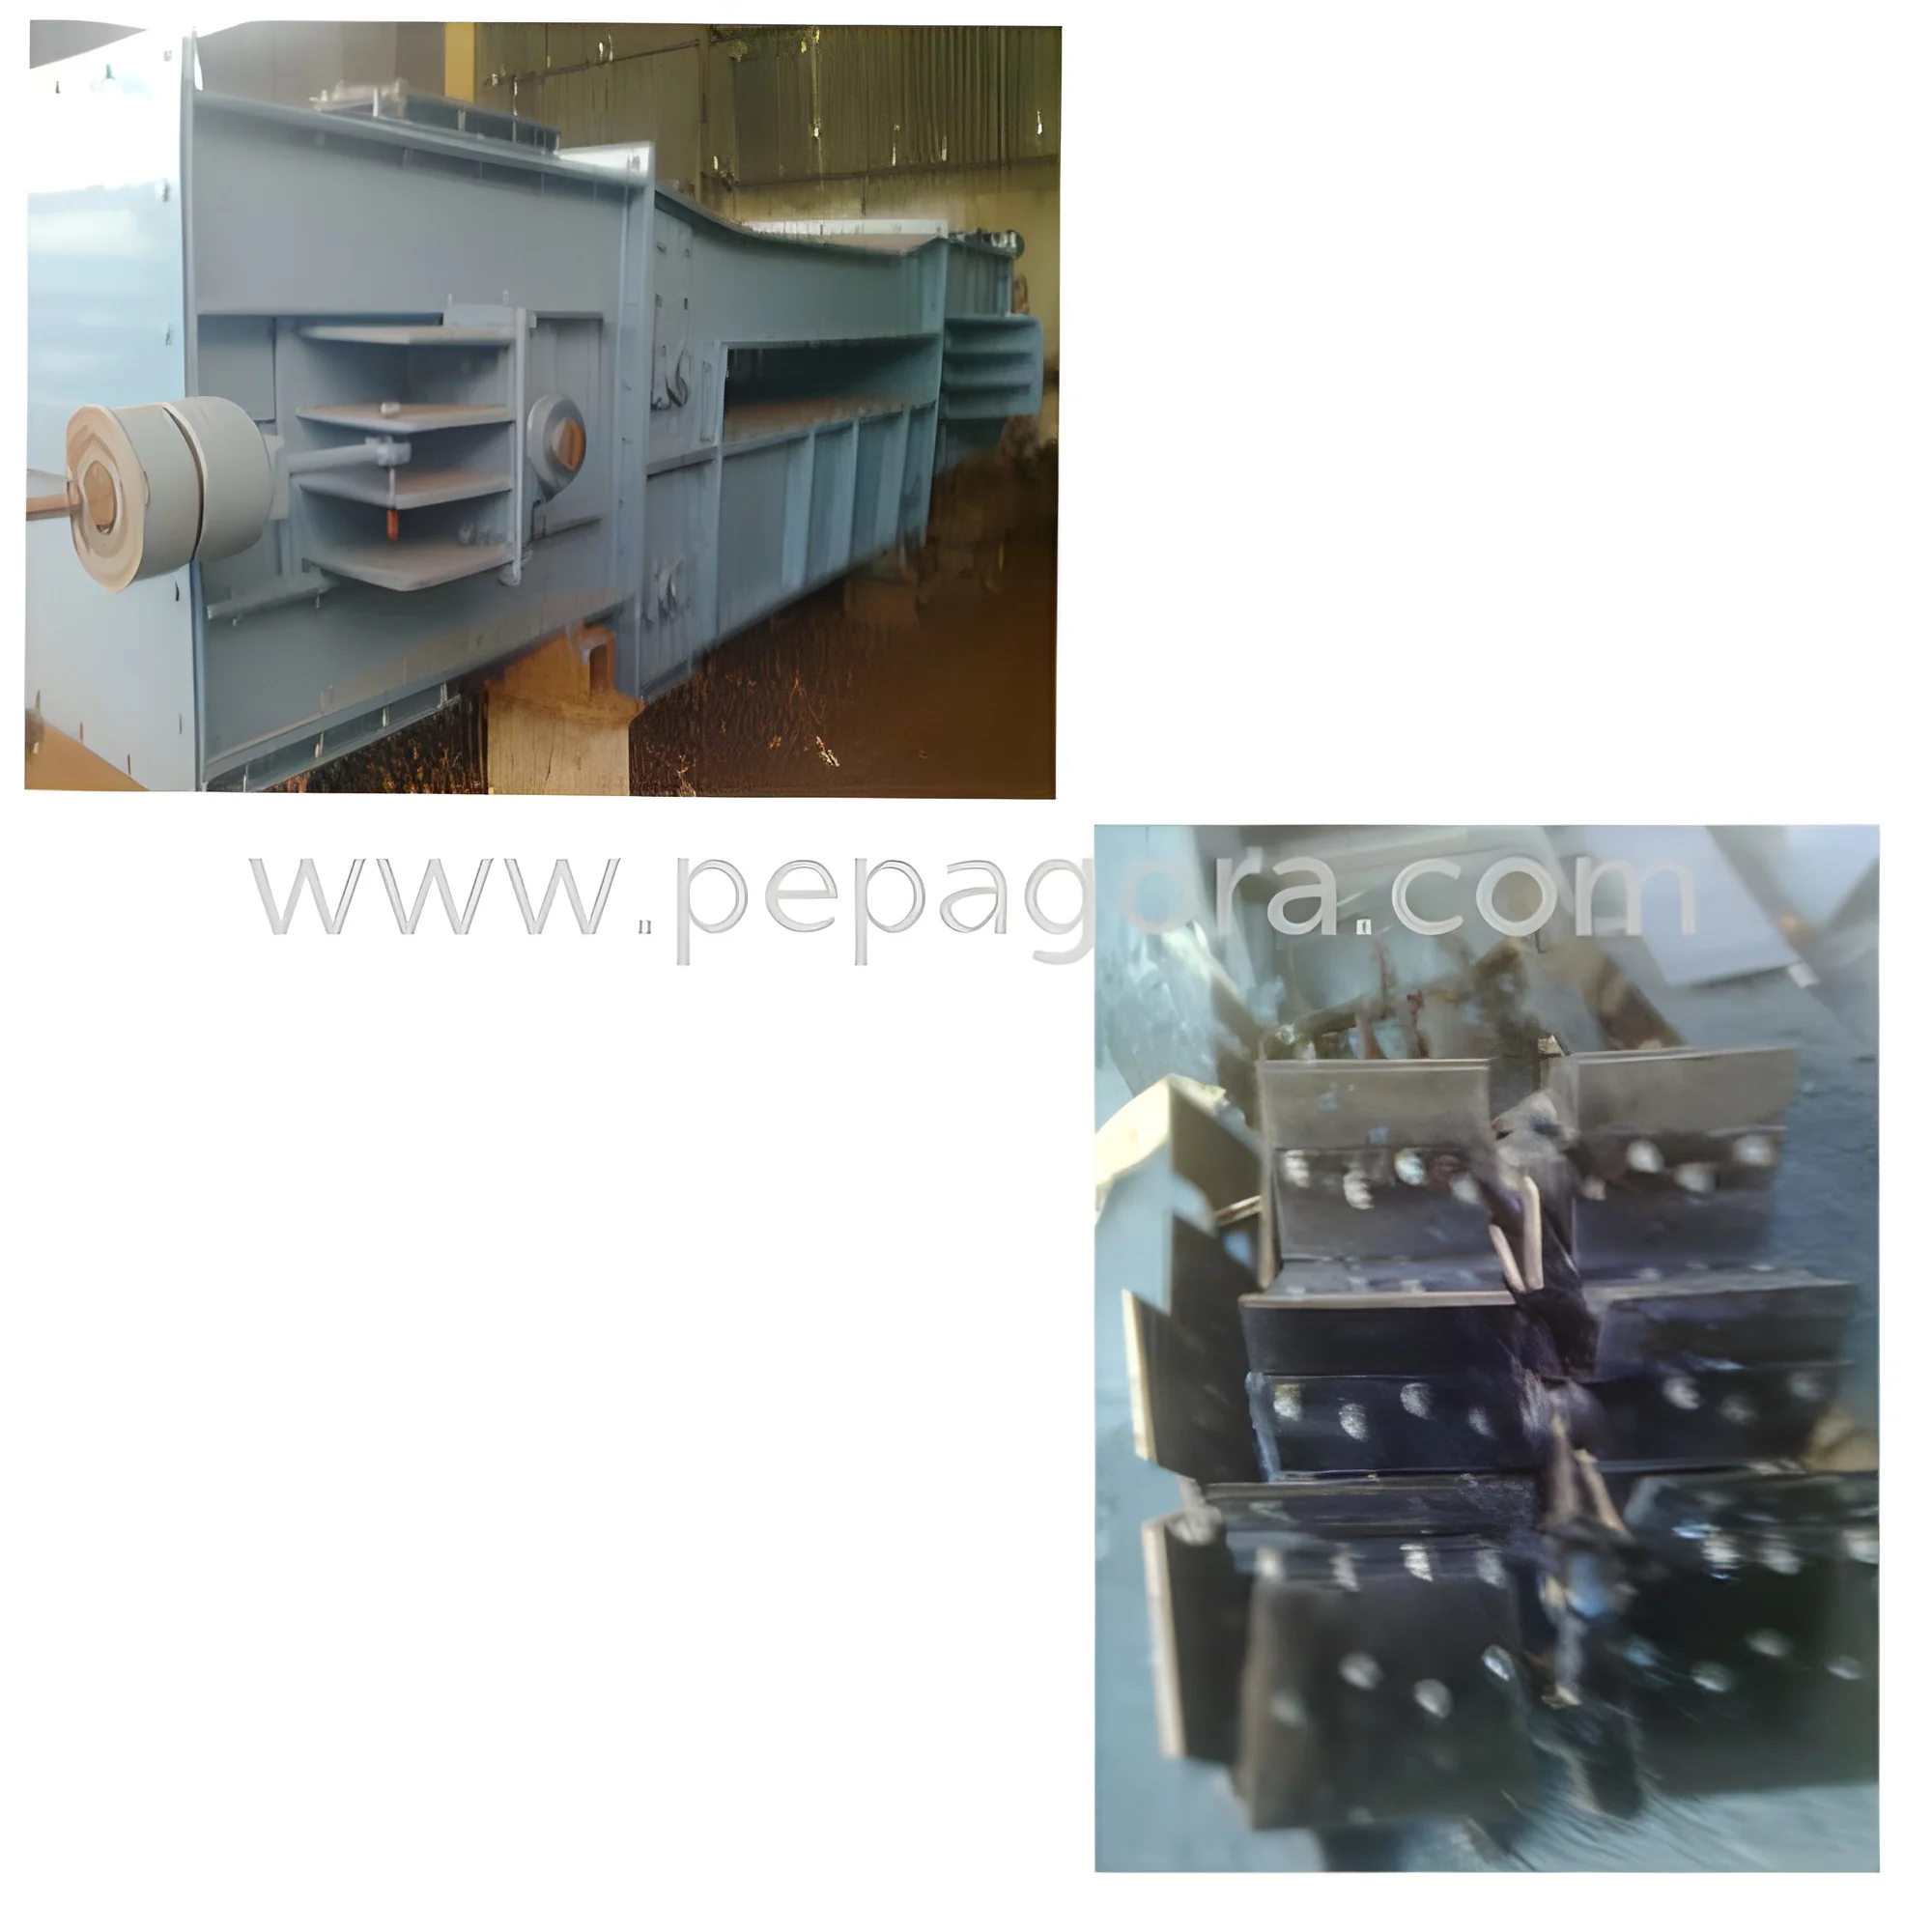
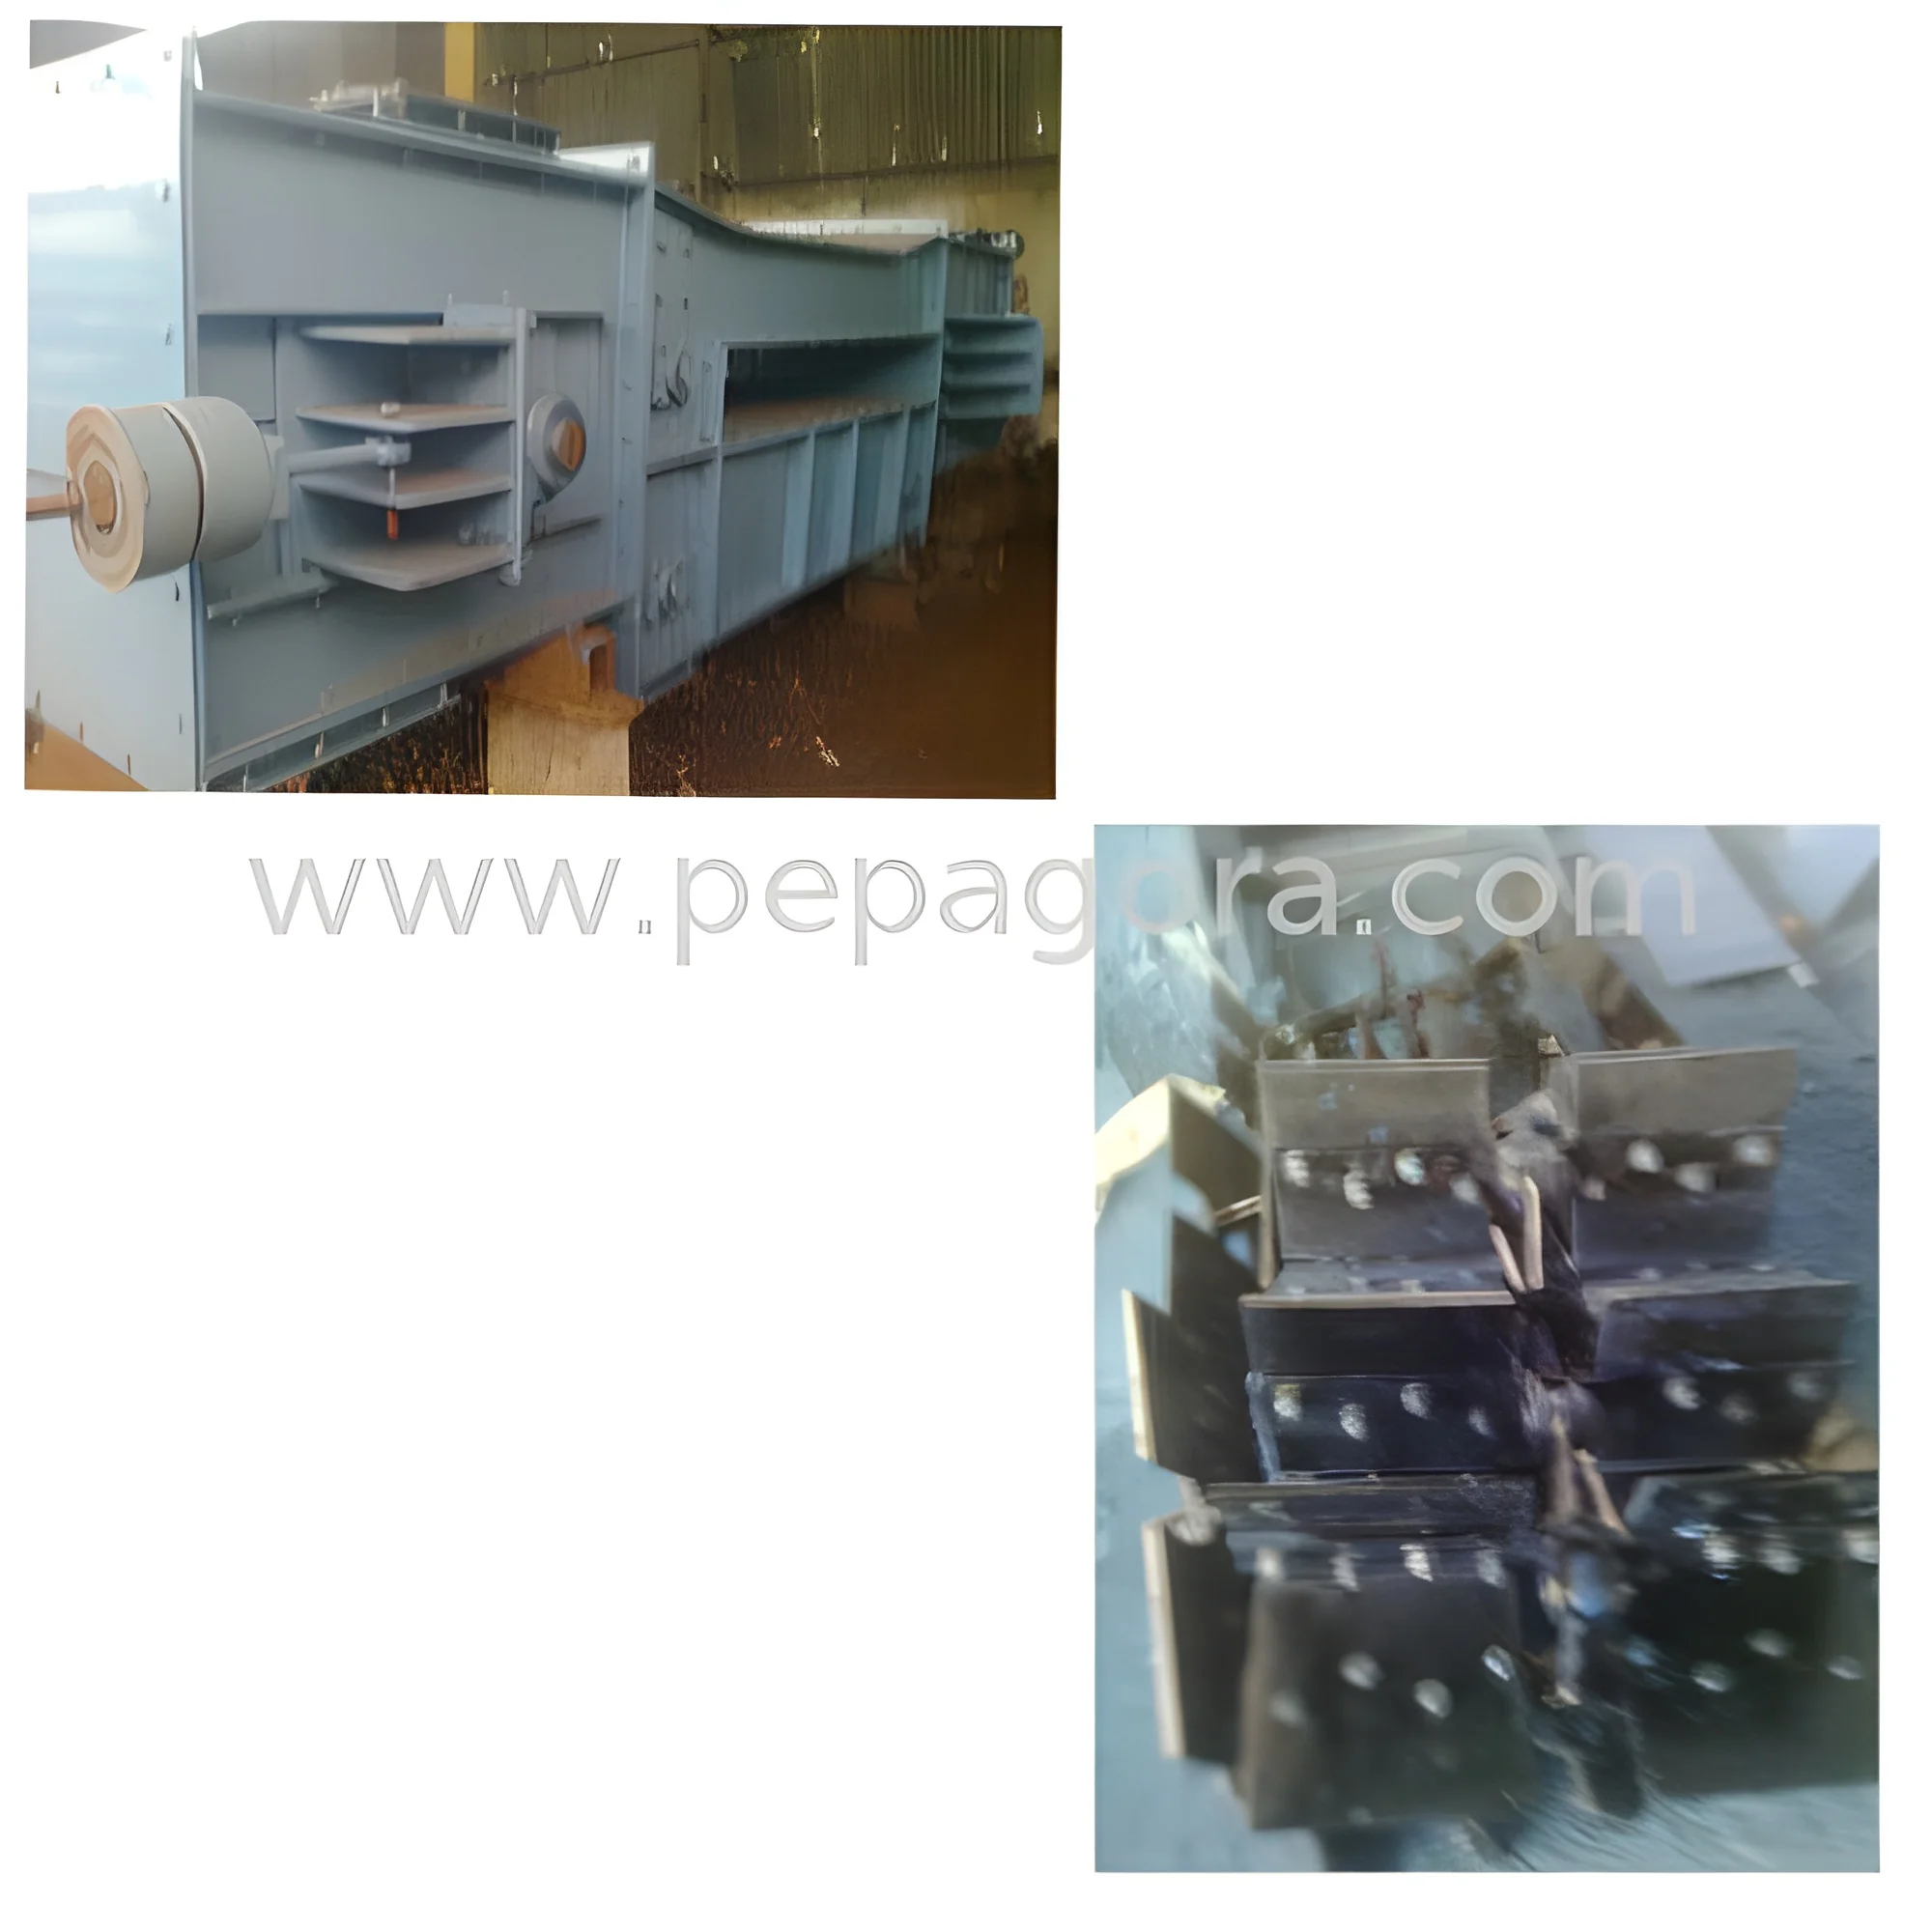
Our industrial drag chain conveyors represent a superior solution for heavy-duty bulk material handling in the most challenging environments. Constructed from durable, oil-resistant stainless steel, these double strand en-masse conveyors utilize flights fixed between two chains to effectively drag material through a fully enclosed trough. This design is specifically engineered for materials that are hot, abrasive, dusty, or slightly cohesive—substances that often cause problems for other conveyor types. The robust build ensures reliable, continuous operation with minimal maintenance, providing a dependable backbone for your material flow processes. The enclosed system not only contains the product but also protects it from external contamination, making it ideal for both industrial and processing applications where purity and containment are essential.

These conveyors serve as critical infrastructure across a wide spectrum of heavy industries. In cement production, they reliably trans...
Our industrial drag chain conveyors represent a superior solution for heavy-duty bulk material handling in the most challenging environments. Constructed from durable, oil-resistant stainless steel, these double strand en-masse conveyors utilize flights fixed between two chains to effectively drag material through a fully enclosed trough. This design is specifically engineered for materials that are hot, abrasive, dusty, or slightly cohesive—substances that often cause problems for other conveyor types. The robust build ensures reliable, continuous operation with minimal maintenance, providing a dependable backbone for your material flow processes. The enclosed system not only contains the product but also protects it from external contamination, making it ideal for both industrial and processing applications where purity and containment are essential.

These conveyors serve as critical infrastructure across a wide spectrum of heavy industries. In cement production, they reliably transport hot clinker and raw materials while preventing dust pollution. Power plants utilize them for efficient ash handling and biomass fuel conveyance. The mining sector depends on their durability to move abrasive ores and minerals, while chemical manufacturers value their resistance to corrosive substances. Furthermore, industries handling food-grade bulk ingredients or pharmaceuticals benefit from the hygienic, enclosed design that prevents contamination. This versatility across sectors underscores their fundamental role in maintaining efficient, clean, and continuous industrial operations where material handling is a core process.

The business value of investing in our drag chain conveyors extends far beyond simple transportation. Their exceptional reliability translates directly into reduced downtime and lower maintenance costs, safeguarding your production schedules. The enclosed design minimizes product loss and environmental emissions, supporting both operational efficiency and regulatory compliance. The oil-resistant stainless steel construction ensures a long service life even in harsh, greasy conditions, providing an excellent return on investment. By ensuring consistent, trouble-free material flow, these conveyors enhance overall plant productivity and operational safety. They are built to integrate seamlessly into your existing layout, offering a robust, long-term solution that strengthens your operational resilience and bottom-line performance.

Key Features:
- Constructed from durable, oil-resistant stainless steel for longevity
- Double strand en-masse chain configuration for superior strength and load capacity
- Fully enclosed trough design prevents spillage and contains dust
- Engineered to handle hot, abrasive, and sluggish bulk materials effectively
- Flights securely fixed between chains for positive material dragging action

Benefits:
- Ensures reliable, continuous operation with minimal maintenance requirements
- Prevents material loss and controls dust for a cleaner, safer work environment
- Oil-resistant construction withstands harsh, greasy industrial conditions
- Handles challenging materials that cause issues for other conveyor types
- Provides a hygienic, enclosed transport solution to prevent contamination
Specifications
| Key Attributes | |
|---|---|
| Material | Stainless Steel |
| Material Feature | Oil Resistant |
| Structure | Conveyor System |
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Industrial drag chain conveyors are engineered to master the toughest material handling challenges where other systems fail. Their fully enclosed, double-strand design excels at transporting hot, abrasive, dusty, or sluggish bulk materials without spillage or dust emission. This makes them indispensable for industries that require clean, contained, and reliable movement of difficult-to-handle substances under demanding operational conditions.
These robust systems are specifically built to handle slightly loose, lumpy, or sticky materials that can jam or damage conventional conveyors. The oil-resistant stainless steel construction ensures longevity even when exposed to greasy or oily industrial environments. Their reliability in continuous operation with minimal maintenance makes them a cornerstone for facilities where uptime is critical and access for repairs is often limited.
- Cement manufacturing plants for moving hot clinker and raw meal
- Power generation facilities for handling fly ash and biomass fuel
- Chemical processing units for conveying abrasive or corrosive powders
- Mining operations for transporting ores, minerals, and tailings
- Bulk food processing for ingredient handling where hygiene is paramount
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
R & G Enterprises, Maharashtra
 Maharashtra, India
Manufacturer
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Industrial Drag Chain Conveyors Stainless Steel Oil Resistant
Industrial drag chain conveyors in stainless steel offer oil-resistant, heavy-duty bulk material handling. Our double strand en-masse conveyors provide reliable performance for demanding industrial applications, ensuring efficient and contained transportation of challenging materials.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
R & G Enterprises
 Maharashtra, India
Manufacturer