IN
₹
Apparel & Fashion

Description
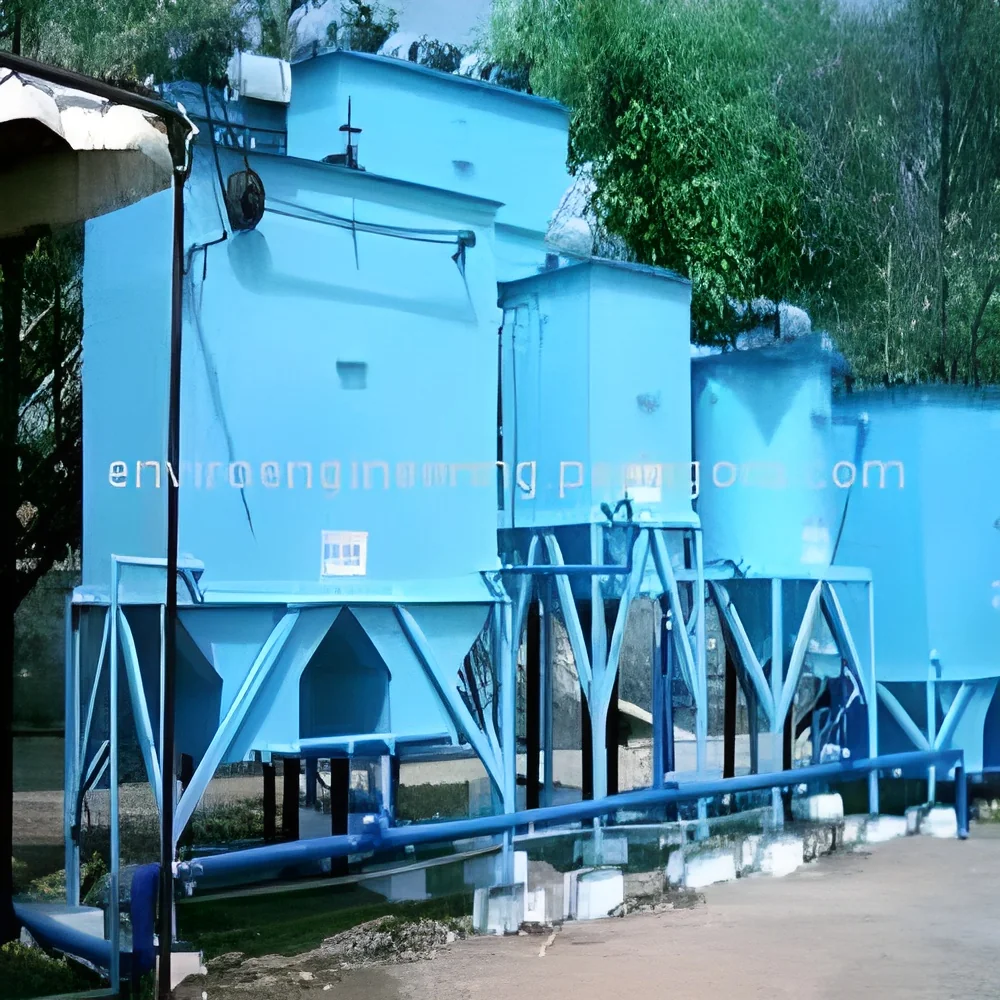
The DM Plant Water Purifier represents advanced water treatment technology designed for reliable demineralized water production. Utilizing sophisticated ion exchange processes, this equipment effectively removes dissolved solids from water with an impressive 96% desalination rate. Operating efficiently within water temperatures of 5-45°C and requiring standard 220V electrical supply, these systems provide consistent performance for both industrial-scale operations and specialized applications. The technology ensures water purity that meets rigorous standards, making it an essential solution for environments where water quality directly impacts process outcomes and final product integrity. With robust construction and straightforward operation, these plants deliver dependable service across various settings.

Multiple industries depend on DM water purification systems for their critical water quality requirements. The pharmaceutical sector utilizes these plants to produce water for medi...
The DM Plant Water Purifier represents advanced water treatment technology designed for reliable demineralized water production. Utilizing sophisticated ion exchange processes, this equipment effectively removes dissolved solids from water with an impressive 96% desalination rate. Operating efficiently within water temperatures of 5-45°C and requiring standard 220V electrical supply, these systems provide consistent performance for both industrial-scale operations and specialized applications. The technology ensures water purity that meets rigorous standards, making it an essential solution for environments where water quality directly impacts process outcomes and final product integrity. With robust construction and straightforward operation, these plants deliver dependable service across various settings.

Multiple industries depend on DM water purification systems for their critical water quality requirements. The pharmaceutical sector utilizes these plants to produce water for medical formulations and purification processes where purity cannot be compromised. Power generation facilities implement these systems for boiler feed water treatment to prevent scaling and corrosion in critical equipment. Manufacturing industries including electronics, automotive components, and food processing rely on demineralized water for production processes, equipment cleaning, and as essential ingredient water. Research laboratories and testing facilities require the consistent high-quality water output that DM plants provide for analytical procedures and experimental applications.

The operational value of DM water purification plants lies in their proven reliability, cost-efficient performance, and consistent output quality. These systems significantly reduce maintenance expenses by preventing scale accumulation in pipelines and equipment, while ensuring uniform product quality through reliable water purification processes. The 96% desalination rate guarantees water purity that complies with international standards, providing businesses with confidence in their manufacturing processes and end-products. The equipment's durable construction and minimal maintenance requirements contribute to extended operational lifespan and reduced downtime, delivering excellent return on investment through consistent performance and reliability in demanding industrial environments.

Key Features:
- High-performance 96% desalination rate for superior water purity
- Wide operational range of 5-45°C water temperature compatibility
- Standard 220V electrical requirement for easy installation
- Advanced ion exchange technology for dissolved solids removal
- Durable construction designed for long-term reliable operation

Benefits:
- Consistent high-purity water output meeting industry standards
- Reduced equipment maintenance through scale prevention
- Cost-effective operation with minimal energy requirements
- Versatile application across multiple industrial sectors
- Reliable performance ensuring process consistency and quality
Specifications
| Key Attributes | |
|---|---|
| Grade Standard | Agriculture Grade |
| Application | Industrial Application |
| Usage | Water Treatment |
| Use | Household Pre-Filtration |
| Voltage (V) | 220 |
| Function | Water Purifier |
| Water Temperature | 5-45 ℃ |
| Desalination Rate | ≥ 96% |
| Price | Negotiable |
| Used to | Remove different dissolved solids from the water |
| Grade Standard | Agriculture Grade |
| Application | Industrial Application |
| Usage | Water Treatment |
| Use | Household Pre-Filtration |
| Voltage (V) | 220 |
| Function | Water Purifier |
| Water Temperature | 5-45 ℃ |
| Desalination Rate | ≥ 96% |
| Price | Negotiable |
| Used to | Remove different dissolved solids from the water |
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
DM plants provide essential demineralized water production through advanced ion exchange technology, effectively removing dissolved solids with 96% desalination efficiency. These systems operate reliably within 5-45°C water temperatures using standard 220V power, making them suitable for diverse industrial environments where consistent water purity is critical for operational success and product quality maintenance across multiple sectors.
The versatility of these water purification systems extends across numerous applications requiring high-purity water. From manufacturing processes to specialized technical applications, these plants deliver consistent performance with minimal maintenance requirements. Their robust construction ensures long-term reliability while the high desalination rate guarantees water quality that meets stringent industry standards for various professional and industrial uses.
- Pharmaceutical manufacturing processes requiring purified water for formulations
- Power generation facilities for high-purity boiler feed water systems
- Laboratory research and analytical procedures needing ultra-pure water
- Electronics manufacturing for component cleaning and production
- Food processing operations as ingredient water and sanitation applications
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Shipping & Logistics
| Port of Dispatch | Chennai |
Company Profile
Enviro Engineering, Tamil Nadu
 Tamil Nadu, India
Industrial Equipment & Machinery•Manufacturer•Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory Size1000-5000 sqm
Annual Production Capacity0
Main Markets
Eastern Asia
South Asia
Southeast Asia
DM Plant Water Purifier Industrial Household Pre Filtration 96% Desalination
DM Plant Water Purifier delivers 96% desalination rate for industrial and household pre-filtration. This reliable equipment removes dissolved solids efficiently with 220V operation and 5-45°C temperature range for consistent pure water production.
Min. Order Quantity: 1 piece
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Enviro Engineering
 Tamil Nadu, India
Industrial Equipment & MachineryManufacturer