IN
₹
Apparel & Fashion
Description
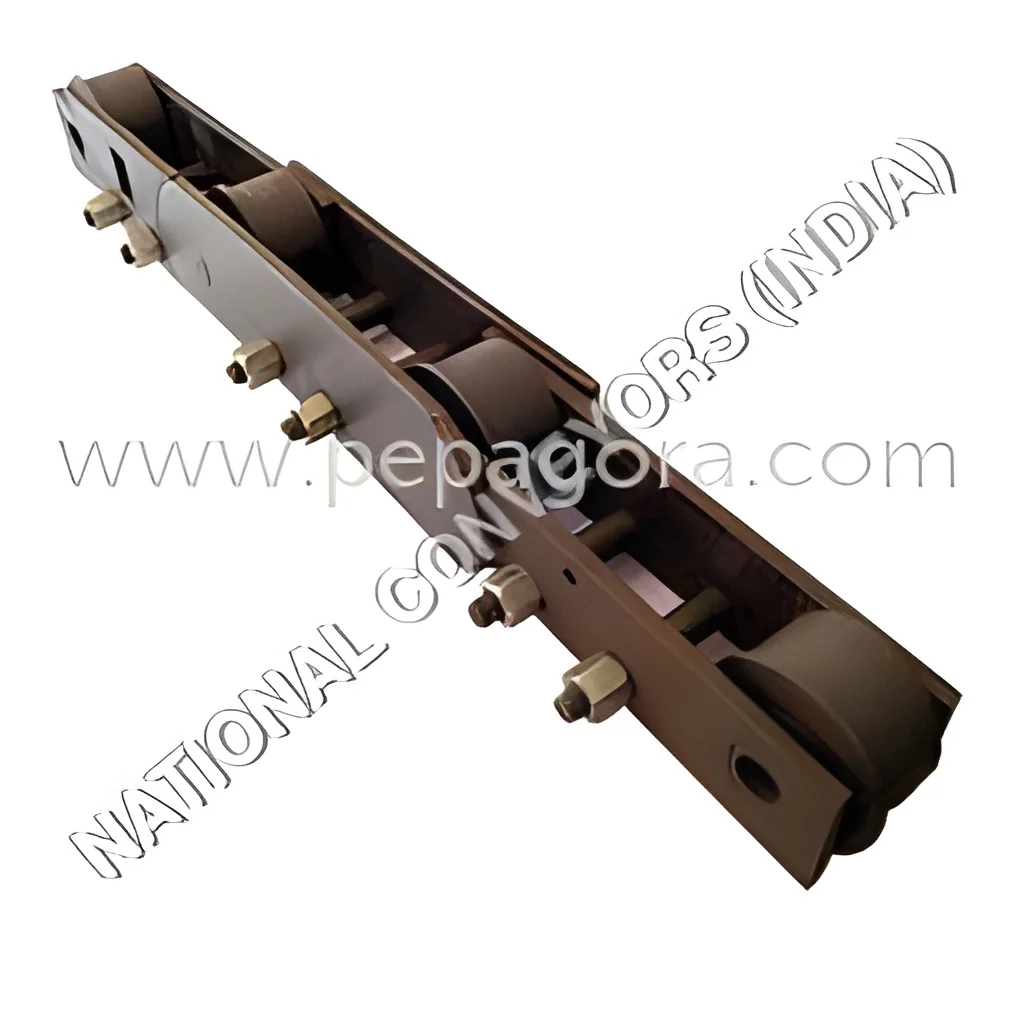
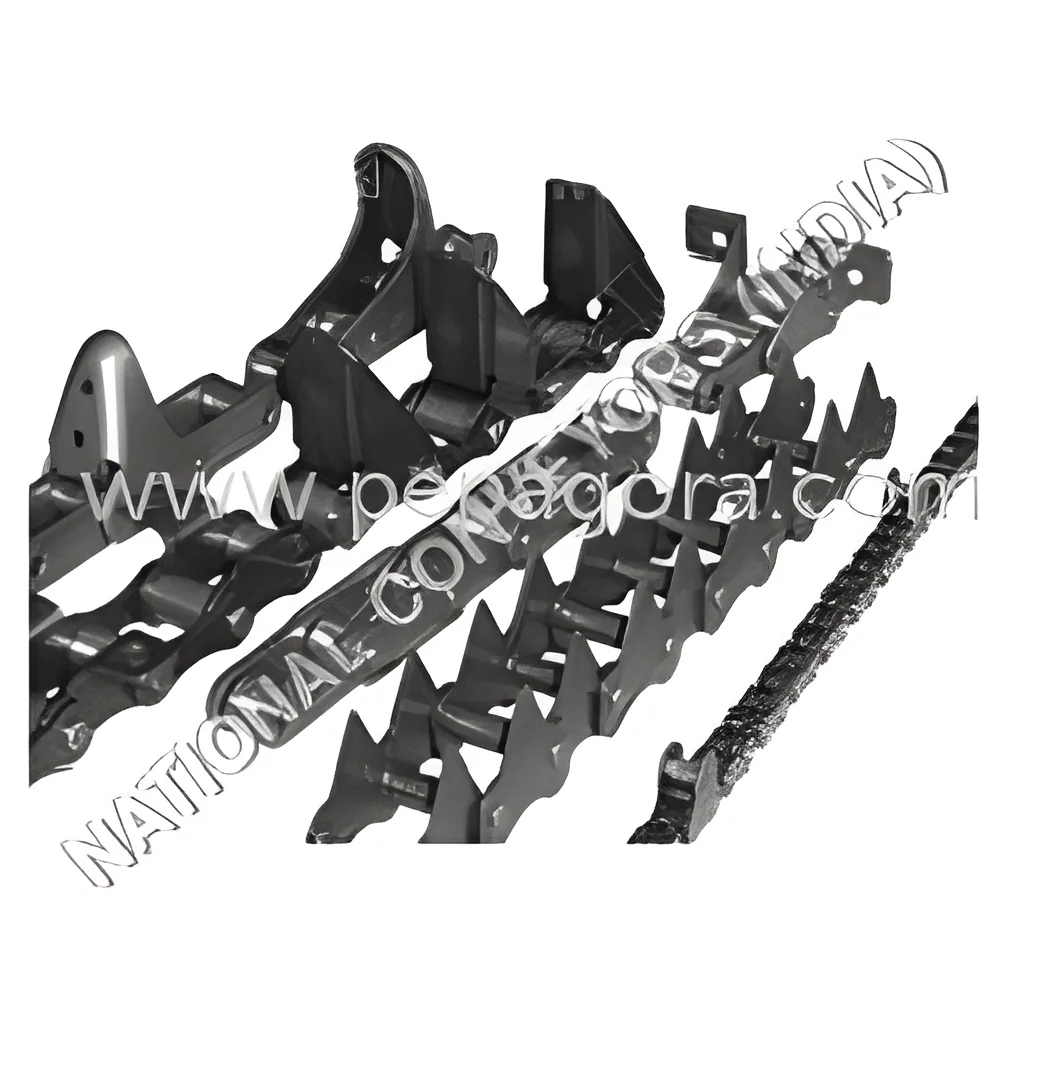
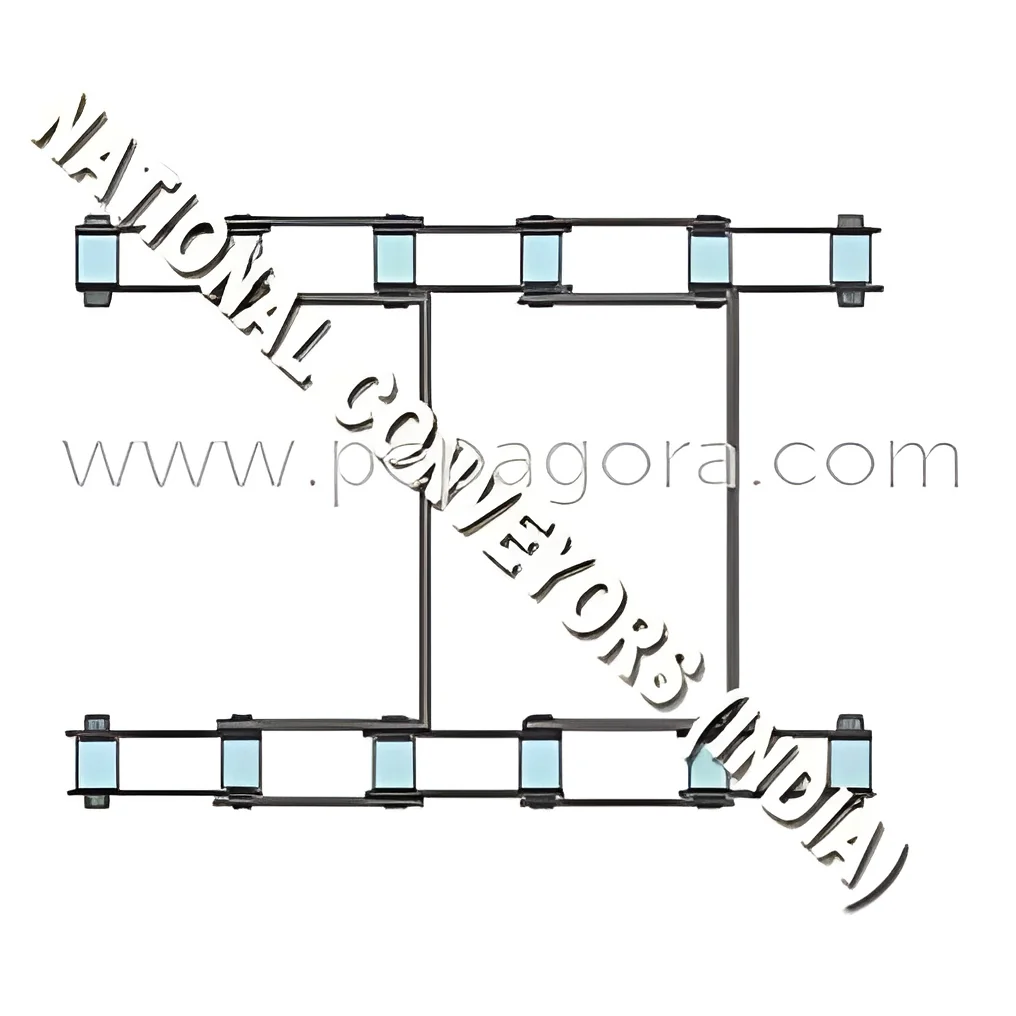
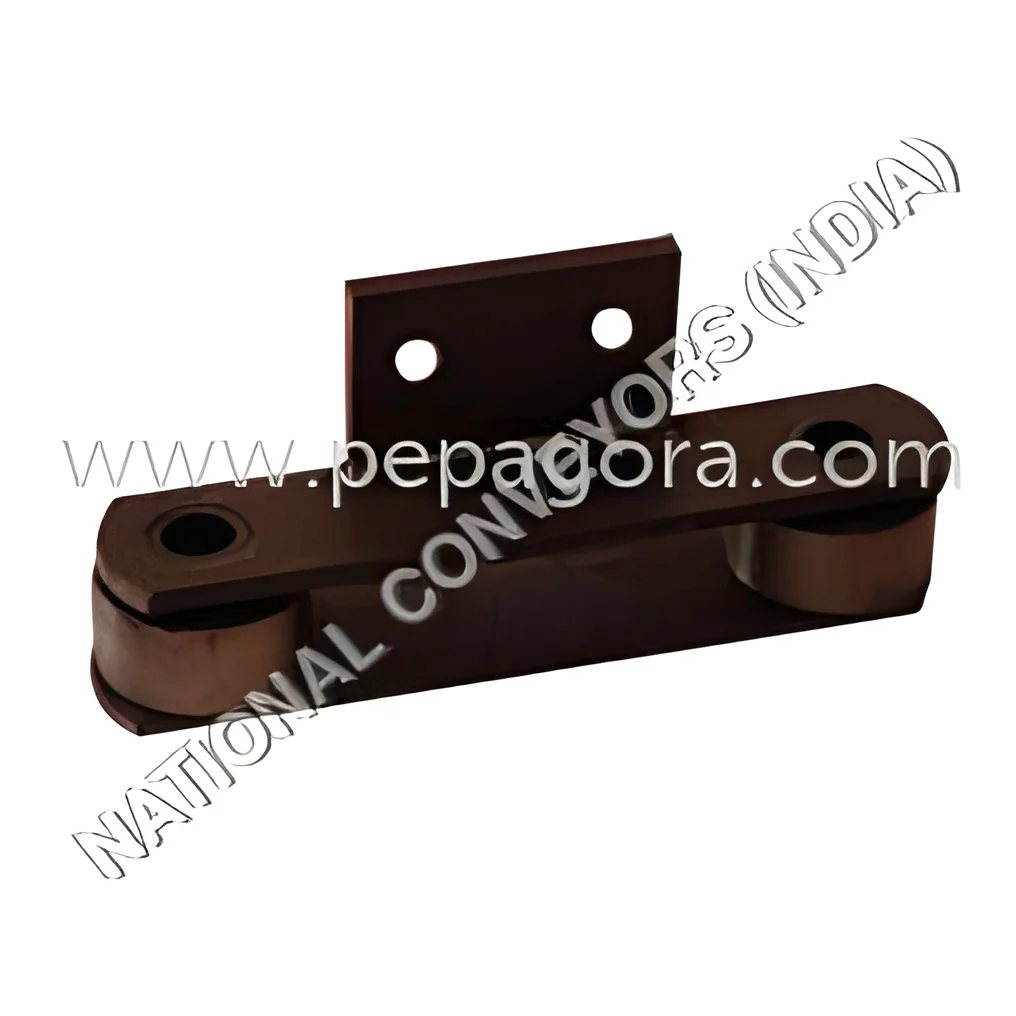
Industrial Cooling Systems Premium Cooler Chains are engineered components built to deliver reliable performance in demanding cooling applications. Manufactured from high-quality materials, these chains are designed for durability and operational efficiency, ensuring consistent thermal management in industrial settings. They undergo rigorous quality testing to meet performance standards for continuous use, providing a dependable solution for systems that cannot afford unexpected downtime. Their construction focuses on resisting wear and corrosion, which are common challenges in industrial environments, thereby extending service life and maintaining cooling efficiency over time.

These cooler chains serve vital roles across industries where precise temperature control directly impacts operational success and product quality. In manufacturing, they are integral to cooling systems that regulate machinery and process temperatures. Food processing operations utilize them in conveyor systems...
Industrial Cooling Systems Premium Cooler Chains are engineered components built to deliver reliable performance in demanding cooling applications. Manufactured from high-quality materials, these chains are designed for durability and operational efficiency, ensuring consistent thermal management in industrial settings. They undergo rigorous quality testing to meet performance standards for continuous use, providing a dependable solution for systems that cannot afford unexpected downtime. Their construction focuses on resisting wear and corrosion, which are common challenges in industrial environments, thereby extending service life and maintaining cooling efficiency over time.

These cooler chains serve vital roles across industries where precise temperature control directly impacts operational success and product quality. In manufacturing, they are integral to cooling systems that regulate machinery and process temperatures. Food processing operations utilize them in conveyor systems that transport products through controlled climate zones, essential for safety and preservation. Chemical and pharmaceutical production relies on their consistent performance to maintain specific temperature parameters during sensitive manufacturing stages. Their application extends to large-scale refrigeration in storage facilities, where they help preserve perishable goods under stable conditions.

The value of these premium cooler chains lies in their contribution to operational reliability and cost-effective performance. Their durable design reduces the frequency of replacements and maintenance interventions, minimizing operational disruptions and associated costs. The efficiency of these chains supports energy-conscious operations by maintaining optimal cooling performance without excessive power consumption. For businesses procuring industrial components, these chains represent a reliable investment that supports system integrity and process consistency. Their proven performance in diverse applications builds trust for long-term use, helping operations maintain productivity and meet quality standards through dependable temperature management.

Key Features:
- Constructed from premium materials for enhanced durability and long service life
- Engineered for high efficiency in maintaining consistent cooling performance
- Features excellent corrosion resistance suitable for challenging industrial environments
- Designed for minimal maintenance requirements and easy integration into existing systems
- Robust build quality capable of withstanding continuous operation and mechanical stress

Benefits:
- Reduces operational downtime through reliable performance and extended component life
- Lowers long-term costs by minimizing maintenance needs and replacement frequency
- Supports consistent product quality by ensuring stable temperature control in processes
- Enhances system efficiency, contributing to potential energy savings in cooling operations
- Provides a dependable solution that builds operational confidence and process stability
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
These premium cooler chains are designed for continuous operation in industrial cooling systems where consistent temperature management is non-negotiable. They perform reliably in manufacturing plants, processing facilities, and large-scale operations that depend on precise thermal control for product quality and safety. The robust construction ensures stable performance across extended operational cycles.
Multiple industries benefit from these chains' ability to withstand challenging conditions. They are suitable for environments with high moisture, temperature variations, and demanding mechanical loads. Their reliable operation supports critical cooling processes in sectors where system failure can lead to significant production losses or compromised product integrity.
- Manufacturing plants for maintaining process cooling systems
- Food processing facilities for refrigeration and freezing conveyors
- Chemical production units requiring temperature-controlled lines
- Automotive manufacturing for engine and component testing cooling
- Industrial cold storage and warehouse refrigeration systems
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
National Engineers India, Punjab
 Punjab, India
Manufacturer•Distributor•Wholesaler•Importer•Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Industrial Cooling Systems Premium Cooler Chains For Durability Efficiency
Premium Industrial Cooling Systems Cooler Chains deliver durable, efficient performance for manufacturing and processing applications. Engineered for reliability in demanding temperature control environments.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
National Engineers India
 Punjab, India
Manufacturer