IN
₹
Apparel & Fashion
Description
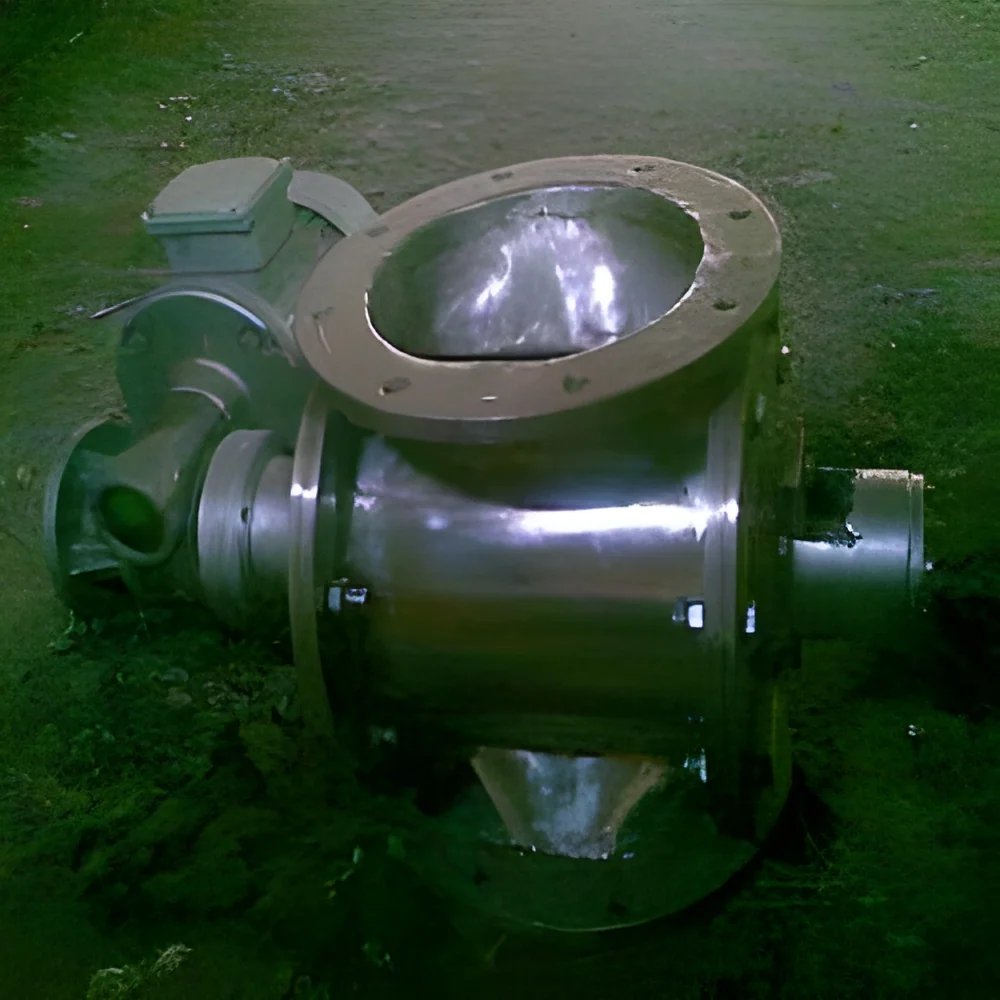
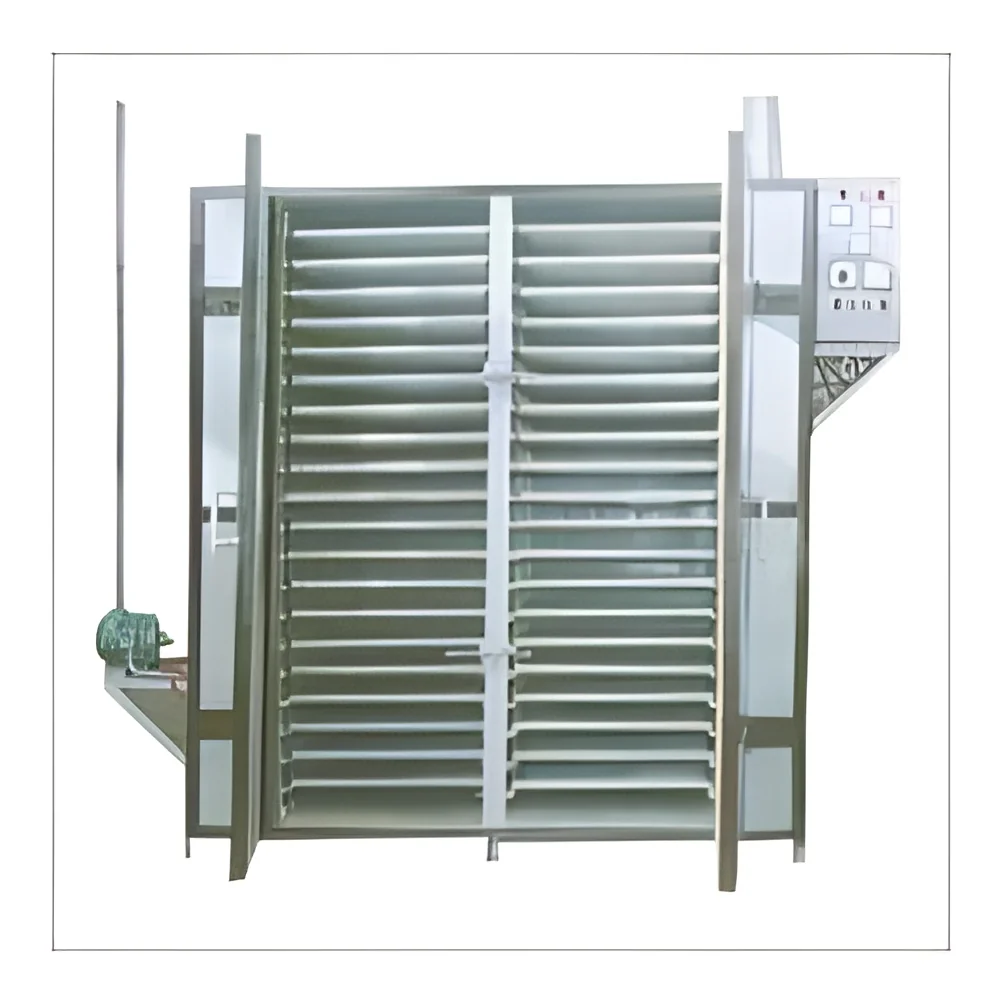
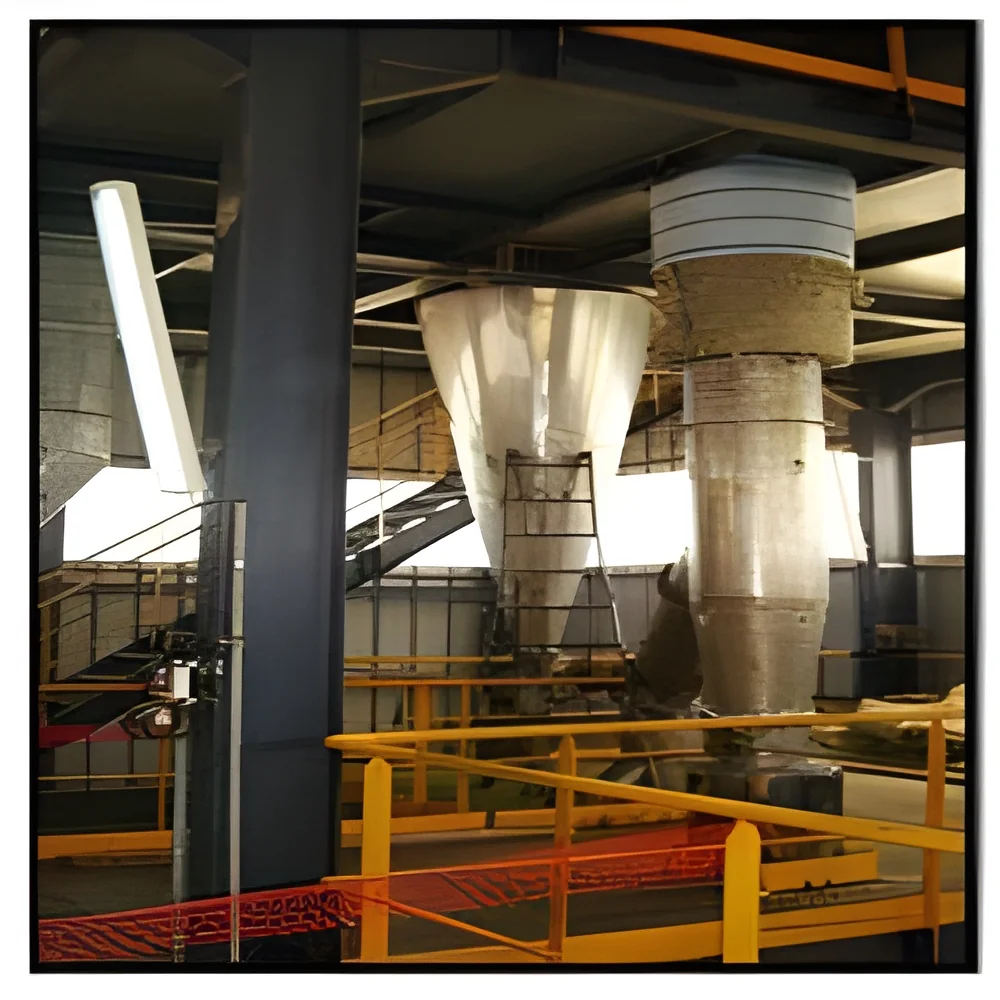
Industrial Material Handling Conveyor Systems represent engineered solutions for efficient goods transport across industrial facilities. Designed to eliminate manual handling bottlenecks, these systems ensure consistent operational flow with reliable movement between locations. Built with precision engineering, they provide smooth, continuous operation even under demanding conditions, making them ideal for operations where downtime is unacceptable. The systems integrate seamlessly into existing infrastructure, supporting everything from small packages to heavy bulk materials with equal efficiency.

These conveyor systems serve critical roles across multiple sectors including manufacturing, warehousing, logistics, food processing, and automotive production. Manufacturing facilities utilize them for just-in-time component delivery to assembly stations, while warehouses depend on them for efficient sorting and storage retrieval operations. Logistics centers rely on these conveyors for sys...
Industrial Material Handling Conveyor Systems represent engineered solutions for efficient goods transport across industrial facilities. Designed to eliminate manual handling bottlenecks, these systems ensure consistent operational flow with reliable movement between locations. Built with precision engineering, they provide smooth, continuous operation even under demanding conditions, making them ideal for operations where downtime is unacceptable. The systems integrate seamlessly into existing infrastructure, supporting everything from small packages to heavy bulk materials with equal efficiency.

These conveyor systems serve critical roles across multiple sectors including manufacturing, warehousing, logistics, food processing, and automotive production. Manufacturing facilities utilize them for just-in-time component delivery to assembly stations, while warehouses depend on them for efficient sorting and storage retrieval operations. Logistics centers rely on these conveyors for systematic package handling and distribution. Food processing plants benefit from their reliable operation and design considerations for various materials. The automotive industry integrates these systems into production lines for precise parts movement between workstations, demonstrating exceptional versatility across different operational environments.

Choosing our conveyor systems delivers exceptional reliability and measurable return on investment through reduced labor costs, increased throughput, and minimized product damage. The robust construction guarantees long-term service life with minimal maintenance requirements and maximum operational uptime. These systems represent strategic investments in operational excellence, providing competitive advantage through improved efficiency and workflow optimization. The focus on quality ensures each installation operates with precision control and dependable performance, translating directly to enhanced bottom-line results for your business.

Key Features:
- Heavy-duty construction with durable materials for extended service life
- Customizable configurations to match specific layout and operational needs
- Smooth, consistent material movement with precision control systems
- Seamless integration with existing automation and handling infrastructure
- Low maintenance design with accessible components for easy servicing

Benefits:
- Increased operational throughput and productivity in material handling
- Reduced manual labor costs and minimized workplace injuries
- Consistent, reliable goods transport with minimal product damage
- Long-term durability with low maintenance requirements and high uptime
- Flexible design that adapts to various industrial environments and materials
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Our conveyor systems are engineered for seamless integration into existing production and logistics workflows. They handle various materials including packages, raw components, and finished goods with consistent reliability. These systems reduce manual handling while increasing throughput in demanding industrial environments.
Customizable configurations suit diverse operational layouts from assembly lines to sorting facilities. Built with robust components, our conveyors operate continuously under heavy loads while maintaining precision movement. They serve as critical infrastructure in automation projects where efficiency and dependability are paramount.
- Automated package sorting and distribution in e-commerce fulfillment centers
- Raw material transport in manufacturing and production assembly lines
- Bulk goods handling in food processing and packaging facilities
- Pallet and container movement in warehouse storage and retrieval systems
- Component transfer between workstations in automotive and electronics manufacturing
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
APT Services, Gujarat
 Gujarat, India
Industrial Equipment & Machinery•Manufacturer•Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Industrial Material Handling Conveyor Systems For Efficient Goods Transport
Industrial Material Handling Conveyor Systems provide efficient, reliable goods transport for warehouses and factories. These durable systems ensure smooth bulk material movement with customizable designs to optimize your operational workflow.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
APT Services
 Gujarat, India
Industrial Equipment & MachineryManufacturer