IN
₹
Apparel & Fashion
Description
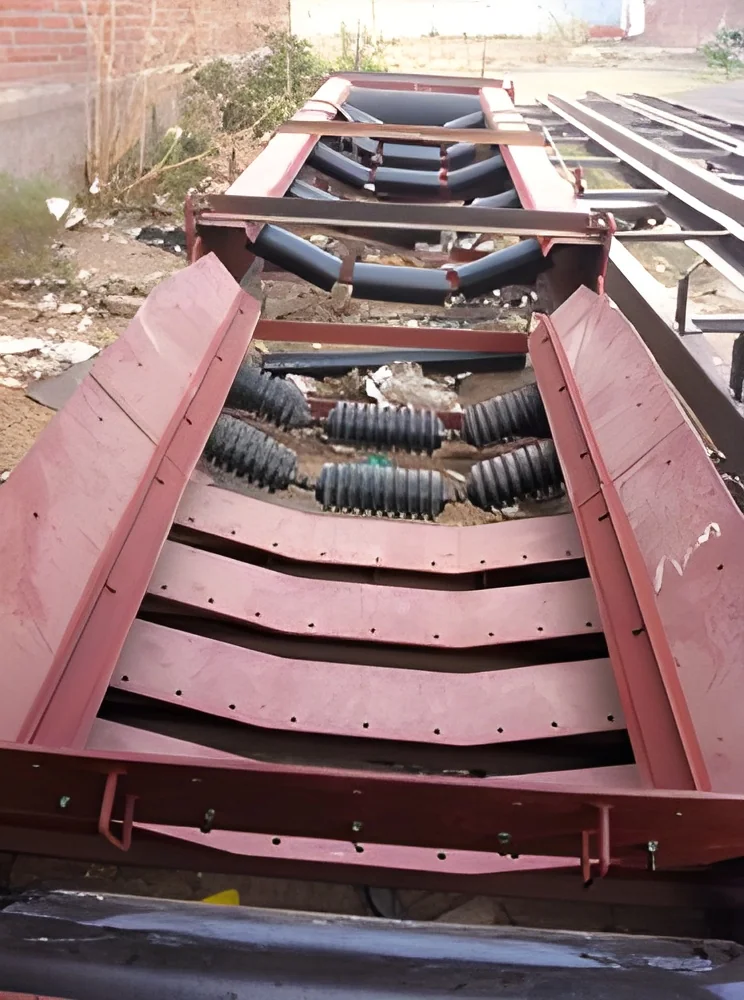
Industrial conveyor systems represent essential infrastructure for modern material handling, designed to optimize workflow efficiency and operational productivity across diverse industrial settings. These robust systems facilitate the seamless movement of goods throughout your facility, reducing manual handling while increasing throughput capacity and operational consistency. Built with precision engineering and durable components, our conveyors ensure reliable performance even in demanding industrial environments with continuous operation requirements. The customizable nature of these solutions allows adaptation to specific layout requirements and material characteristics, providing flexible configurations for various load capacities and operational needs. Each system is manufactured with attention to detail, ensuring smooth operation and minimal maintenance requirements for long-term reliability and cost-effective performance.

These conveyor systems serve critical roles across multi...
Industrial conveyor systems represent essential infrastructure for modern material handling, designed to optimize workflow efficiency and operational productivity across diverse industrial settings. These robust systems facilitate the seamless movement of goods throughout your facility, reducing manual handling while increasing throughput capacity and operational consistency. Built with precision engineering and durable components, our conveyors ensure reliable performance even in demanding industrial environments with continuous operation requirements. The customizable nature of these solutions allows adaptation to specific layout requirements and material characteristics, providing flexible configurations for various load capacities and operational needs. Each system is manufactured with attention to detail, ensuring smooth operation and minimal maintenance requirements for long-term reliability and cost-effective performance.

These conveyor systems serve critical roles across multiple industries where efficient material movement directly impacts productivity and profitability. In manufacturing plants, they enable streamlined production by moving components between assembly stations and supporting just-in-time manufacturing processes. Logistics and distribution operations utilize them for efficient sorting, storage, and shipping operations in warehouses and distribution centers. The automotive industry relies on these systems for moving heavy components along production lines, while food processing facilities benefit from designs that meet stringent hygiene and compliance standards. Packaging operations use conveyors to transport products through labeling, sealing, and palletizing processes, ensuring consistent workflow from production to shipment while maintaining product integrity throughout the handling process.

Investing in industrial conveyor systems delivers significant business value through operational cost reduction and productivity enhancement. These systems minimize labor requirements while maximizing output, providing rapid return on investment through improved efficiency and reduced material handling expenses. Their reliability ensures continuous operation with minimal downtime, protecting production schedules and delivery commitments while maintaining consistent quality standards. The customizable nature of these solutions means you receive exactly what your operation requires without unnecessary features or compromises, ensuring optimal performance for your specific material handling challenges. We stand behind our products with comprehensive support and service, ensuring your conveyor system remains operational and efficient for years to come, making it a strategic investment for businesses focused on growth and operational excellence.

Key Features:
- Heavy-duty construction with durable materials for long-lasting performance in industrial environments
- Customizable lengths, widths, and configurations to fit specific facility layouts and space constraints
- Multiple belt material options including rubber, PVC, and metal for different application requirements
- Integrated safety features including emergency stops, guarding systems, and overload protection
- Compatibility with various drive systems and power options for flexible installation and operation

Benefits:
- Increased operational efficiency through automated material movement and reduced manual handling
- Enhanced productivity with consistent workflow and minimized production bottlenecks
- Reduced labor costs by automating repetitive material transport tasks
- Improved workplace safety with integrated protection features and reduced manual lifting
- Long-term reliability with durable construction and minimal maintenance requirements
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Our industrial conveyor systems transform material handling operations by automating the movement of goods throughout your facility. They efficiently transport everything from small components to heavy pallets, reducing manual labor while increasing throughput and operational safety. These systems maintain consistent workflow from receiving to shipping, minimizing bottlenecks and optimizing your production capacity across various industrial environments.
Engineered for seamless integration into existing operations, these conveyor systems support diverse load capacities and environmental conditions. Industries benefit from tailored configurations that address specific layout challenges and material characteristics, ensuring smooth material flow that adapts to changing production demands. The robust construction withstands continuous operation while maintaining reliability for critical material handling tasks.
- Automotive manufacturing plants for moving vehicle components between assembly stations
- Food and beverage facilities for hygienic transportation of packaged products
- E-commerce fulfillment centers for efficient order sorting and parcel distribution
- Pharmaceutical production lines for controlled movement of sensitive materials
- Airport logistics for reliable baggage handling and cargo transfer operations
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile

AllMarc Industries, Gujarat
 Gujarat, India
Manufacturer•Distributor / Wholesaler
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Industrial Conveyor Systems For Efficient Material Handling
Industrial conveyor systems for efficient material handling in manufacturing and logistics. Customizable solutions with robust construction ensure seamless integration across industries, trusted for durability and performance.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
AllMarc Industries
 Gujarat, India
Manufacturer