IN
₹
Apparel & Fashion

Description
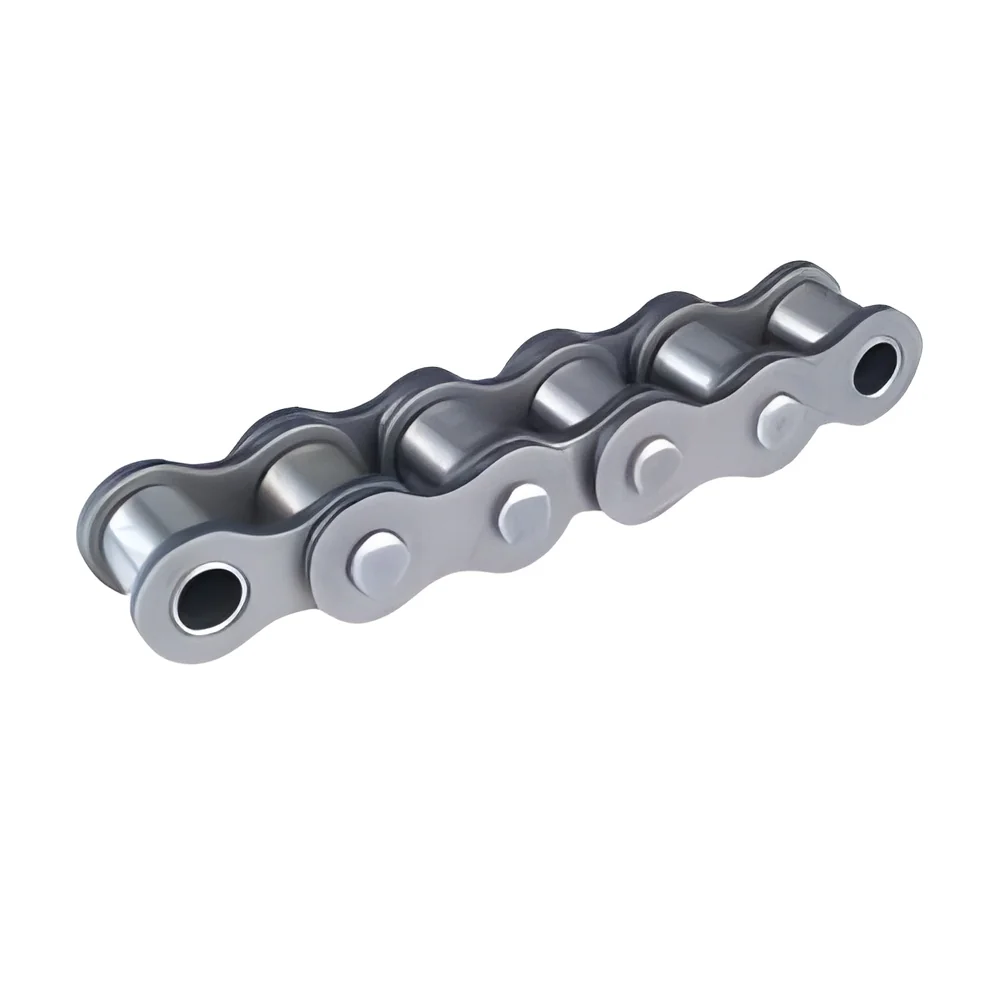
Our heavy duty conveyor long pitch chains represent industrial-grade engineering excellence for demanding material handling applications. Manufactured from premium materials, these chains deliver exceptional tensile strength and durability to withstand continuous heavy-load operations. The extended pitch design ensures smoother engagement with sprockets, significantly reducing wear and extending operational lifespan. Each chain undergoes comprehensive quality testing to guarantee performance consistency and reliability in the most challenging industrial environments. This commitment to quality ensures seamless integration with various conveyor systems while maintaining operational efficiency.

These chains serve critical functions across multiple industrial sectors where reliable material transport is essential. Automotive manufacturers utilize them for moving vehicle components through assembly processes with precision and consistency. Food processing plants benefit from their hygieni...
Our heavy duty conveyor long pitch chains represent industrial-grade engineering excellence for demanding material handling applications. Manufactured from premium materials, these chains deliver exceptional tensile strength and durability to withstand continuous heavy-load operations. The extended pitch design ensures smoother engagement with sprockets, significantly reducing wear and extending operational lifespan. Each chain undergoes comprehensive quality testing to guarantee performance consistency and reliability in the most challenging industrial environments. This commitment to quality ensures seamless integration with various conveyor systems while maintaining operational efficiency.

These chains serve critical functions across multiple industrial sectors where reliable material transport is essential. Automotive manufacturers utilize them for moving vehicle components through assembly processes with precision and consistency. Food processing plants benefit from their hygienic design and reliable performance in production line applications. Mining and construction operations rely on their robust construction for transporting heavy bulk materials under demanding conditions. Logistics and distribution centers integrate these chains into automated sorting systems to enhance operational throughput and efficiency across their facilities.

Businesses investing in our heavy duty conveyor long pitch chains gain significant operational advantages through reduced downtime and enhanced productivity. The chains' reliable performance minimizes unexpected failures, ensuring consistent material flow and protecting against costly production interruptions. Their durable construction translates to long-term cost savings through reduced maintenance requirements and extended service life. Backed by rigorous quality assurance and engineering excellence, these chains provide a trustworthy solution for optimizing material handling processes while maintaining operational safety and efficiency standards.

Key Features:
- High tensile strength construction for heavy-load applications
- Extended pitch design for smoother sprocket engagement
- Superior wear and corrosion resistance properties
- Precision manufacturing for consistent performance
- Rigorous quality testing to industry standards

Benefits:
- Reduced maintenance requirements and operational costs
- Extended service life through durable construction
- Enhanced productivity with reliable performance
- Compatibility with various conveyor systems
- Consistent operation in demanding environments
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Heavy duty conveyor long pitch chains are engineered for demanding material transport applications where reliability and strength are critical. Their robust construction handles substantial loads across extended distances while maintaining consistent performance in continuous operation environments. These chains feature enhanced wear resistance and smooth sprocket engagement for reduced maintenance needs across various industrial settings.
Multiple industries depend on these long pitch chains for their material handling infrastructure due to their proven durability and operational efficiency. Manufacturing facilities utilize them for assembly line operations while logistics centers integrate them into automated distribution systems. The chains' design ensures compatibility with existing conveyor setups, minimizing installation time and maximizing productivity across diverse operational requirements.
- Automotive manufacturing plants for moving engine components and assemblies
- Food processing facilities for conveying packaged products through production lines
- Mining operations for transporting bulk materials like ores and aggregates
- Warehouse distribution centers for automated sorting and pallet handling
- Heavy equipment manufacturing for transferring large machinery components
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Bhumi Enterprise, Maharashtra
 Maharashtra, India
Tools & Hardware•Manufacturer•Trading Company•Distributor / Wholesaler
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Main Markets
Domestic
Heavy Duty Conveyor Long Pitch Chains For Industrial Material Handling
Heavy duty conveyor long pitch chains deliver reliable industrial material handling with superior durability and seamless integration across manufacturing and material handling systems.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Bhumi Enterprise
 Maharashtra, India
Tools & HardwareManufacturer