IN
₹
Apparel & Fashion
Description
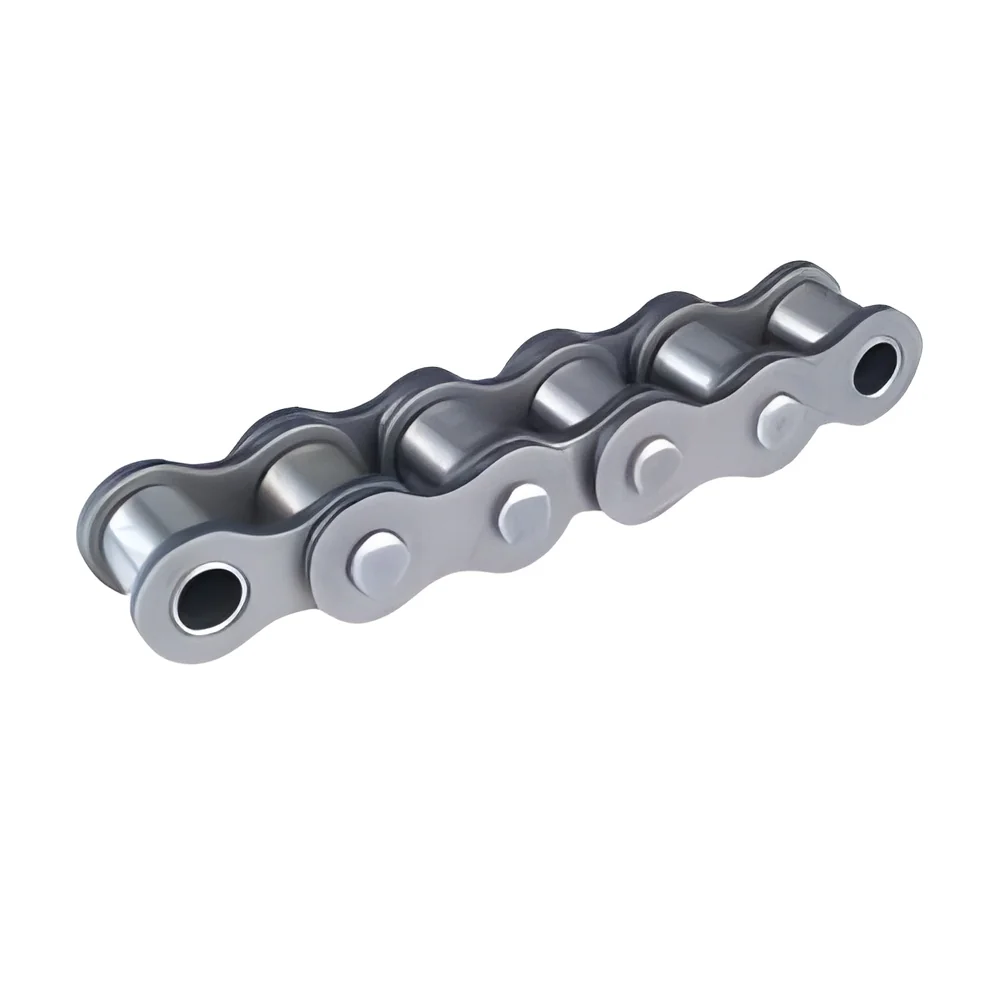
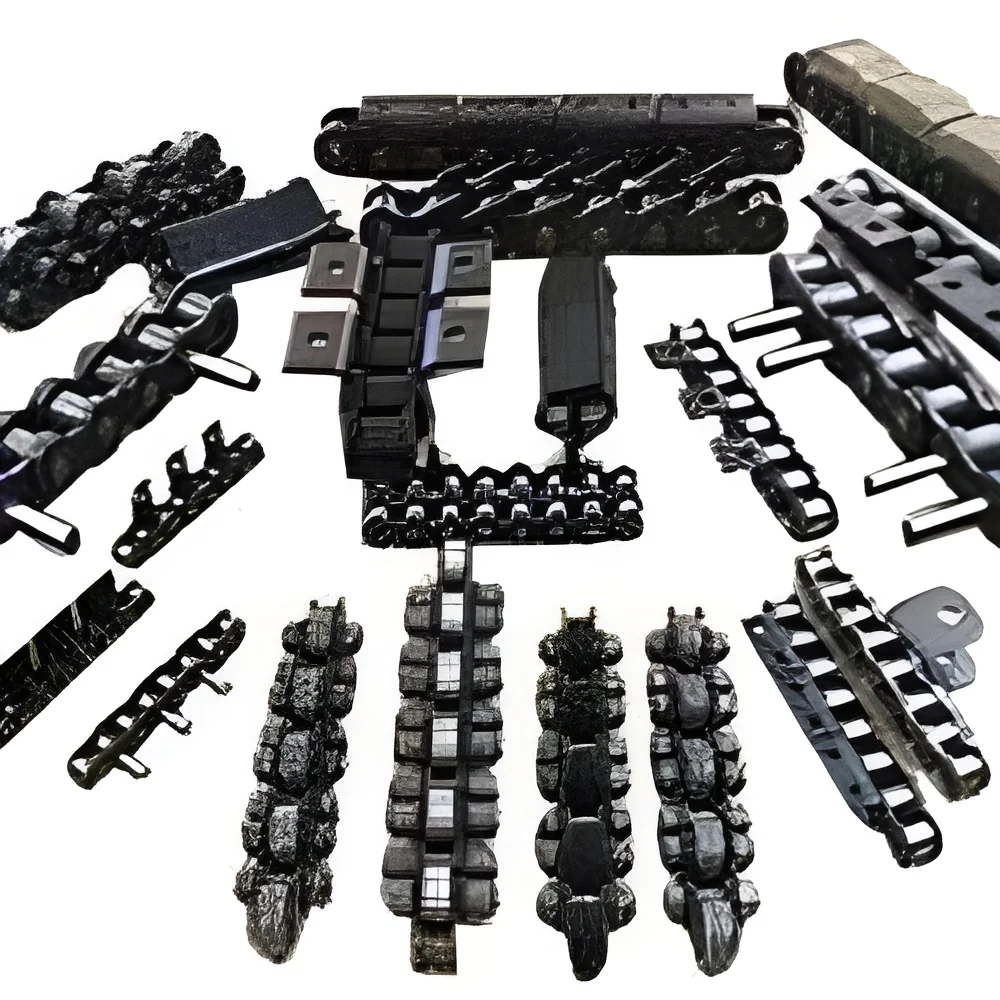
Premium conveyor chains represent advanced material handling technology designed to meet the most demanding industrial transportation requirements. Manufactured using high-quality materials and rigorous production standards, these chains undergo comprehensive quality testing to ensure exceptional performance and extended service life. The corrosion-resistant properties and ability to withstand environmental challenges make them suitable for diverse operational conditions. Their robust construction ensures reliable performance while maintaining competitive value through long-term durability and minimal maintenance needs.

These conveyor chains serve critical roles across multiple industrial sectors including automotive manufacturing, food processing, warehousing, mining, and agricultural operations. In automotive plants, they facilitate smooth movement of components through assembly processes. Food processing facilities benefit from their consistent performance and hygienic transport ca...
Premium conveyor chains represent advanced material handling technology designed to meet the most demanding industrial transportation requirements. Manufactured using high-quality materials and rigorous production standards, these chains undergo comprehensive quality testing to ensure exceptional performance and extended service life. The corrosion-resistant properties and ability to withstand environmental challenges make them suitable for diverse operational conditions. Their robust construction ensures reliable performance while maintaining competitive value through long-term durability and minimal maintenance needs.

These conveyor chains serve critical roles across multiple industrial sectors including automotive manufacturing, food processing, warehousing, mining, and agricultural operations. In automotive plants, they facilitate smooth movement of components through assembly processes. Food processing facilities benefit from their consistent performance and hygienic transport capabilities. Mining operations rely on their heavy-duty construction for moving bulk materials, while distribution centers utilize them in automated systems to enhance logistics efficiency. The versatility of these chains makes them suitable for both standard and demanding industrial applications.

The operational value of our conveyor chains lies in their ability to minimize downtime and reduce maintenance requirements. Their durable construction ensures reliable performance under continuous operation, leading to increased productivity and lower total operational costs. The chains' design focuses on seamless integration with existing systems, ensuring optimal material flow and operational efficiency. This combination of reliability, durability, and cost-effectiveness makes them a strategic investment for facilities seeking to optimize their material handling processes and improve overall operational performance.

Key Features:
- Corrosion-resistant construction for extended operational life
- Temperature variation resistance for diverse environmental conditions
- High-quality material composition ensuring strength and durability
- Engineered for smooth operation in demanding industrial settings
- Rigorous quality testing procedures for consistent reliability

Benefits:
- Reduced maintenance requirements and operational downtime
- Enhanced productivity through reliable material transport
- Long service life with consistent performance under heavy use
- Suitable for diverse industrial environments and applications
- Cost-effective operation with minimal maintenance needs
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Our conveyor chains provide robust material transport solutions across multiple industrial sectors. Engineered to handle heavy loads efficiently, they maintain reliable performance in both horizontal and inclined configurations. These chains support continuous operations in production lines and logistics systems, ensuring consistent material flow without interruptions. Their durable construction withstands demanding conditions while requiring minimal maintenance for sustained operation.
Manufacturers depend on our conveyor chains for their exceptional durability and consistent performance. The corrosion-resistant materials perform reliably across various environments, including those with moisture exposure or temperature variations. This reliability translates to reduced operational downtime and enhanced efficiency for industrial facilities. The chains' robust design ensures they can handle continuous heavy-duty use while maintaining smooth material transport throughout extended operational cycles.
- Automotive assembly lines for moving components between manufacturing stations
- Food processing facilities for transporting packaged goods in hygienic conditions
- Warehouse distribution centers for automated sorting and loading operations
- Mining operations for heavy-duty transportation of ores and bulk materials
- Agricultural processing plants for grain handling and equipment systems
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Bhumi Enterprise, Maharashtra
 Maharashtra, India
Tools & Hardware•Manufacturer•Trading Company•Distributor / Wholesaler
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Main Markets
Domestic
Premium Conveyor Chains For Material Handling Durability
Premium conveyor chains deliver reliable material handling with corrosion-resistant construction for long-lasting durability across industrial applications. Engineered for smooth operations and consistent performance in demanding environments.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Bhumi Enterprise
 Maharashtra, India
Tools & HardwareManufacturer