IN
₹
Apparel & Fashion
Description
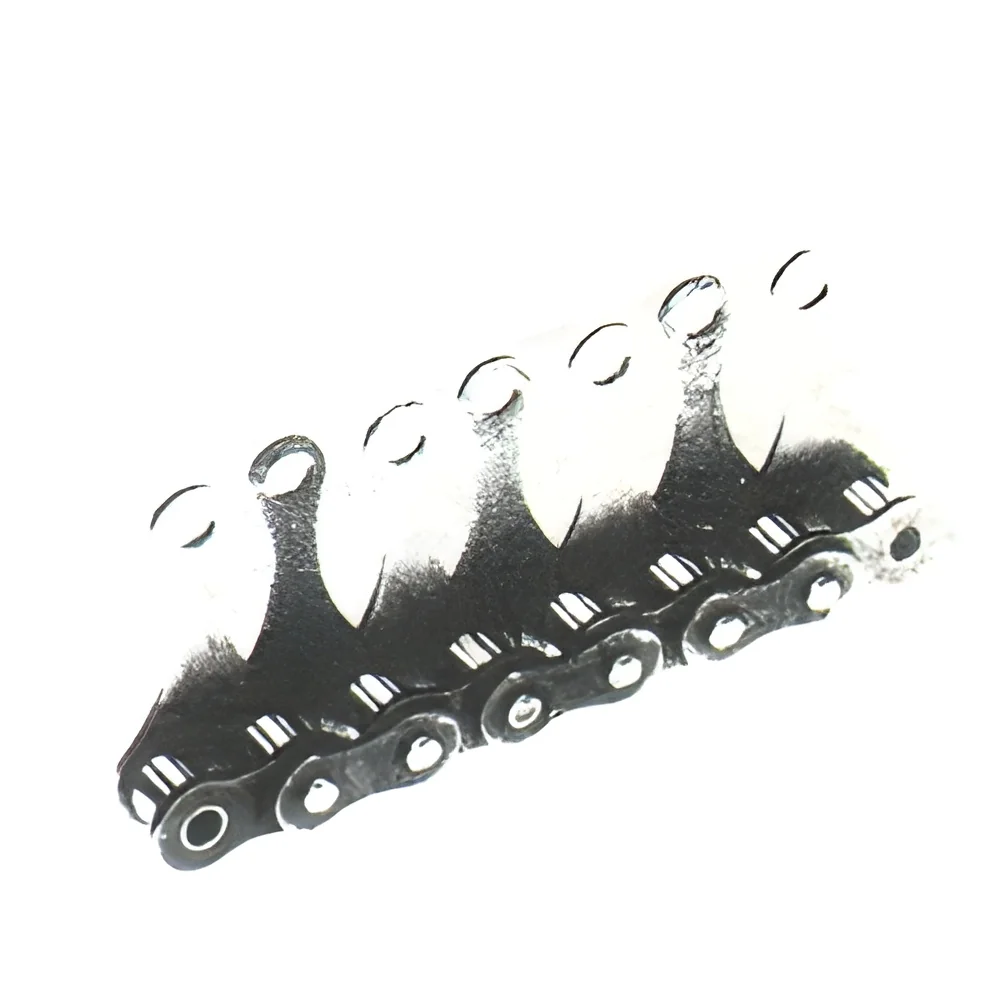
Our industrial conveyor chains are engineered to deliver reliable performance in the most demanding material handling environments. Manufactured using premium materials and advanced production techniques, these chains undergo rigorous quality control to meet exacting industry standards. Each component is precision-engineered to provide smooth, efficient material transportation while withstanding continuous industrial operation. The design focuses on minimal maintenance requirements and maximum operational uptime, making these chains an optimal choice for operations seeking to enhance their material handling processes without compromising on durability or performance.

These conveyor chains serve critical functions across multiple industrial sectors including automotive manufacturing, food processing, mining operations, warehouse logistics, and general production facilities. In automotive plants, they facilitate the seamless movement of vehicle components and assemblies. Food processing...
Our industrial conveyor chains are engineered to deliver reliable performance in the most demanding material handling environments. Manufactured using premium materials and advanced production techniques, these chains undergo rigorous quality control to meet exacting industry standards. Each component is precision-engineered to provide smooth, efficient material transportation while withstanding continuous industrial operation. The design focuses on minimal maintenance requirements and maximum operational uptime, making these chains an optimal choice for operations seeking to enhance their material handling processes without compromising on durability or performance.

These conveyor chains serve critical functions across multiple industrial sectors including automotive manufacturing, food processing, mining operations, warehouse logistics, and general production facilities. In automotive plants, they facilitate the seamless movement of vehicle components and assemblies. Food processing operations benefit from their reliable performance in transporting packaged goods. Mining and extraction industries rely on their heavy-duty construction for moving bulk materials, while distribution centers utilize them in automated sorting and packaging systems. Their adaptability makes them suitable for both precision light-duty applications and rugged heavy-duty scenarios requiring consistent performance.

The value of these conveyor chains lies in their ability to improve operational efficiency while reducing long-term operational costs. Their proven reliability means fewer breakdowns and maintenance interruptions, ensuring continuous production flow and consistent output. The chains are built to perform consistently under pressure, delivering significant return on investment through reduced downtime, lower maintenance expenses, and improved operational productivity. Operations can depend on these chains to handle demanding material transport tasks day after day, making them a valuable component for any facility prioritizing efficiency and reliability in their material handling systems.

Key Features:
- Manufactured from premium quality materials for enhanced durability and long service life
- Precision engineering ensures smooth operation and minimal maintenance requirements
- Robust construction designed specifically for heavy-duty industrial applications and environments
- Rigorous quality control processes guarantee consistent performance and reliability
- Compatible with various conveyor system types including roller, slat, and overhead configurations

Benefits:
- Enhanced operational efficiency through reliable material transportation and reduced downtime
- Lower long-term costs due to durable construction and minimal maintenance requirements
- Consistent performance under demanding conditions ensures continuous production flow
- Adaptable to various industrial applications from light packaging to heavy material handling
- Improved productivity through efficient material movement and reduced manual handling
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
These industrial conveyor chains are designed to handle demanding material transport tasks across diverse operational environments. They move raw materials, components, and finished goods efficiently in manufacturing plants, warehouses, and processing facilities. Their robust construction ensures continuous operation under significant loads and challenging conditions, maintaining consistent workflow and reducing manual handling requirements.
Specifically engineered for integration with various conveyor systems including roller, slat, and overhead configurations, these chains adapt to different operational scales. They serve light-duty packaging lines and heavy-duty mining operations with equal reliability. This versatility allows operations to optimize material flow, enhance operational efficiency, and minimize handling costs while ensuring dependable performance day after day.
- Automotive manufacturing plants for moving chassis and components along assembly lines
- Food and beverage facilities for transporting packaged products in hygienic conditions
- Mining and quarry operations for heavy-duty extraction and raw material processing
- Warehouse and distribution centers for automated sorting, palletizing, and order fulfillment
- General manufacturing facilities for assembly line production and part transportation between workstations
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile

Allied Tools & Hardware Syndicate, Andhra Pradesh
 Andhra Pradesh, India
Manufacturer•Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Industrial Conveyor Chains For Material Handling Systems
Industrial conveyor chains for material handling systems provide reliable, heavy-duty performance in demanding applications. Engineered with quality materials for seamless transportation across manufacturing, mining, and logistics operations.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Allied Tools & Hardware Syndicate
 Andhra Pradesh, India
Manufacturer