IN
₹
Apparel & Fashion
Description
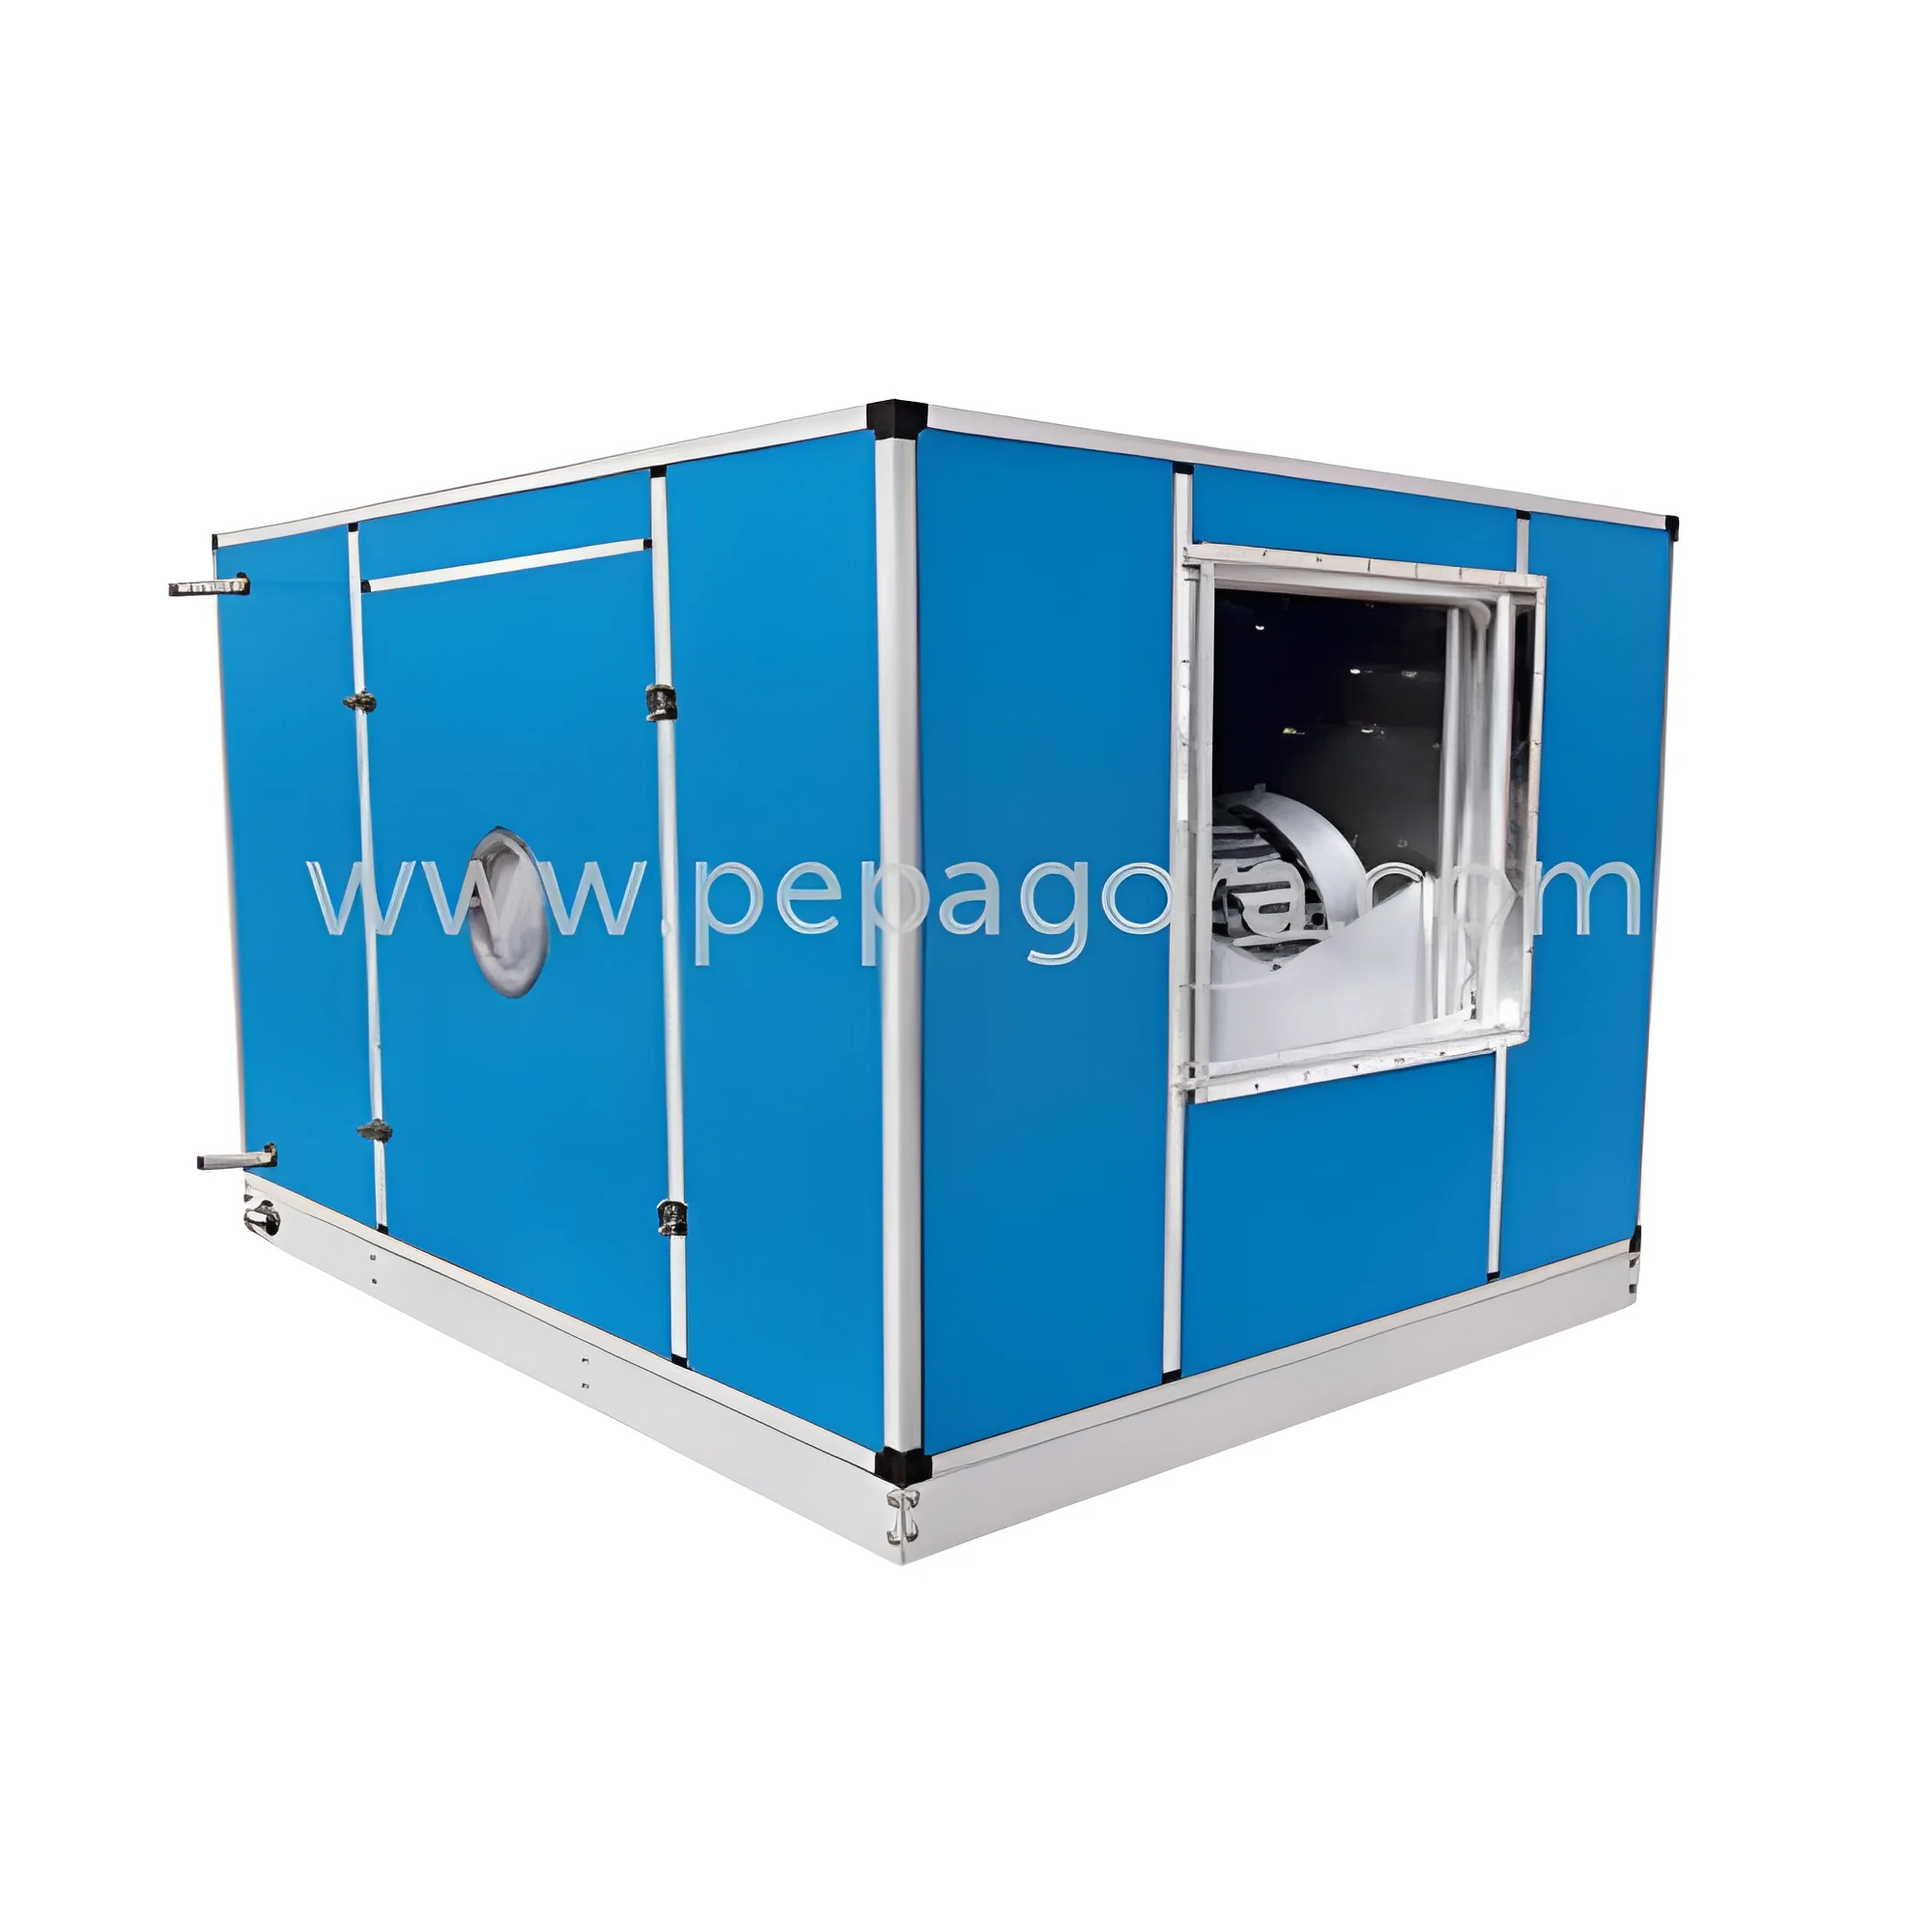
Our Premium Clean Room Air Handling Units are engineered for critical environments where air quality directly determines operational success. Built with durable galvanized iron (G.I.) construction, these units offer exceptional corrosion resistance and structural integrity for long-term reliability. They incorporate advanced multi-stage filtration and precision climate control systems to maintain stringent air purity, temperature, and humidity levels. This makes them an indispensable solution for industries where even microscopic contaminants can lead to significant product loss, safety issues, or compliance failures, providing trusted environmental control where it matters most.

These specialized air handling units serve vital functions across multiple high-stakes sectors. In pharmaceutical manufacturing, they are essential for maintaining ISO 5 to ISO 8 cleanrooms for aseptic filling, vial washing, and sterile packaging. Electronics manufacturers rely on them for semiconductor wafer...
Our Premium Clean Room Air Handling Units are engineered for critical environments where air quality directly determines operational success. Built with durable galvanized iron (G.I.) construction, these units offer exceptional corrosion resistance and structural integrity for long-term reliability. They incorporate advanced multi-stage filtration and precision climate control systems to maintain stringent air purity, temperature, and humidity levels. This makes them an indispensable solution for industries where even microscopic contaminants can lead to significant product loss, safety issues, or compliance failures, providing trusted environmental control where it matters most.

These specialized air handling units serve vital functions across multiple high-stakes sectors. In pharmaceutical manufacturing, they are essential for maintaining ISO 5 to ISO 8 cleanrooms for aseptic filling, vial washing, and sterile packaging. Electronics manufacturers rely on them for semiconductor wafer fabrication, PCB assembly, and microelectronics production where airborne particles can cause catastrophic yield loss. Healthcare facilities deploy these units in operating suites, burn units, and compounding pharmacies to safeguard patient health. They are equally critical in biotechnology for vaccine development, in aerospace for clean assembly of flight hardware, and in food processing for high-care packaging areas, ensuring each sector meets its unique regulatory and quality mandates.

The business value of these units extends beyond basic compliance to deliver measurable operational advantages. Their robust G.I. construction ensures a long service life with minimal maintenance, reducing total cost of ownership and preventing costly downtime. The energy-efficient design optimizes power consumption, lowering operational expenses without sacrificing performance. Their reliability ensures consistent product quality, higher yield rates, and reduced scrap or rework. By providing a perfectly controlled environment, they mitigate contamination risks, protect valuable research and production batches, and help facilities pass stringent audits, making them a strategic investment for safeguarding quality, reputation, and profitability.

Key Features:
- Durable galvanized iron (G.I.) construction for superior strength and corrosion resistance in demanding environments.
- Advanced multi-stage filtration system, including pre-filters, HEPA, and ULPA options, to achieve precise air purity levels.
- Integrated precision controls for accurate management of temperature, humidity, and pressure differentials.
- Customizable configurations to meet specific cleanroom classification requirements, from ISO 5 to ISO 8 and beyond.
- Energy-efficient components and design optimized to reduce operational power consumption and lifecycle costs.

Benefits:
- Ensures reliable protection of sensitive processes and products from airborne contamination and environmental fluctuations.
- Delivers long-term durability and consistent performance, minimizing maintenance needs and operational disruptions.
- Helps achieve and maintain compliance with strict international standards and regulatory requirements for critical industries.
- Reduces operational costs through energy-efficient operation and lowers the total cost of ownership over the system's lifespan.
- Provides a trusted, stable environmental foundation that enhances product quality, yield, and overall operational success.
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Clean Room Air Handling Units are engineered to maintain exacting air purity standards where contamination control is non-negotiable. They precisely regulate temperature, humidity, and particulate levels to create stable, controlled environments essential for protecting sensitive processes and ensuring product integrity across industries where quality is paramount.
These robust systems are designed for demanding applications requiring absolute environmental control. Their construction and customizable configurations adapt to various cleanroom classifications and international standards, providing consistent, reliable performance under the most rigorous operational conditions and strict regulatory compliance frameworks.
- Pharmaceutical manufacturing facilities for sterile drug production and packaging in ISO-classified cleanrooms.
- Microelectronics and semiconductor fabrication plants to prevent particle contamination that can ruin sensitive components.
- Biotechnology and life sciences research laboratories handling cell cultures and sensitive biological materials.
- Hospital operating theaters, isolation rooms, and sterile processing areas for critical infection control.
- Aerospace and precision engineering facilities for manufacturing components where zero contaminants are mandatory.
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
AM Clean Air Engineering Private Limited, Tamil Nadu
 Tamil Nadu, India
Industrial Equipment & Machinery•Manufacturer•Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Main Markets
Eastern Asia
South Asia
Southeast Asia
Clean Room Air Handling Units Premium G.I. Construction
Premium Clean Room Air Handling Units with durable G.I. construction deliver superior air quality control for critical environments in pharmaceuticals, electronics, and healthcare, ensuring reliable performance and compliance.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
AM Clean Air Engineering Private Limited
 Tamil Nadu, India
Industrial Equipment & MachineryManufacturer