IN
₹
Description
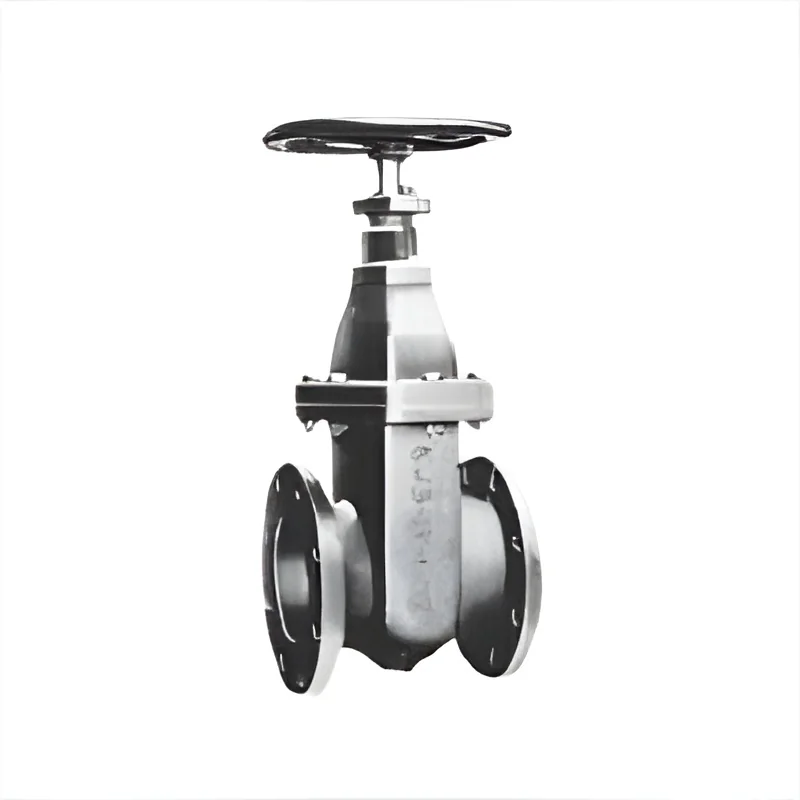
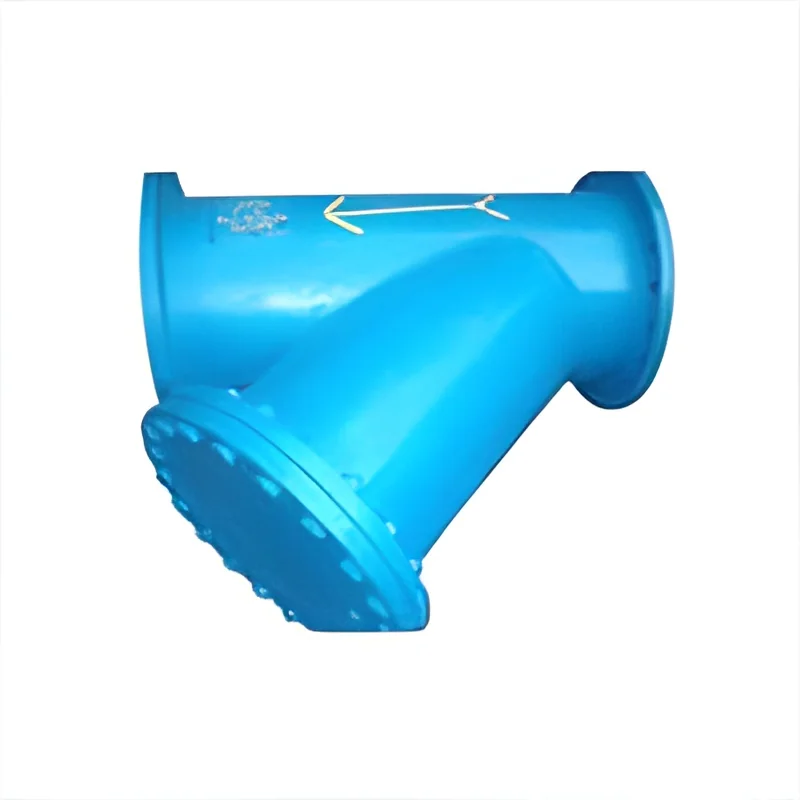
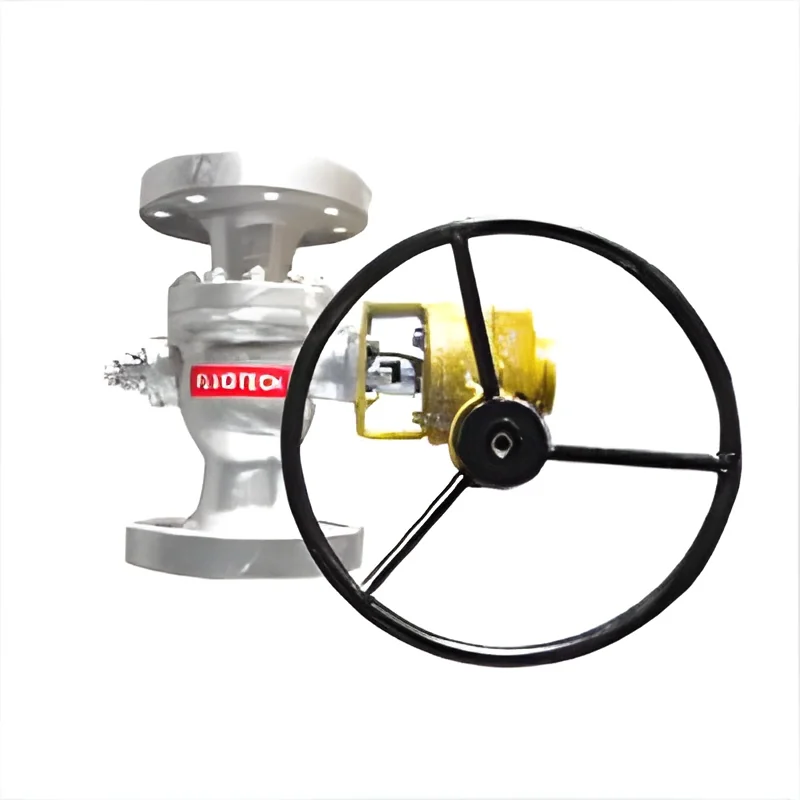
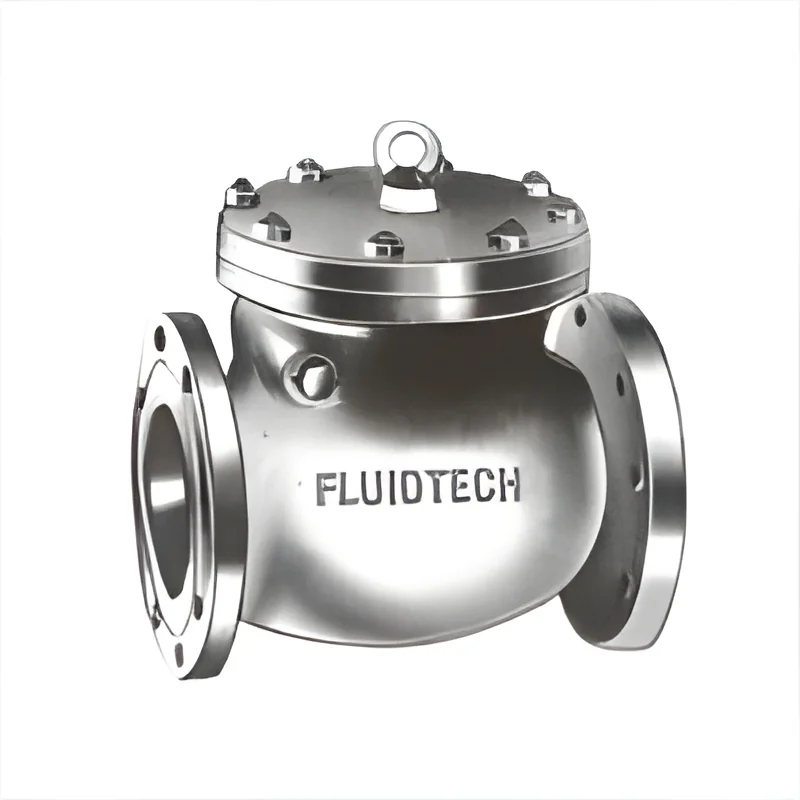
Our industrial check valves are engineered for dependable, automatic one-way flow control in demanding liquid and gas applications. Precision-built to prevent backflow, they safeguard critical components like pumps and compressors while maintaining consistent process integrity. Constructed from robust materials, these valves offer exceptional durability and reliable operation under high pressure, corrosive environments, and extreme temperatures, ensuring long-term performance with minimal maintenance requirements.

These valves are vital across numerous industries. In water and wastewater treatment plants, they protect filtration systems and pumps from reverse flow. The chemical processing industry relies on their chemical-resistant designs for safe transfer of aggressive fluids. Oil and gas sectors depend on them for pipeline and pumping station safety. They are also crucial in HVAC systems for energy efficiency, in power generation for steam control, and in mining for handling abrasi...
Our industrial check valves are engineered for dependable, automatic one-way flow control in demanding liquid and gas applications. Precision-built to prevent backflow, they safeguard critical components like pumps and compressors while maintaining consistent process integrity. Constructed from robust materials, these valves offer exceptional durability and reliable operation under high pressure, corrosive environments, and extreme temperatures, ensuring long-term performance with minimal maintenance requirements.

These valves are vital across numerous industries. In water and wastewater treatment plants, they protect filtration systems and pumps from reverse flow. The chemical processing industry relies on their chemical-resistant designs for safe transfer of aggressive fluids. Oil and gas sectors depend on them for pipeline and pumping station safety. They are also crucial in HVAC systems for energy efficiency, in power generation for steam control, and in mining for handling abrasive slurries, demonstrating their versatility and critical role in industrial operations.

For serious buyers, these check valves represent a smart investment in operational reliability and cost reduction. Their robust construction minimizes failure risks and associated downtime, protecting larger capital equipment. The focus on quality and reliability delivers clear business value by enhancing system safety, reducing lifetime maintenance costs, and ensuring uninterrupted production. This commitment to durability and performance makes them a trusted choice for demanding industrial environments.

Key Features:
- Robust cast steel or stainless steel body construction for maximum durability and pressure handling.
- Multiple material options including brass, stainless steel, and special alloys for corrosion resistance.
- Variety of seat materials like EPDM, Viton, and PTFE tailored for specific fluid compatibility.
- Available in various sizes, end connections, and pressure ratings to meet project requirements.
- Engineered for simple installation, easy maintenance, and long-term, trouble-free service life.

Benefits:
- Prevents backflow to protect pumps, compressors, and other critical equipment from damage.
- Reduces maintenance costs and avoids costly unplanned shutdowns in industrial processes.
- Ensures operational safety and process integrity across diverse fluid handling applications.
- Enhances system efficiency and longevity with durable, corrosion-resistant construction.
- Provides reliable performance in high-pressure, high-temperature, and corrosive environments.
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Industrial check valves are essential for maintaining unidirectional flow and preventing damaging backflow in piping systems. They automatically protect pumps, compressors, and other critical equipment from reverse flow, pressure surges, and potential failure. This ensures continuous, safe operation across various industrial processes without needing external power or control systems, enhancing system integrity and operational safety.
These valves are specified for diverse applications due to their reliability and versatility. They handle aggressive chemicals, high-purity water, abrasive slurries, and high-pressure steam, safeguarding entire systems from contamination and damage. Industries rely on them to reduce maintenance costs, avoid unplanned shutdowns, and ensure efficient fluid handling, making them a fundamental component in any industrial infrastructure.
- Preventing backflow and protecting pumps in municipal water treatment and distribution systems.
- Ensuring one-way flow in chemical processing, transfer lines, and dosing systems.
- Safeguarding compressors and preventing reverse flow in oil and gas pipeline networks.
- Maintaining efficiency and preventing energy loss in HVAC and heating systems.
- Handling abrasive slurries and process fluids in mining and mineral extraction operations.
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Fluidtech Valves, Maharashtra
 Maharashtra, India
Industrial Equipment & Machinery•Manufacturer•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Main Markets
South Asia
Industrial Check Valves For Reliable One Way Flow Control
Industrial check valves ensure reliable one-way flow control for liquids and gases. Durable construction, trusted for water treatment, chemical processing, oil and gas applications. Ideal for protecting pumps and compressors.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Fluidtech Valves
 Maharashtra, India
Industrial Equipment & MachineryManufacturer