IN
₹
Apparel & Fashion
Description
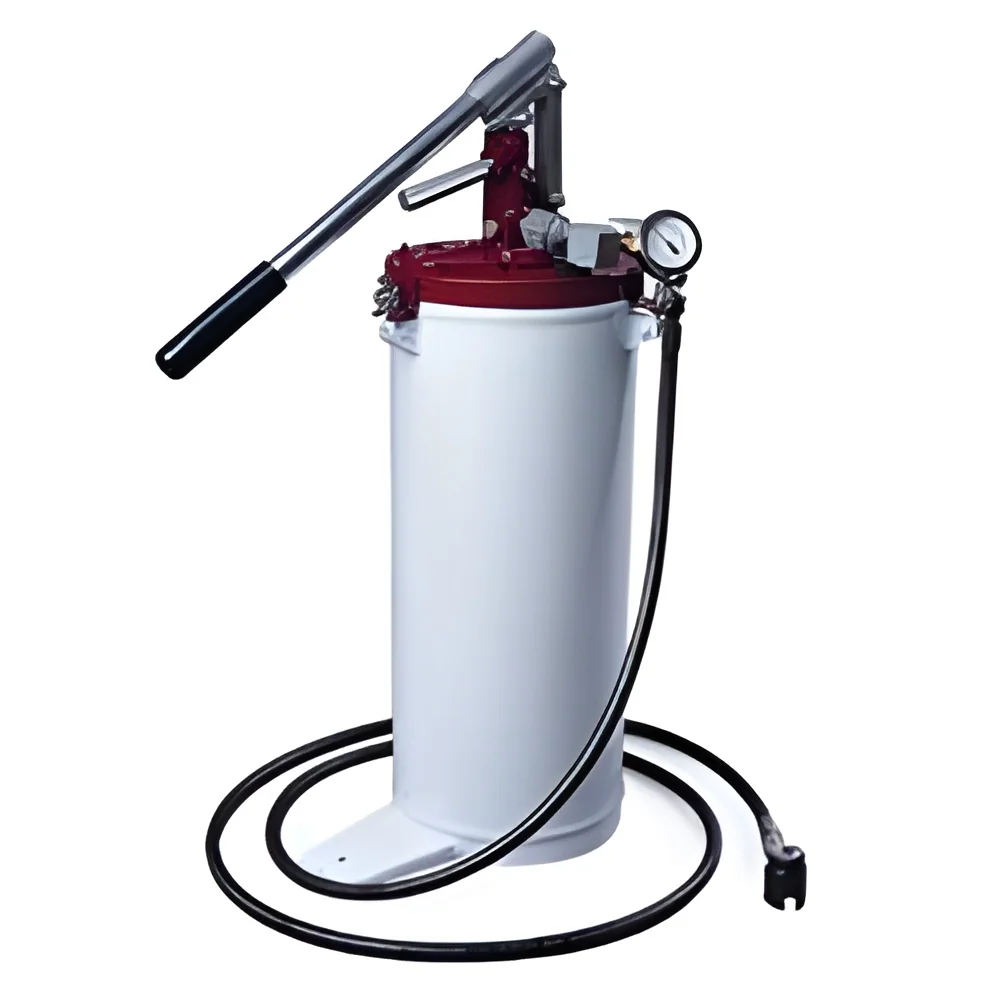
The Industrial Heavy Duty Bucket Pump is a precision-engineered manual transfer solution designed for safety, efficiency, and reliability when moving liquids from containers like drums, pails, and barrels. Constructed from industrial-grade materials selected for durability and chemical resistance, it handles a broad spectrum of substances—from volatile solvents and aggressive chemicals to viscous oils and sensitive food-grade products. Its robust build ensures leak-proof operation and an extended service life, directly reducing operational downtime and long-term maintenance costs. This pump is an indispensable tool for any facility requiring controlled, manual fluid handling with a paramount focus on operator safety, product integrity, and process consistency.

This bucket pump sees widespread adoption across multiple critical industries due to its proven versatility and dependable performance. In chemical processing and manufacturing, it is trusted for transferring acids, alkalis, and...
The Industrial Heavy Duty Bucket Pump is a precision-engineered manual transfer solution designed for safety, efficiency, and reliability when moving liquids from containers like drums, pails, and barrels. Constructed from industrial-grade materials selected for durability and chemical resistance, it handles a broad spectrum of substances—from volatile solvents and aggressive chemicals to viscous oils and sensitive food-grade products. Its robust build ensures leak-proof operation and an extended service life, directly reducing operational downtime and long-term maintenance costs. This pump is an indispensable tool for any facility requiring controlled, manual fluid handling with a paramount focus on operator safety, product integrity, and process consistency.

This bucket pump sees widespread adoption across multiple critical industries due to its proven versatility and dependable performance. In chemical processing and manufacturing, it is trusted for transferring acids, alkalis, and solvents while effectively minimizing fume exposure and preventing dangerous spills. Pharmaceutical and cosmetic producers utilize it for handling sensitive ingredients and formulations under clean, controlled conditions. The food and beverage sector relies on it for hygienic dispensing of oils, flavors, and syrups without risk of contamination. Furthermore, it is extensively used in agriculture for pesticides and fertilizers, in automotive and industrial maintenance for lubricants and fluids, and in printing and coating operations for inks and finishes. Its broad applicability makes it a fundamental component in production, packaging, and maintenance lines globally.

The core business value of this heavy-duty pump lies in its direct contribution to enhanced operational efficiency, guaranteed workplace safety, and the protection of valuable inventory. By enabling precise, controlled liquid dispensing, it significantly reduces product waste and minimizes the financial and environmental risks associated with spills or cross-contamination. Its durable, industrial-grade construction translates to a lower total cost of ownership, delivering an excellent return on investment through reduced replacement frequency and minimal upkeep requirements. For procurement managers and operations directors, investing in this pump means acquiring a proven, reliable asset that meets stringent industry standards for safety and performance. Its suitability for harsh and demanding environments makes it a smart, low-risk investment that supports smooth, uninterrupted operations.

Key Features:
- Constructed from industrial-grade, corrosion-resistant materials for long-lasting durability in harsh chemical environments.
- Leak-proof design featuring secure seals and robust connections to prevent spills and ensure maximum operator safety.
- Compatible with a wide range of standard container sizes including 5-gallon pails, 30-55 gallon drums, and common IBCs.
- Engineered to handle diverse fluid types, from thin solvents to viscous oils and food-grade liquids, with reliable performance.
- Features an ergonomic handle and user-friendly pumping mechanism designed to reduce operator fatigue during extended use.

Benefits:
- Enhances workplace safety by minimizing operator exposure to hazardous chemicals and preventing dangerous liquid spills.
- Reduces product waste and loss through precise, controlled dispensing, leading to direct cost savings on materials.
- Delivers reliable, consistent performance in demanding industrial settings, ensuring process continuity and reducing downtime.
- Offers a durable, long-service-life solution that lowers the total cost of ownership through reduced maintenance and replacement needs.
- Provides a versatile and trusted tool that meets the stringent handling requirements of chemical, food, and pharmaceutical industries.
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
These industrial bucket pumps are engineered for safe and efficient handling of diverse fluids, from aggressive chemicals to sensitive food-grade liquids. Their design minimizes waste, reduces operator exposure to hazardous materials, and ensures consistent, reliable performance in demanding environments. This makes them essential for maintaining workflow integrity, protecting product quality, and upholding strict safety standards across various operations.
These robust pumps serve a wide range of industries due to their versatile and durable construction. They are commonly used in chemical manufacturing, pharmaceutical production, food and beverage processing, agriculture, and automotive sectors. The pump design allows for straightforward integration into existing systems, providing a dependable solution for tasks like decanting, dispensing, and transferring liquids from standard drums, barrels, and intermediate bulk containers (IBCs) with precision and control.
- Safe transfer of solvents, acids, and alkalis in chemical manufacturing plants and laboratory environments.
- Hygienic dispensing of edible oils, syrups, and liquid ingredients within food and beverage processing facilities.
- Precise handling of lubricants, adhesives, and sealants on automotive assembly lines and in maintenance workshops.
- Efficient decanting and application of fertilizers, pesticides, and herbicides in agricultural operations.
- Reliable transfer of water-based paints, inks, dyes, and coatings in printing, painting, and industrial finishing processes.
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Petece Enviro Engineers, Tamil Nadu
 Tamil Nadu, India
Electronics & Electrical•Trading Company•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Main Markets
North America
Northern Europe
Mid East
Southern Europe
Eastern Europe
South Asia
Western Europe
Africa
Domestic
Industrial Heavy Duty Bucket Pumps For Chemical Food Fluid Transfer
Industrial heavy duty bucket pumps for reliable chemical, food, and fluid transfer. Built for safety and efficiency in demanding processing applications with durable, leak-proof construction.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Petece Enviro Engineers
 Tamil Nadu, India
Electronics & ElectricalTrading Company