IN
₹
Apparel & Fashion

Description
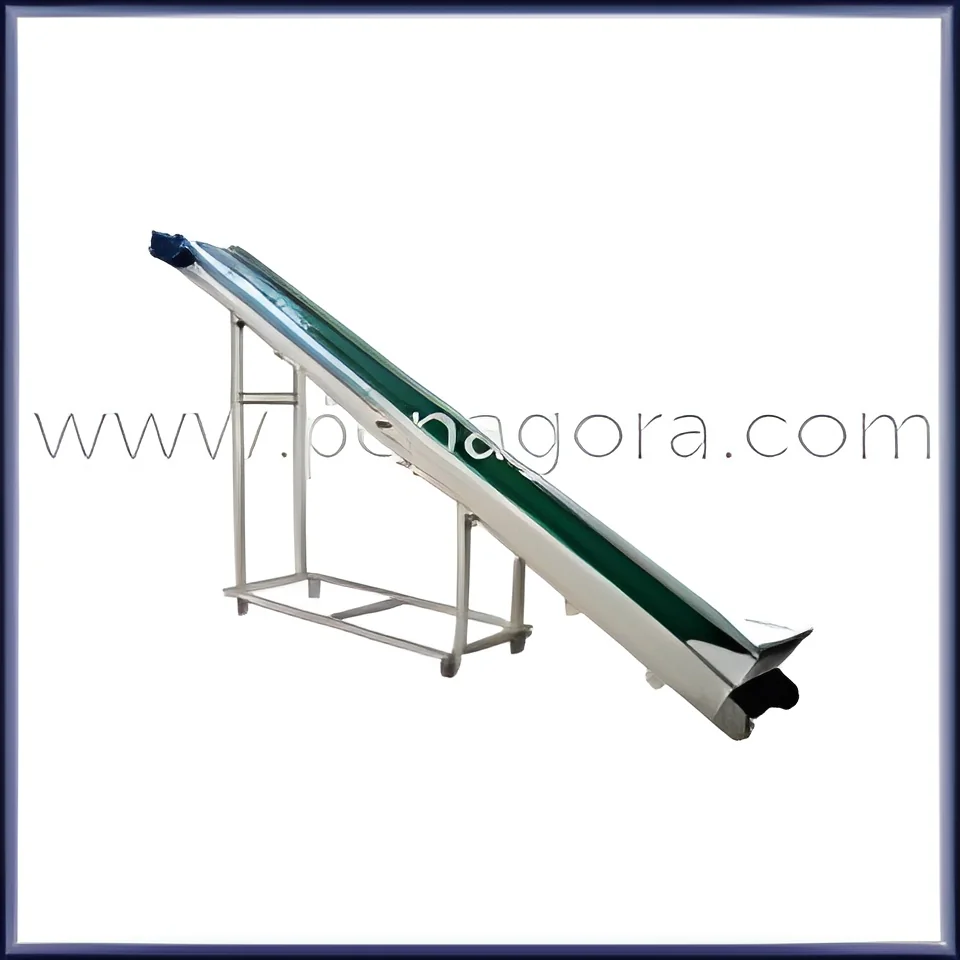
The Industrial Bulk Material Vertical Transport Bucket Elevator represents a specialized solution for moving bulk materials vertically in industrial settings where floor space is limited and efficiency is paramount. This equipment utilizes a continuous chain or belt with attached buckets to lift materials from lower to higher levels, providing a compact alternative to inclined conveyors that require more horizontal space. Engineered for reliability and durability, these systems handle a wide range of materials including grains, ores, powders, and aggregates with consistent performance. The vertical design minimizes the system's footprint while maximizing material flow capacity, making it ideal for facilities where space optimization directly impacts operational efficiency. With robust construction and precision engineering, this bucket elevator ensures smooth, continuous operation that integrates seamlessly into existing production lines and material handling processes.

Multiple indus...
The Industrial Bulk Material Vertical Transport Bucket Elevator represents a specialized solution for moving bulk materials vertically in industrial settings where floor space is limited and efficiency is paramount. This equipment utilizes a continuous chain or belt with attached buckets to lift materials from lower to higher levels, providing a compact alternative to inclined conveyors that require more horizontal space. Engineered for reliability and durability, these systems handle a wide range of materials including grains, ores, powders, and aggregates with consistent performance. The vertical design minimizes the system's footprint while maximizing material flow capacity, making it ideal for facilities where space optimization directly impacts operational efficiency. With robust construction and precision engineering, this bucket elevator ensures smooth, continuous operation that integrates seamlessly into existing production lines and material handling processes.

Multiple industries depend on vertical bucket elevators for their material handling needs due to the equipment's versatility and reliability. In agricultural operations, these systems move grains, seeds, and animal feed between storage, drying, and processing equipment while maintaining product integrity. Mining operations utilize them to transport extracted ores, coal, and minerals from extraction points to processing facilities, handling abrasive materials with minimal wear. Food processing plants rely on these elevators for hygienic transfer of ingredients like sugar, flour, and spices between different production stages. Chemical manufacturers use them to move powders, pellets, and compounds safely between processing equipment, while construction material producers handle cement, sand, and aggregates in batching plants. Each industry benefits from the elevator's ability to handle specific material characteristics while maintaining consistent throughput and operational reliability.

For businesses investing in material handling equipment, the Industrial Bulk Material Vertical Transport Bucket Elevator delivers substantial value through operational efficiency, reduced labor requirements, and long-term reliability. The system's robust construction ensures minimal maintenance and extended service life, providing a solid return on investment through consistent performance. By automating vertical material transfer, businesses reduce manual handling costs while increasing throughput and minimizing product loss through spillage. The elevator's design allows for integration with automation systems and sensing devices, enhancing process control and operational visibility. This combination of durability, efficiency, and integration capability makes it a trustworthy solution for serious buyers who prioritize equipment reliability and long-term operational performance in their material handling systems.

Key Features:
- Vertical material transport design optimizes floor space utilization in industrial facilities
- Robust construction with durable components withstands demanding operating environments
- Continuous operation ensures smooth material flow between different processing levels
- Handles diverse materials from fine powders to coarse aggregates with minimal spillage
- Automation-ready design allows integration with control systems and sensing devices

Benefits:
- Maximizes floor space efficiency by utilizing vertical rather than horizontal transport
- Reduces manual labor requirements through automated material handling
- Minimizes product loss and contamination with enclosed, controlled transfer
- Increases operational throughput with continuous, reliable material movement
- Provides long-term reliability with durable construction and minimal maintenance needs
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
The Industrial Bulk Material Vertical Transport Bucket Elevator provides efficient vertical movement of diverse materials while conserving valuable floor space in industrial facilities. Its continuous operation ensures smooth material flow between different processing levels, eliminating bottlenecks and reducing manual handling requirements. The system's robust construction withstands demanding environments while maintaining consistent performance for production lines that depend on reliable material transfer.
This vertical transport solution serves multiple industries by handling everything from fine powders to coarse aggregates with minimal spillage and contamination. Its design accommodates various material characteristics and operational requirements, making it adaptable to specific processing needs. The elevator's reliable performance supports high-volume operations where downtime directly impacts productivity and profitability.
- Agriculture: Vertically transporting grains, seeds, and animal feed between storage silos, dryers, and processing equipment in farming operations.
- Mining: Elevating ores, coal, and extracted minerals from underground operations to surface processing facilities and storage areas.
- Food Processing: Moving sugar, flour, spices, and other ingredients between mixing, packaging, and storage levels in food production plants.
- Chemical Manufacturing: Transferring powders, pellets, and chemical compounds between reaction vessels, dryers, and packaging stations safely.
- Construction Materials: Handling cement, sand, aggregates, and other building materials in batching plants and mixing facilities for concrete production.
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Advance Equipment Co, Maharashtra
 Maharashtra, India
Industrial Equipment & Machinery•Manufacturer•Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Industrial Bulk Material Vertical Transport Bucket Elevator
Industrial Bulk Material Vertical Transport Bucket Elevator efficiently moves grains, ores, powders, and aggregates vertically in tight spaces for agriculture, mining, and manufacturing industries with reliable, automation-ready performance.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Advance Equipment Co
 Maharashtra, India
Industrial Equipment & MachineryManufacturer