IN
₹
Apparel & Fashion
Description
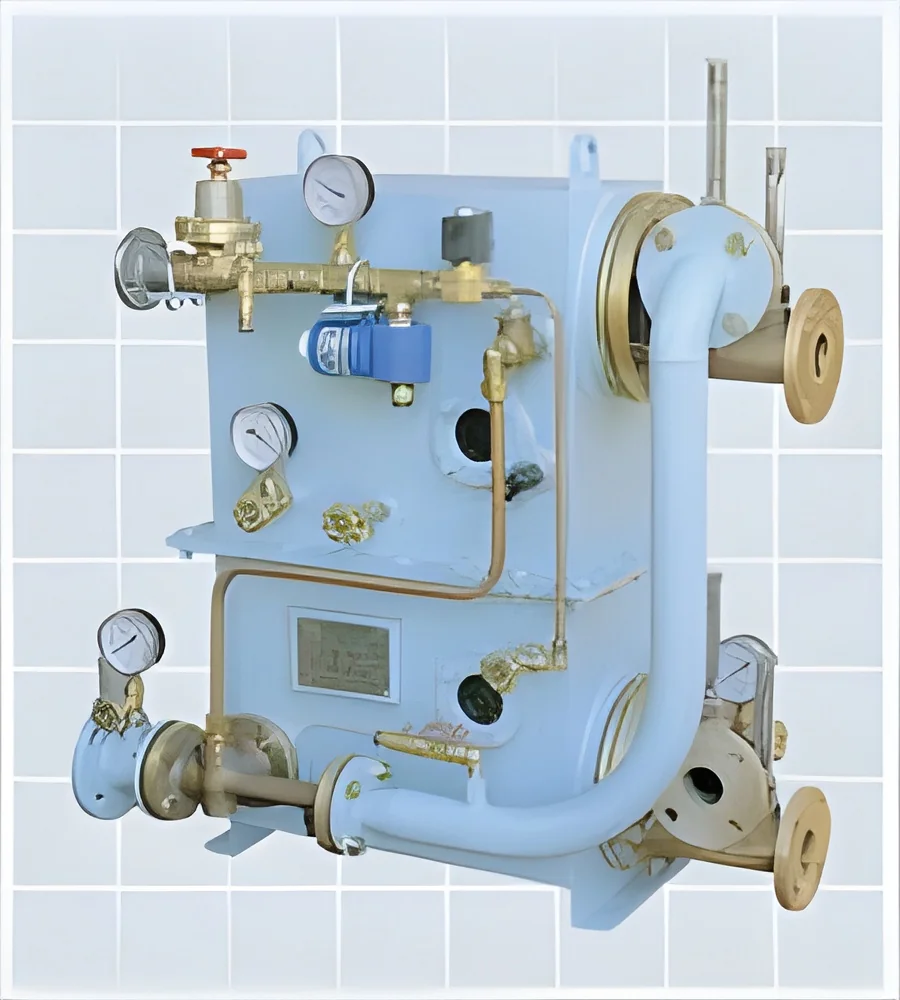
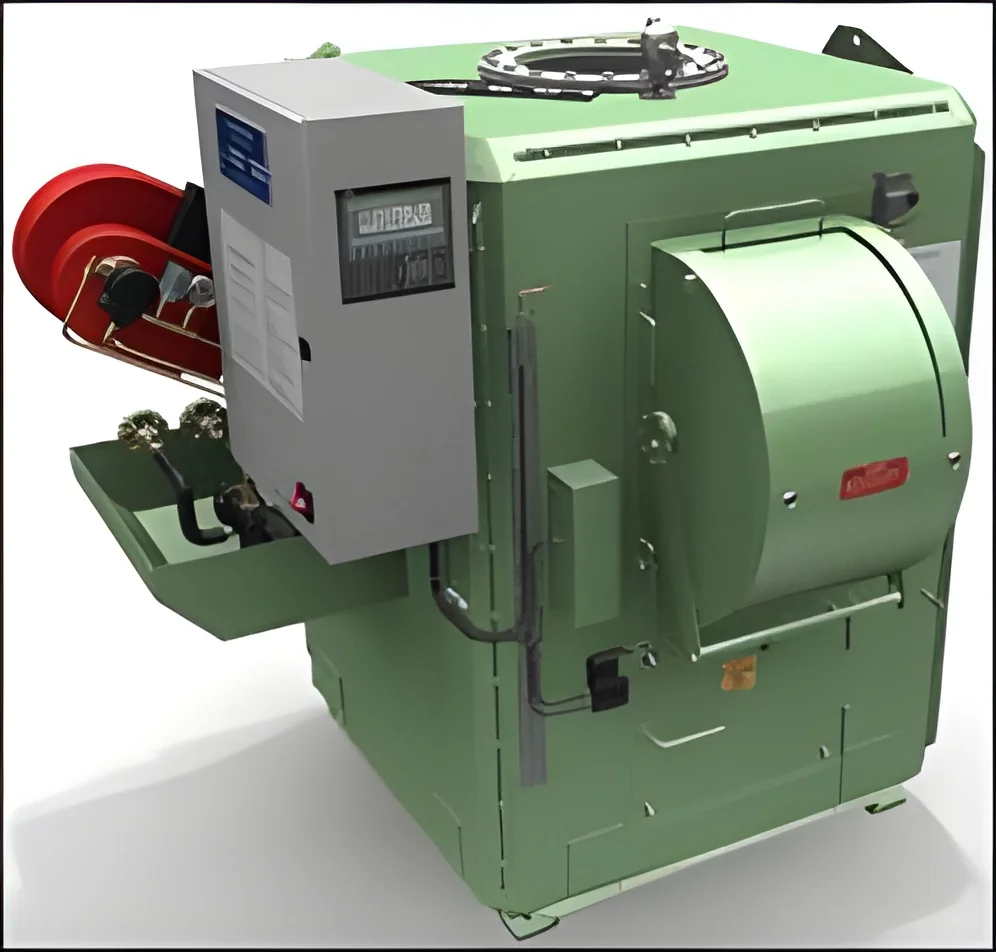
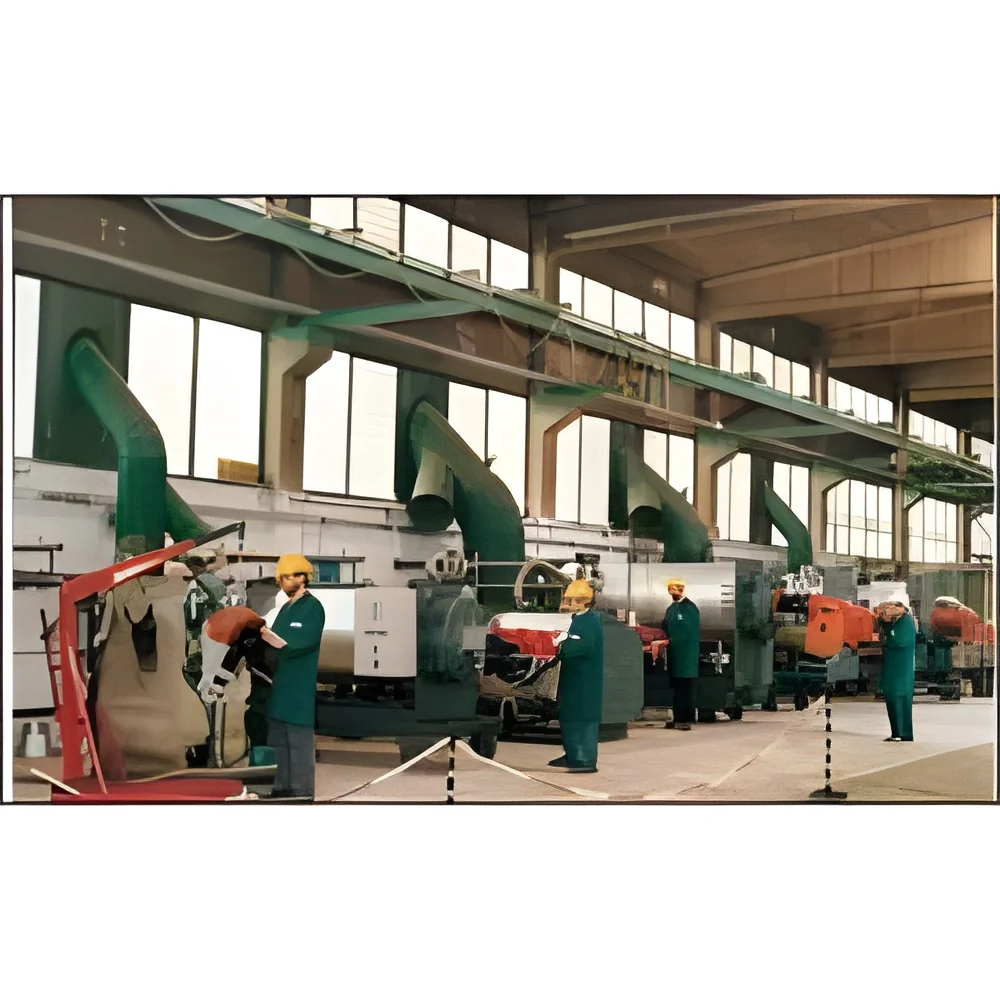
Our industrial boilers represent advanced thermal engineering solutions designed for demanding manufacturing and heating applications. These systems deliver reliable steam generation and hot water supply through optimized combustion technology and durable construction. Engineered to minimize thermal inertia while maximizing heat transfer efficiency, they provide consistent performance across extended operational periods. The integration of high-quality burners and precision components ensures stable output for industrial processes requiring controlled thermal energy. These boilers are built to withstand continuous operation in challenging industrial environments while maintaining energy efficiency and operational reliability.

These heating systems serve critical functions across multiple industrial sectors where thermal energy is essential for production processes. In manufacturing facilities, they provide steam for machinery operation, component cleaning, and production line heating....
Our industrial boilers represent advanced thermal engineering solutions designed for demanding manufacturing and heating applications. These systems deliver reliable steam generation and hot water supply through optimized combustion technology and durable construction. Engineered to minimize thermal inertia while maximizing heat transfer efficiency, they provide consistent performance across extended operational periods. The integration of high-quality burners and precision components ensures stable output for industrial processes requiring controlled thermal energy. These boilers are built to withstand continuous operation in challenging industrial environments while maintaining energy efficiency and operational reliability.

These heating systems serve critical functions across multiple industrial sectors where thermal energy is essential for production processes. In manufacturing facilities, they provide steam for machinery operation, component cleaning, and production line heating. Food processing plants utilize them for cooking, pasteurization, and sterilization operations requiring precise temperature control. Textile manufacturers depend on these boilers for dye fixation, fabric drying, and finishing processes. Chemical and pharmaceutical industries employ them for reaction heating, distillation, and equipment sterilization. Commercial and institutional facilities rely on these systems for space heating, domestic hot water, and sanitation requirements in large-scale operations.

Businesses select these industrial boilers for their proven reliability, operational efficiency, and long-term cost-effectiveness. The design focuses on reducing lifecycle costs through energy-efficient operation, minimal maintenance requirements, and durable construction that withstands industrial demands. Quality components from trusted suppliers ensure consistent performance and simplify maintenance procedures. These boilers deliver reliable thermal energy that supports production continuity and manufacturing quality standards. Their robust construction and efficient operation translate into reduced operational expenses and dependable service throughout extended product lifecycles.

Key Features:
- Optimized combustion chamber design for enhanced thermal exchange efficiency
- High-performance burners supporting multiple fuel types and configurations
- Durable construction with quality components from established suppliers
- Engineered for continuous operation in demanding industrial environments
- Designed to minimize thermal inertia and maximize energy utilization

Benefits:
- Consistent steam generation supporting uninterrupted manufacturing operations
- Reduced lifecycle costs through energy efficiency and minimal maintenance
- Reliable performance ensuring production continuity and quality standards
- Flexible fuel options adapting to various industrial requirements and locations
- Durable construction providing long service life in challenging environments
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
These industrial boilers provide robust steam and hot water generation for continuous manufacturing operations. Their efficient design ensures stable thermal output for production lines, sanitation systems, and facility heating needs across various industrial settings. Built with durable components and optimized combustion chambers, they maintain consistent performance in demanding environments while minimizing energy consumption and operational interruptions.
Engineered for flexibility across different fuel types and operational requirements, these boilers adapt to specific industrial processes. They serve critical heating functions in production facilities where temperature control and reliable steam supply are essential for manufacturing quality and operational continuity. The design prioritizes easy maintenance and long service intervals, reducing downtime and supporting uninterrupted industrial operations throughout extended production cycles.
- Steam generation for food processing, cooking, and sterilization operations
- Thermal energy for textile manufacturing including dyeing and drying processes
- Heating systems for chemical production and pharmaceutical manufacturing
- Hot water supply for large commercial facilities and healthcare institutions
- Process heating in automotive manufacturing and industrial cleaning applications
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Capttronics Solution India Private Limited, Maharashtra
 Maharashtra, India
Home & Lifestyle•Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Industrial Boilers For Manufacturing And Heating Applications
Premium industrial boilers for manufacturing and heating applications deliver reliable steam generation with low lifecycle costs. Engineered for diverse industrial processes requiring consistent thermal energy.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Capttronics Solution India Private Limited
 Maharashtra, India
Home & LifestyleDistributor / Wholesaler