IN
₹
Apparel & Fashion
Description
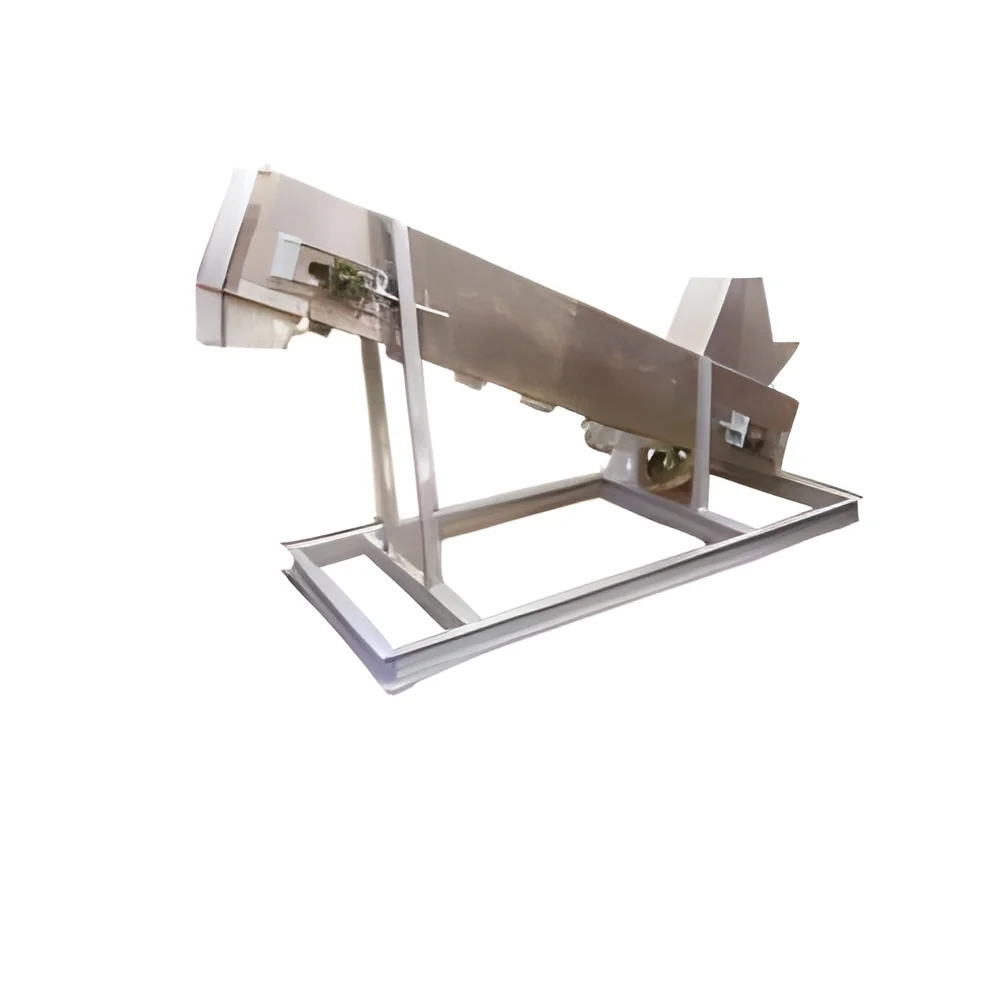
Our premium bulk material handling belt conveyor systems are manufactured entirely in-house, providing complete quality control and reliable performance for industrial operations. Each system features durable rollers, idlers, head/tail pulleys, snub pulleys, and self-aligning components engineered for longevity and efficiency. Designed to transport bulk materials smoothly across various distances and elevations, these conveyors significantly reduce manual labor while enhancing operational throughput. Available in both portable and fixed configurations with belt widths ranging from 300mm to 1000mm, they offer the flexibility needed to meet diverse layout requirements and capacity demands across different industrial settings.

These belt conveyor systems serve critical functions across multiple industries where efficient material movement is essential. In mining operations, they transport ores, coal, and minerals from extraction points to processing areas with minimal spillage and maximu...
Our premium bulk material handling belt conveyor systems are manufactured entirely in-house, providing complete quality control and reliable performance for industrial operations. Each system features durable rollers, idlers, head/tail pulleys, snub pulleys, and self-aligning components engineered for longevity and efficiency. Designed to transport bulk materials smoothly across various distances and elevations, these conveyors significantly reduce manual labor while enhancing operational throughput. Available in both portable and fixed configurations with belt widths ranging from 300mm to 1000mm, they offer the flexibility needed to meet diverse layout requirements and capacity demands across different industrial settings.

These belt conveyor systems serve critical functions across multiple industries where efficient material movement is essential. In mining operations, they transport ores, coal, and minerals from extraction points to processing areas with minimal spillage and maximum efficiency. Food processing facilities utilize them for hygienic handling of ingredients and finished products, while agricultural operations rely on them for grain and produce transport. Manufacturing plants integrate these systems into assembly lines for raw material supply, and logistics centers use them for sorting and distribution tasks. Their versatility makes them indispensable for maintaining continuous material flow in high-demand industrial environments.

Businesses investing in our belt conveyor systems gain enhanced operational reliability, reduced handling costs, and increased productivity. The in-house manufacturing approach ensures each component meets stringent quality standards, resulting in systems that withstand demanding conditions with minimal maintenance requirements. Built with high-grade materials and precision engineering, these conveyors minimize downtime and operational disruptions. Their adaptability to various material types and industry applications makes them a valuable long-term asset for companies seeking to scale operations, improve safety, and optimize material handling efficiency for sustainable growth.

Key Features:
- In-house manufactured rollers, idlers, and pulleys ensuring consistent quality and reliability
- Self-aligning idler systems that automatically correct belt tracking to reduce wear and maintenance
- Multiple belt width options from 300mm to 1000mm to match specific capacity requirements
- Available in both portable and fixed configurations for flexible installation and mobility
- Robust construction using heavy-duty materials suitable for continuous industrial operation

Benefits:
- Enhanced operational reliability with reduced downtime and maintenance requirements
- Increased productivity through efficient, continuous bulk material transport
- Reduced manual labor costs and improved workplace safety
- Flexible configurations that adapt to existing facility layouts and space constraints
- Long service life with durable components built for demanding industrial environments
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Our heavy-duty belt conveyor systems are engineered for continuous, high-volume transport of bulk materials across demanding industrial environments. They efficiently handle everything from raw ores and minerals to processed food items and packaged goods, ensuring smooth material flow with minimal downtime. The robust construction and precision components guarantee reliable operation in harsh conditions, making them ideal for operations where consistent throughput is critical.
These systems are designed for seamless integration into existing production lines and facility layouts. With customizable belt widths and configurations, they adapt perfectly to specific capacity requirements and spatial constraints. Industries ranging from mining and agriculture to manufacturing and distribution centers rely on these conveyors to boost productivity, reduce manual labor costs, and streamline their material handling processes for improved operational efficiency.
- Transporting bulk ores, coal, and minerals in mining extraction and processing facilities
- Moving grains, cereals, flour, and packaged food products in agricultural and food processing plants
- Handling raw materials like metal scraps, aggregates, and cement in manufacturing and construction sites
- Sorting and distributing parcels, cartons, and palletized goods in logistics warehouses and distribution hubs
- Carrying fertilizers, chemicals, and bulk powders in agricultural and industrial processing operations
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Chamunda Equipment, Gujarat
 Gujarat, India
Industrial Equipment & Machinery•Manufacturer•Distributor / Wholesaler
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Main Markets
South Asia
Bulk Material Handling Belt Conveyor Systems With Rollers And Idlers
Premium bulk material handling belt conveyor systems with rollers and idlers for mining, food processing, and logistics industries. Durable, reliable, and customizable for efficient transport of raw materials and goods.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Chamunda Equipment
 Gujarat, India
Industrial Equipment & MachineryManufacturer