IN
₹
Apparel & Fashion
Description
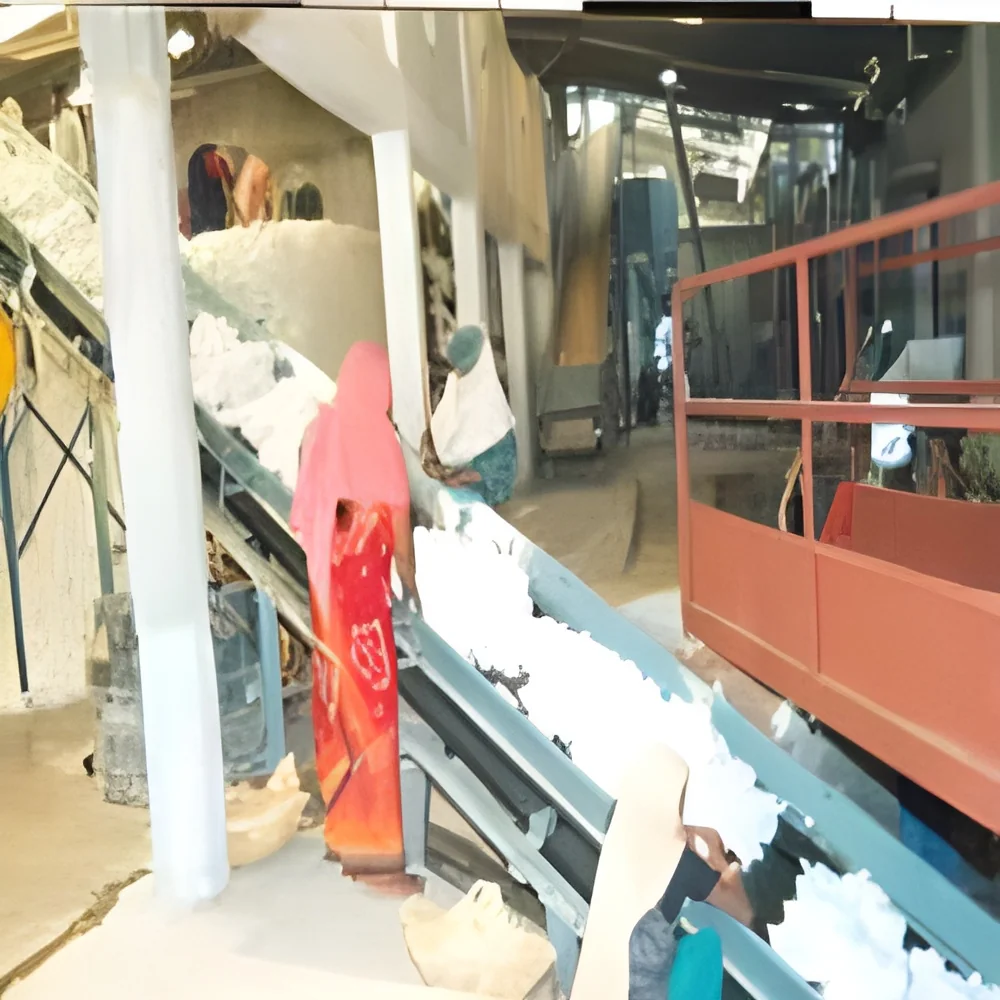
Our Heavy Duty Belt Conveyor is a purpose-built industrial solution designed for the demanding task of bulk material transportation. It efficiently handles a wide spectrum of materials, from sluggish, heavy aggregates and sticky substances to free-flowing powders and granular products, with lump sizes ranging from small to large. Engineered for both horizontal and inclined paths, this system provides a reliable, continuous flow that is essential for modern, high-volume operations. The core strength lies in its robust construction, featuring a durable belt supported by precisely aligned idlers and a strong frame, all designed to withstand heavy loads, abrasive materials, and harsh environmental conditions. This results in a conveyor that delivers consistent performance, minimal downtime, and long service life, forming the backbone of efficient material handling infrastructure.

This conveyor finds indispensable usage across heavy industries where moving large volumes of material is a da...
Our Heavy Duty Belt Conveyor is a purpose-built industrial solution designed for the demanding task of bulk material transportation. It efficiently handles a wide spectrum of materials, from sluggish, heavy aggregates and sticky substances to free-flowing powders and granular products, with lump sizes ranging from small to large. Engineered for both horizontal and inclined paths, this system provides a reliable, continuous flow that is essential for modern, high-volume operations. The core strength lies in its robust construction, featuring a durable belt supported by precisely aligned idlers and a strong frame, all designed to withstand heavy loads, abrasive materials, and harsh environmental conditions. This results in a conveyor that delivers consistent performance, minimal downtime, and long service life, forming the backbone of efficient material handling infrastructure.

This conveyor finds indispensable usage across heavy industries where moving large volumes of material is a daily operational necessity. In mining and mineral processing, it is the primary method for transporting tons of ore, coal, and overburden from pit to plant. The cement industry relies on it for the continuous flow of raw meal, clinker, and finished cement. Power plants use it for fuel handling, while ports and terminals depend on it for rapid loading and unloading of bulk carriers. Its ability to operate on inclines makes it ideal for applications where material must be elevated to silos, hoppers, or processing equipment, eliminating the need for more complex and costly lifting systems. Its versatility and reliability make it a standard fixture in any industry requiring efficient, large-scale bulk transport.

The business value delivered by this heavy-duty conveyor system is rooted in operational reliability, cost efficiency, and enhanced productivity. Its durable design minimizes unexpected breakdowns and reduces maintenance frequency, leading to higher uptime and more predictable operating costs. By automating material movement, it drastically cuts labor requirements, lowers energy consumption per ton conveyed compared to alternatives, and improves workplace safety by reducing manual handling risks. The system's smooth and controlled operation also minimizes product degradation and spillage, preserving material quality. Investing in this reliable conveyor translates into a robust, low-operational-cost solution that streamlines your core material flow, boosts throughput capacity, and provides a solid return on investment through years of dependable service.

Key Features:
- Heavy-duty construction with a robust frame and high-tensile strength belt designed to endure continuous operation under substantial loads and abrasive conditions.
- Capable of handling both horizontal and inclined transport paths, with configurations available to suit specific layout and elevation change requirements.
- Engineered to transport a wide variety of bulk materials, from fine powders and granules to large, heavy lumps, ensuring broad application suitability.
- Features precisely manufactured idlers and rollers that ensure smooth belt travel, reduce friction, and extend the lifespan of both the belt and components.
- Designed for reliable performance with minimal spillage and dust generation, incorporating effective sealing and tracking systems for clean operation.

Benefits:
- Ensures high operational uptime and consistent material flow, critical for maintaining production schedules and overall plant efficiency.
- Reduces long-term operating costs through lower energy consumption, decreased manual labor, and minimal maintenance requirements.
- Enhances workplace safety by automating the movement of heavy, hazardous, or dusty materials, limiting direct worker exposure.
- Provides a durable and long-lasting solution built from quality components, offering excellent return on investment over its extended service life.
- Delivers reliable transportation with minimal product loss or damage due to spillage, preserving material integrity and reducing waste.
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
This heavy-duty belt conveyor is engineered for continuous, reliable transport of bulk materials across demanding industrial environments. Its robust construction handles everything from fine powders to large, abrasive lumps, moving materials efficiently over long distances with minimal energy consumption and operational oversight. The system's design prioritizes smooth material flow, reducing spillage and wear while maintaining consistent throughput in challenging conditions.
Versatile in application, the conveyor operates effectively in both horizontal and inclined setups, adapting to complex plant layouts and elevation changes. It serves as a critical link in material handling processes, connecting different stages of production, storage, and dispatch. By automating material movement, it significantly reduces manual labor costs, minimizes handling damage, and enhances overall workplace safety by limiting direct human interaction with heavy or hazardous materials.
- Mining and quarrying operations for transporting extracted materials like coal, metallic ores, aggregates, and overburden from excavation sites to crushers, stockpiles, or processing plants.
- Cement and construction material plants for handling raw materials such as limestone, clay, gypsum, and finished products like cement and clinker between various production and storage points.
- Power generation facilities for the continuous supply of fuel, including coal and biomass, from storage yards to boiler feed systems, ensuring uninterrupted plant operation.
- Ports and terminals for loading and unloading bulk cargo like grains, fertilizers, and minerals between ships, barges, railcars, and storage silos.
- Steel plants and foundries for moving raw materials (iron ore, coke, limestone) through the production chain and handling finished products like slabs, billets, and coils.
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Bajaj Steel Industries Limited, Maharashtra
 Maharashtra, India
Food & Agriculture•Manufacturer•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Heavy Duty Belt Conveyor For Bulk Material Handling Inclined Horizontal
Heavy Duty Belt Conveyor for bulk material handling in inclined or horizontal configurations. This robust system reliably transports sluggish to free-flowing materials of various lump sizes, ensuring efficient industrial operations.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Bajaj Steel Industries Limited
 Maharashtra, India
Food & AgricultureManufacturer