
 IN
₹
Apparel & Fashion
Description
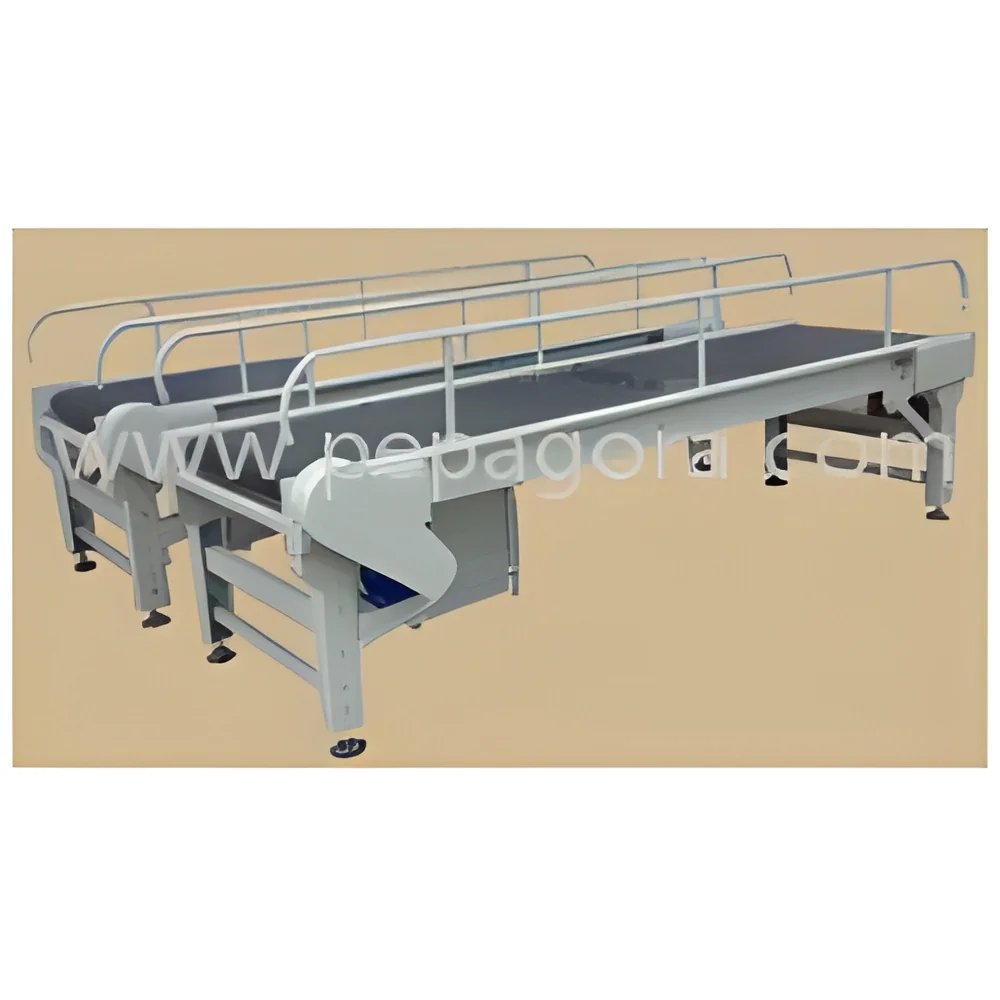
Our industrial belt conveyor systems represent advanced engineering solutions for bulk material handling challenges across diverse industrial environments. Engineered for maximum reliability and operational efficiency, these conveyors provide seamless transportation of various materials while maintaining consistent performance. The systems feature robust construction with premium components that ensure long-term durability and minimal maintenance requirements. Designed to handle multiple material types including fine chemicals, lump ore, stone, coal, and challenging substances that may pack due to moisture or react with traditional components, these conveyors maintain operational excellence even with difficult materials. The customization capabilities allow perfect adaptation to specific operational layouts and material handling requirements without compromising performance.

These belt conveyor systems serve critical functions across multiple industrial sectors including mining operat...
Our industrial belt conveyor systems represent advanced engineering solutions for bulk material handling challenges across diverse industrial environments. Engineered for maximum reliability and operational efficiency, these conveyors provide seamless transportation of various materials while maintaining consistent performance. The systems feature robust construction with premium components that ensure long-term durability and minimal maintenance requirements. Designed to handle multiple material types including fine chemicals, lump ore, stone, coal, and challenging substances that may pack due to moisture or react with traditional components, these conveyors maintain operational excellence even with difficult materials. The customization capabilities allow perfect adaptation to specific operational layouts and material handling requirements without compromising performance.

These belt conveyor systems serve critical functions across multiple industrial sectors including mining operations, manufacturing plants, agricultural processing, construction projects, and logistics facilities. In mining environments, they efficiently transport extracted materials from excavation points to processing facilities while handling heavy loads and abrasive substances. Manufacturing operations utilize them for moving components between production stages and assembly areas, ensuring smooth workflow continuity. Agricultural facilities benefit from their capacity to handle grains, fertilizers, and bulk food products during processing and storage operations. Construction sites depend on them for transporting sand, gravel, concrete, and building materials across extensive project areas. The systems prove particularly valuable in environments handling corrosive materials that would compromise traditional conveyor systems, making them essential for chemical processing and specialized industrial applications requiring material integrity.

The business value of our belt conveyor systems centers on their exceptional reliability and operational efficiency that directly impact bottom-line performance. They significantly reduce manual handling costs while increasing throughput capacity and maintaining consistent material flow throughout operations. The reduced maintenance requirements and durable construction translate to lower total cost of ownership and minimal operational downtime, providing substantial return on investment. Customization options ensure perfect alignment with specific operational needs, while the ability to handle diverse materials provides operational flexibility for evolving business requirements. These systems represent strategic investments in operational excellence, delivering consistent performance and reliability that serious industrial operators demand for their critical material handling operations across various sectors and applications.

Key Features:
- Heavy-duty construction ensures reliable performance in demanding industrial environments
- Customizable design options accommodate specific layout and operational requirements
- Corrosion-resistant components handle reactive and abrasive materials effectively
- Efficient bulk material handling capacity for various product types and sizes
- Modular system design enables easy integration with existing infrastructure

Benefits:
- Enhanced operational efficiency through continuous material flow and reduced handling time
- Lower total cost of ownership with minimal maintenance requirements and durable construction
- Increased throughput capacity for improved productivity and operational output
- Flexible material handling capabilities for diverse industrial applications and requirements
- Reduced operational downtime through reliable performance and robust system design
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Industrial belt conveyor systems provide continuous material transport for demanding operations across multiple sectors. They efficiently move bulk materials including ores, grains, chemicals, and packaged goods while reducing manual handling and increasing operational throughput. The modular design allows seamless integration with existing production lines and warehouse management systems for enhanced workflow efficiency.
These robust systems handle diverse materials from fine powders to large aggregates, even under challenging environmental conditions. They perform exceptionally well with corrosive, abrasive, or moisture-sensitive products where alternative transport methods often fail. The customizable configurations support specific layout requirements and operational parameters across various industrial settings and material types.
- Mining operations for transporting coal, minerals, and extracted materials from excavation sites to processing plants
- Manufacturing facilities for moving raw materials and components between production stations and assembly lines
- Warehouse and distribution centers for efficient loading, unloading, and sorting of packaged goods and pallets
- Agricultural processing plants for handling grains, fertilizers, and bulk food products during processing and storage
- Construction sites for moving sand, gravel, concrete, and building materials across large project areas
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Canara Engineers Pvt Ltd, Maharashtra
 Maharashtra, India
Industrial Equipment & Machinery•Manufacturer•Distributor / Wholesaler
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Industrial Belt Conveyor Systems For Bulk Material Handling
Industrial belt conveyor systems for bulk material handling deliver reliable heavy-duty performance in mining, manufacturing, and logistics operations with customizable configurations for diverse industrial needs.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Canara Engineers Pvt Ltd
 Maharashtra, India
Industrial Equipment & MachineryManufacturer


