IN
₹
Description
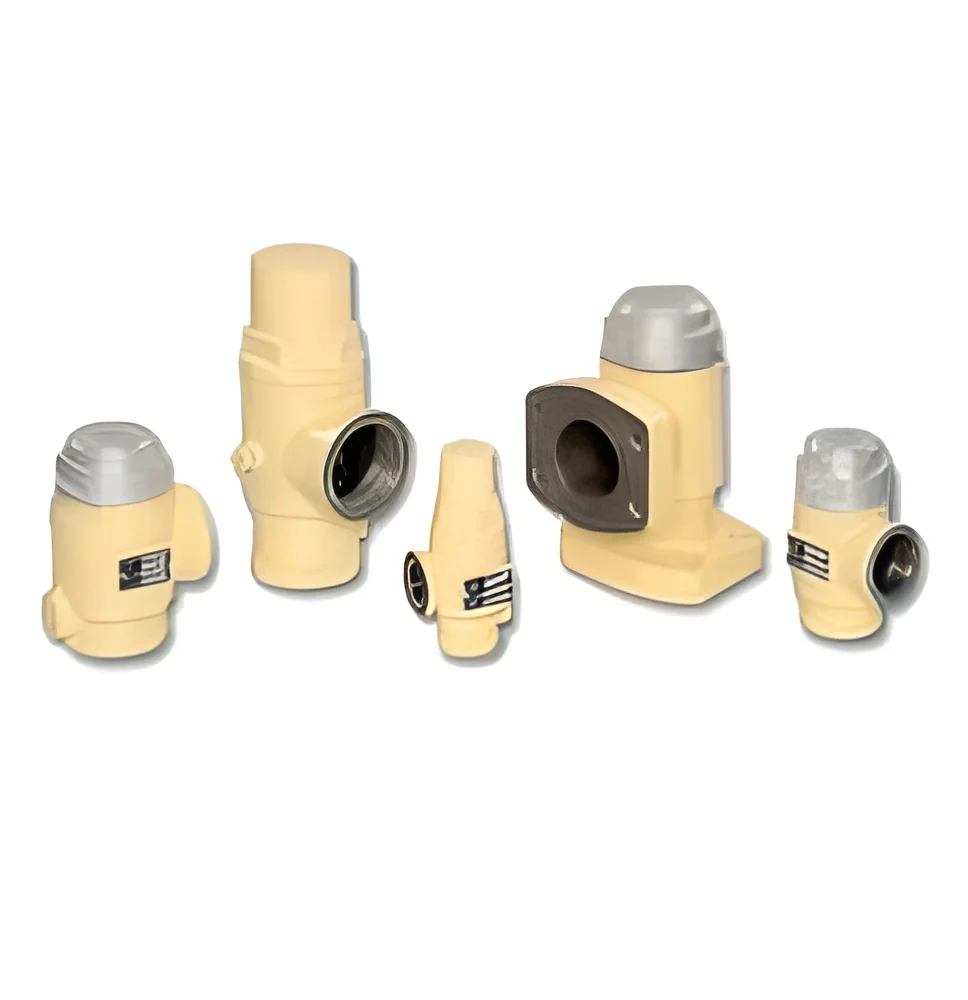
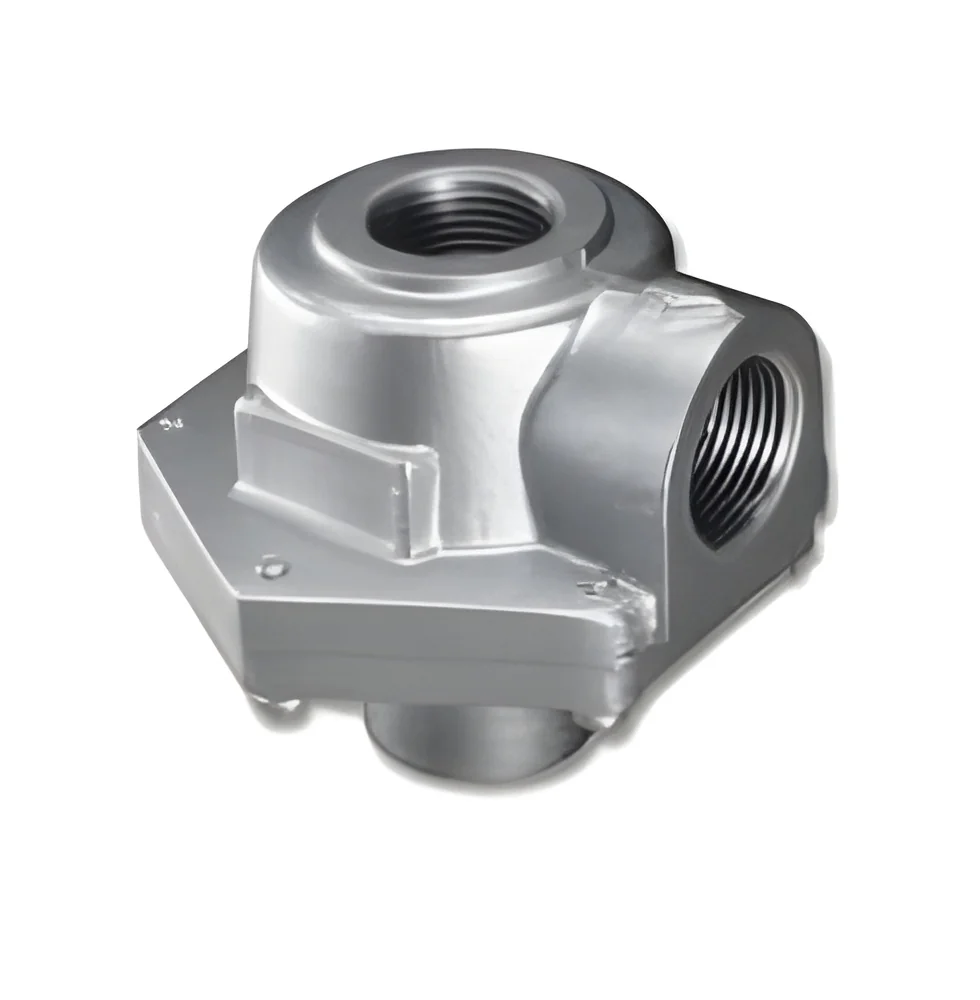
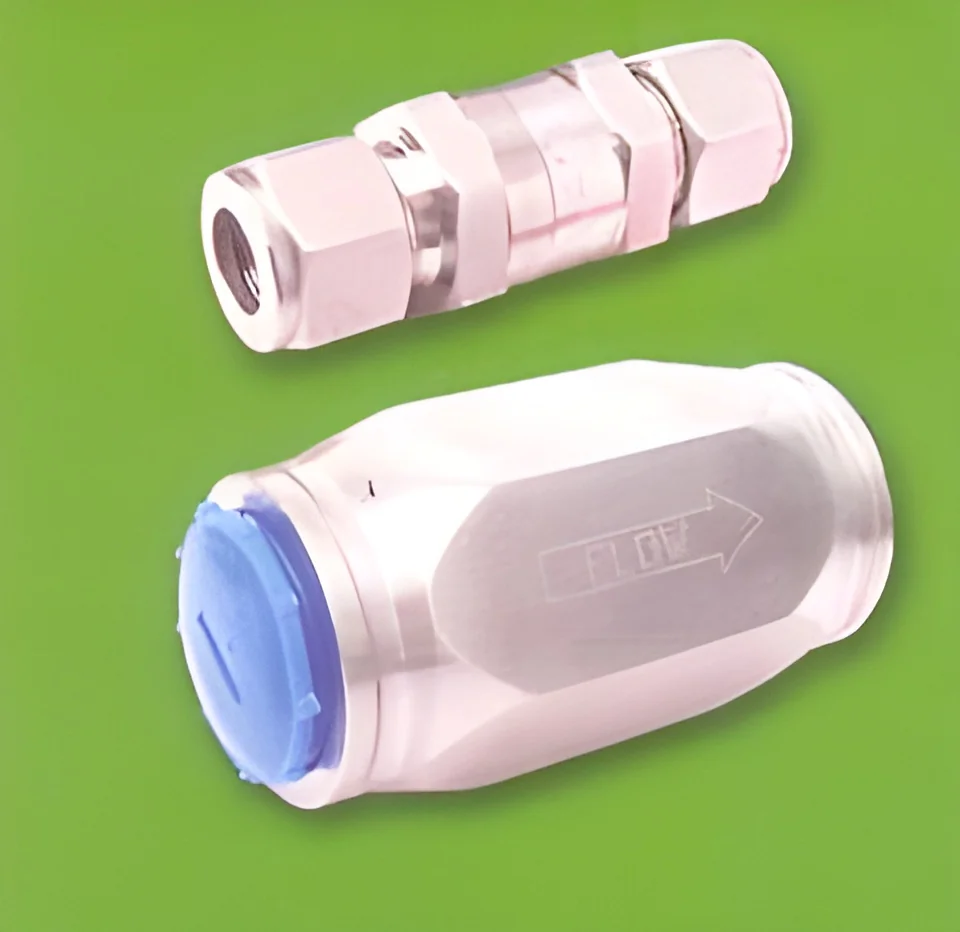
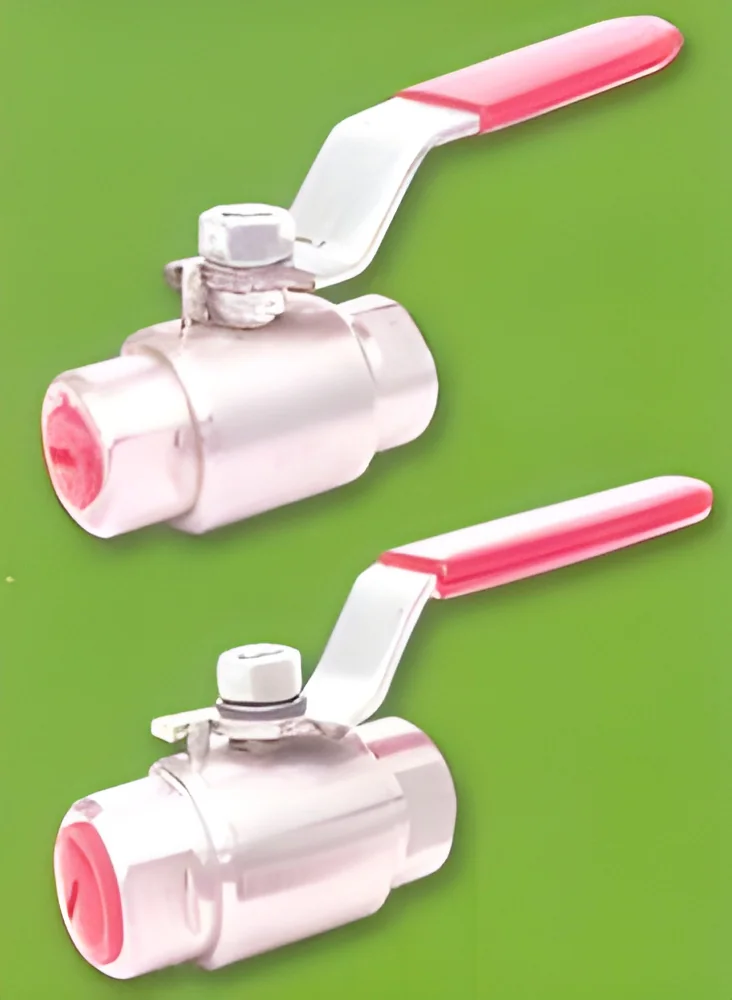
Our premium ball valves deliver exceptional shut-off capability and precise flow control specifically engineered for the food and agriculture sectors. Designed with precision engineering, they ensure reliable performance under demanding operating conditions while maintaining system integrity over extended periods. Constructed to withstand frequent operation and harsh environments, these valves offer consistent performance that operations managers can depend on for their most critical fluid control processes.

These versatile valves serve essential functions across multiple industries, including food processing plants, beverage production facilities, agricultural irrigation systems, and water treatment operations. They prove particularly valuable in chemical processing, pharmaceutical manufacturing, and industrial applications where sanitary conditions and reliable fluid control are paramount. The valves' adaptability makes them suitable for both high-pressure scenarios and standard flu...
Our premium ball valves deliver exceptional shut-off capability and precise flow control specifically engineered for the food and agriculture sectors. Designed with precision engineering, they ensure reliable performance under demanding operating conditions while maintaining system integrity over extended periods. Constructed to withstand frequent operation and harsh environments, these valves offer consistent performance that operations managers can depend on for their most critical fluid control processes.

These versatile valves serve essential functions across multiple industries, including food processing plants, beverage production facilities, agricultural irrigation systems, and water treatment operations. They prove particularly valuable in chemical processing, pharmaceutical manufacturing, and industrial applications where sanitary conditions and reliable fluid control are paramount. The valves' adaptability makes them suitable for both high-pressure scenarios and standard fluid handling requirements across diverse operational environments, from small-scale processing to large industrial installations.

The operational value of our ball valves lies in their exceptional reliability, reduced maintenance requirements, and long service life, which directly translate to lower operational costs and minimized downtime. Their robust construction ensures consistent performance even under frequent use, while the comprehensive connection options allow businesses to integrate them seamlessly into existing systems. This combination of durability, flexibility, and performance makes our ball valves a practical investment for operations seeking quality fluid control solutions that deliver measurable returns through improved efficiency and reduced maintenance.

Key Features:
- Multiple end connections including screwed, flanged, and ferrule tube options for flexible installation
- Available in two, three, and four-way design configurations to suit various system layouts
- SAE standard compliant flanged ends for sizes 1.5 and above ensuring compatibility
- Robust construction engineered specifically for high-pressure industrial applications
- Durable materials and precision manufacturing for consistent long-term performance

Benefits:
- Reliable leak-free operation reduces product loss and maintains system integrity
- Extended service life minimizes replacement costs and system downtime
- Versatile connection options simplify integration into existing infrastructure
- Consistent performance under pressure ensures process reliability and safety
- Reduced maintenance requirements lower total cost of ownership over time
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
These industrial ball valves provide precise fluid control in demanding environments, ensuring leak-free operation and extended service life across various applications. Engineered for reliability in both high-pressure and standard duty scenarios, they are ideal for critical processes where consistent performance is non-negotiable.
Common uses include food processing lines, agricultural irrigation systems, and fluid transfer setups. Built to handle frequent operation while maintaining integrity, these valves reduce downtime and operational costs, making them a practical investment for businesses that depend on reliable fluid management systems.
- Food and beverage processing, including ingredient transfer and cleaning systems
- Agricultural irrigation networks, water distribution, and fertilizer injection systems
- Industrial process piping for chemical transfer and manufacturing operations
- Pharmaceutical production lines requiring sanitary fluid handling
- Water treatment plants and municipal water distribution infrastructure
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Baba Hitech Engineering, Tamil Nadu
 Tamil Nadu, India
Industrial Equipment & Machinery•Manufacturer•Retailer•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Main Markets
South Asia
Ball Valves For Food And Agriculture Industries With Multiple End Connections
Premium ball valves for food and agriculture industries offer reliable flow control with multiple end connections, sizes, and custom designs for superior performance and durability in demanding applications.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Baba Hitech Engineering
 Tamil Nadu, India
Industrial Equipment & MachineryManufacturer