IN
₹
Apparel & Fashion
Description
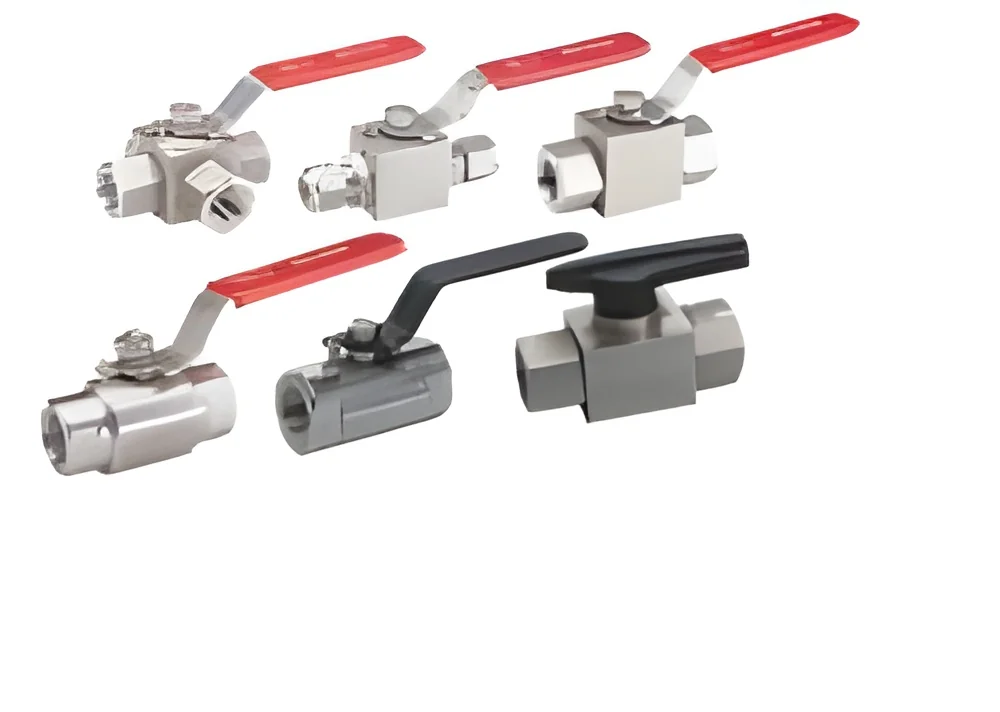
Our premium ball valves represent advanced fluid control technology specifically engineered for the food and agriculture industries. Manufactured to international quality standards, these valves offer exceptional durability and minimal maintenance requirements while delivering industry-leading performance. Designed to handle extreme operating conditions from -100°C to 650°C with pressure ratings up to 3000psi, they provide reliable shut-off and flow control solutions where hygiene, safety, and consistency are paramount. The robust construction features materials selected for compatibility with various media, ensuring long-term reliability and trouble-free operation in the most challenging environments.

These ball valves serve critical functions across multiple industries, particularly in food processing plants where they handle ingredients, cleaning solutions, and product transfer with strict hygiene compliance. In agricultural applications, they control water flow in irrigation syste...
Our premium ball valves represent advanced fluid control technology specifically engineered for the food and agriculture industries. Manufactured to international quality standards, these valves offer exceptional durability and minimal maintenance requirements while delivering industry-leading performance. Designed to handle extreme operating conditions from -100°C to 650°C with pressure ratings up to 3000psi, they provide reliable shut-off and flow control solutions where hygiene, safety, and consistency are paramount. The robust construction features materials selected for compatibility with various media, ensuring long-term reliability and trouble-free operation in the most challenging environments.

These ball valves serve critical functions across multiple industries, particularly in food processing plants where they handle ingredients, cleaning solutions, and product transfer with strict hygiene compliance. In agricultural applications, they control water flow in irrigation systems, manage chemical distribution in spraying equipment, and operate in dairy processing machinery. The pharmaceutical and chemical industries utilize these valves for precise fluid handling in manufacturing processes, while water treatment facilities rely on them for purification system controls. Their versatility extends to beverage production, maintaining sanitary conditions while handling various liquids under different pressure and temperature requirements.

The business value of these ball valves lies in their exceptional reliability and cost-effectiveness throughout their entire lifecycle. Engineered for durability, they significantly reduce maintenance costs and operational downtime, providing excellent return on investment. Each valve undergoes rigorous factory testing using advanced methods to ensure compliance with specific operational needs. Proper valve selection considering system design, material compatibility, and operational parameters guarantees safe and efficient performance, making them a trusted choice for importers, distributors, and wholesalers seeking quality fluid control solutions.

Key Features:
- High-pressure rating up to 3000psi for demanding industrial applications
- Extreme temperature resistance from -100°C to 650°C for versatile operation
- Durable construction with minimal maintenance requirements for long service life
- Food-grade materials compliant with industry hygiene and safety standards
- Leak-proof design ensuring reliable performance in critical applications

Benefits:
- Reduced operational downtime through reliable performance in extreme conditions
- Lower maintenance costs with durable construction and long service life
- Enhanced safety with strict compliance to industry standards and regulations
- Improved process efficiency with precise flow control and consistent operation
- Cost-effective solution providing excellent return on investment over time
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
These industrial ball valves deliver precise flow control in demanding liquid and gas handling systems across multiple sectors. Engineered for reliability, they perform consistently in high-pressure environments and variable temperature conditions, ensuring operational continuity and reduced downtime for critical processes. These valves meet strict hygiene and safety standards for food-grade and agricultural applications with robust construction and material compatibility for automated control systems and fluid transfer operations.
Specifically designed for food processing and agricultural operations, these ball valves provide leak-proof performance and long service life in challenging environments. Their versatility makes them ideal for process piping, ingredient handling, sanitation systems, and chemical distribution where consistent performance and durability are essential for maintaining production efficiency and operational safety.
- Food processing lines for ingredient transfer and cleaning system controls
- Agricultural irrigation systems and chemical spraying equipment
- Dairy processing plants requiring hygienic fluid handling solutions
- Beverage production facilities for liquid transfer operations
- Water treatment plants and purification system management
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
A Saluji Engineering Works, Maharashtra
 Maharashtra, India
Tools & Hardware•Manufacturer•Distributor / Wholesaler
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Food & Agriculture Ball Valves 3000psi 100C To 650C
Food & Agriculture Ball Valves handle extreme pressures up to 3000psi and temperatures from -100°C to 650°C. These durable, low-maintenance valves ensure reliable fluid control for demanding industrial applications with consistent performance.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
A Saluji Engineering Works
 Maharashtra, India
Tools & HardwareManufacturer