IN
₹
Apparel & Fashion
Description
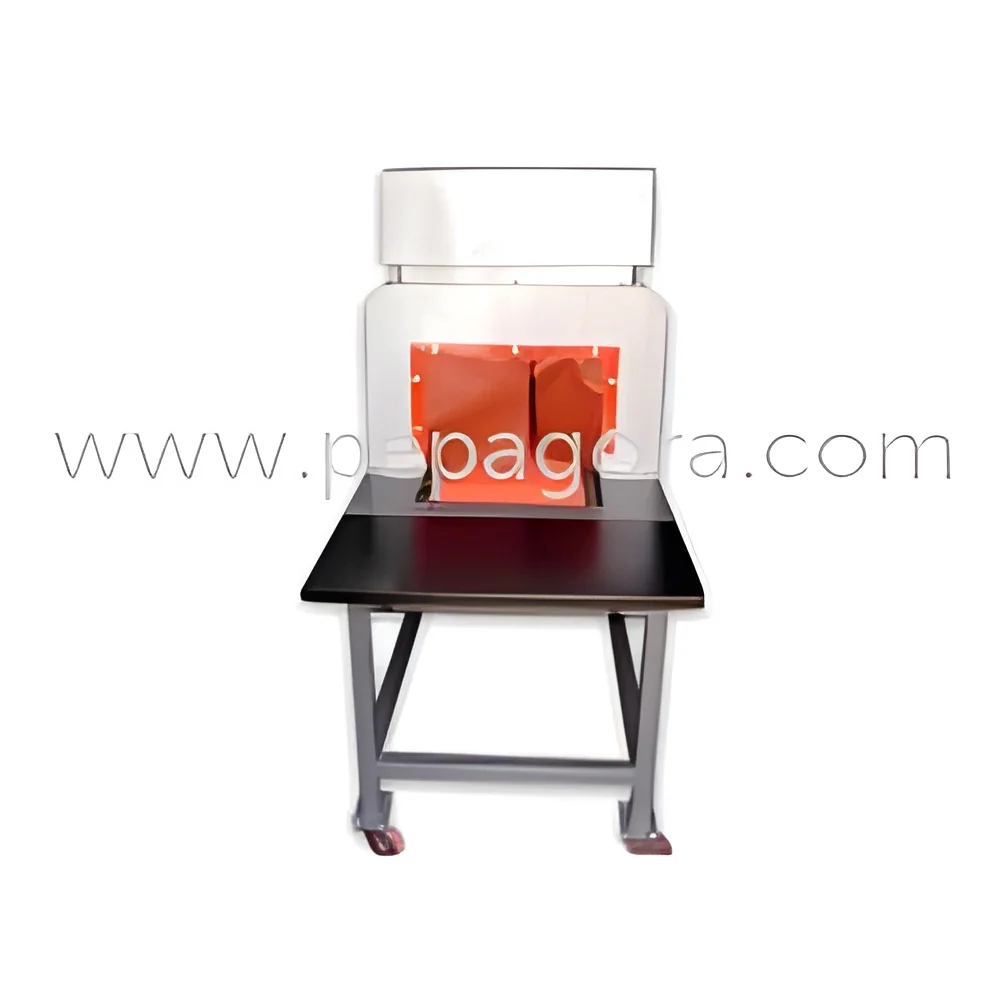
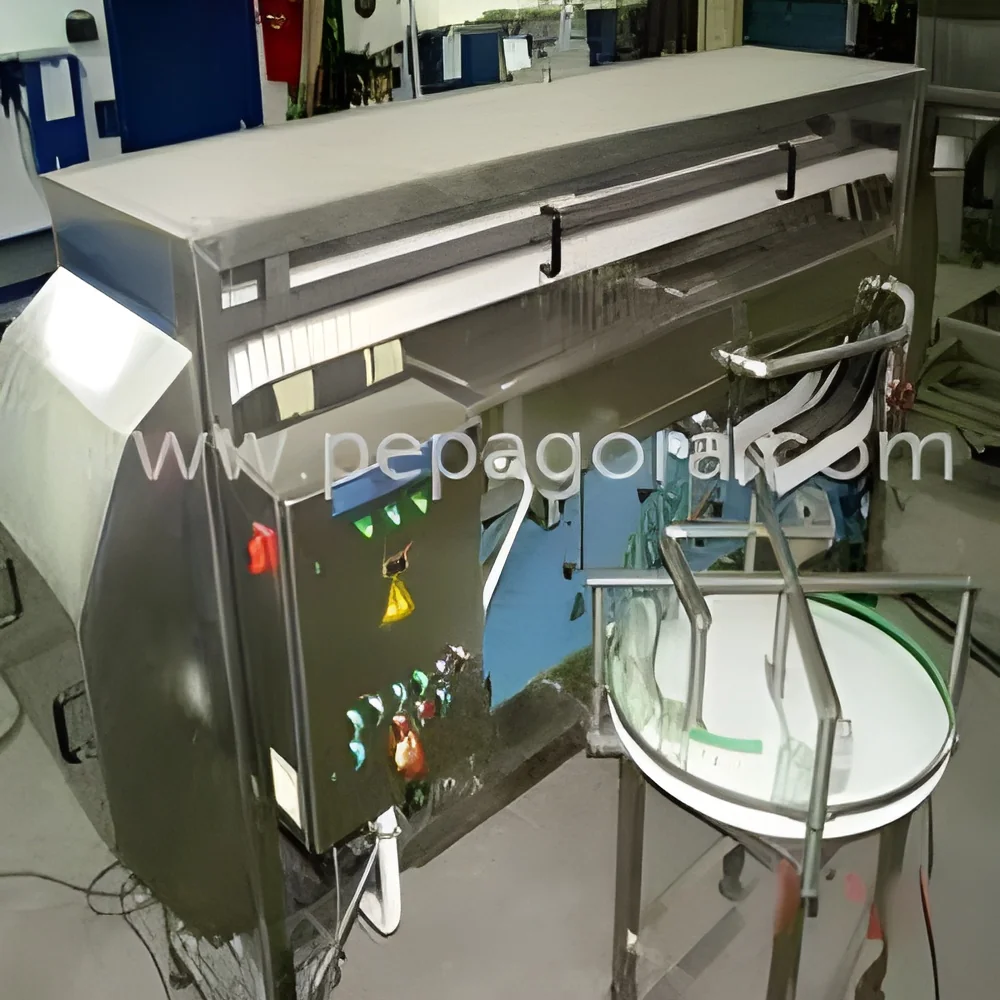
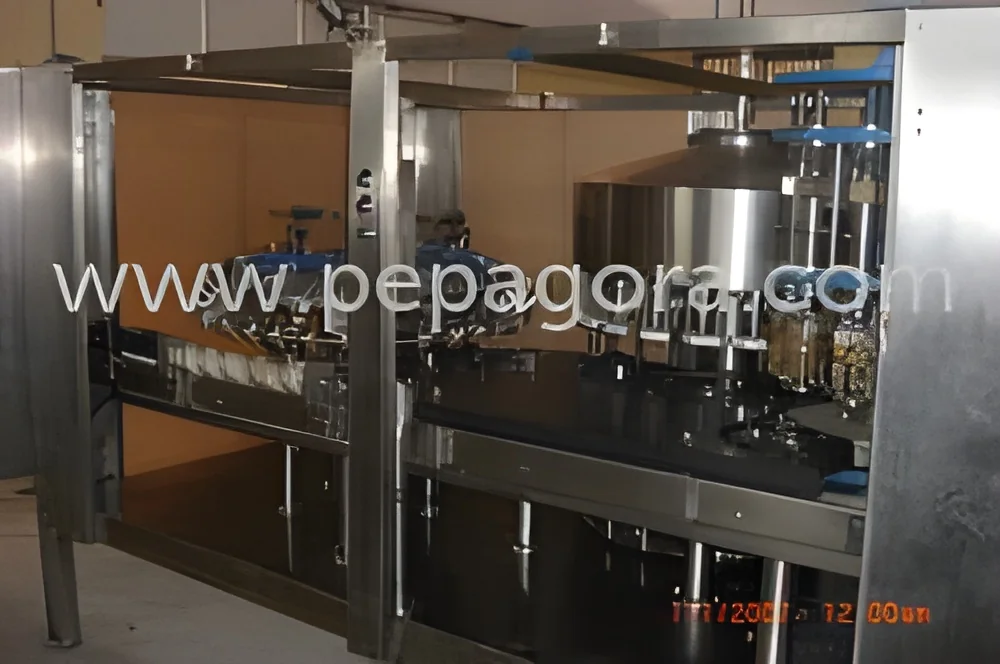
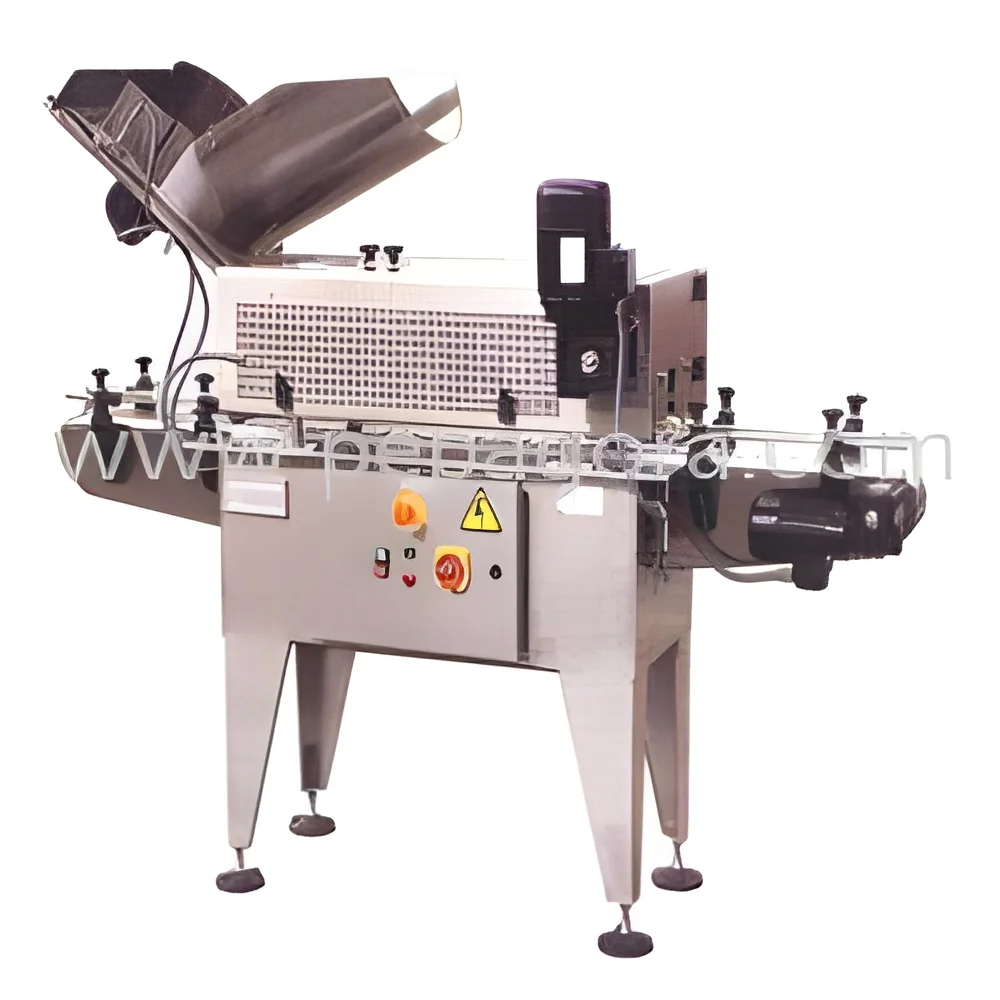
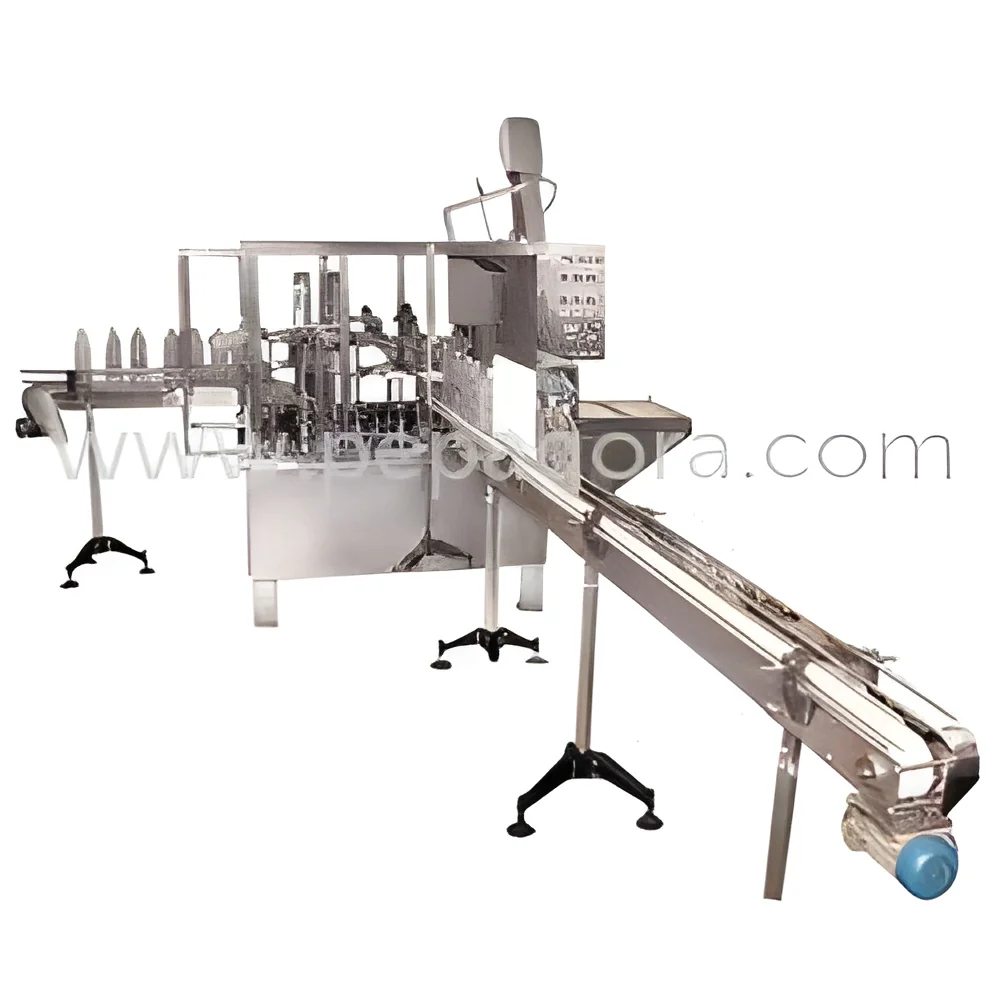
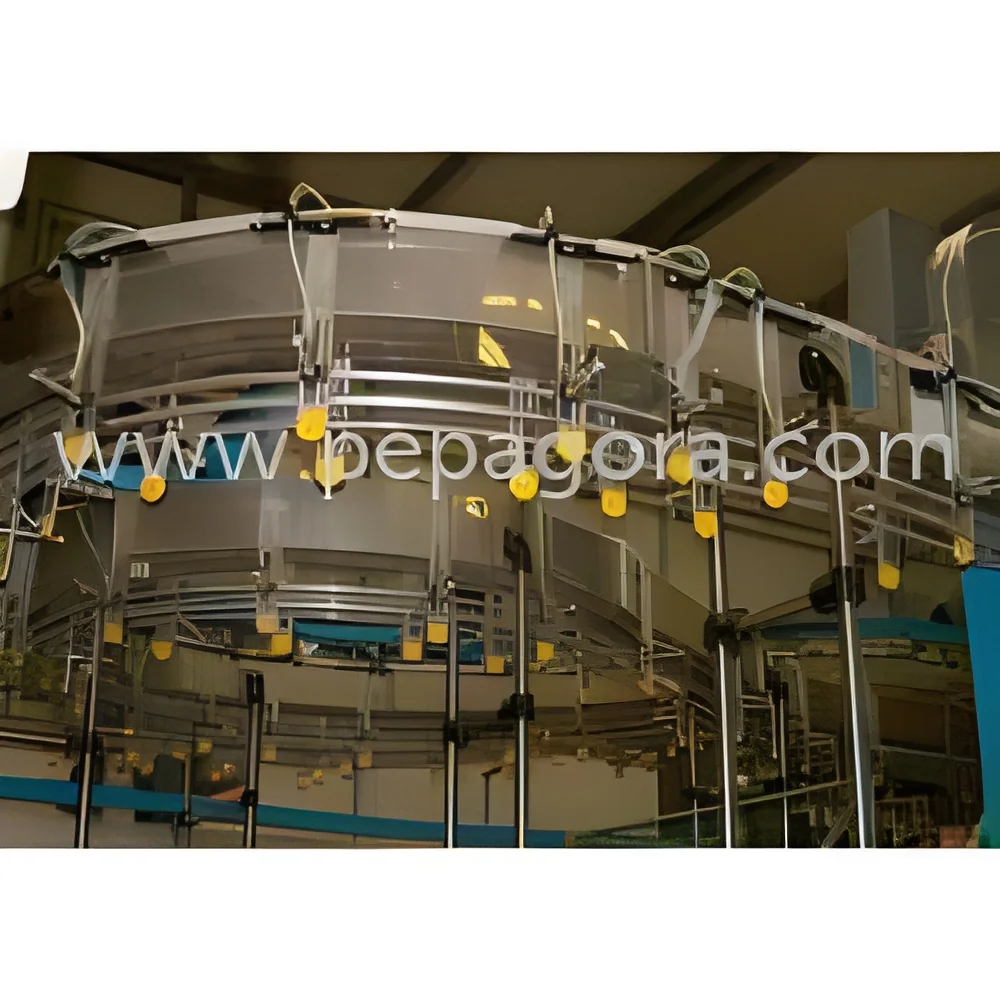
Our High Speed PET Bottle Air Conveyors represent advanced material handling technology engineered for modern manufacturing requirements. These systems utilize precisely controlled air flow to transport PET bottles efficiently along production lines without physical contact, ensuring minimal risk of damage, contamination, or labeling issues. Built with precision engineering, they support high-speed operations while maintaining exceptional stability and reducing operational noise levels. The conveyors are constructed from durable, food-grade materials that meet strict industry hygiene standards, providing long-term reliability even in demanding 24/7 production environments. This robust design ensures consistent performance across various manufacturing settings.

These air conveyors see extensive application across multiple industries, with beverage manufacturers utilizing them for water, soda, and juice bottles where hygiene and speed are critical operational factors. Pharmaceutical com...
Our High Speed PET Bottle Air Conveyors represent advanced material handling technology engineered for modern manufacturing requirements. These systems utilize precisely controlled air flow to transport PET bottles efficiently along production lines without physical contact, ensuring minimal risk of damage, contamination, or labeling issues. Built with precision engineering, they support high-speed operations while maintaining exceptional stability and reducing operational noise levels. The conveyors are constructed from durable, food-grade materials that meet strict industry hygiene standards, providing long-term reliability even in demanding 24/7 production environments. This robust design ensures consistent performance across various manufacturing settings.

These air conveyors see extensive application across multiple industries, with beverage manufacturers utilizing them for water, soda, and juice bottles where hygiene and speed are critical operational factors. Pharmaceutical companies depend on these systems for transporting medicine bottles with precision handling and contamination-free operation. The cosmetics industry employs these conveyors for shampoo, conditioner, and lotion containers requiring gentle treatment throughout production. Food processing plants benefit from their efficiency in handling dairy and edible oil bottles, while chemical manufacturers rely on them for safe transport of liquid product containers without leakage risks. Each industry values the system's ability to maintain product integrity while optimizing production flow.

The operational value of our air conveyors lies in their proven reliability and efficiency, directly impacting overall production performance and cost-effectiveness. These systems significantly reduce maintenance requirements through minimal moving parts and decrease product loss by preventing bottle damage during transport. Their energy-efficient design lowers operational expenses while supporting sustainability initiatives within manufacturing operations. The systems ensure perfect integration with existing production lines, maximizing return on investment through enhanced productivity. With demonstrated durability across various industrial environments, they offer extended service life and consistent performance, making them a strategic investment for businesses focused on improving production capacity and quality control measures.

Key Features:
- High-speed operation with precise bottle handling capabilities
- Customizable design accommodating various bottle sizes and shapes
- Food-grade construction materials meeting hygiene standards
- Minimal moving parts reducing maintenance requirements
- Adjustable air flow control for different bottle weights

Benefits:
- Enhanced production efficiency through high-speed operation
- Reduced contamination risk with contact-free transport
- Lower maintenance costs with minimal moving parts
- Flexible adaptation to various production requirements
- Improved product quality with gentle handling
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Our air conveyors provide seamless integration into high-volume PET bottle handling systems, offering gentle transport without physical contact. This design significantly reduces contamination risks while maintaining product integrity throughout production lines, making them essential for sensitive manufacturing environments where hygiene and precision are paramount.
These systems accommodate various bottle sizes and shapes, providing operational flexibility for diverse production requirements. With adjustable speed and load settings, they easily adapt to changing production demands while enhancing line efficiency and minimizing downtime during product changeovers, ensuring continuous operation across multiple shifts.
- Beverage production lines for carbonated drinks and bottled water
- Pharmaceutical packaging operations for syrup and medicine containers
- Cosmetic manufacturing facilities for shampoo and lotion bottles
- Dairy processing plants for milk and juice containers
- Chemical industry applications for safe liquid product handling
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Pack Tech Systems & Equipments, Tamil Nadu
 Tamil Nadu, India
Industrial Equipment & Machinery•Manufacturer•Distributor / Wholesaler
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
High Speed PET Bottle Air Conveyors For Beverage Pharmaceutical Cosmetic Industries
High Speed PET Bottle Air Conveyors deliver reliable transport for beverage, pharmaceutical, and cosmetic industries with precision handling and maximum load capacity for high-speed bottling lines.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Pack Tech Systems & Equipments
 Tamil Nadu, India
Industrial Equipment & MachineryManufacturer